Well that seems to point at a problem with the ways, like Peter mentioned. Somehow the table is moving (twisting, tilting) in such a way that your movement at the piece is not the same as the movement at your linear scale.
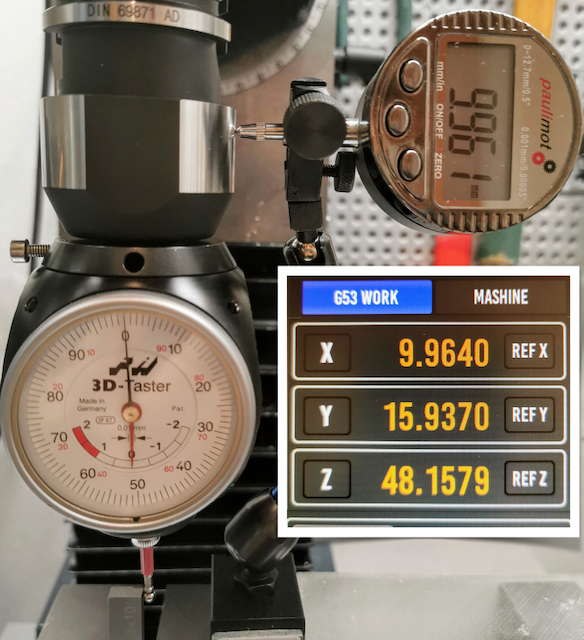
At first - thank you, guys, for the trying to help! Yesterday I spend a lot of time and check all possible mechanical parts, but without susses, It seams that mechanics work correctly. But ok, if mechanics are ok, than I need to search the problem by the edge finder gauge. One more tests with the following results:
As you can see I used 10.01mm parallel, because my digital gauge can only 12,5 mm. At first I found Zero Point on the left side, set the machine and digital gauge also to Zero, and as usual tried to measure the parallel from right side. And ... the result on the digital gauge is the same (deviation is only 0.003 what it pretty cool) as the linuxcnc displays and it has the same error as by other tests with 20mm parallels.
I reach out to you, as you are one of the few users who have found a way to make LinuxCNC work using Linear-Encoders as part of the feedback loop.
I am in the beginning of converting my Lathe, but simply can not find any guidance in what steps/sequence one should start configuring LinuxCNC when adding Linear-Scales to your CNC-Setup.
If you had to do it all over, in what steps would you recommend, editing/changing/adding what to the LinuxCNC configuration, to get the feedback-loop working & Tuning of that loop ?
I would love to find a basic manual on how this process looks like (for dummies & beginners), or even create one for this forum, once I can gather all the feedback from the best experts in these rounds, and then tried it out for myself.
Added 3 Nov 2020:
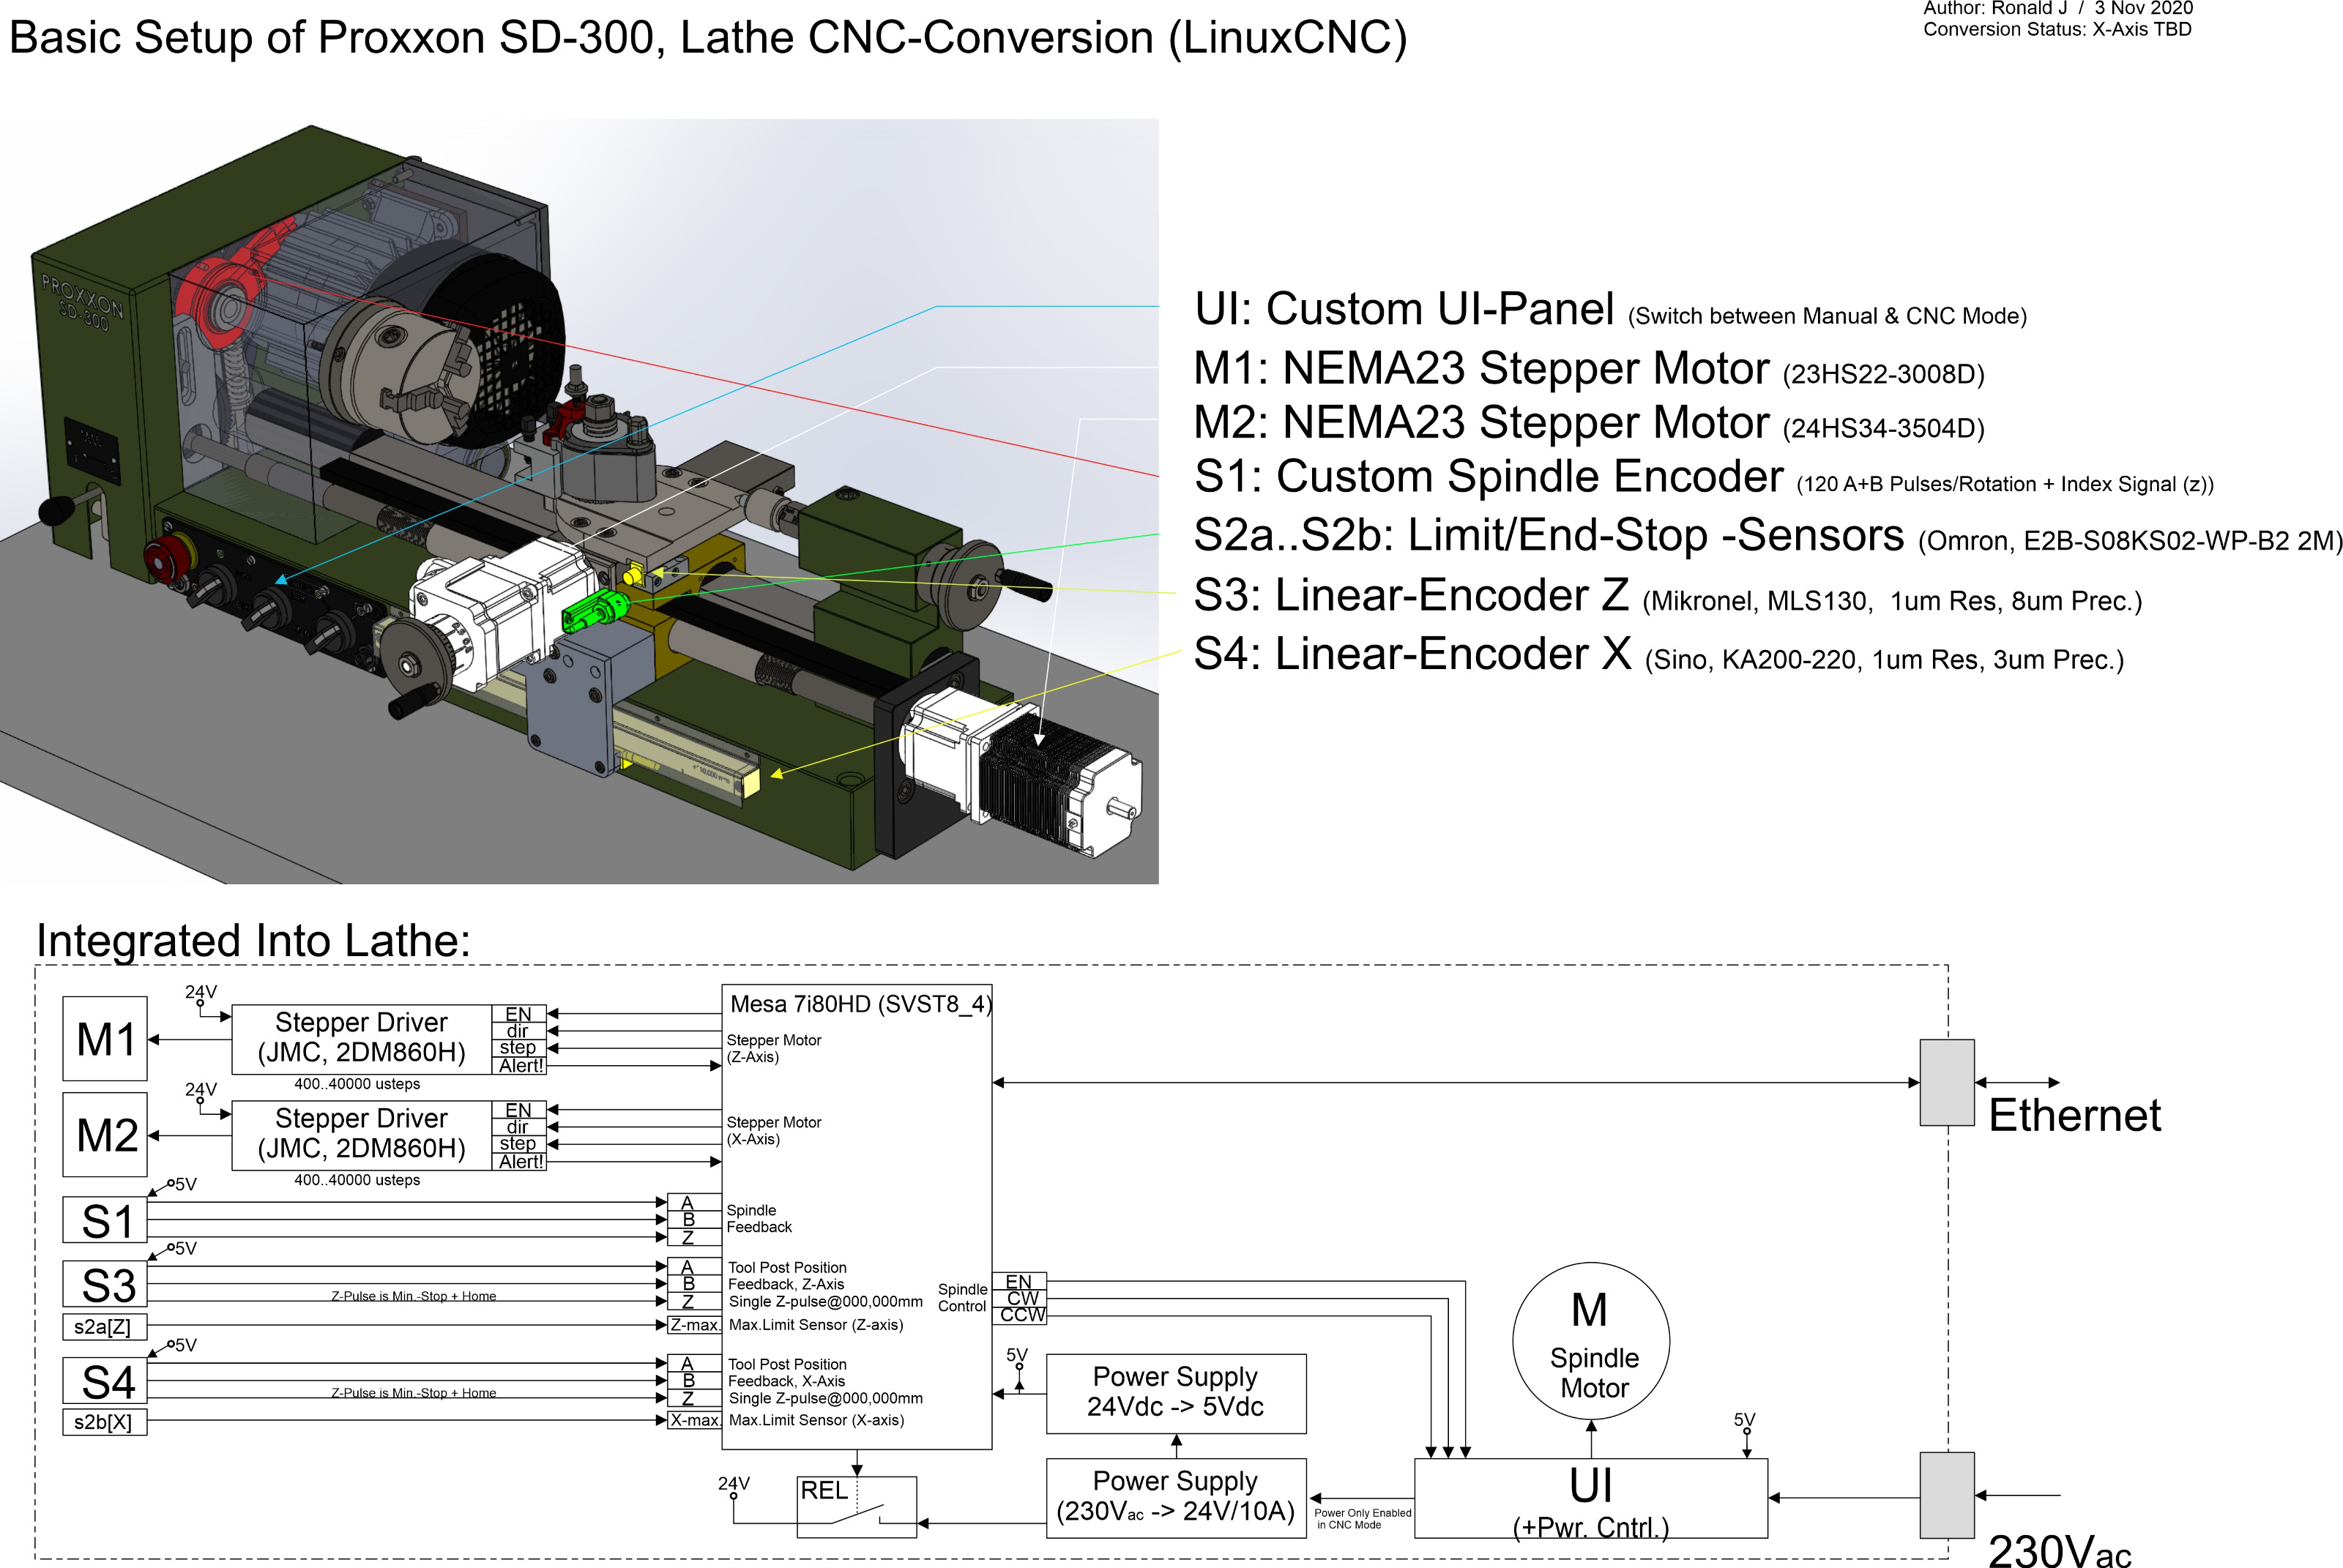
I refer to a basic setup using Stepper-motors & Feedback Sensors, in combination with any capable Mesa Card:
Thank you AndyPugh for your reply.
I added a functional Diagram to my initial post, so the basic info is there.
If any other questions pop-up, please let me know.