Wiring a chinese tool presetter.

More
7 years 9 months ago #125174 by andypugh
So, you would probably need to pull-up the yellow wire (say 1k to +24V) and then connect it to a 7i77 input. The red wire can be wired direct.

Please Log in or Create an account to join the conversation.

More
7 years 9 months ago #125217 by sliptonic
Awesome. Thank you, Andy.
I connected it with an or2 with my touch probe. I also connected the 'machine protect' connection with an or2 to the Zmin limit switch as rodw suggested.

Seems to be working perfect. Now I just need to figure out my workflow for setting tool length offsets and touching off.

Thanks guys.
The following user(s) said Thank You: rodw

Please Log in or Create an account to join the conversation.
More
7 years 6 months ago - 7 years 6 months ago #130545 by DeckelHead
I thought I'd add in an attachment that has some specs... This one is a Shina and can be purchased on Amazon (from which I downloaded the attachment). I suspect all of the different brands are made in the same factory; either that, or one is original and the others are all clones. Both concepts seem to be the Chinese manufacturing/marketing paradigm, so it is kind of hard to tell.

[edit: hmmm, your one has fewer wires, and mine definitely has an LED, so apparently the units are different... Have you gotten the software part of the preset working? I'm curious how the whole 'insert a new tool, go and preset it so you verify you have the right tool in' part gets added to LinuxCNC and works]

Anyhow, here you go....
Last edit: 7 years 6 months ago by DeckelHead.

Please Log in or Create an account to join the conversation.

More
7 years 6 months ago - 7 years 6 months ago #130555 by pl7i92
you can also red the Parameter VAR out and give it a Go for the Rest towards the Setter
as a G91 move

BEST practice for me in Education here is to get a TOOL with given Max length 100.00mm here RIM 10mm it is exactly the 100 +- 0,01mm
tool number 100 this is the tool that never changend the holder
WE set this to Cordinate system P6 G59 as the Tool ZERO point
then you simply call G59 Tx M6 (with Hx length set to Zero)
touch down
and enter the Different to 100 to the Tool table
THIS can be automatet as G10 L1 Px Z[100-#5323]
use a ngc to make all this to your need
Button that calls this ngc
Last edit: 7 years 6 months ago by pl7i92. Reason: new ad

Please Log in or Create an account to join the conversation.

More
7 years 5 months ago #132723 by RotarySMP
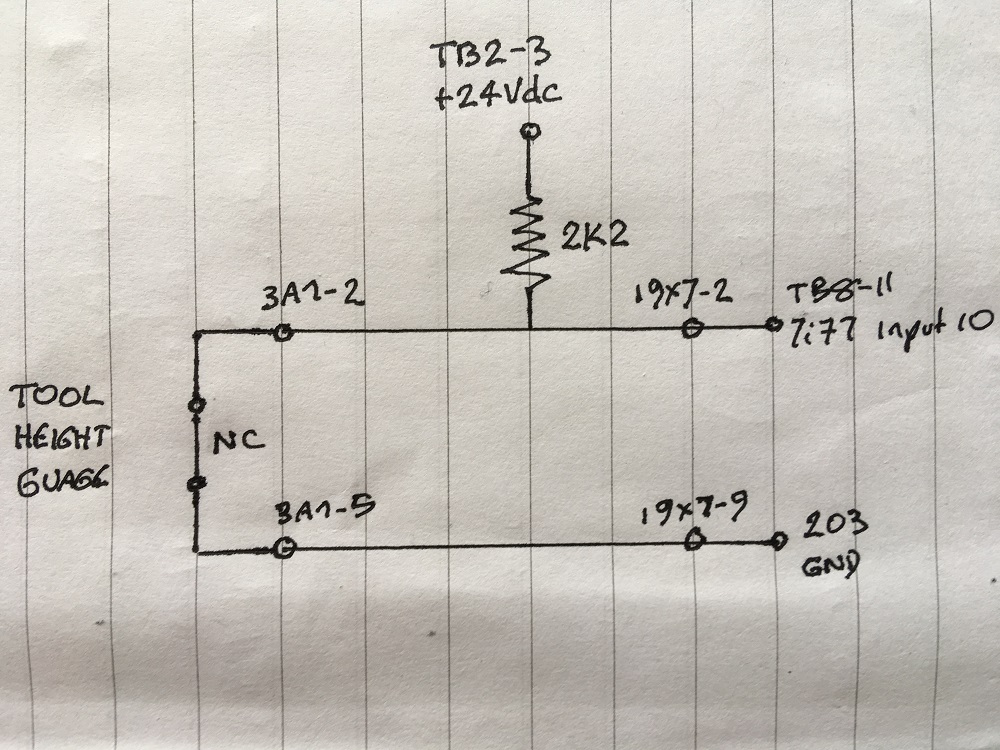
I asked this on my MAHO thread, but it didn't get noticed. Is this the correct wiring for the tool length sensor?


When I check it with HALShow, the attached 7i77 pin stays high, even when the button is pushed. I would appreciate some suggestions in trouble shooting this.
Mark

Please Log in or Create an account to join the conversation.

More
7 years 5 months ago #132728 by Mike_Eitel
3 easy questions
What show measurement betwee your points 19x7-2 and 19x7-9
Is your 7i72 field connected to 203 gnd
What happens on io pin of 7i72
Mike
The following user(s) said Thank You: RotarySMP, J Green

Please Log in or Create an account to join the conversation.

Time to create page: 0.471 seconds
Powered by Kunena Forum
