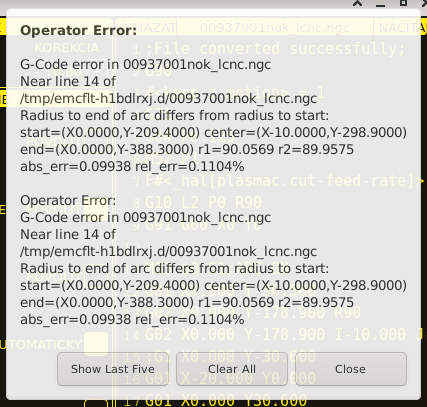
Error message "Radius to end of arc differs....etc etc"

More
5 years 7 months ago #203980 by Jocman
Glad to ear everything went fine.
BTW, at that time I fixed my problem by editing the setting for the postprocessor to linuxcnc output, more or less same as you did.

Andrea

Please Log in or Create an account to join the conversation.
More
1 year 9 months ago #319052 by gekonko
Hello,
i get the same error in QtplasmaC v2.9-238.314 RIP with EN (and SK) locale and Metric system. I have tryed to change CENTER_ARC_RADIUS_TOLERANCE_MM for my machine, but without luck. It seems that this tolerance stays default and does not change. Unfortunately, I cannot change generated tolerance from this cad/cam. This software is prahistoric but I am bound to it because it has functions for generating custom hvac components and nesting. Problem is that generated files from this cad/cam are only with 0.1mm accuracy. 


the error is reasonably small for my application

 
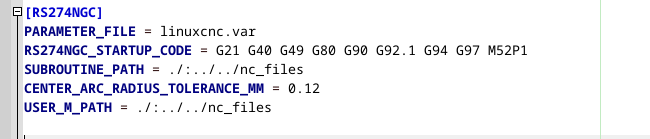
changed ini file, I have also tried to use bigger tolerance = 0.5

 
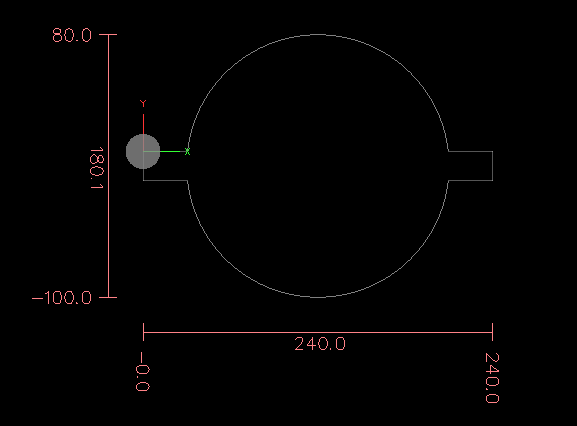
this is how the workpiece should look like.


File Attachment:

File Name: 00937001nok_lcnc.ngc
File Size:503 B


Please Log in or Create an account to join the conversation.
More
1 year 9 months ago #319056 by rodw
Try setting the arc distance mode at the beginning of the program
linuxcnc.org/docs/stable/html/gcode/g-co...ml#gcode:g90.1-g91.1
some times the code is in absolute mode and QTplasmac is expecting relative mode or vice versa.

Please Log in or Create an account to join the conversation.
More
1 year 9 months ago #319060 by gekonko
Thank you for your response, but I forgot to include it in the .ngc file - I have tested it before and it does not help in my case.

Please Log in or Create an account to join the conversation.

More
1 year 9 months ago #319065 by phillc54
Some things look odd with your gcode file:

The first N12760 should be commented out.
The second N12760 should have a J value of -89.450, not -89.500
N12770 should not be commented out.
The second N12800 should have a J value of 89.450, not -89.400

This comment at the top ";File converted successfully;" hints that a conversion was done somewhere, I don't think that it was successful.

This gcode loads:
Warning: Spoiler!


Please Log in or Create an account to join the conversation.

More
1 year 9 months ago #319102 by gekonko
@phillc54:
I really shouldnt post at midnight. You are right. Lines with R90 were added by me manually and should be commented out.

"The second N12760 should have a J value of -89.450, not -89.500"
- yes and no, really. From the CAM the precision is fixed to 0.1 so therefore it is "correct" in this case. I really just need to adjust tolerance in linuxcnc somehow, because no possibility to change presision in cam. 

The source G-code is originally generated for esab NCE290. ";File converted successfully;" Means, it went trough parser which converts it to linuxcnc readable code without unknown command confilct (values are not checked).

If you are interested, there is complete program from CAM.


File Attachment:

File Name: pre00937001.txt
File Size:9.64 KB

just to show you, how the code looks before


File Attachment:

File Name: post00937001.ngc
File Size:34.22 KB

after converting to Linuxcnc readable code

Please Log in or Create an account to join the conversation.

Time to create page: 0.336 seconds
Powered by Kunena Forum
