hobbing helical gear

More
6 years 1 month ago - 6 years 1 month ago #180635 by Aciera
Replied by Aciera on topic hobbing helical gear
Do you already have an encoder on your hob spindle and a stepper/servo motor on your gear mounting shaft?

I'm sure your machine is or was able to cut helical gears. Do you know how that was done on your machine originally or is that part of your question?
Last edit: 6 years 1 month ago by Aciera.

Please Log in or Create an account to join the conversation.
More
6 years 1 month ago #180685 by jefsaro
Replied by jefsaro on topic hobbing helical gear
yes, the machine can do it originally, but when I bought it, the parts were missing to make the helical

Please Log in or Create an account to join the conversation.

More
6 years 1 month ago - 6 years 1 month ago #180688 by Aciera
Replied by Aciera on topic hobbing helical gear
You said the mechanical differential that linked the hobbing spindle to the gear blank is missing and you would like to replace that with an "electronic gear" using LinuxCNC. This can be done as Andy has demonstrated by linking the hobbing spindle by means of an encoder to a stepper motor on the blank gear mounting shaft.

Is anything else missing besides the mechanical differential to cut helical gears?

Can you read german?

And again: Do you already have an encoder on your hob spindle and a stepper/servo motor on your gear mounting shaft?

And again: Do you know how cutting helical gears was done on your machine originally?
Last edit: 6 years 1 month ago by Aciera. Reason: Clarification

Please Log in or Create an account to join the conversation.

More
6 years 1 month ago - 6 years 1 month ago #180707 by Aciera
Replied by Aciera on topic hobbing helical gear
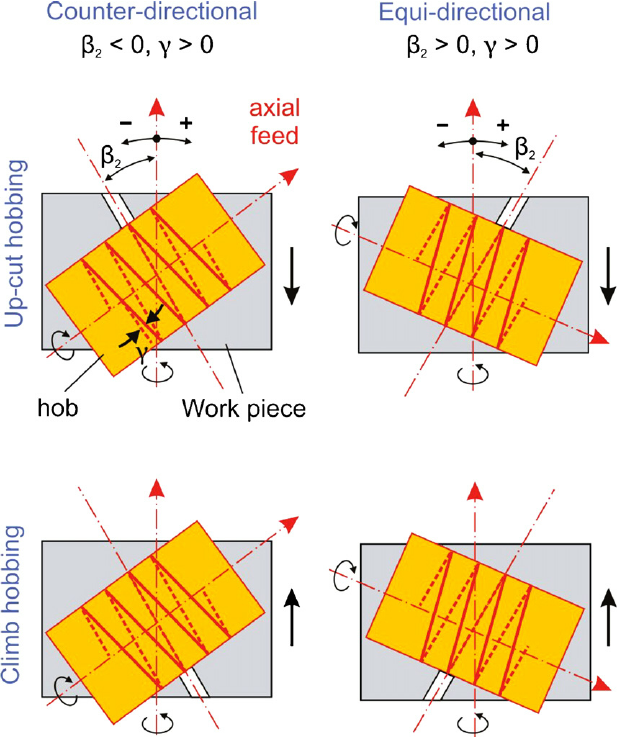
Ok, I can't make up my mind if there always needs to be an "axial feed" when cutting helical gears. I thought that wasn't necessary:


What does your book say about that?
Last edit: 6 years 1 month ago by Aciera.
The following user(s) said Thank You: tommylight

Please Log in or Create an account to join the conversation.

More
6 years 1 month ago - 6 years 1 month ago #180718 by Aciera
Replied by Aciera on topic hobbing helical gear
Phew! Now, I'm not too bad at math but after a couple hours of research on hobbing helical gears my head is spinning.
My hat is OFF to the people who invented that.:blink:

I think I'll let Andy figure that out overnight and wait for him to present his solution (including a GUI).
Last edit: 6 years 1 month ago by Aciera.

Please Log in or Create an account to join the conversation.

More
6 years 1 month ago #180734 by Henk
Replied by Henk on topic hobbing helical gear
A standard conventional pfauter hobbing machine has two sets of change gears. One to set the number of teeth and one to set the lead of the helical gears. For axial feed there is another set of gears.

When hobbing helical gears, you require additional rotation of the gear blank that is linked to the axial axis movement in order to produce the helix. On my pfauter, it is the z axis. On Andy's machine it is the X axis.

So basically, there needs to be a set ratio between the gear being cut and the hob + another ratio between z axis movement and the gear being cut. The latter is controlled by the lead of the gear being cut.

Axial feed is not necessary for cutting a helical gear on a small scale. At my workplace, we hob large gears sometimes over 10 tons. Sometimes the hob will get blunt before the cut can be completed. In this case it is convenient to shift the hob axially in order to spread the action over the entire length of the hob. This can be done without stopping the cutting process, but generally we don't do that.

Henk
The following user(s) said Thank You: CORBETT, Aciera

Please Log in or Create an account to join the conversation.

Time to create page: 0.215 seconds
Powered by Kunena Forum
