Lathe G2/G3 arc move path inaccuracy

More
3 years 8 months ago #265576 by andypugh
What is the tool orientation? Is it possible that it is set with the controlled point inside the insert, rather than on the tangent intersection.

linuxcnc.org/docs/stable/html/lathe/lath...e_tool_orientation_a

I have forgotten if you are compensating in the CAM or in the controller, but I seem to recall that you plotted the G-code path in CAD and got the right result,
I will try to find the time to plot it out myself to see if I agree....

Please Log in or Create an account to join the conversation.

More
3 years 8 months ago #265578 by agdeutschman
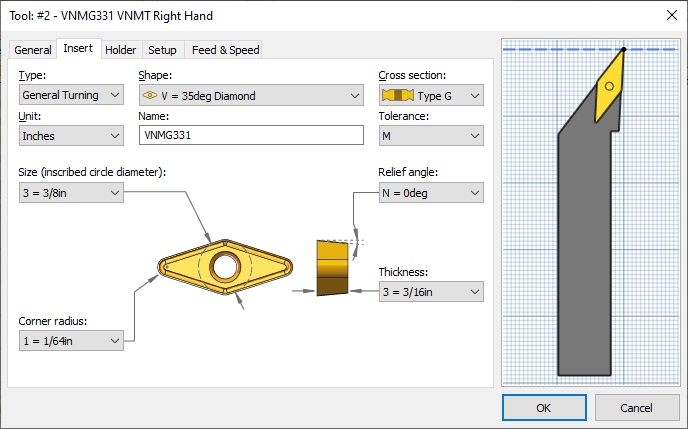
It seems odd to me that the amount my radius is off is almost exactly the tool radius for VNMG331.

Please Log in or Create an account to join the conversation.
More
3 years 8 months ago - 3 years 8 months ago #265579 by agdeutschman
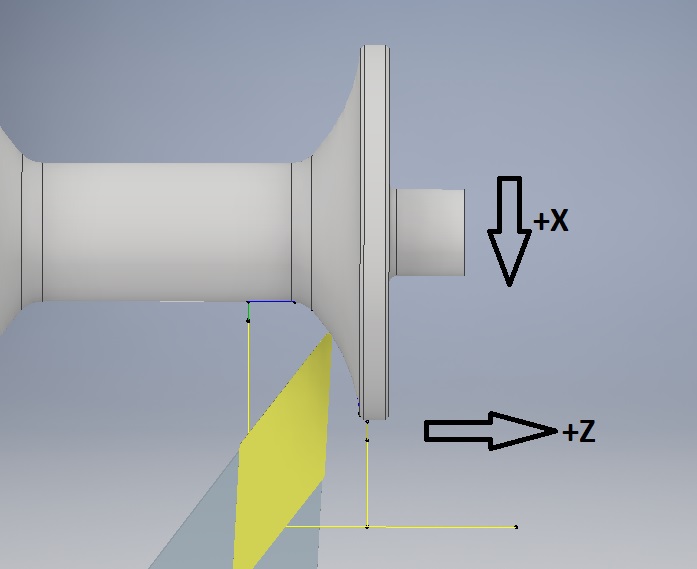
I believe for the radius I have been testing, orientation is position 1.

I am using CAM compensation, not controller.  I appreciate you taking the time to double check the path.  My tool holder style has a -3 degree side angle.


Last edit: 3 years 8 months ago by agdeutschman.

Please Log in or Create an account to join the conversation.
More
3 years 8 months ago #265608 by andypugh
Well, I am no less baffled than before....

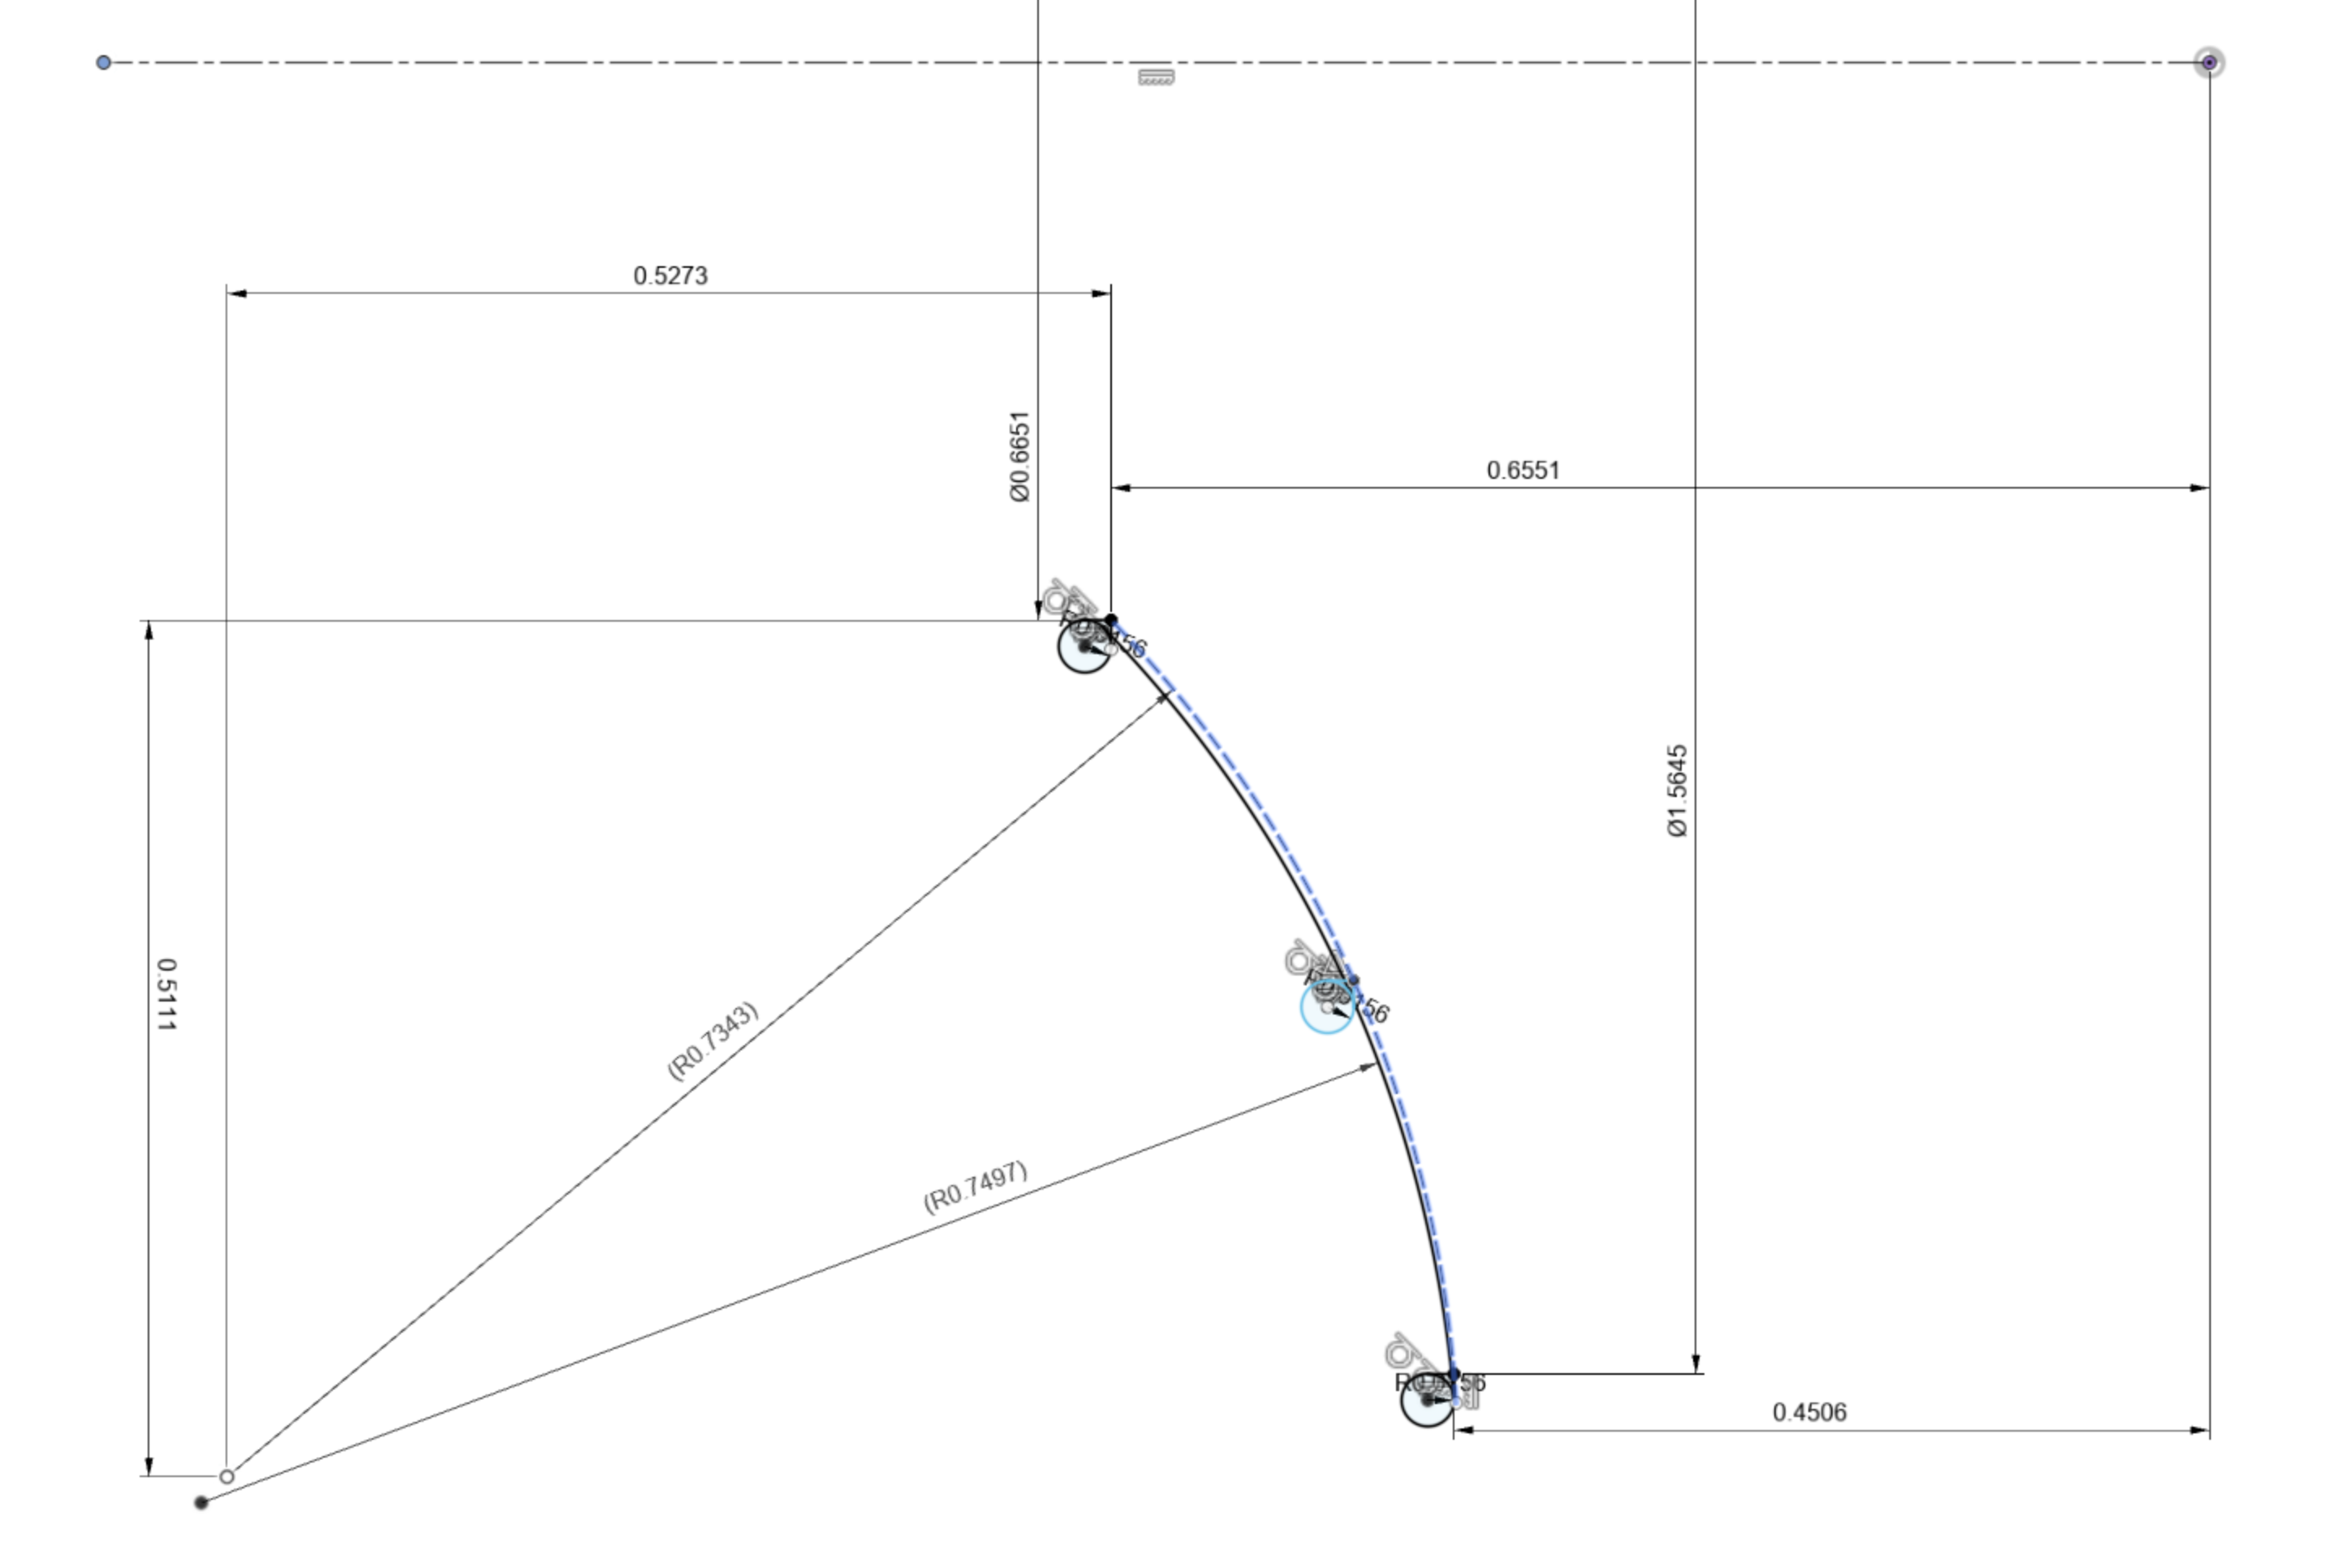
The actual radius of the controlled path is 0.734 (dotted in the picture) and that should (based on three little tool tip drawings and a tangent arc) give a .7497 radius arc. 


I have two things left to try, but they are rather clutching at straws. 

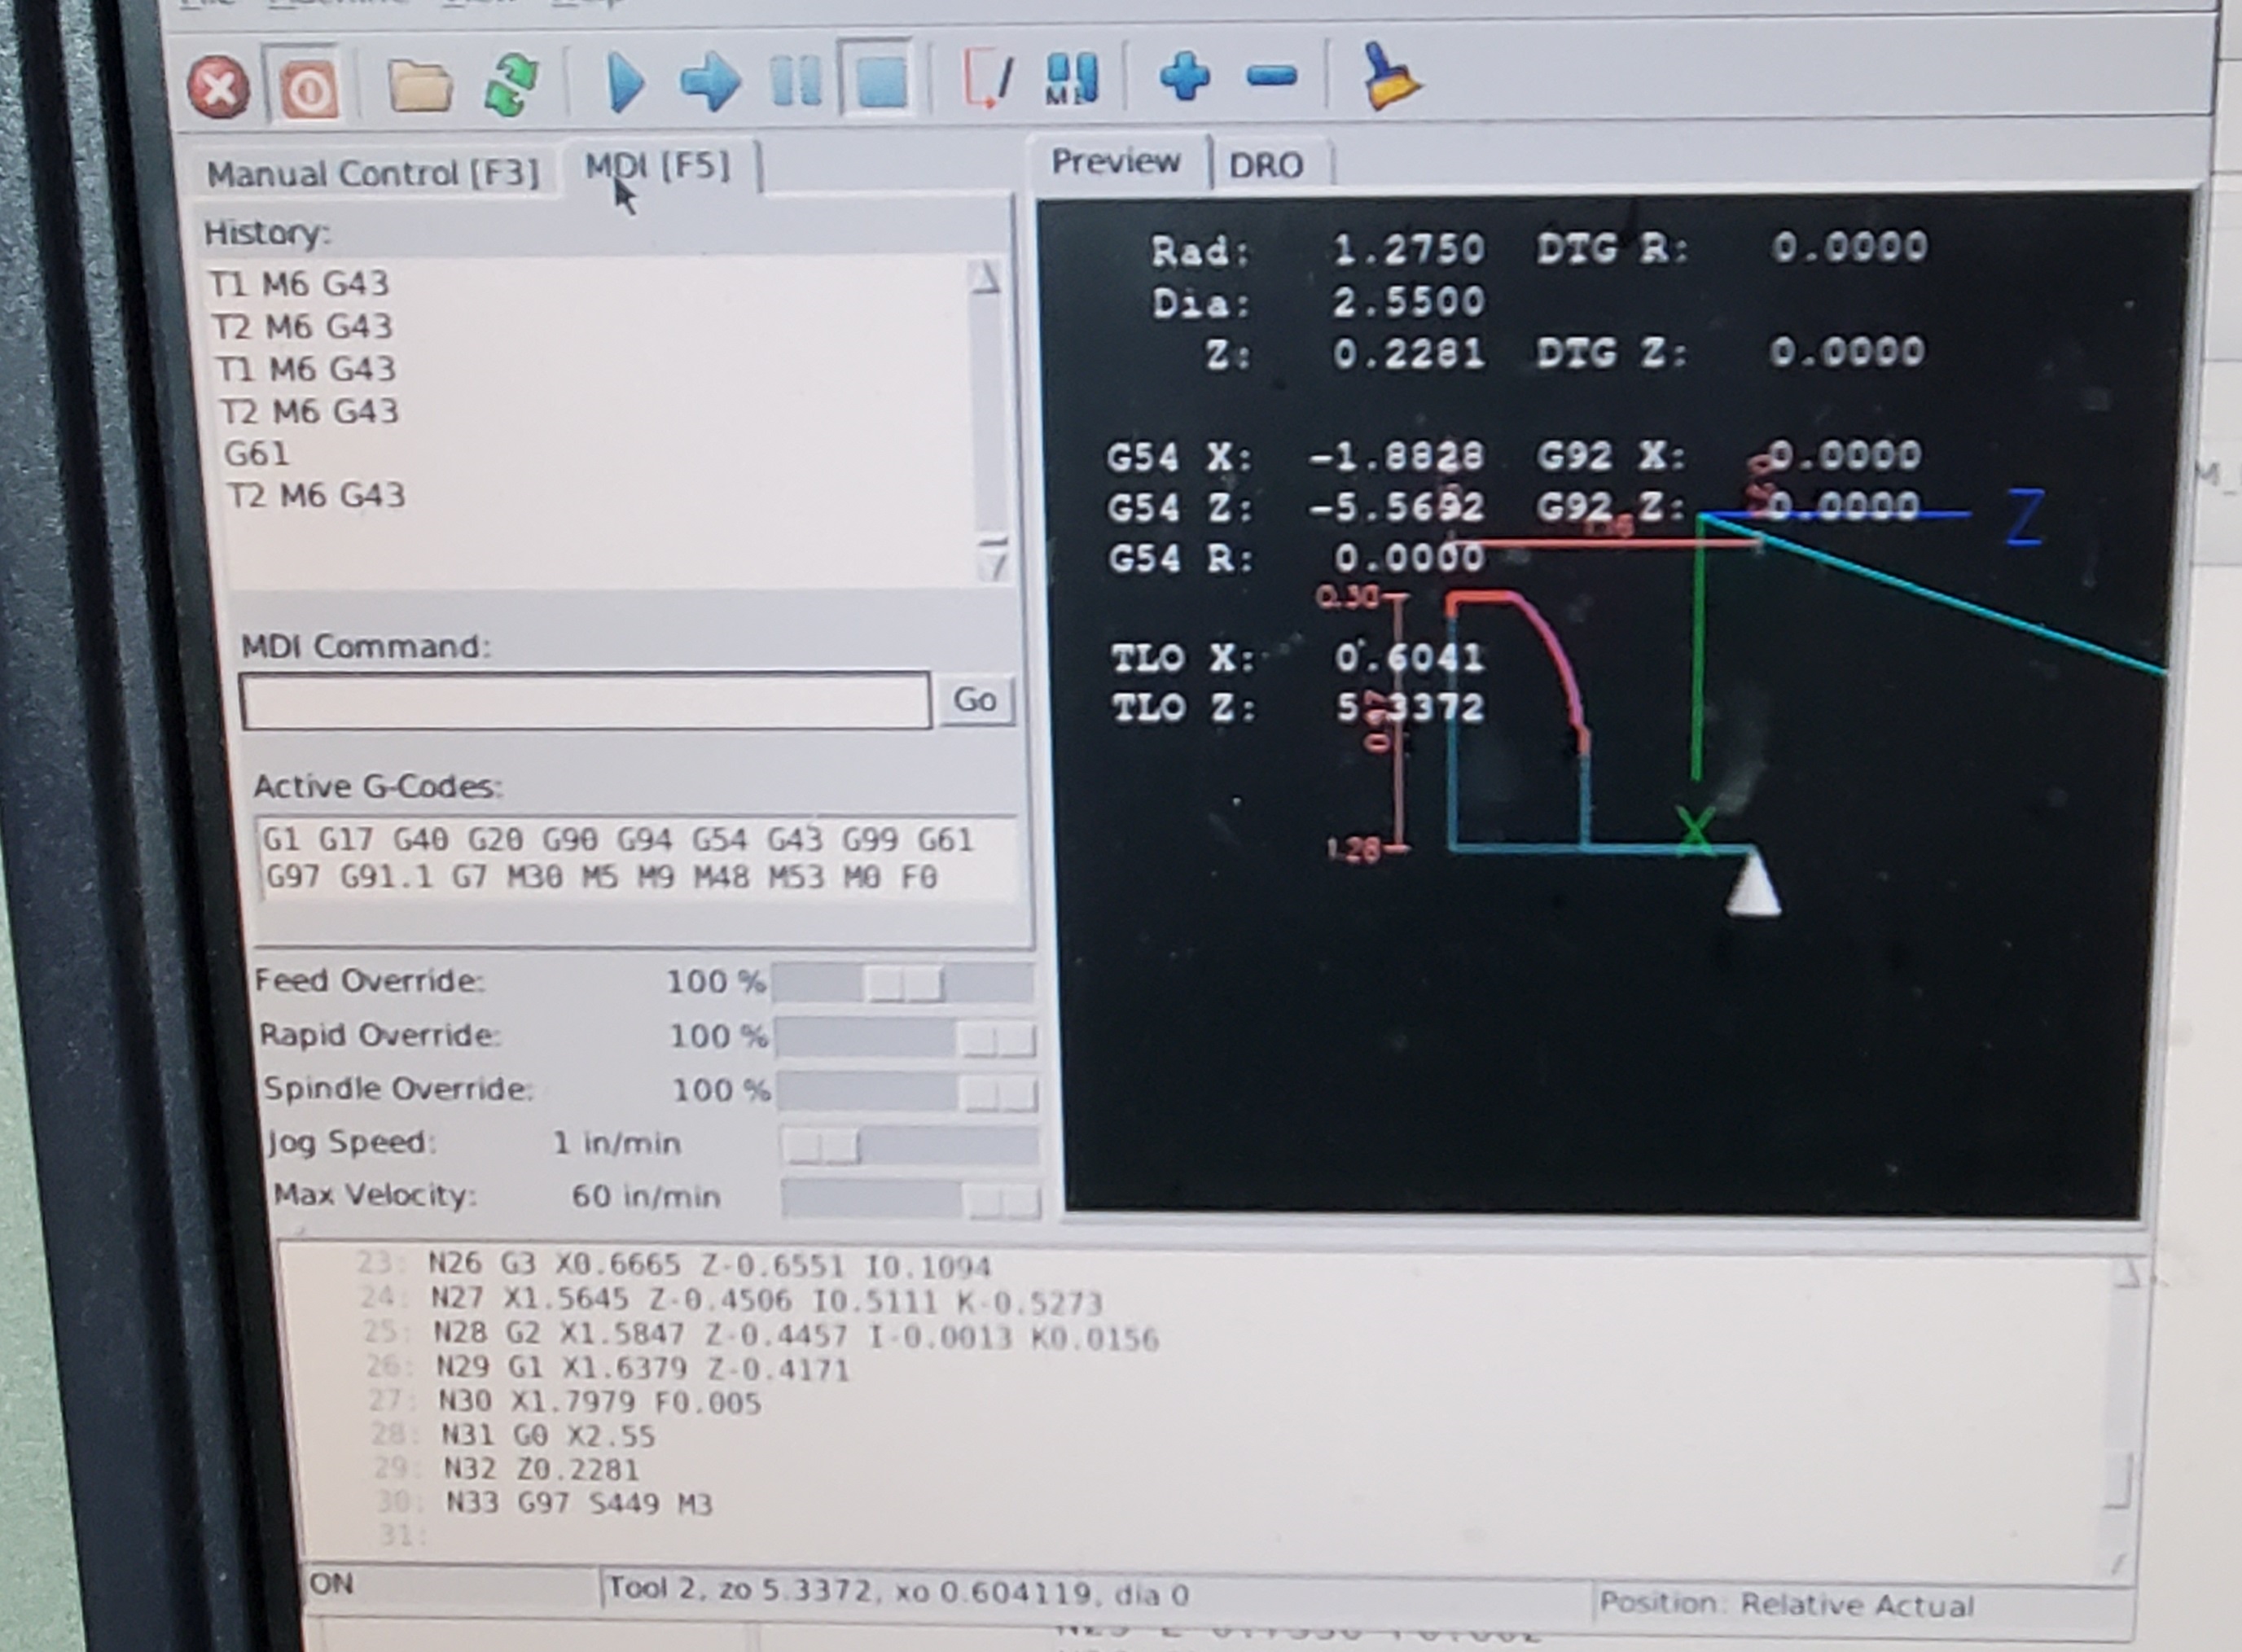
1) Try setting the tool radius in the tool table to zero. Just to be entirely sure that LinuxCNC isn't trying to do cutter comp. 
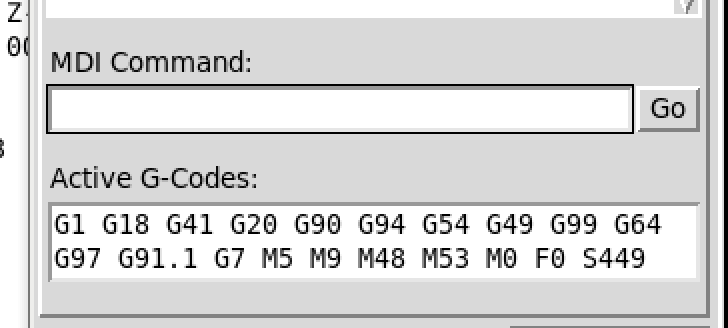
2) Try adding a G40 to the G-code to make even more sure that it isn't doing cutter comp. Though if G41 or G42 were active they should show up in the active G-codes display.


Please Log in or Create an account to join the conversation.
More
3 years 8 months ago #265615 by agdeutschman
andypugh, thanks for sketching out and verifying!     

I will attempt solutions 1 and 2 tonight and measure tomorrow morning.

Thanks!

Please Log in or Create an account to join the conversation.
More
3 years 8 months ago #265656 by agdeutschman
I set Tool 2 radius/diameter to zero in the tool table and evoked G40 at the beginning of my program.

I re-cut the profile an additional .010" Z+ with the changes.  There is no change in the profile and it still measures .734".  

Please Log in or Create an account to join the conversation.
Time to create page: 0.080 seconds
Powered by Kunena Forum
