Trajectory Planner using Ruckig Lib

More
2 years 11 months ago #285001 by Grotius
Hi Joco,

Thanks for your detailled error report.
The gcode file is from cam repository : github.com/grotius-cnc/cam/blob/main/gcode.ngc

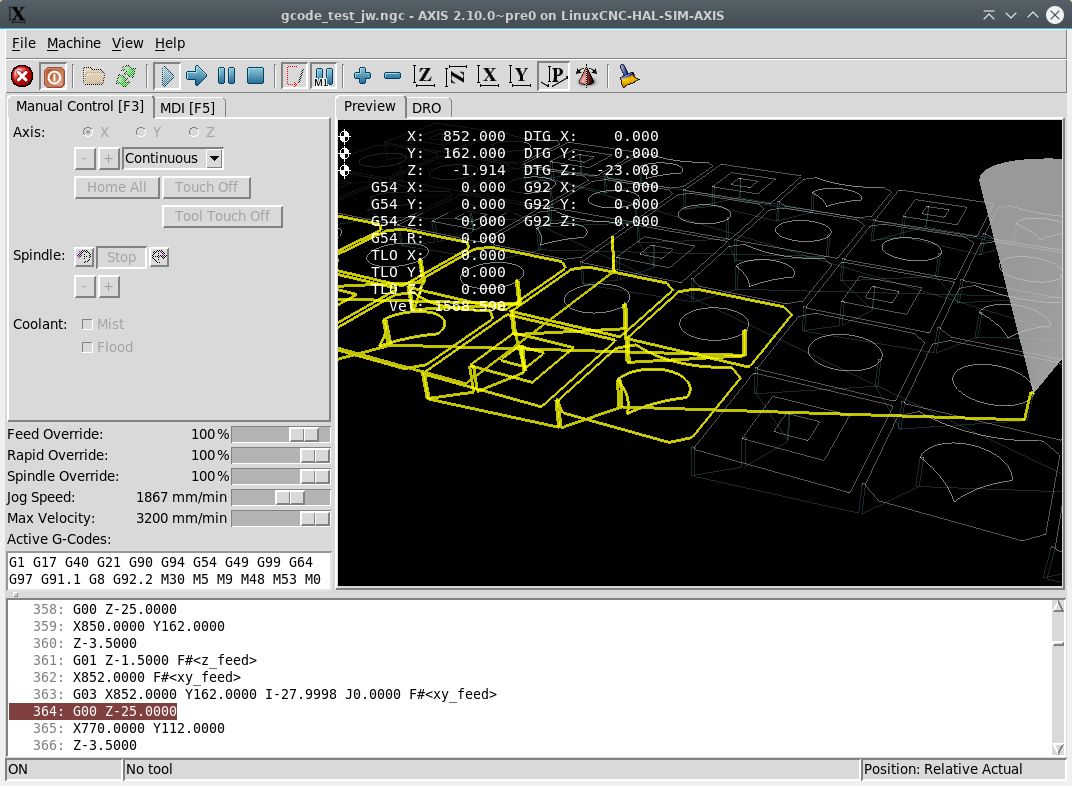
I added your modified gcode_test_jw.ngc to the source. And opened the file in axis. Then press run after home,
and error reproduced indeed.

tpAddCircle.
vector size: 6
lengt of this segment: -nan
traject lenght now: -nan
arc startpoint x: 192.000000, y: 162.000000, z: -1.500000
arc endpoint x: 192.000000, y: 162.000000, z: -1.500000
arc center x: 164.000200, y: 162.000000, z: -1.500000


It's obvious, the arc has the same start- & endpoint, wich results in a isnan output for arc lenght in this case.
So i can do 2 things here.
  1. Change it into a line when start & end are the same.
  2. Filter out this segment, trow it away
The following user(s) said Thank You: akb1212

Please Log in or Create an account to join the conversation.
More
2 years 11 months ago #285002 by Joco
So line 21 is:   G03 X192.0000 Y162.0000 I-27.9998 J0.0000 F#<xy_feed>

This essentially a circle.  Use ncviewer.com/ to step through the code file.  Really useful to visualise what is happening where.

Are you factoring the fact the fact that the arc at this line is in fact a circle or is something happening under the hood which is causing this to happen as a result of what is being produced by the ruckig library?

Cheers - J

Please Log in or Create an account to join the conversation.

More
2 years 11 months ago #285003 by Grotius
The isnan is fixed by changing isnan to 0 output. So segment's are just there, segment lenght is set to zero.
To inform you where in the source this is done :

github.com/grotius-cnc/linuxcnc/blob/884.../tp/tp_lines.cpp#L89
github.com/grotius-cnc/linuxcnc/blob/884.../tp/tp_arcs.cpp#L233

Github is updated.

Joco, it seems the rapids are below the workpiece. But the file run's oke now.
You may edit the file yourself on github.
 
 
The following user(s) said Thank You: akb1212

Please Log in or Create an account to join the conversation.

More
2 years 11 months ago - 2 years 11 months ago #285004 by Joco
Thanks - yeah its a hack as I can't set WCS to be able to have positive upward Z moves.

Normally Z would be removed on my plasma as that is all under plasmac control.  Once WCS can be set then will change.  OR is it ok to kill off Z moves entirley?  For the purposes of this test file.

J.
Last edit: 2 years 11 months ago by Joco.
The following user(s) said Thank You: Grotius

Please Log in or Create an account to join the conversation.

More
2 years 11 months ago #285005 by Grotius
@Joco,

Are you factoring the fact the fact that the arc at this line is in fact a circle or is something happening under the hood which is causing this to happen as a result of what is being produced by the ruckig library?

This zero lenght arc is produced by a cam program using cavaliercontours. Normally this would be filtered out by a function, but for no reason it's still there. It has nothing to do with our code and or ruckig lib.


Please Log in or Create an account to join the conversation.

More
2 years 11 months ago #285006 by Joco
Tested these latest adjustments: #884ce9

No apparent errors but motion on the physical machine is not happen as epected.  It seems to rapid to that "zero arc" point which is supposed to be a hole and just stops.


File Attachment:

File Name: axis-scurv...ov24.txt
File Size:255 KB


Please Log in or Create an account to join the conversation.

Time to create page: 0.220 seconds
Powered by Kunena Forum
