Gscreen - a GTK / Glade / Python based screen

More
13 years 6 months ago #32714 by LAIR82
Thats good to know,

The way it looks, I will be starting our third retrofit in about 2 weeks, and it usually takes about 9-10 weeks to rewire and program these big lathes. So in about 3 months we will have 3 big turning centers all on Linux using the Gscreen interface.

Then we are going to our first mill to convert over.

Thanks

Rick

Please Log in or Create an account to join the conversation.
More
13 years 6 months ago #33107 by jlviloria
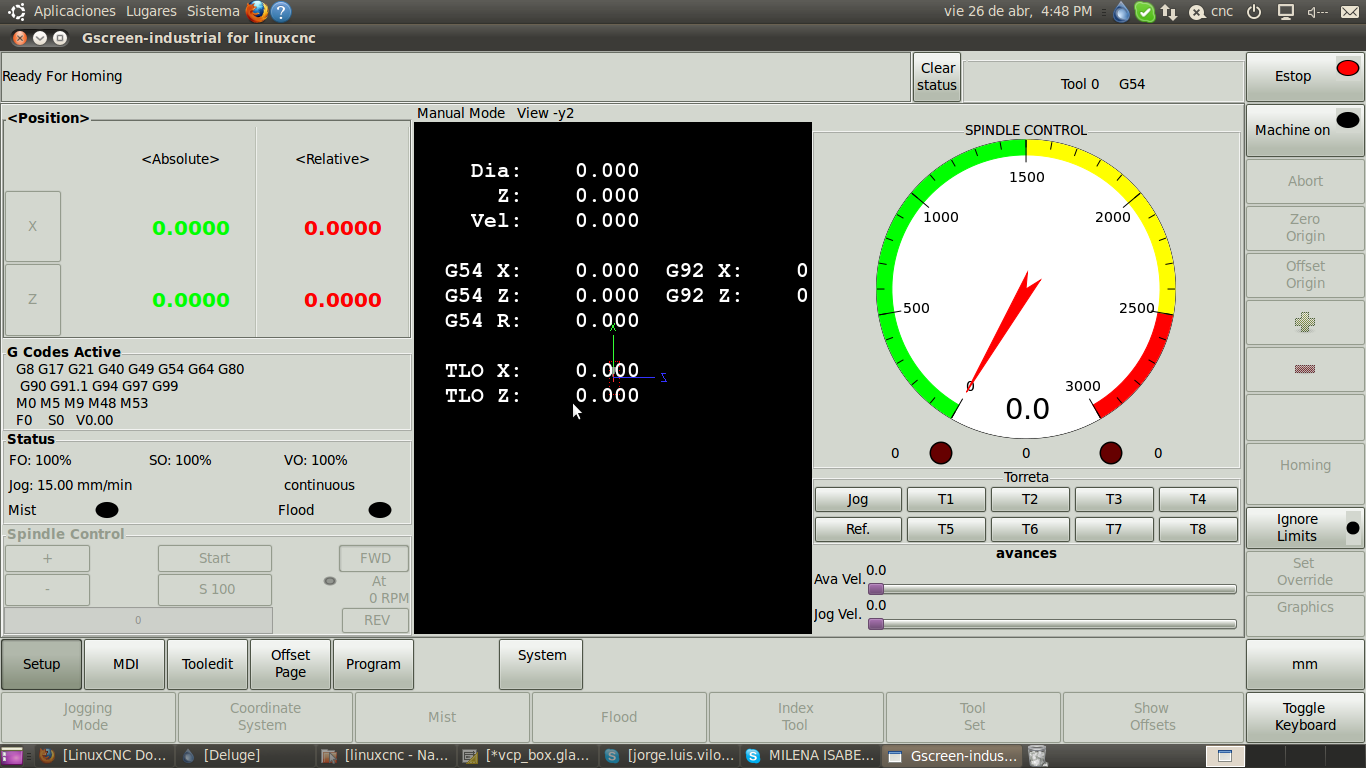
Chris, I want to change the font to a hal_dro (dro_x1, etc), as I can tell, I looked on the internet, which is by pango.FontDescription ("serif 20"), but I have tried several ways without success.

using "Industrial GScreen"

In advance thank you very much,

Jorge Viloria

Please Log in or Create an account to join the conversation.

More
13 years 6 months ago #33111 by cmorley
find the file industrial_handler.py

at about line 290 change to this:
Code:
for i in self.data.axis_list: self.widgets["dro_%s1"%i].show() self.widgets["dro_%s1"%i].modify_font(pango.FontDescription("serif 10")) self.widgets["dro_%s2"%i].show() self.widgets["dro_%s2"%i].modify_font(pango.FontDescription("serif 10")) self.widgets["dro_%s3"%i].show() self.widgets["dro_%s3"%i].modify_font(pango.FontDescription("serif 10")) self.widgets["axis_%s"%i].show() self.widgets["home_%s"%i].show()
The following user(s) said Thank You: jlviloria

Please Log in or Create an account to join the conversation.

More
13 years 6 months ago - 13 years 6 months ago #33162 by newbynobi
Hallo Chris,

searching a bug in gmoccapy I realized that the bug is not in my code.

Please do the following in industrial:

- turn on machine and reference all axis
- switch on the spindle, witch will run with the rpm set in preferences, in my case 450 rpm
- change do MDI mode and enter S2500

The spindle stops instead of speeding up to the S value.

IMHO it is a bug, spindle works well after you give an M3 command in MDI.


Norbert
Last edit: 13 years 6 months ago by newbynobi.

Please Log in or Create an account to join the conversation.

More
13 years 6 months ago #33178 by cmorley
Yes I see that behaviour.

This is Linuxcnc setting the outputs according to the active G/M codes when setting the S speed.
Since M3 or 4 is not set, it stops the spindle.

Some might say the spindle should stop when you switch from manual to MDI.
If you feel strongly about it file a bug report or discuss it on the dev mail list.

Chris M

Please Log in or Create an account to join the conversation.

More
13 years 6 months ago #33261 by jlviloria
Chris,

I'm testing GScreen-industrial successfully on my lathe.

I have some doubts.

1) When starting I get the measurement in inches, but what I have in mm, in the "DRO" of gremlin out in mm, touch him twice click the button mm / inch units.

2) Do not I have all this physical buttons on my screen. is very hard for me to jog change going forward one by one. any help at this point would be very helped, I've thought about hal_scale in vcp_box, but I could not connect to LinuxCNC.


thanks in advance.


Jorge Viloria.

Please Log in or Create an account to join the conversation.

Time to create page: 0.221 seconds
Powered by Kunena Forum
