Inssues Hole cutting

More
2 years 5 months ago #299961 by paulsao
Inssues Hole cutting was created by paulsao
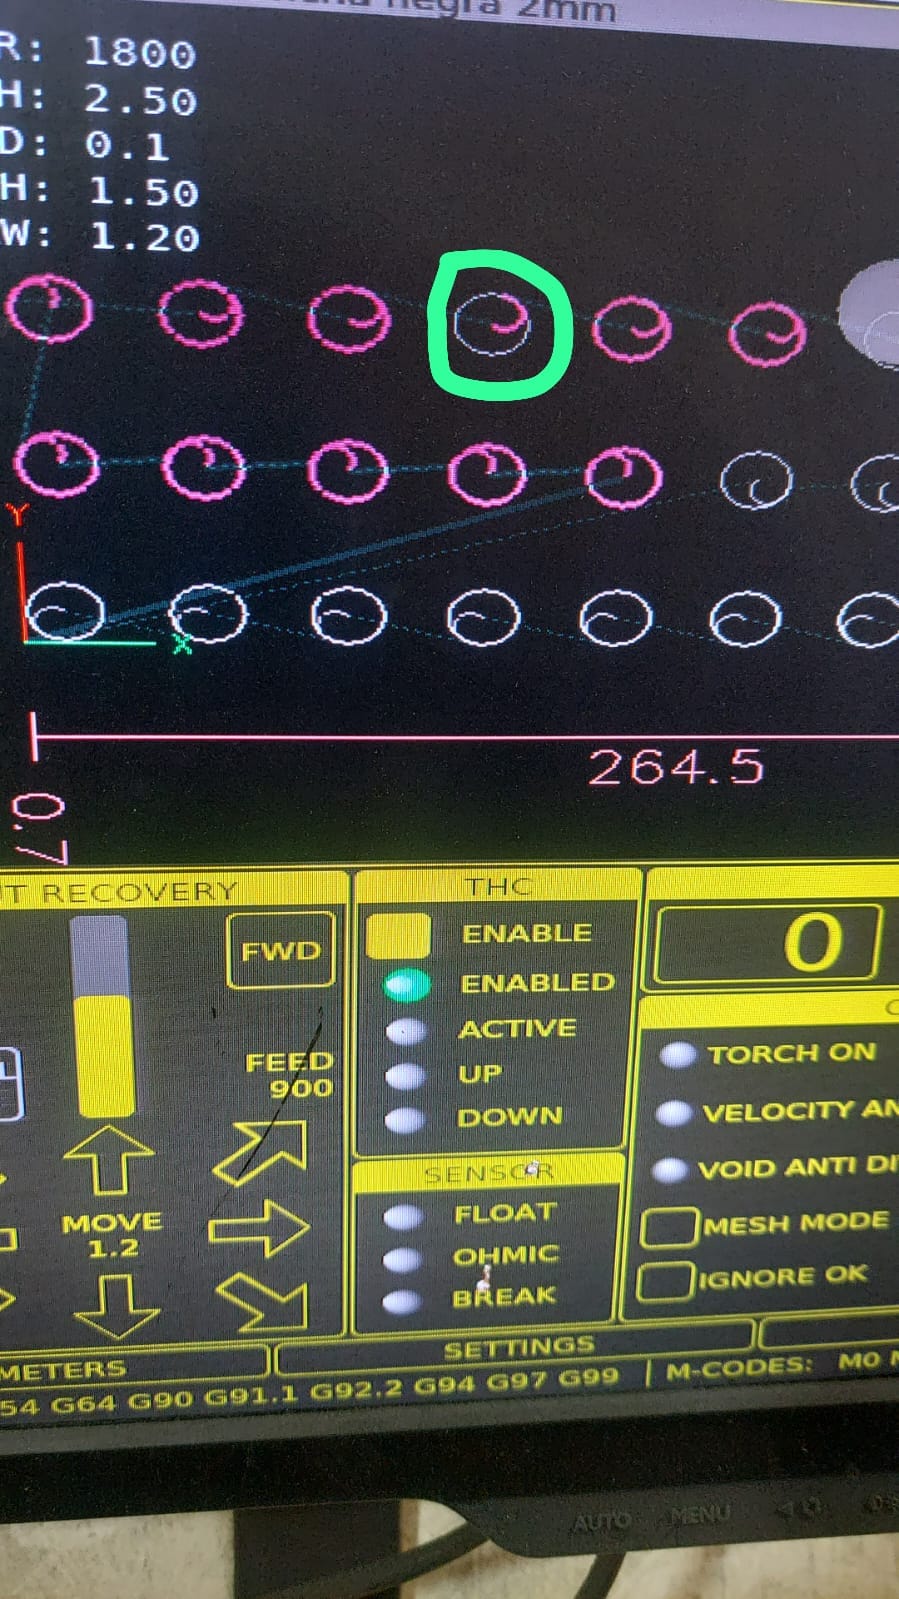
Hello.I am using shetcaam and Qtplasmac making holes with central arc entry and using plasmac's automatic circle creation Option 2. Slowing down and overcutting. The problem is that Qtplasmac detects some holes automatically and others not, and only cuts the arc as it happens in the image. This occurs only at the arch entrance. 

Please Log in or Create an account to join the conversation.

More
2 years 5 months ago #299964 by snowgoer540
Replied by snowgoer540 on topic Inssues Hole cutting
May be helpful if you could post your g-code, please. :)
The following user(s) said Thank You: paulsao

Please Log in or Create an account to join the conversation.

More
2 years 5 months ago - 2 years 5 months ago #299966 by paulsao
Replied by paulsao on topic Inssues Hole cutting
Thanks for you reply.

;     file name: holes.tap
; date and time: Mon May 06 2024    15:33:00
; postprocessor: LinuxCNC_PlasmaCv1.scpost rev: 0.5
;
;begin pre-amble
 G21 (units: metric)
 G40 (cutter compensation: off)
 G90 (distance mode: absolute)
 M52 P1 (adaptive feed: on)
 M65 P2 (enable THC)
 M65 P3 (enable torch)
 M68 E3 Q0 (velocity 100%)
 G64 P0.254 Q0.025 (tracking tolerances: 0.254mm)
#<holes>      = 2
#<h_velocity> = 50
#<h_diameter> = 42
#<oclength>   = 4
;end pre-amble
;
;begin material setup
 T0 M6 (select plasma tool)
 G43 H0 (apply tool offsets)
 M66 P3 L3 Q2 (wait for valid change)
 F#<_hal[plasmac.cut-feed-rate]>
;end material setup
 G0 X119.111 Y45.5
 M3 $0 S1 (plasma start)
 M67 E3 Q100
 G3 X113.985 Y50.627 I-2.563 J2.563
 G3 X113.985 Y50.627 I5.127 J-5.127
 M5 $0 (plasma end)
 G0 X91.333 Y45.5
 M3 $0 S1 (plasma start)
 G3 X86.207 Y50.627 I-2.563 J2.563
 G3 X86.207 Y50.627 I5.127 J-5.127
 M5 $0 (plasma end)
 G0 X63.556 Y45.5
 M3 $0 S1 (plasma start)
 G3 X58.429 Y50.627 I-2.563 J2.563
 G3 X58.429 Y50.627 I5.127 J-5.127
 M5 $0 (plasma end)
 G0 X35.778 Y45.5
 M3 $0 S1 (plasma start)
 G3 X30.651 Y50.627 I-2.563 J2.563
 G3 X30.651 Y50.627 I5.127 J-5.127
 M5 $0 (plasma end)
 G0 X8 Y45.5
 M3 $0 S1 (plasma start)
 G3 X2.873 Y50.627 I-2.563 J2.563
 G3 X2.873 Y50.627 I5.127 J-5.127
 M5 $0 (plasma end)
 G0 X8 Y83
 M3 $0 S1 (plasma start)
 G3 X2.873 Y88.127 I-2.563 J2.563
 G3 X2.873 Y88.127 I5.127 J-5.127
 M5 $0 (plasma end)
 G0 X35.778 Y83
 M3 $0 S1 (plasma start)
 G3 X40.904 Y88.127 I2.563 J2.563
 G3 X40.904 Y88.127 I-5.127 J-5.127
 M5 $0 (plasma end)
 G0 X63.556 Y83
 M3 $0 S1 (plasma start)
 G3 X68.682 Y88.127 I2.563 J2.563
 G3 X68.682 Y88.127 I-5.127 J-5.127
 M5 $0 (plasma end)
 G0 X91.333 Y83
 M3 $0 S1 (plasma start)
 G3 X96.46 Y88.127 I2.563 J2.563
 G3 X96.46 Y88.127 I-5.127 J-5.127
 M5 $0 (plasma end)
 G0 X119.111 Y83
 M3 $0 S1 (plasma start)
 G3 X124.238 Y88.127 I2.563 J2.563
 G3 X124.238 Y88.127 I-5.127 J-5.127
 M5 $0 (plasma end)
 G0 X146.889 Y83
 M3 $0 S1 (plasma start)
 G3 X152.015 Y88.127 I2.563 J2.563
 G3 X152.015 Y88.127 I-5.127 J-5.127
 M5 $0 (plasma end)
 G0 X174.667 Y83
 M3 $0 S1 (plasma start)
 G3 X179.793 Y88.127 I2.563 J2.563
 G3 X179.793 Y88.127 I-5.127 J-5.127
 M5 $0 (plasma end)
 G0 X202.444 Y83
 M3 $0 S1 (plasma start)
 G3 X207.571 Y88.127 I2.563 J2.563
 G3 X207.571 Y88.127 I-5.127 J-5.127
 M5 $0 (plasma end)
 G0 X230.222 Y83
 M3 $0 S1 (plasma start)
 G3 X235.349 Y88.127 I2.563 J2.563
 G3 X235.349 Y88.127 I-5.127 J-5.127
 M5 $0 (plasma end)
 G0 X258 Y83
 M3 $0 S1 (plasma start)
 G3 X263.127 Y88.127 I2.563 J2.563
 G3 X263.127 Y88.127 I-5.127 J-5.127
 M5 $0 (plasma end)
 G0 X258 Y45.5
 M3 $0 S1 (plasma start)
 G3 X263.127 Y40.373 I2.563 J-2.563
 G3 X263.127 Y40.373 I-5.127 J5.127
 M5 $0 (plasma end)
 G0 X258 Y8
 M3 $0 S1 (plasma start)
 G3 X263.127 Y2.873 I2.563 J-2.563
 G3 X263.127 Y2.873 I-5.127 J5.127
 M5 $0 (plasma end)
 G0 X230.222 Y8
 M3 $0 S1 (plasma start)
 G3 X225.096 Y2.873 I-2.563 J-2.563
 G3 X225.096 Y2.873 I5.127 J5.127
 M5 $0 (plasma end)
 G0 X202.444 Y8
 M3 $0 S1 (plasma start)
 G3 X197.318 Y2.873 I-2.563 J-2.563
 G3 X197.318 Y2.873 I5.127 J5.127
 M5 $0 (plasma end)
 G0 X174.667 Y8
 M3 $0 S1 (plasma start)
 G3 X169.54 Y2.873 I-2.563 J-2.563
 G3 X169.54 Y2.873 I5.127 J5.127
 M5 $0 (plasma end)
 G0 X146.889 Y8
 M3 $0 S1 (plasma start)
 G3 X141.762 Y2.873 I-2.563 J-2.563
 G3 X141.762 Y2.873 I5.127 J5.127
 M5 $0 (plasma end)
 G0 X119.111 Y8
 M3 $0 S1 (plasma start)
 G3 X113.985 Y2.873 I-2.563 J-2.563
 G3 X113.985 Y2.873 I5.127 J5.127
 M5 $0 (plasma end)
 G0 X91.333 Y8
 M3 $0 S1 (plasma start)
 G3 X86.207 Y2.873 I-2.563 J-2.563
 G3 X86.207 Y2.873 I5.127 J5.127
 M5 $0 (plasma end)
 G0 X63.556 Y8
 M3 $0 S1 (plasma start)
 G3 X58.429 Y2.873 I-2.563 J-2.563
 G3 X58.429 Y2.873 I5.127 J5.127
 M5 $0 (plasma end)
 G0 X35.778 Y8
 M3 $0 S1 (plasma start)
 G3 X30.651 Y2.873 I-2.563 J-2.563
 G3 X30.651 Y2.873 I5.127 J5.127
 M5 $0 (plasma end)
 G0 X8 Y8
 M3 $0 S1 (plasma start)
 G3 X2.873 Y2.873 I-2.563 J-2.563
 G3 X2.873 Y2.873 I5.127 J5.127
 M5 $0 (plasma end)
 G0 X146.889 Y45.5
 M3 $0 S1 (plasma start)
 G3 X152.015 Y40.373 I2.563 J-2.563
 G3 X152.015 Y40.373 I-5.127 J5.127
 M5 $0 (plasma end)
 G0 X174.667 Y45.5
 M3 $0 S1 (plasma start)
 G3 X179.793 Y40.373 I2.563 J-2.563
 G3 X179.793 Y40.373 I-5.127 J5.127
 M5 $0 (plasma end)
 G0 X202.444 Y45.5
 M3 $0 S1 (plasma start)
 G3 X207.571 Y40.373 I2.563 J-2.563
 G3 X207.571 Y40.373 I-5.127 J5.127
 M5 $0 (plasma end)
 G0 X230.222 Y45.5
 M3 $0 S1 (plasma start)
 G3 X235.349 Y40.373 I2.563 J-2.563
 G3 X235.349 Y40.373 I-5.127 J5.127
 M5 $0 (plasma end)
 ;
 ;begin post-amble
 G40 (cutter compensation: off)
 G90 (distance mode: absolute)
 M65 P2 (enable THC)
 M65 P3 (enable torch)
 M68 E3 Q0 (velocity 100%)
 M5 $-1 (backup stop)
 ;end post-amble
 ;
 ;begin statistics
 ;Pierces = 30
 ;   Cuts = 30,    Length = 1708.24mm
 ;end statistics
 ;
 M30 (end program)
 
Last edit: 2 years 5 months ago by paulsao.

Please Log in or Create an account to join the conversation.
More
2 years 5 months ago #299972 by snowgoer540
Replied by snowgoer540 on topic Inssues Hole cutting
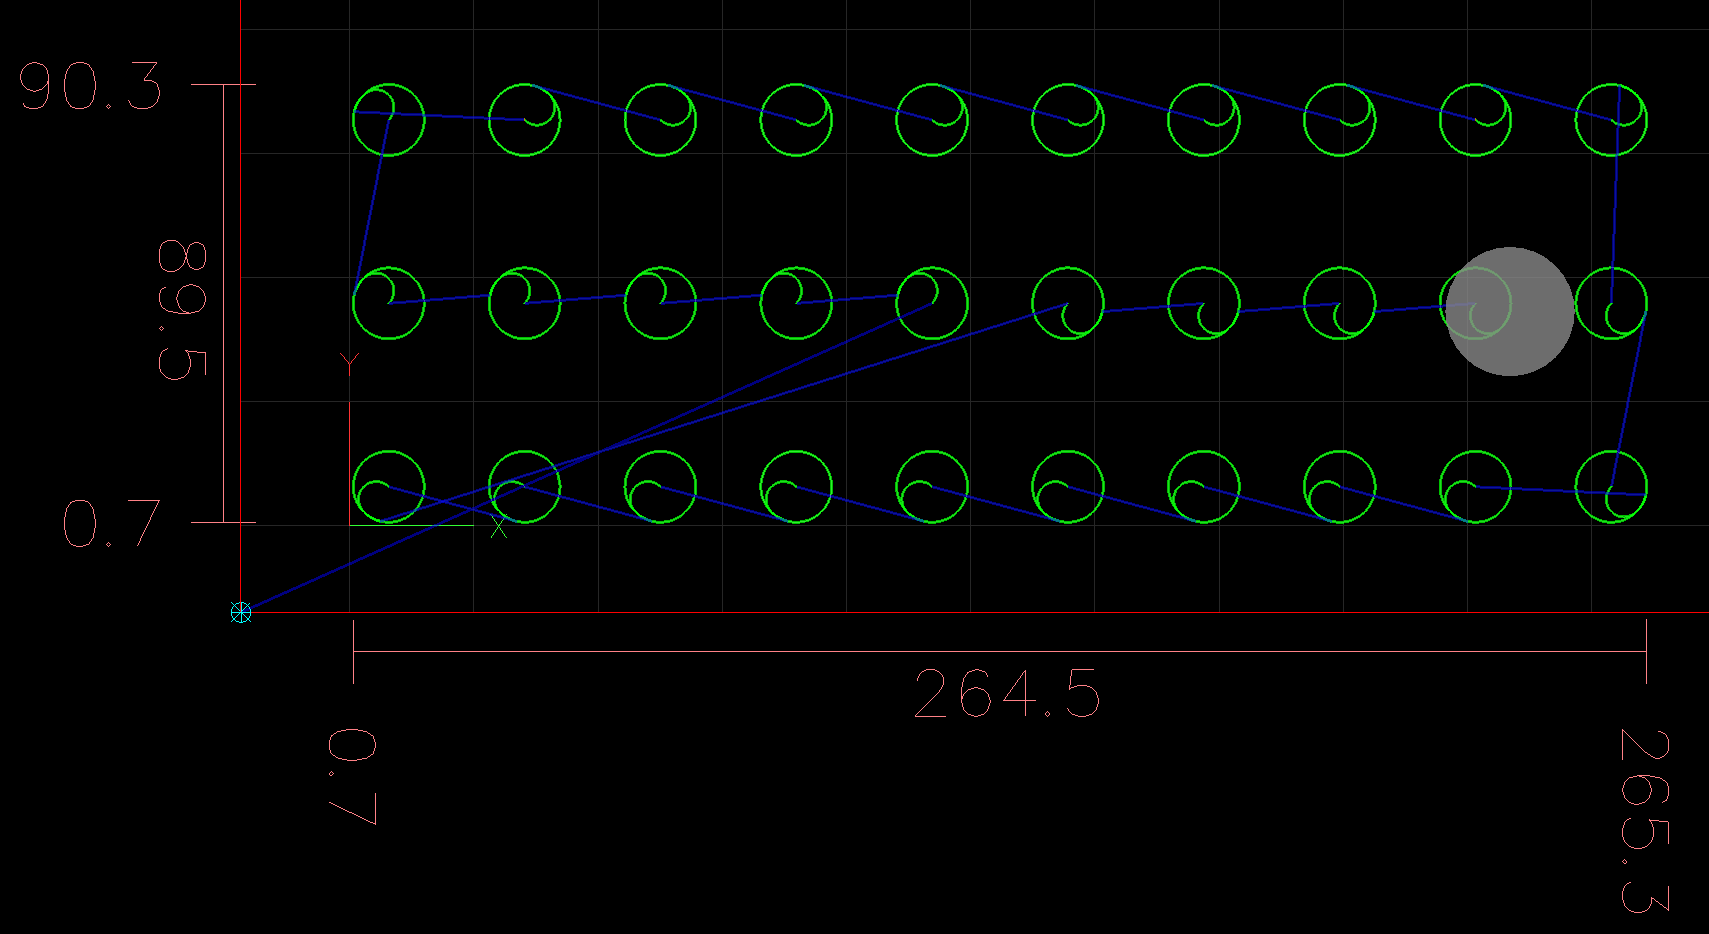
It runs fine here on my virtual machine. I did notice that it's running at 49.6% of the material feed rate, instead of 50%, I am not really sure why, but perhaps rounding error as I'm running this on an imperial simulation. Ignore the differences in colors, I change the color of the plotter via stylesheets.

The following user(s) said Thank You: paulsao

Please Log in or Create an account to join the conversation.
More
2 years 5 months ago #299973 by paulsao
Replied by paulsao on topic Inssues Hole cutting
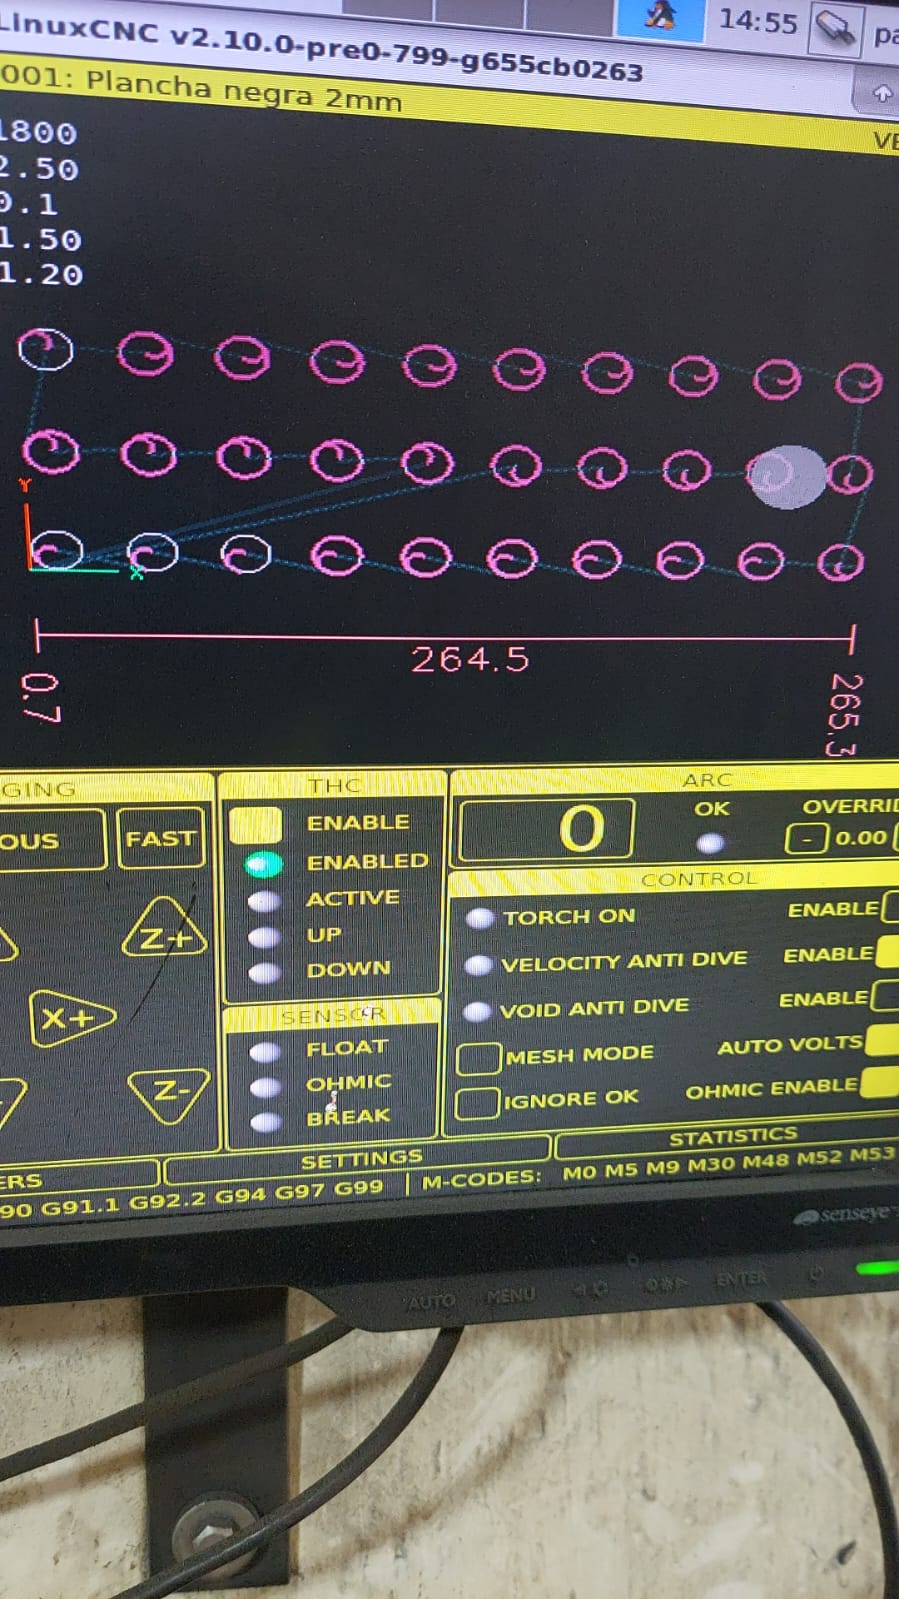
It has me confused but I'm sure there is a mistake, because the problem only occurs when there is an arc in the entrance and not a perpendicular entrance. With the same code I have 4 uncut holes. I use metric units. 

Please Log in or Create an account to join the conversation.

More
2 years 5 months ago #299985 by snowgoer540
Replied by snowgoer540 on topic Inssues Hole cutting
I only had a few minutes this evening, I should have ran it through a metric config as well. Phill might be able to pick up where I left off this evening.

It is odd that everything ran at 49.6% velocity instead of 50%. Maybe it’s somehow related ¯\_(ツ)_/¯
The following user(s) said Thank You: paulsao

Please Log in or Create an account to join the conversation.

Moderators: snowgoer540
Time to create page: 0.064 seconds
Powered by Kunena Forum