
Search Results (Searched for: )

  • zz912
24 Feb 2026 23:16

And so IMHO it does not really make sense to have a hardware button to send MDI commands which you need to type with the keyboard.


It makes sense. But the reason is not the one described by BertaA.

My dream is to build a CNC machine, controlled by LinuxCNC, that will meet all the requirements (standards and laws) for a CNC machine that the European Union requires. I think that it is possible to compete with brands like Heidenhain, Siemens, Fanuc ... in a certain category of machines.

When I studied the safety standards for CNC machines, I found a requirement there:
MDI commands or sequence commands must be executable only with a physical button. I think that the standard even described what the button should look like. I don't remember exactly because it's been a long time since I read it.

Therefore, it would not be bad to make a configuration that would ensure the execution of MDI commands only with a HAL signal.
  • PCW
24 Feb 2026 23:08
Replied by PCW on topic 7i76EU+7i85+7i84U
Yes, it may be a cable issue.

Just verified that:

7i76eu_7i76x1_7i85x1d.bin from the distribution zip file.

md5 checksum:

485114d3d22390a7e5b44d77588981c5  7i76eu_7i76x1_7i85x1d.bin

Works correctly with a 7I85 on P1 (all 5 sserial ports on the 7I85 work correctly)

Is it possible you have a 7I85S rather than 7I85?


  • rodw
24 Feb 2026 22:47
Replied by rodw on topic 7i76EU+7i85+7i84U
Yes, it was sleeping for days before it received the kiss of life!
  • tommylight
24 Feb 2026 22:42
Replied by tommylight on topic 7i76EU+7i85+7i84U

I drew up my own pin out diagram converting the wire colours to be correct and my 7i73 woke up!
Did it sleep well ?
:)
  • rodw
24 Feb 2026 22:40
Replied by rodw on topic 7i76EU+7i85+7i84U
Take care here, Network cabling comes in two different flavours T568B and T568A. Google for the difference
In my case, Mesa's serial port manual describes one of these standards but in my country the normal standard was the other!
I drew up my own pin out diagram converting the wire colours to be correct and my 7i73 woke up!
  • tommylight
24 Feb 2026 21:55
Replied by tommylight on topic Remora - Cannot clear E-STOP, without error
Changed the subject tittle to reflect use of Remora, is that OK?
  • tommylight
24 Feb 2026 21:52
Pictures of the wiring?
  • PCW
24 Feb 2026 21:24
I'll try and get to the 7I96 configuration later today or tomorrow

but note you need a  RS-485 interface, and that's only available on the 7I96 configuration.
The 7I92 configs  would need to add a RS-485 chip or a daughtercard with a RS-485 interface.


  • jtrantow
24 Feb 2026 21:06
I added the RS485 termination resistors and I'm successfully talking to the VFD.

When I get new firmware I will retry automatic gear detection with a faster update of the motor frequency.
  • RotarySMP
24 Feb 2026 20:55
Replied by RotarySMP on topic Schaublin 125-CNC retrofit.
Thanks, but I gave it an S command, both on a separate entry before, and on the same entry as the M3, but that doesn't correct it. When I command spindle on with S100 M3, the green spindle turning indications on the Gmoccapy display goes on, but the VFD is not commanded. Pushing the physical button I get both the display indication, and the spindle turning.
  • T_D
24 Feb 2026 20:42
Replied by T_D on topic G-code wizard für Gmoccapy
Ich habe mir das mal angeschaut mit pyngcgui also das an sich startet auch und ich habe das auch anwenden können mit diesem plugin welches man noch zusätzlich laut beispiel Konfiguration installieren soll nur hab ich noch nicht verstanden wie ich mir das auf den mill catalog stelle , schön wäre es wenn nativecam läuft und eventuell kann mir ja wer. Dabei helfen das zum laufen zu bekommen . Gruß tom
  • HansU
24 Feb 2026 20:34 - 24 Feb 2026 20:34
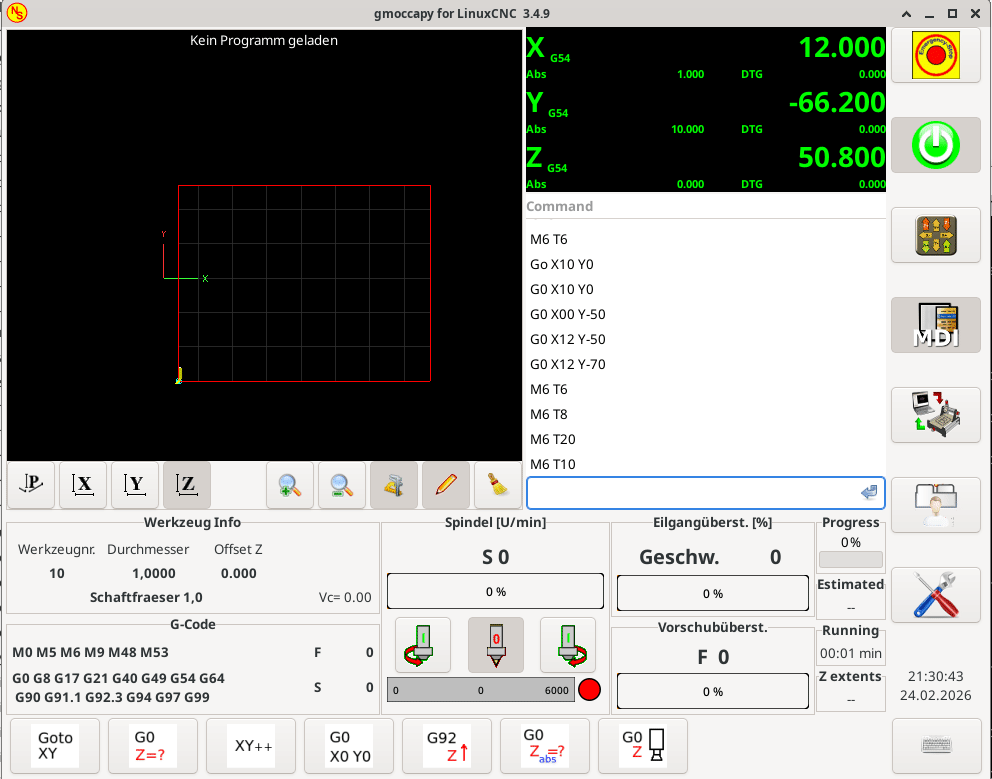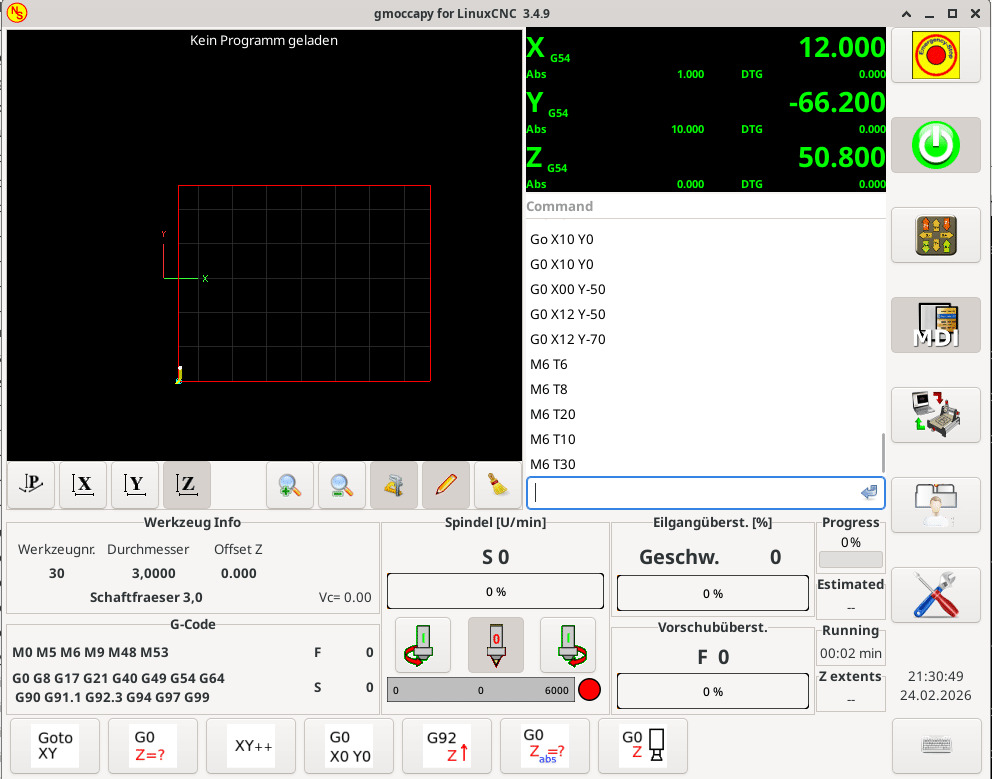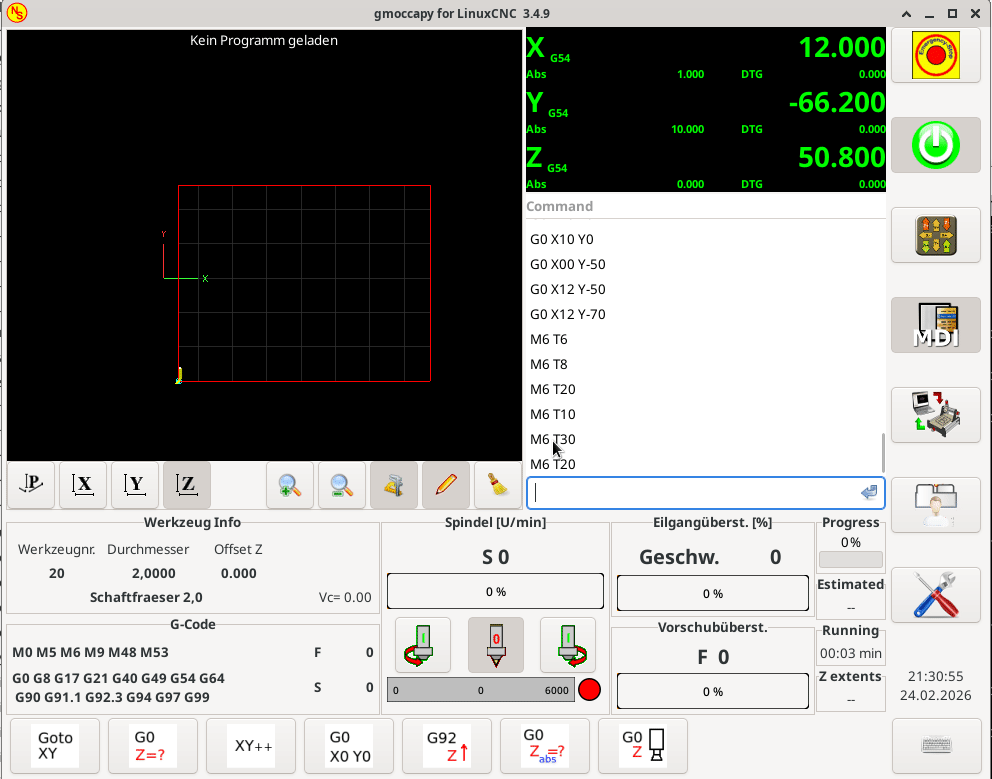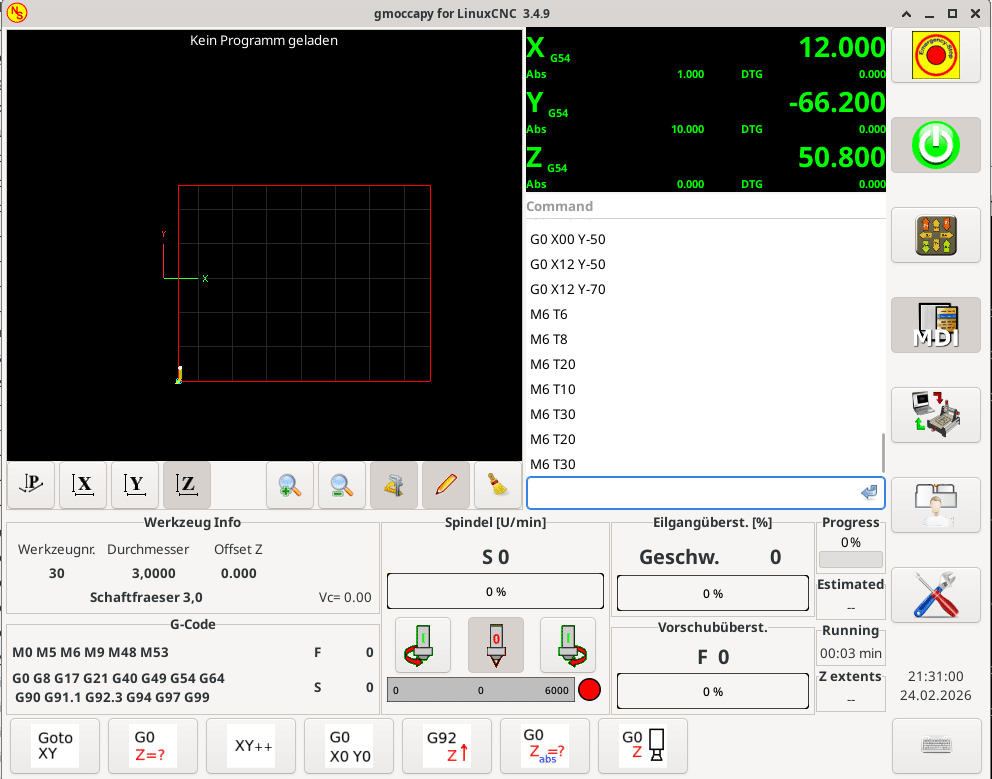
I don't know what's wrong with your enter button, but normally it should work with the enter button:
 

And so IMHO it does not really make sense to have a hardware button to send MDI commands which you need to type with the keyboard.

How is the behaviour on your machine different from that I have shown?
  • Dudelbert
24 Feb 2026 20:30
Replied by Dudelbert on topic Schaublin 125-CNC retrofit.
I may be totally wrong, but I think when using M3 for the first time in MDI after startup, you need to give it a speed (M3 S400). Afterwards, that speed is assumed.
  • HansU
24 Feb 2026 20:19
  • RotarySMP
24 Feb 2026 20:00
Replied by RotarySMP on topic Schaublin 125-CNC retrofit.
Weird one here. I have three physical buttons on my control panel connected to halui.spindle.0.forward, halui.spindle.0.reverse, and halui.spindle.0.stop. These are working normally.

But if I type an M3 or M4 command, I get no spindle rotation. It was working before, and just stopped working abbruptly. I would have expected the external buttons to trigger the same signal path as M3 M4? Any thoughts what I need to be looking for would be appreciated.
Cheers,
Mark
Displaying 6736 - 6750 out of 11907 results.
Time to create page: 0.182 seconds
Powered by Kunena Forum

