Search Results (Searched for: )

  • tommylight
02 Feb 2026 20:34
Replied by tommylight on topic Forum Fehler, ... :-(
Can you post from a phone or a tablet?
  • Muecke
02 Feb 2026 19:50
Forum Fehler, ... :-( was created by Muecke
Ich würde ja wirklich gerne auf mein eigenes Thema antworten, doch das Forum meint, es gäbe einen internen Fehler. :-( 
 
  • tar_san
02 Feb 2026 18:32
Thank you for the reply.
  • tommylight
02 Feb 2026 18:23
Replied by tommylight on topic Raspberry pi 5 freze
Can you run LinuxCNC from the terminal and copy/paste the errors reported when that happens?
Usually linuxcnc -l should start last used config.
  • krille
02 Feb 2026 18:08
Raspberry pi 5 freze was created by krille
Hi and so much thanks to the people made all the work with the linuxcnc for raspberry pi 5 ,its a great job.
I have downloaded 4.8.9 and it's a great distro working so fine from beguining and today after a week or two the program stop and freze after 5-10 min. I can still run the stepper from the keyboard and the speedometer on the spindle is i ok and run but the rest of the program stop . the only way to go on is a hard rebot and then it start fine and then the problem starts again . Are there people who can help me in the right direction 
I use the byte2bot board in Lathe config. /krister
  • opw
02 Feb 2026 15:19
Hi guys, 

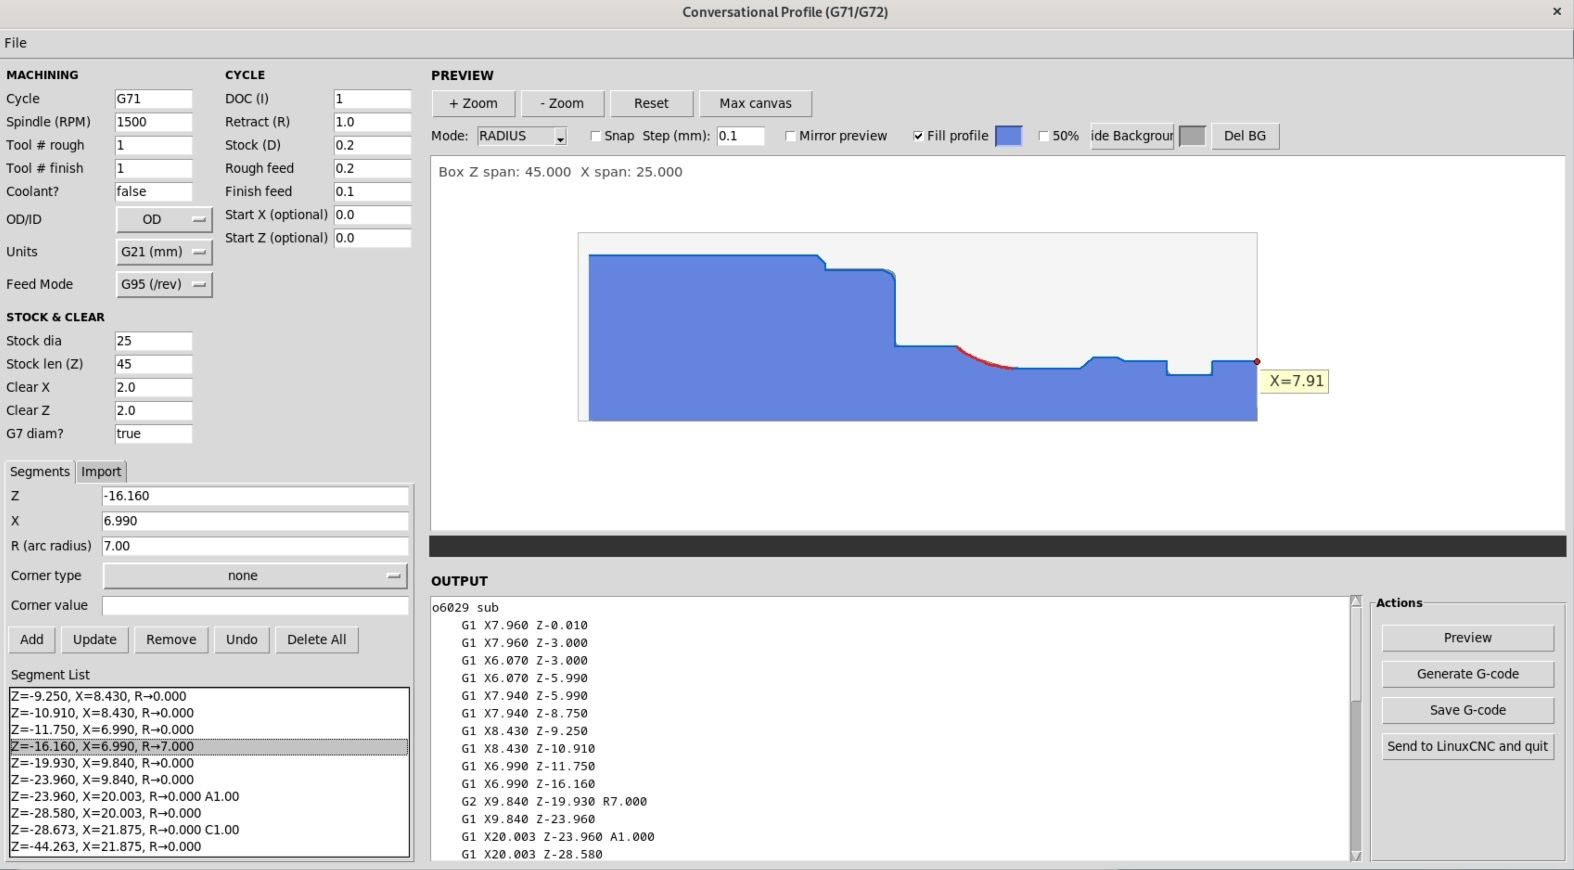
Created this simple, but effective profile editor for myself. 
It is a lightweight Tk-based conversational editor for lathe profiles, designed for LinuxCNC / PathPilot style workflows.It lets you sketch, edit, and preview turning profiles interactively, then generates a G71 or G72 roughing cycle with a G70 finish pass. All core functionality uses only the Python standard library (Tk), so it can be dropped directly into a AXIS environment.Optional DXF / 3MF import is supported via external libraries.

For example you can: 
 
  1. import an STL as a background reference
  2. Auto create segment points or (recommended) tracing the rotational outline with profile points 
  3. Adding chamfers and radii for finishing details
  4. Adjusting geometry for optimal cutting
  5. Setting machining parameters
  6. Generating G-code
  7. Sending to LinuxCNC/AXIS
 You can find it here:  Repository


  • djdelorie
02 Feb 2026 15:05
Replied by djdelorie on topic Where should linux cnc tool offsets be stored?
I will add, though, that when I started using my ATC I mixed the old and new ways, and it was a disaster :-)
 
  • djdelorie
02 Feb 2026 15:04
Replied by djdelorie on topic Where should linux cnc tool offsets be stored?
I suspect ALL cnc's apply offsets the same way. And as long as the offsets add up to the right tool location, it doesn't matter if you change G54 or T1 when you manually change tools. If you're using a trim router with a collet and change tools all the time but never issue a T command, you just have to know how to change the G54 so that it does the right thing.

So external measurement, toolsetters, manual tool touch off, part touch off, they're all just ways of making those offsets add up to the right thing.
  • ruediger123
02 Feb 2026 14:35
Replied by ruediger123 on topic LinuxCNC S-Curve Accelerations
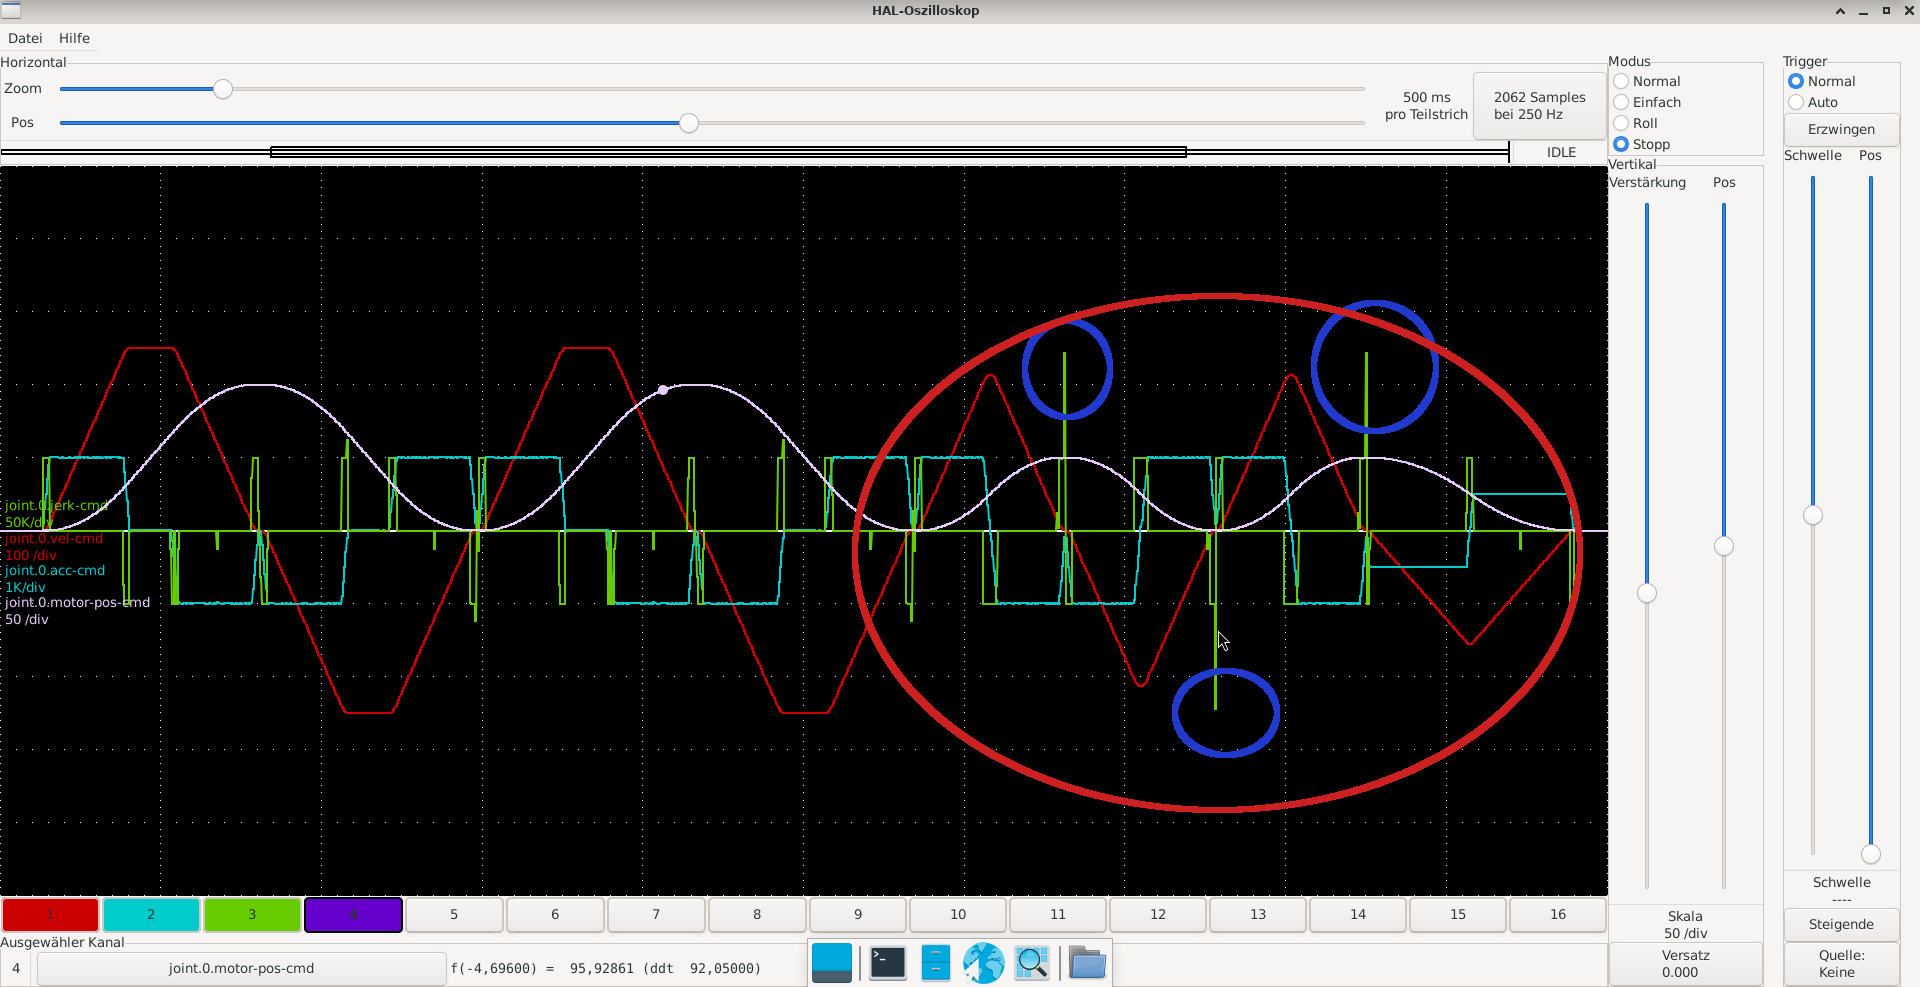
@grandixximo 

In the blue circles, the jerk is outside the limits.
In the red circle, the speed of the axis should, in my opinion, always be the same.

 
  • Hakan
02 Feb 2026 14:20
Is there much to say about it? Both Mesa and EtherCAT work, and work well.

We do miss an EtherCAT documentation page linuxcnc.org/docs/devel/html/ .
Much info is scattered here in the forum and at a few github pages. This could be better.

It's not uncommon to have some configuration issues, specifically with the ethercat-conf.xml file.
This adds to the complexity. Mesa has a pncconf tool, there is nothing similar for EtherCAT.
The forum people can come to help if you get stuck on that.
Once configured, my impression is that an EtherCAT system just runs.

Both parallel ports and Mesa have their weak points but people have worked around them for many years and don't see them anymore.
EtherCAT has one unique weak point   forum.linuxcnc.org/ethercat/58227-how-go...trol?start=10#341798
which isn't to difficult to work around.

Your Leadshine EL8 drives have several digital IOs that you can use for general purposes.
This may make the Beckhoff components redundant. Worth checking.

 
  • tommylight
02 Feb 2026 13:50
Replied by tommylight on topic keyboard shortcut

Would it be possible to configure the parallel port in "in" or "x" mode to have more ports?
The only way to know for sure is to test it, most will work, but some will not.
And you can not get more ports, the limit is 17, but you can choose between more inputs or more outputs:
OUT = 12 out 5 in
IN = 4 out 13 in
X = 8 out 9 in
Be aware that pins 1,14,16,17 require more current to trigger when set as inputs.
  • Todd Zuercher
02 Feb 2026 12:49
Replied by Todd Zuercher on topic Maxnc15CL Motor timing help
Don't rule out the possibility that there are electrical issues with the stepper motors/drives. A bad connection between the motor and drive can often cause problems or even kill a drive. Also make sure that the screws turn freely without any binding. Start with slow accelerations and max velocities and longer step timings increasing until you find the limits of the machine, then reduce to give you a safety margin.
  • rodw
02 Feb 2026 10:03 - 02 Feb 2026 10:05
On the flip side, all the electronics are in the drives so there is no control board to fail so you could argue Ethercat has fewer failure points do more reliable. I do like Mesa but Ethercat is easier to wire. Hers is a Ethercat plasma control box somebody shared with me today.


One small Chinese IO module and a Proma plasma THC
  • rodw
02 Feb 2026 09:54
Seeme like Linuxcnc is set up assuming premeasured tools in a magazine. HOweer you can do this with repeatable tooling or adopt TTD in your MT3 or R8 spindle. When I set up QtDragon, I bought a tool setter and the tiny marble plate with a hole in it from Tormach. I measured all my tools in the toolsetter Including the 3D probe as tool 99.So after touching off with tool 99 with the probing routines, QTdragon asked me to change the tool manually and continue. This worked very well as you could run out a singlee gcode file instead of running  out seperate files for each tool the eold fashioned way!
  • Ismacr63
02 Feb 2026 09:48
Replied by Ismacr63 on topic keyboard shortcut
Yes, I completely agree, it could be more dangerous than practical. Do you think any alternative would be to install a physical button on one of the ports to activate the spindle?

I have a parallel port with all the ports occupied. Would it be possible to configure the parallel port in "in" or "x" mode to have more ports?
Displaying 7516 - 7530 out of 11386 results.
Time to create page: 0.557 seconds
Powered by Kunena Forum