
- Posts: 36
- Thank you received: 3
Servo Wiring and Tuning detailed How To example Mesa 7i77.
- petmakris
- Offline
- Junior Member
-

Less
More
3 years 9 months ago - 3 years 9 months ago #260891
by petmakris
Replied by petmakris on topic Servo Wiring and Tuning detailed How To example Mesa 7i77.
Amazing how-to, thanks, great starting point for me.
I find this video with a basic overview of the tuning method to provide quite supplementary information
Ziegler-Nichols Method
I find this video with a basic overview of the tuning method to provide quite supplementary information
Ziegler-Nichols Method
Last edit: 3 years 9 months ago by petmakris.
Please Log in or Create an account to join the conversation.
- vre
- Offline
- Platinum Member
-

Less
More
- Posts: 612
- Thank you received: 17
1 year 9 months ago #318984
by vre
Replied by vre on topic Servo Wiring and Tuning detailed How To example Mesa 7i77.
In halscope what are the units ?
For example if set f-error to 200m/div what and i see 1 div how this translates to mm ?
Also in cmd-velocity if i set to 1/div how this translates to mm/sec ?
I have seen a post by @andypugh that showed an alternative method of pid tuning
know anyone the link of this post ?
For example if set f-error to 200m/div what and i see 1 div how this translates to mm ?
Also in cmd-velocity if i set to 1/div how this translates to mm/sec ?
I have seen a post by @andypugh that showed an alternative method of pid tuning
know anyone the link of this post ?
Please Log in or Create an account to join the conversation.
- PCW
- Offline
- Moderator
-

Less
More
- Posts: 18115
- Thank you received: 5334
1 year 9 months ago #318985
by PCW
Replied by PCW on topic Servo Wiring and Tuning detailed How To example Mesa 7i77.
If the machine uses mm units, 200m = 0.2 mm/division
and a velocity of 1 means 1mm/s
and a velocity of 1 means 1mm/s
The following user(s) said Thank You: tommylight, vre
Please Log in or Create an account to join the conversation.
- tommy
- Offline
- Premium Member
-

Less
More
- Posts: 106
- Thank you received: 3
1 year 7 months ago #324907
by tommy
Replied by tommy on topic Servo Wiring and Tuning detailed How To example Mesa 7i77.
I would need a bit of hint on my tuning of AC servos + 7i95t, as I cannot decrease those spikes on acceleration and deceleration, doesn't matter if I go higher or lower with FF2. On linear move there is f-error 0.001mm or less. Should I start adjusting parameters on diver?
Also if I "go crazy" with short presses on arrow keys for jog, especially with changing direction, f-error is all the way up to 1mm or more.
Captures below are taken during running some test g-code:
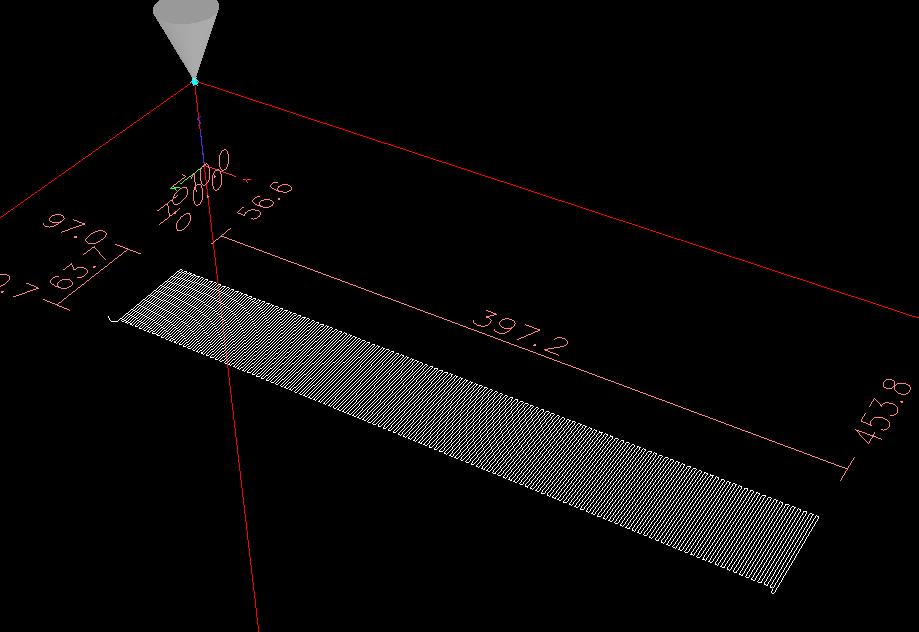
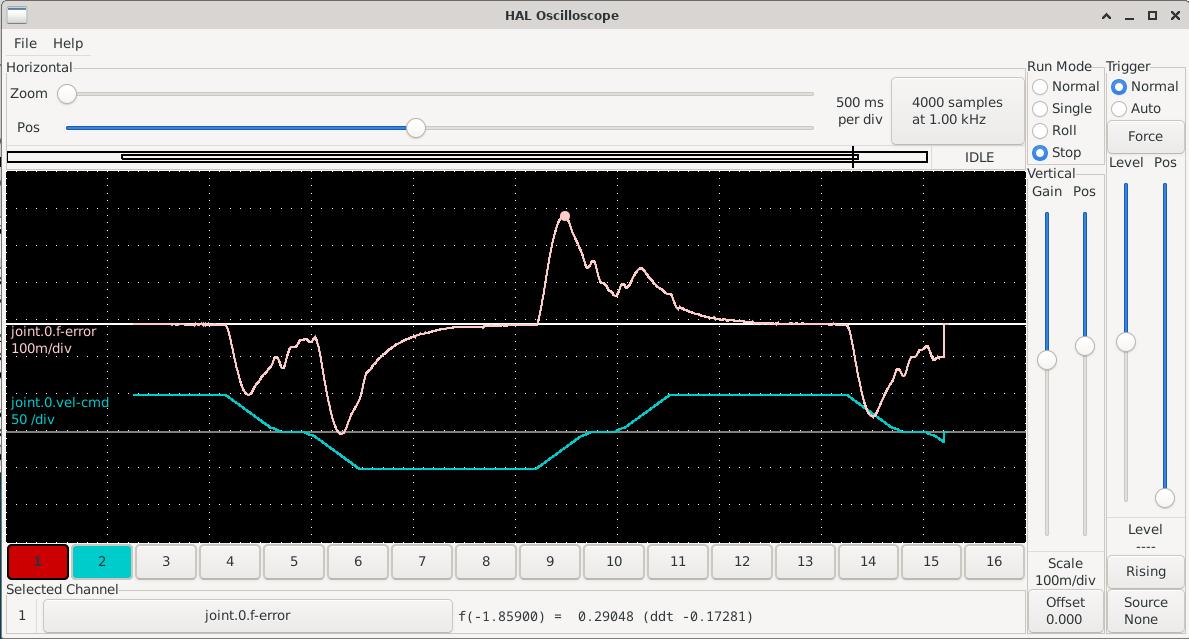
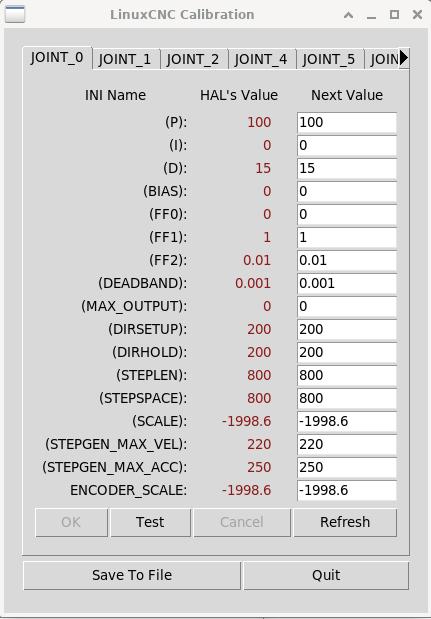
Also if I "go crazy" with short presses on arrow keys for jog, especially with changing direction, f-error is all the way up to 1mm or more.
Captures below are taken during running some test g-code:
Please Log in or Create an account to join the conversation.
- PCW
- Offline
- Moderator
-
Less
More
- Posts: 18115
- Thank you received: 5334
1 year 7 months ago - 1 year 7 months ago #324908
by PCW
Replied by PCW on topic Servo Wiring and Tuning detailed How To example Mesa 7i77.
Are these step/dir servos with encoder feedback to LinuxCNC?
If so it seems there is significant delay from command to motion.
This may well be a drive tuning/setup issue. Maybe drive acceleration
set lower than LinuxCNCs setting or some other filtering or constraints
in the drive.
If so it seems there is significant delay from command to motion.
This may well be a drive tuning/setup issue. Maybe drive acceleration
set lower than LinuxCNCs setting or some other filtering or constraints
in the drive.
Last edit: 1 year 7 months ago by PCW.
Please Log in or Create an account to join the conversation.
- tommylight
- Away
- Moderator
-
Less
More
- Posts: 22011
- Thank you received: 7491
1 year 7 months ago #324910
by tommylight
Replied by tommylight on topic Servo Wiring and Tuning detailed How To example Mesa 7i77.
If those are step/dir drives, you should be looking here:
forum.linuxcnc.org/10-advanced-configura...glass-scale-feedback
Also
dirsetup and dirhold to 20000
and stepspace and steplen to 5000
Untill you get things working properly, then you can lower the steplen and stepspace while testing to make sure there are no missed steps.
As you have them, chances are some steps are being missed by the drive so LinuxCNC keep upping the number of steps till it catches up.
-
Yes, i am aware the drive manual might say 200ns, but that is almost always not correct, except on very good quality drives.
Please Log in or Create an account to join the conversation.
Time to create page: 0.138 seconds