
- Posts: 1635
- Thank you received: 595
Retrofitting a 1986 Maho MH400E
- RotarySMP
- Offline
- Platinum Member
-

Less
More
1 year 10 months ago #315789
by RotarySMP
Replied by RotarySMP on topic Retrofitting a 1986 Maho MH400E
Hi Guys,
The Maho has been out of service/ limited service for a couple of months while I gave procrastination and denial a chance to solve it's problems...
Cheers,
Mark
The Maho has been out of service/ limited service for a couple of months while I gave procrastination and denial a chance to solve it's problems...
Cheers,
Mark
The following user(s) said Thank You: tommylight
Please Log in or Create an account to join the conversation.
- spumco
- Offline
- Platinum Member
-
Less
More
- Posts: 2180
- Thank you received: 905
1 year 10 months ago #315798
by spumco
Replied by spumco on topic Retrofitting a 1986 Maho MH400E
Drawbar springs?
I can't tell from the diagram you had in the vid, but it looks (and sounds) like the hydraulic DB is a spring return system - I thought I only heard the pump loading up during release.
And DB springs are consumables...
Easy enough to pull the DB and have a look at the springs (if I'm right) before fully digging in to bearings.
Please Log in or Create an account to join the conversation.
- RotarySMP
- Offline
- Platinum Member
-
Less
More
- Posts: 1635
- Thank you received: 595
1 year 10 months ago #315828
by RotarySMP
Replied by RotarySMP on topic Retrofitting a 1986 Maho MH400E
Yeah, that is the first thing I will check. I just started trying to remove the draw bar unit. I dont have a good cut away or manual for this, so will just disassemble what I can find.
Please Log in or Create an account to join the conversation.
- D Jensen
- Offline
- Senior Member
-

Less
More
- Posts: 69
- Thank you received: 16
1 year 10 months ago #315837
by D Jensen
Replied by D Jensen on topic Retrofitting a 1986 Maho MH400E
Here are the pages from my manual on how to disassemble and re-grease the spindle. Mine is NT40 so a bit bigger and with a different pull stud. But I would think much the same. I've added the page on how to adjust the claws. It's very quick and simple. The whole assembly item 2 is fitted when it's all assembled into the spindle, in my case back in the machine. It simply screws in. When the depth dimension is right ( I used the tail end on my dial calipers) you simply tighten the grub item 1. That presses the ball into the coned recess in the stud and expands the thread onto item 2. The hatched portion where item 2 points to are actually longitudinal cuts in the thread.
Your 30 size tool holder will have a different adjustment length I would think. .In the diagram you can see that as the claws are retracted they are jammed closed by the bore of the spindle. That means that it is more likely any rattle is due to damaged or worn claws I think. The claws are the finer cross hatch.
Cheers,
David


The following user(s) said Thank You: RotarySMP
Please Log in or Create an account to join the conversation.
- D Jensen
- Offline
- Senior Member
-
Less
More
- Posts: 69
- Thank you received: 16
1 year 10 months ago #315841
by D Jensen
Replied by D Jensen on topic Retrofitting a 1986 Maho MH400E
I noted your comments on Z axis machining and thought I might stick my neck out here.
Your machine looks like it came with the old Philips controller from one of the early photos. They set the axes up differently to what I believe is the current convention. That is with the Y and Z axes swapped. So you might find your servo closing relays in the wrong physical order on the DIN C rail. The convention seems to be X side to side, Y forward and aft, and Z up and down. Certainly Heidenhain uses that on controllers from my TNC 155 up to 400 series. Early Bridgeports used the TNC 155 so they are that convention also.
Rotary axis A, B and C rotate around X, Y, and Z axes respectively. So I code my rotary axis as C, but it is possible to not use that convention by changing a parameter.
So in the your programming examples you wouldn't change the axes orientation, you simply tell the machine the cutter in in the Y axis by using G18 in the G code.
There is a program showing this in one of the links to my cloud previously. It's the one where it pretends to cut a spiral thread using a cutter in the Y axis and the C rotary table.Rather like a vertical lathe.
The next problem is that on our machines the cutter is usually attached to the Y axis, so it moves that way. The other 2 involve the table moving up and down and sideways.. On the typical Bridgeport of that era, the quill moves the cutter in the Z direction and the table moves back and forward and sideways. And yet you set up the program identically for both!
So the convention is that the DATUM is the work piece. So when you do the familiar right hand rule with your real hand, You place the back of your hand on the work piece whilst standing in front of the machine. And keep it stuck in the same place on the work piece as it moves.
Now look at where the cutter is moving relative to you hand:
If it is moving in the direction your thumb is pointing then it's moving positive X
If it is moving in the direction your index finger is pointing then it's moving positive Y
If it is moving in the direction your middle finger is pointing then it's moving positive Z
That works for all types of 3 axis machines.I have no idea how they label machines with 5 axes and seemingly infinite rotation axes.
In our case what seems counter intuitive is that for X+ the table will move left and for Z+ the table will move down.
Cheers,
David
The following user(s) said Thank You: RotarySMP
Please Log in or Create an account to join the conversation.
- RotarySMP
- Offline
- Platinum Member
-
Less
More
- Posts: 1635
- Thank you received: 595
1 year 10 months ago #315871
by RotarySMP
Replied by RotarySMP on topic Retrofitting a 1986 Maho MH400E
Hi David,
Thanks a lot for that. I have a bunch of questions for you...
What year is your machine?
Have you lubricated your bearings already?
Did you confirm yours has the tapered roller bearings?
What Max RPM does it have?
What alternative grease did you use, as it seems Kluber F23A is discontinued?
Is the instruction you uploaded for the vertical spindle or the horizontal?
Do you have any advice on removing the draw bar unit?
My understanding is that the vertical has a more complicated set up with integral bearings. My machine is also 40 taper. It's pulls studs are the ISO 7388 Type B option and my Manual covers the adjustment in 7.35 like yours.
No wonder that MAHO gave out such different manuals, as my user manual (in German) has the cover guard removal in that section 7.10, and nothing on spindle lubrication, but I guess this is tied in with them keeping reinventing the wheel, as there are also drawings of 400E with these horizontal...
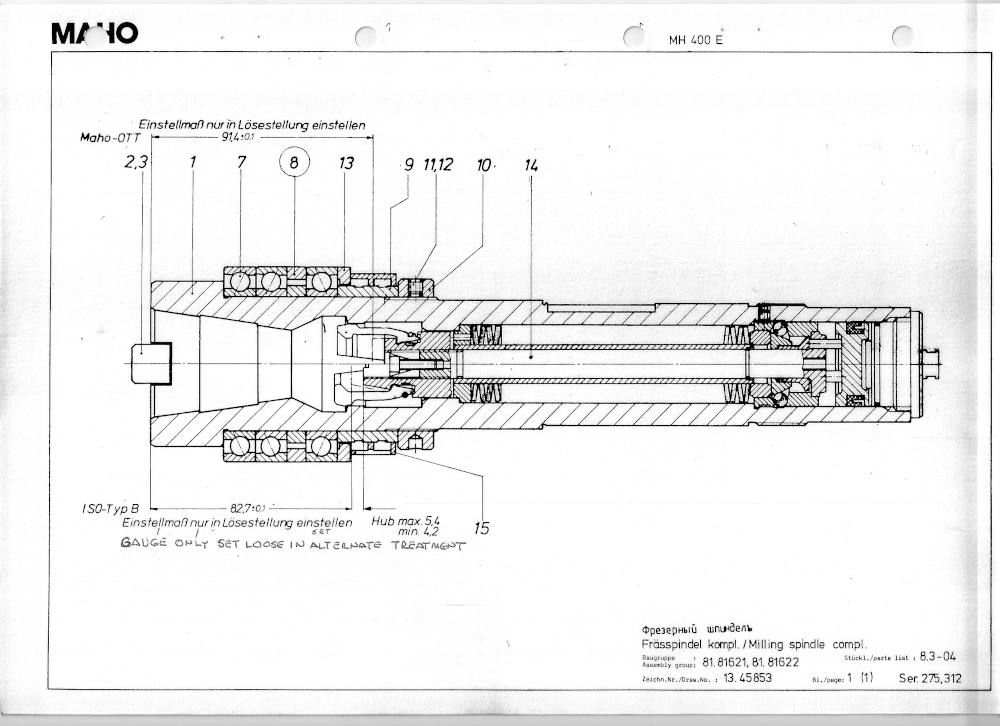
...and vertical spindle bearing configurations.
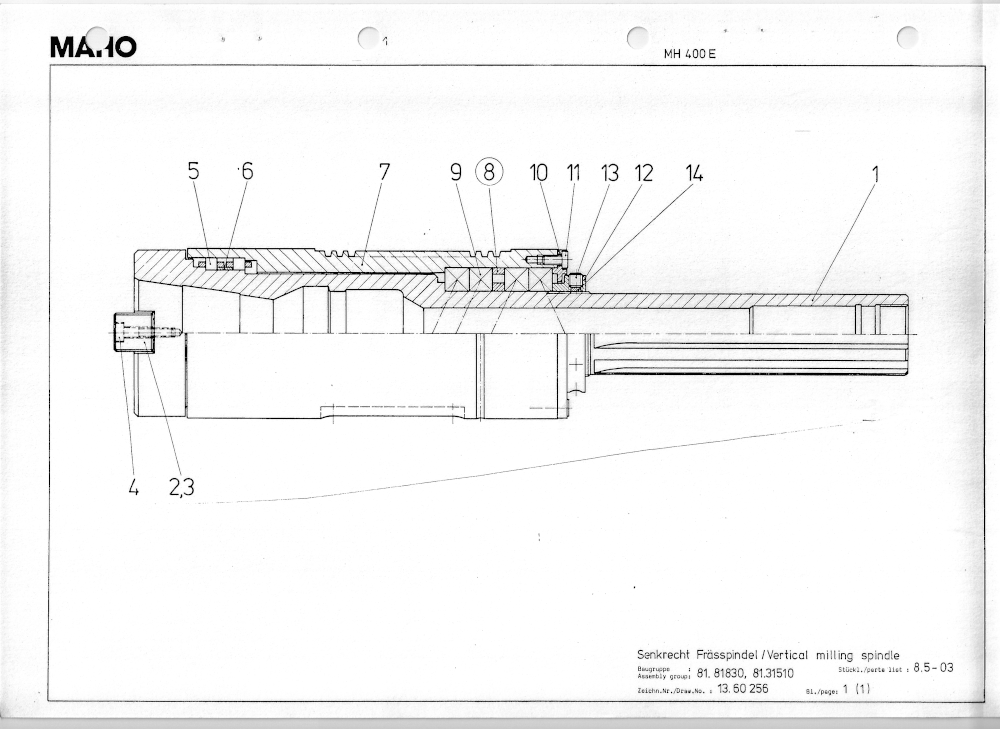
I am starting to feel like Forest Gump, where a Maho spindle is like a box of chocolates
If you have the whole manual scanned, I would appreciate a copy of it please. I can send you my German language version if you are interested.
With regards to the axis swap, when I did my LinuxCNC retrofit, I configured mine as a vertical mill (Z up down) whereas Maho configured them standard as a horizontal, with an option to Axis swap. Servo closing relays? My schematic doesn't have any. 7K2 provides the muscle power to all three channels of the Indramat, and the axis enables are hard wired onto inputs from the vertical axis motor brake, and a couple of other contacts, so LinuxCNC has no control over them.
I have my PP of my CAM set up for a vertical mill as well. I have been editing my G-code files, to do the axis swap (reversing Y/Z, inverting one, replacing I, J with I, K, and Inverting it, and could easily write a macro to automate that.
I was in the middle of setting up a second LinuxCNC configuraton with the mill as horizontal (Y vertical movement), but was getting confused with the Ini edits, before I got sidetracked with my DoAll gearbox, and now with the spindle noise. I still need to complete the second config, as it makes most sense to have both, and then I can use the same PP, and code generated can be used on either configurations.
Cheers,
Mark
Thanks a lot for that. I have a bunch of questions for you...
What year is your machine?
Have you lubricated your bearings already?
Did you confirm yours has the tapered roller bearings?
What Max RPM does it have?
What alternative grease did you use, as it seems Kluber F23A is discontinued?
Is the instruction you uploaded for the vertical spindle or the horizontal?
Do you have any advice on removing the draw bar unit?
My understanding is that the vertical has a more complicated set up with integral bearings. My machine is also 40 taper. It's pulls studs are the ISO 7388 Type B option and my Manual covers the adjustment in 7.35 like yours.
No wonder that MAHO gave out such different manuals, as my user manual (in German) has the cover guard removal in that section 7.10, and nothing on spindle lubrication, but I guess this is tied in with them keeping reinventing the wheel, as there are also drawings of 400E with these horizontal...
...and vertical spindle bearing configurations.
I am starting to feel like Forest Gump, where a Maho spindle is like a box of chocolates
If you have the whole manual scanned, I would appreciate a copy of it please. I can send you my German language version if you are interested.
With regards to the axis swap, when I did my LinuxCNC retrofit, I configured mine as a vertical mill (Z up down) whereas Maho configured them standard as a horizontal, with an option to Axis swap. Servo closing relays? My schematic doesn't have any. 7K2 provides the muscle power to all three channels of the Indramat, and the axis enables are hard wired onto inputs from the vertical axis motor brake, and a couple of other contacts, so LinuxCNC has no control over them.
I have my PP of my CAM set up for a vertical mill as well. I have been editing my G-code files, to do the axis swap (reversing Y/Z, inverting one, replacing I, J with I, K, and Inverting it, and could easily write a macro to automate that.
I was in the middle of setting up a second LinuxCNC configuraton with the mill as horizontal (Y vertical movement), but was getting confused with the Ini edits, before I got sidetracked with my DoAll gearbox, and now with the spindle noise. I still need to complete the second config, as it makes most sense to have both, and then I can use the same PP, and code generated can be used on either configurations.
Cheers,
Mark
Please Log in or Create an account to join the conversation.
Moderators: piasdom
Time to create page: 3.038 seconds