
- Posts: 265
- Thank you received: 40
Retrofitting a 1986 Maho MH400E
- drimaropoylos
- Offline
- Elite Member
-

Less
More
9 years 1 month ago #99426
by drimaropoylos
Replied by drimaropoylos on topic Retrofitting a 1986 Maho MH400E
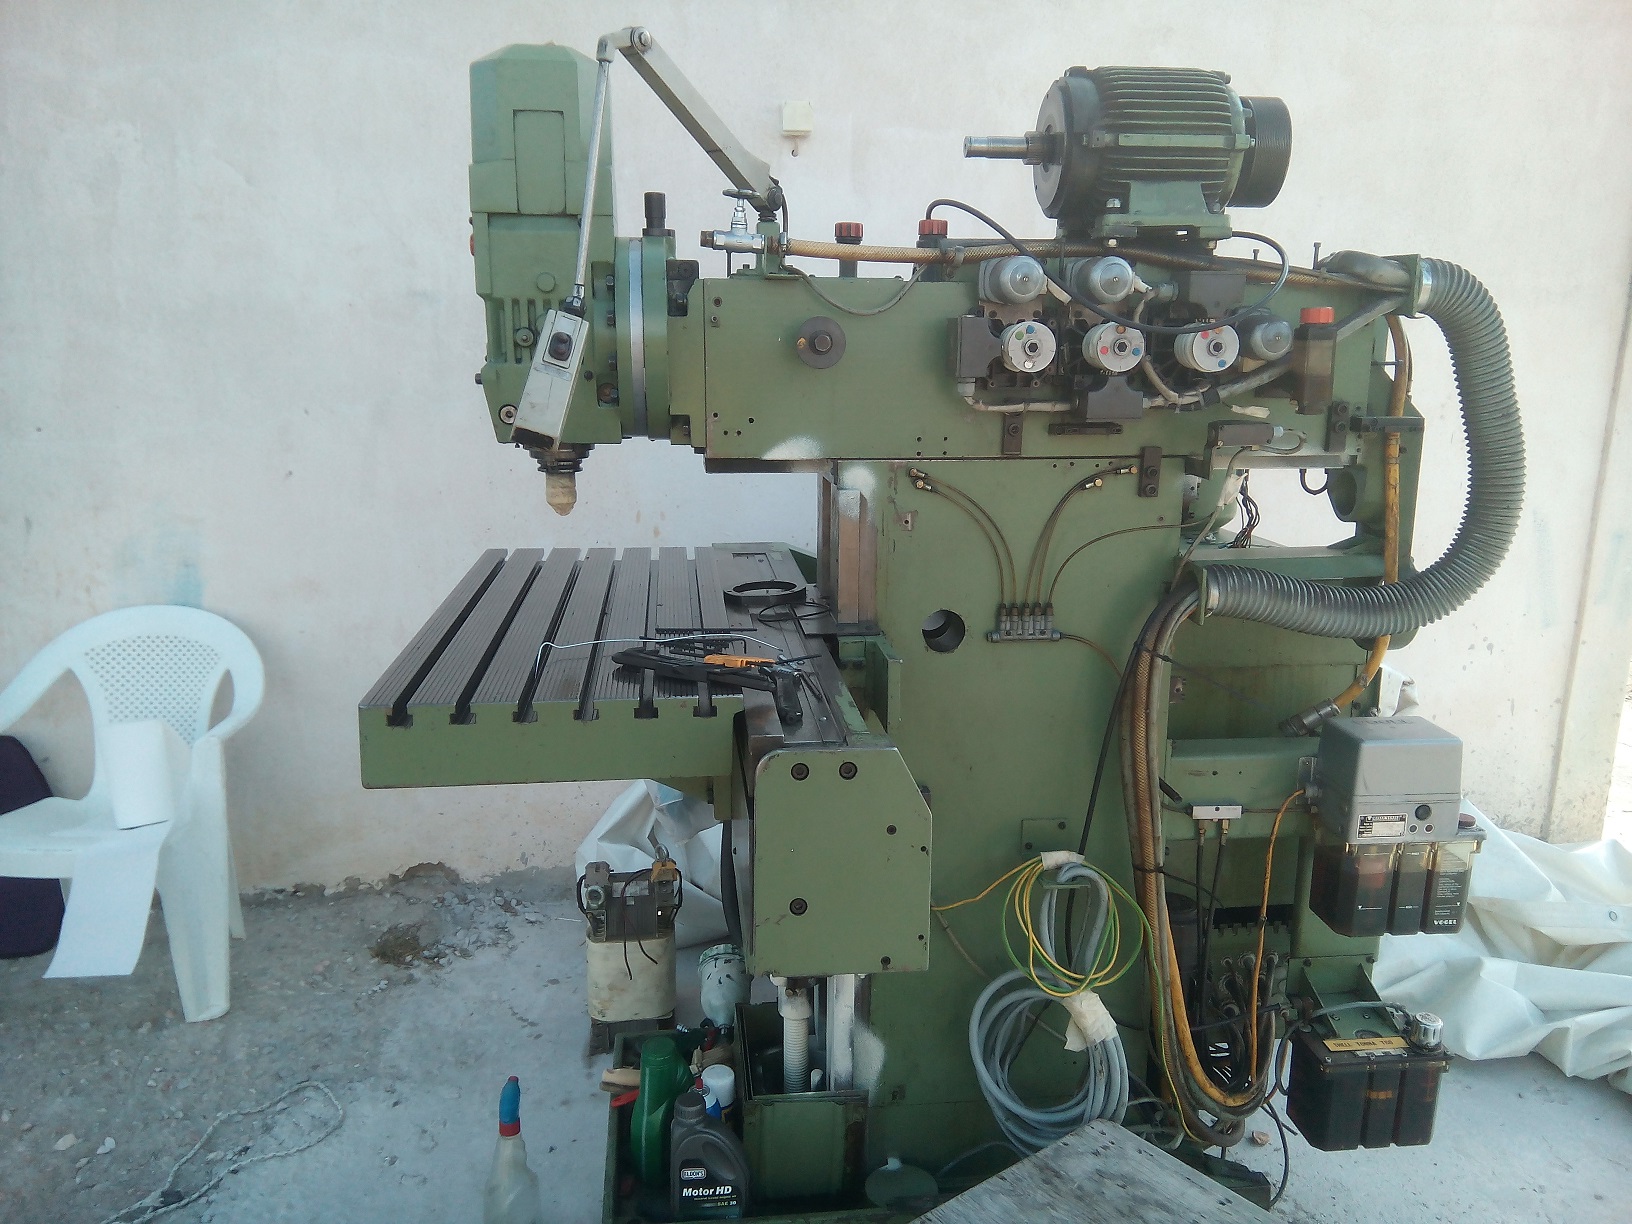
This is the machine striped. For the ballscrew, for start I have ordered balls 3.5mm g10 precision from eBay
John
John
- RotarySMP
- Offline
- Platinum Member
-

Less
More
- Posts: 1635
- Thank you received: 595
9 years 1 month ago - 9 years 1 month ago #99449
by RotarySMP
Replied by RotarySMP on topic Retrofitting a 1986 Maho MH400E
Hi John,
Thanks for sharing your files. Are you also planning to use Gmoccapy?
Concerning the last MAHO wiring diagram which needs modification (Sheet 06 in my set) do you have a recommendation for the axis enable set up? As far as I can tell, the three axis are enabled, and the Z motor brake released as soon as the machine is released from E-Stop (7K2 relay) or when the Z Brake release is selected on the 28A1 relay board.
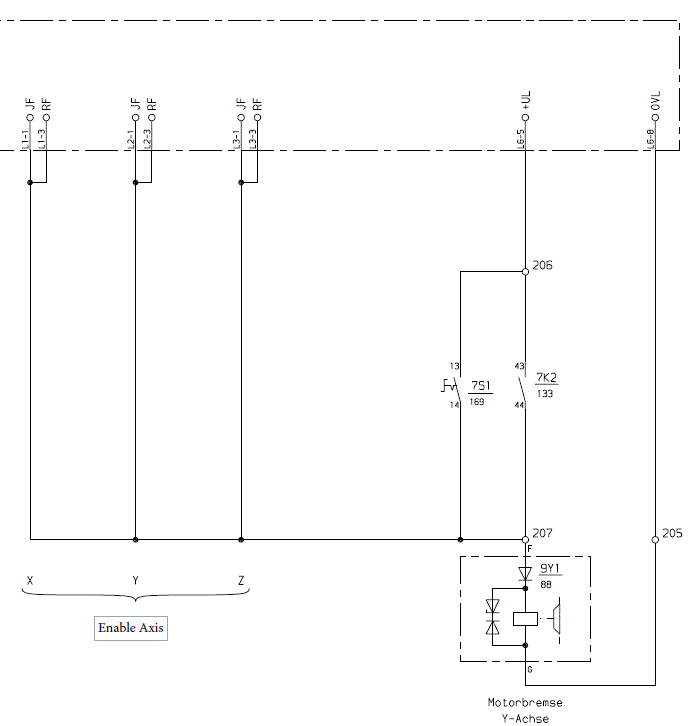
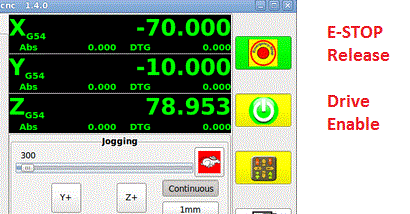
LinuxCNC would normally separate these functions, first releasing the machine from E-Stop, and then enabling the drives.
Option 1
If we keep the MAHO's set up, then we need to connect the LinuxCNC "E-Stop release" button though the HAL to the MESA TB3-17 "CNC Ready" output, closing 19K1, which releases the E-Stop chain, and thus enabling all axis.
That leaves nothing for the LinuxCNC "Machine On/Enable drives" button to do.
Option 2
We add a relay between screw connection 207, and the Indramat enable pins giving LinuxCNC separate drive enable control. We will also need to move the Z brake wiring to be controlled by that same relay, otherwise we'd drop the Z axis as soon as we exit E stop, without the drive enabled.
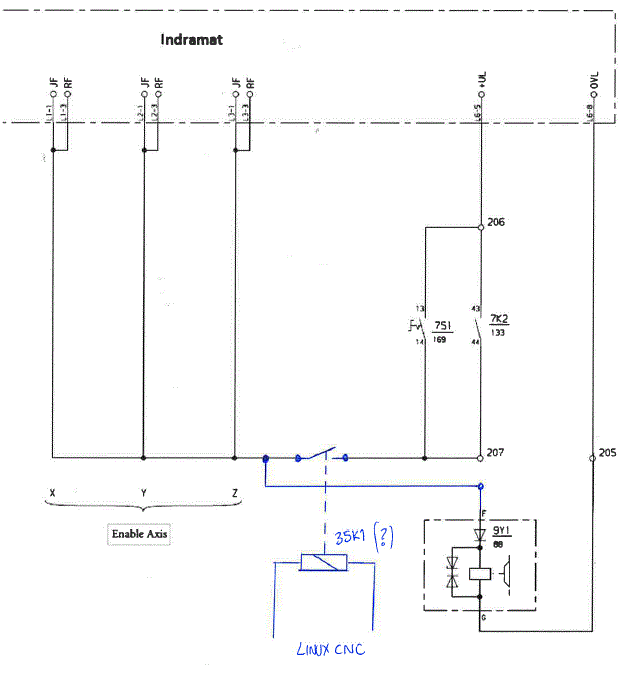
Ideally, I'd like to use the existing relay 35K1 for this, as it was "Address M" before, and now unused. There is an input "feedback address M and T" on pin IPC1-1. I need to energise that and see if it actually controls the 35K1 relay. If the control signal to that relay is available, the second issue will be whether the relay is rated for the current of the brake, as it will be energised for hours. What is your Z brake rated at? And the final show stopper would be if the second pole of the relays is wired to ground on the PCB of the relay board. If that is the case, then I guess we will be putting an addition relay on a rail.
[edit] Option 3
Split the drive enables and wire X to the MESA 7i77 TB5-4 and Y to TB5-8. Run the Z enable and it's brake from TB5- 12 to control both the Axis enable and release the brake. This would take three relays to use the existing power at screw connection 207, thus keeping the hardware E-Stop in the enable loop. All three MESA Enable pins could be connected in the HAL to the single drive enable pin. Not sure if there would be an advantage in doing this.
Really nice machine you got there. Also looks like it had an easy life.
Yesterday I got Linuxcnc 2.7.10 loaded onto the ITX PC. I set it up with a CF card instead of a hard drive, but am already regretting that. Followed the WIKI to set it with no swap drive turn off and all the cacheing to a ram drive. After installation, the security updates took forever - probably because of RAM cache and no swap. I only have 2Gb of ram. I wanted a minimum footprint controller for my lathe when I bought the CF card adaptor, but space is pretty irrelevant no I am using it on the MAHO. Since I will probably have to do a final fresh install once I the development phase is over, I'll live with it for now.
Mark
Thanks for sharing your files. Are you also planning to use Gmoccapy?
Concerning the last MAHO wiring diagram which needs modification (Sheet 06 in my set) do you have a recommendation for the axis enable set up? As far as I can tell, the three axis are enabled, and the Z motor brake released as soon as the machine is released from E-Stop (7K2 relay) or when the Z Brake release is selected on the 28A1 relay board.
LinuxCNC would normally separate these functions, first releasing the machine from E-Stop, and then enabling the drives.
Option 1
If we keep the MAHO's set up, then we need to connect the LinuxCNC "E-Stop release" button though the HAL to the MESA TB3-17 "CNC Ready" output, closing 19K1, which releases the E-Stop chain, and thus enabling all axis.
That leaves nothing for the LinuxCNC "Machine On/Enable drives" button to do.
Option 2
We add a relay between screw connection 207, and the Indramat enable pins giving LinuxCNC separate drive enable control. We will also need to move the Z brake wiring to be controlled by that same relay, otherwise we'd drop the Z axis as soon as we exit E stop, without the drive enabled.
Ideally, I'd like to use the existing relay 35K1 for this, as it was "Address M" before, and now unused. There is an input "feedback address M and T" on pin IPC1-1. I need to energise that and see if it actually controls the 35K1 relay. If the control signal to that relay is available, the second issue will be whether the relay is rated for the current of the brake, as it will be energised for hours. What is your Z brake rated at? And the final show stopper would be if the second pole of the relays is wired to ground on the PCB of the relay board. If that is the case, then I guess we will be putting an addition relay on a rail.
[edit] Option 3
Split the drive enables and wire X to the MESA 7i77 TB5-4 and Y to TB5-8. Run the Z enable and it's brake from TB5- 12 to control both the Axis enable and release the brake. This would take three relays to use the existing power at screw connection 207, thus keeping the hardware E-Stop in the enable loop. All three MESA Enable pins could be connected in the HAL to the single drive enable pin. Not sure if there would be an advantage in doing this.
Really nice machine you got there. Also looks like it had an easy life.
Yesterday I got Linuxcnc 2.7.10 loaded onto the ITX PC. I set it up with a CF card instead of a hard drive, but am already regretting that. Followed the WIKI to set it with no swap drive turn off and all the cacheing to a ram drive. After installation, the security updates took forever - probably because of RAM cache and no swap. I only have 2Gb of ram. I wanted a minimum footprint controller for my lathe when I bought the CF card adaptor, but space is pretty irrelevant no I am using it on the MAHO. Since I will probably have to do a final fresh install once I the development phase is over, I'll live with it for now.
Mark
Last edit: 9 years 1 month ago by RotarySMP. Reason: Add option 3
- drimaropoylos
- Offline
- Elite Member
-
Less
More
- Posts: 265
- Thank you received: 40
9 years 1 month ago - 9 years 1 month ago #99472
by drimaropoylos
Replied by drimaropoylos on topic Retrofitting a 1986 Maho MH400E
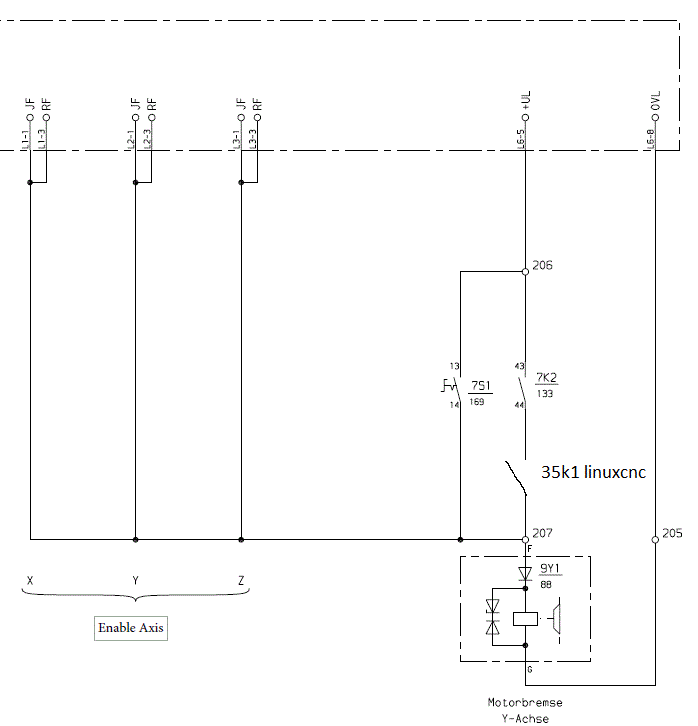
Hello, I thing we should choose the split logic of linuxcnc. And the wiring should be like this if the contact can handle the current.
Gmoccapy is the prettiest, and excellent if you put hard buttons next to screen.
I think you should buy a solid state hard drive and install LinuxCnc from the start, LinuxCnc must run to the full potential to properly calibrate the closed loop.
John
Gmoccapy is the prettiest, and excellent if you put hard buttons next to screen.
I think you should buy a solid state hard drive and install LinuxCnc from the start, LinuxCnc must run to the full potential to properly calibrate the closed loop.
John
Last edit: 9 years 1 month ago by drimaropoylos.
- drimaropoylos
- Offline
- Elite Member
-
Less
More
- Posts: 265
- Thank you received: 40
9 years 1 month ago - 9 years 1 month ago #99474
by drimaropoylos
Replied by drimaropoylos on topic Retrofitting a 1986 Maho MH400E
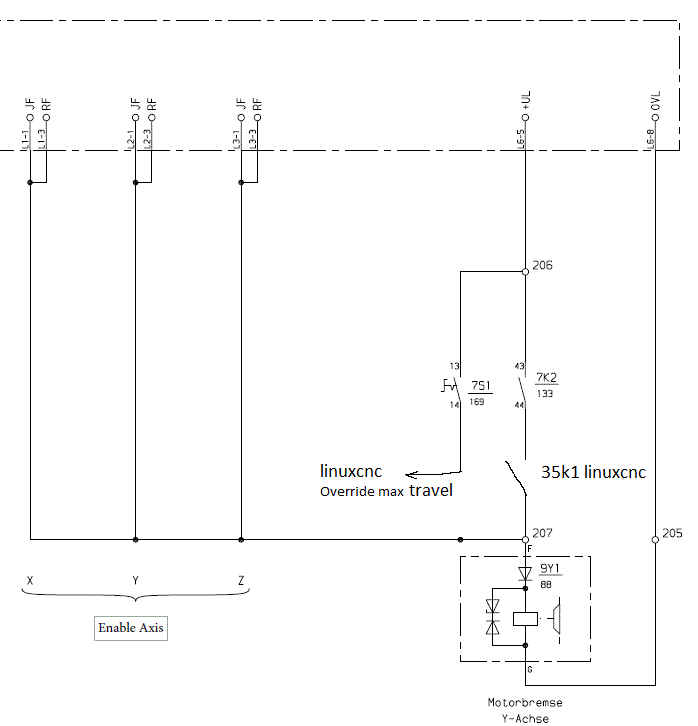
Or something like this to let LinuxCnc to temporary disable the estop for max travel
Last edit: 9 years 1 month ago by drimaropoylos.
- drimaropoylos
- Offline
- Elite Member
-
Less
More
- Posts: 265
- Thank you received: 40
9 years 1 month ago - 9 years 1 month ago #99480
by drimaropoylos
Replied by drimaropoylos on topic Retrofitting a 1986 Maho MH400E
The relay boars for the 7s1 says break release but instead enables the drive and releases break, I am confused. What is the real use of that switch?
Last edit: 9 years 1 month ago by drimaropoylos.
- RotarySMP
- Offline
- Platinum Member
-
Less
More
- Posts: 1635
- Thank you received: 595
9 years 1 month ago #99489
by RotarySMP
Replied by RotarySMP on topic Retrofitting a 1986 Maho MH400E
According to the MAHO user manual, it is to release the brake so that you can manually crank the Z axis off it's end stop. Not sure how that is supposed to work, it the drive is activated to lock the motor at the same time.
That video is quite similar to the control panel I have been thinking about. I ordered a 17" touch screen today, and also want to put soft keys around the bezel. A pendant with jog wheel is also planned. I am not planning to put as many functions on buttons as they did though.
I took a look at the relay panel and wiring this evening, but doubt we can use 35K1 for that drive enable, as we will only have access to one side of the relay. The other side goes to earth on the PCB.
Setting up the MESA cards, I noticed on MAHO sheet 12, that the Phillips had three input pins for "Enable Axis X/Y/Z". It makes no sense to implement this in this way under LinuxCNC, especially since the are all active off the same signal. I would sort of understand if each Indramat channel output a separate "Channel Ready/Healthy" signal, but it does'nt. The "Indramat ready" is fedback via L4 Bb1 and Bb2, to break the "NC Ready" chain if not ready. Seems to me like feeding that signal from L4 back to LinuxCNC as "Indramat not ready" would be a better solution.
Moderators: piasdom
Time to create page: 1.964 seconds