
- Posts: 19899
- Thank you received: 4655
Retrofitting a 1986 Maho MH400E
- andypugh
- Offline
- Moderator
-

Less
More
7 years 11 months ago #121086
by andypugh
That's a relief! I was worried that there was something really wrong with the component.
Replied by andypugh on topic Retrofitting a 1986 Maho MH400E
RotarySMP wrote: Thanks Andy, that solved the problem.
That's a relief! I was worried that there was something really wrong with the component.
Please Log in or Create an account to join the conversation.
- RotarySMP
- Offline
- Platinum Member
-

Less
More
- Posts: 1635
- Thank you received: 595
7 years 11 months ago - 7 years 11 months ago #121253
by RotarySMP
Replied by RotarySMP on topic Retrofitting a 1986 Maho MH400E
Sergey who programmed the gearbox comp for me, needed a couple of Sanvik 25x25mm insert lathe tool shanks milled down to 17mm to fit the multi-fix on his lathe.
Since I don't have the guards on, and can't use coolant, my long suffering 1/2" (12.7mm) four flute carbide end mill (bought at Boeing surplus a decade before I had the mill), was used. This mill is in pretty bad shape, from being misused as a counterbore on the lathe. It was already resharped by me on the Clarkson.
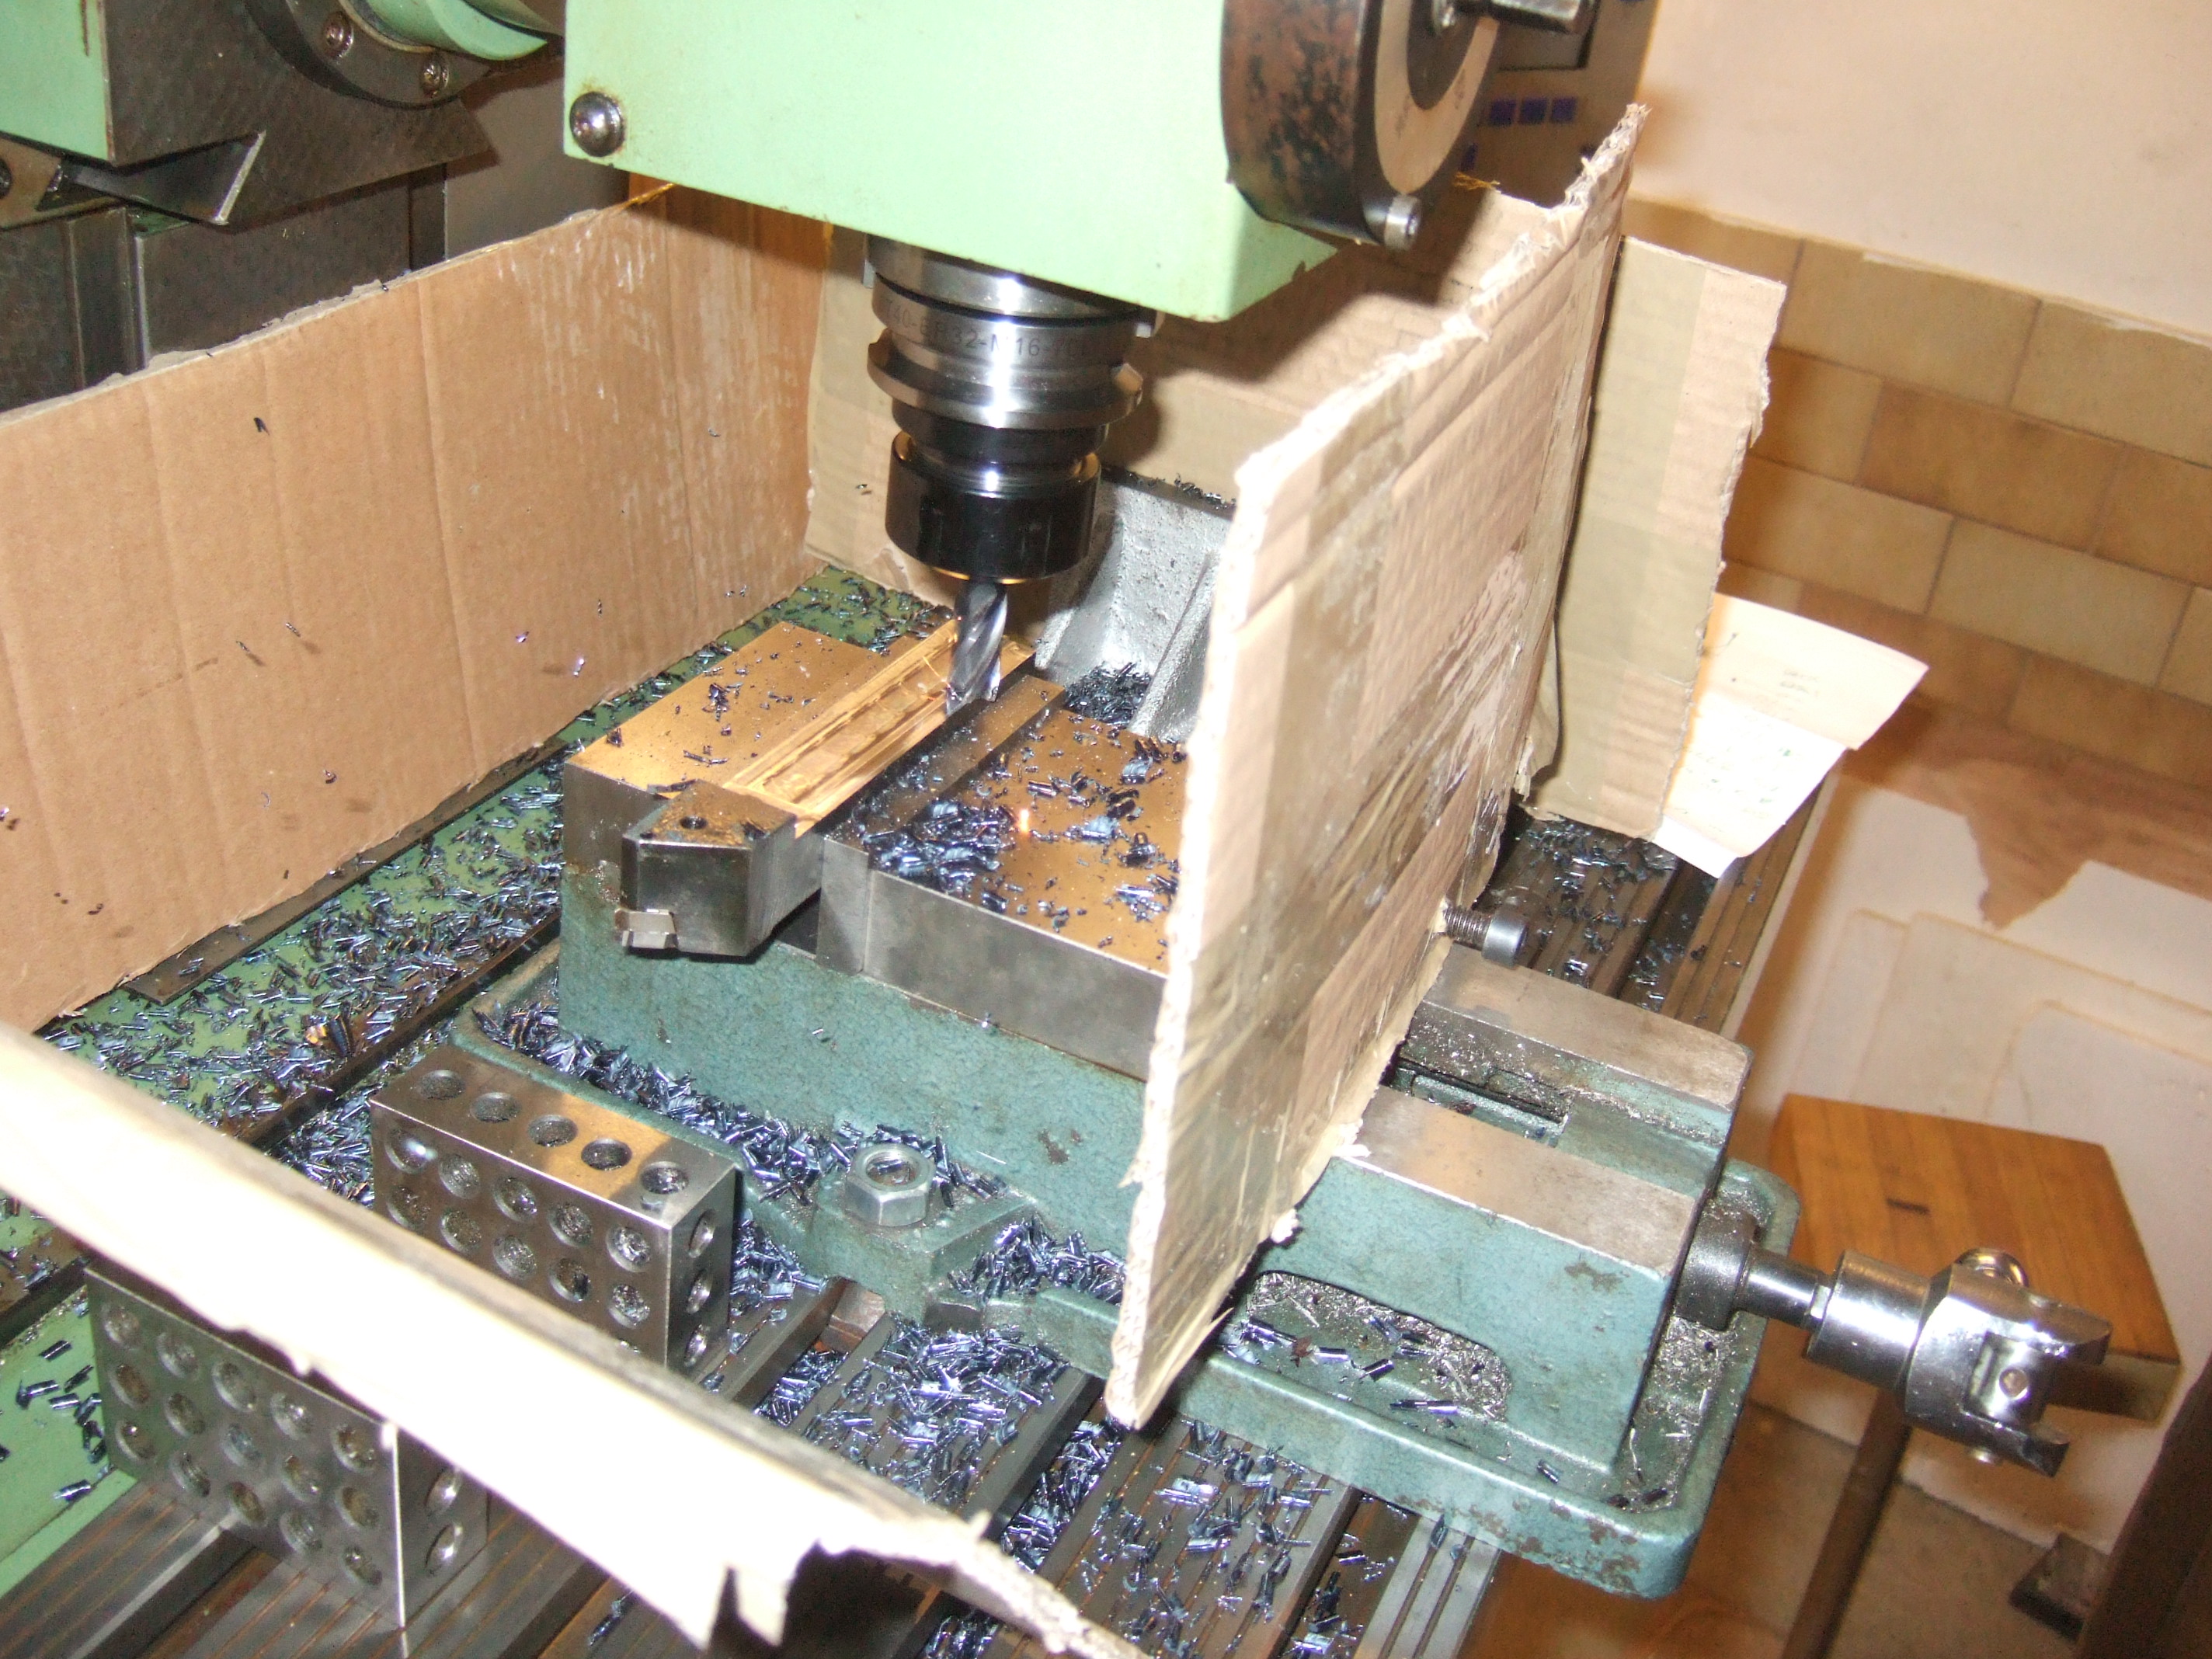
We did the first shank using a single layer program, and kept editing it and rerunning it for a lower Z. Actually the first pass, I wanted to try 0.5mm Ap, but screwed up typing and cut 5mm deep. Dumb mistake number 1. The MAHO chomped through like a champ though.
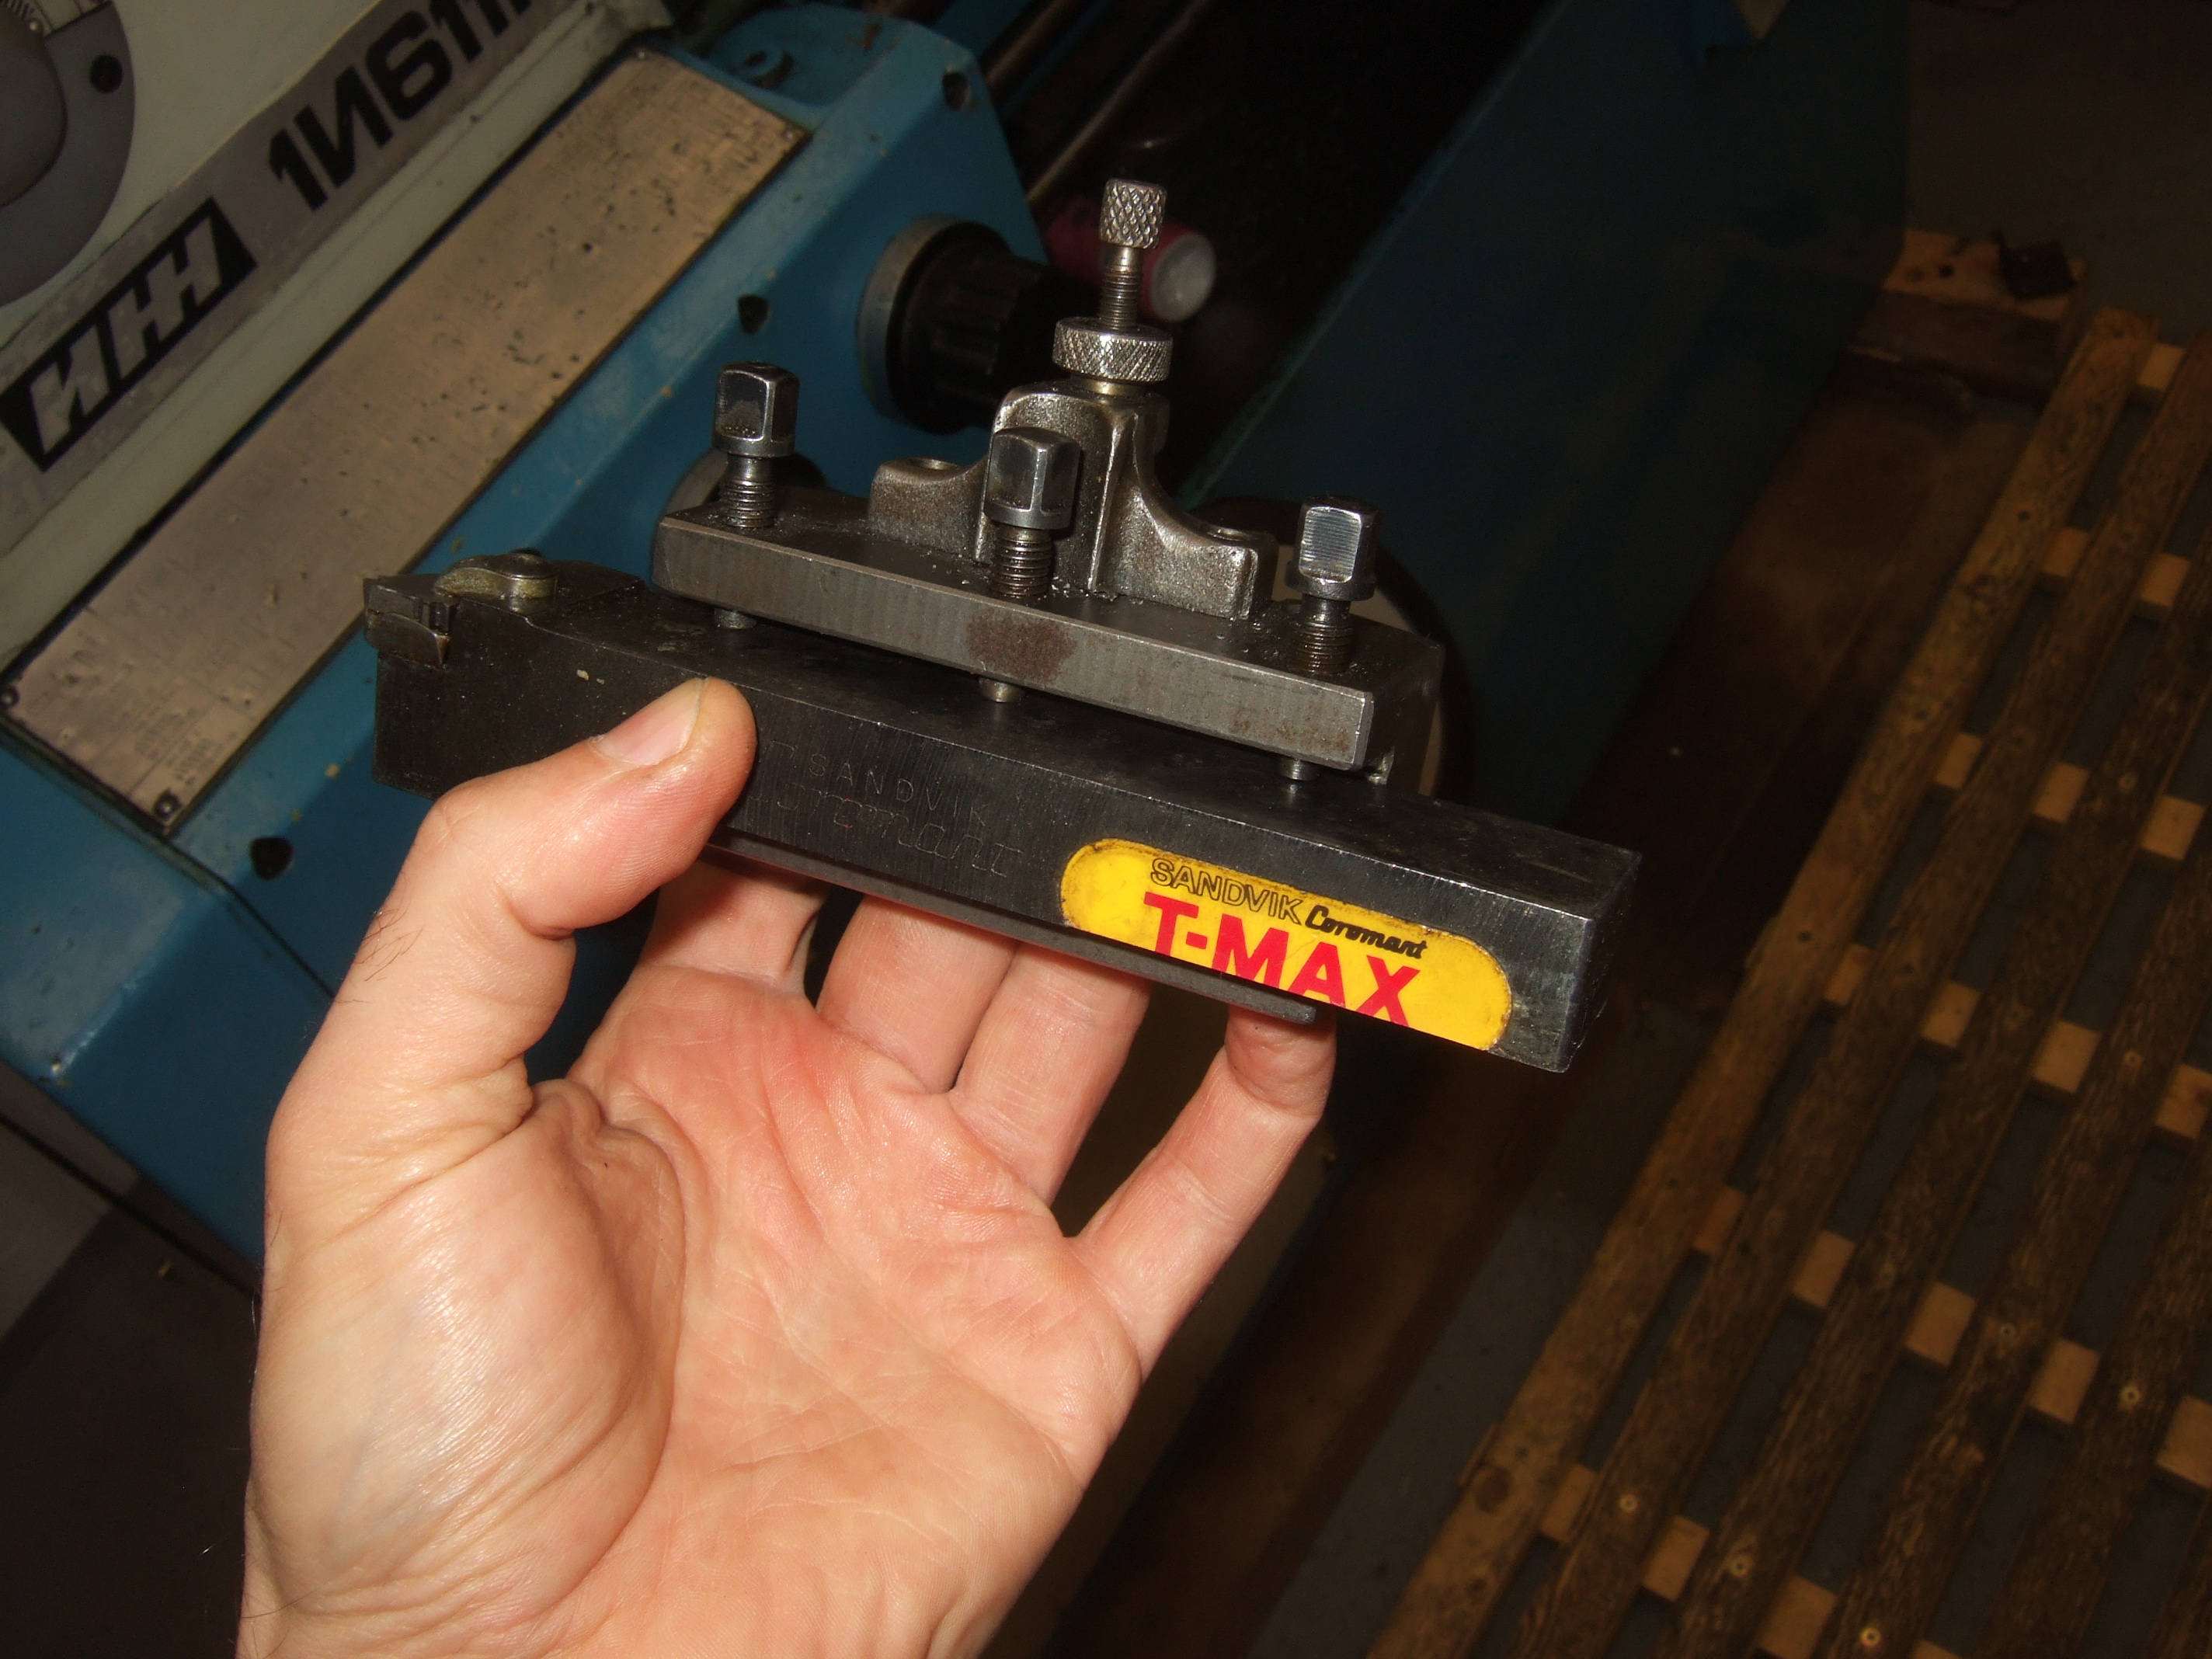
Once the first one was done, I cut/paste the code to make a gcode program to cut down the second shank in four passes.
This feeds and speed calculator feeds and speeds calculator[/url] was used, but I selected low carbon steel, rather than alloy steel. Dumb mistake number 2. Made for some fireworks, but the 1/2" (12.7mm) four flute carbide end mill was also a champ.
Unfortunately, I had an unwanted plunge cut in there. Dumb mistake number 3. This was obviously one mistake more than the mill would forgive, so the end mill gave up an edge, and is now back in the container of things needing resharpening. At least I got my stupidity on video. It seems stupidity on video is a big thing these days. I had used the LinuxCNC backplot to look for errors, and had clicked through the various views, but missed this.
Also picked up up a couple of other issues which will need to be addressed.
1/ When the spindle motor starts, the monitor sometimes blanks. I think it is a power interuption. Weird, as the original, unmodified MAHO power cable for the CRT monitor powers the LCD.
2/ The next job was to drill a 6 bolt holes for a chuck adaptor. Used a hole finder to set up pthe middle point. It turns out there is still some flakiness in the Y axis encoder. X-axis is correct, but as you can see, the scaling of the Y axis is out. It is not an INI scaling issue as the LS-403's have micron output from the EXE, and the INI is set at 1000.
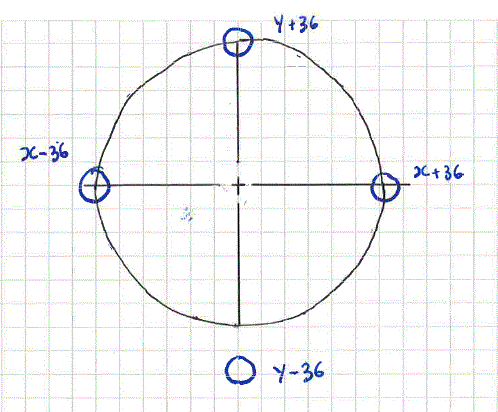
Since this Y axis encoder was flakey in the past when its supply voltage was below 5V, and last week I'd wired the active USB Hub to be powered by that same little 5V PSU, that is where troubleshooting will start.
Mark
Since I don't have the guards on, and can't use coolant, my long suffering 1/2" (12.7mm) four flute carbide end mill (bought at Boeing surplus a decade before I had the mill), was used. This mill is in pretty bad shape, from being misused as a counterbore on the lathe. It was already resharped by me on the Clarkson.
We did the first shank using a single layer program, and kept editing it and rerunning it for a lower Z. Actually the first pass, I wanted to try 0.5mm Ap, but screwed up typing and cut 5mm deep. Dumb mistake number 1. The MAHO chomped through like a champ though.
Once the first one was done, I cut/paste the code to make a gcode program to cut down the second shank in four passes.
This feeds and speed calculator feeds and speeds calculator[/url] was used, but I selected low carbon steel, rather than alloy steel. Dumb mistake number 2. Made for some fireworks, but the 1/2" (12.7mm) four flute carbide end mill was also a champ.
Unfortunately, I had an unwanted plunge cut in there. Dumb mistake number 3. This was obviously one mistake more than the mill would forgive, so the end mill gave up an edge, and is now back in the container of things needing resharpening. At least I got my stupidity on video. It seems stupidity on video is a big thing these days. I had used the LinuxCNC backplot to look for errors, and had clicked through the various views, but missed this.
Also picked up up a couple of other issues which will need to be addressed.
1/ When the spindle motor starts, the monitor sometimes blanks. I think it is a power interuption. Weird, as the original, unmodified MAHO power cable for the CRT monitor powers the LCD.
2/ The next job was to drill a 6 bolt holes for a chuck adaptor. Used a hole finder to set up pthe middle point. It turns out there is still some flakiness in the Y axis encoder. X-axis is correct, but as you can see, the scaling of the Y axis is out. It is not an INI scaling issue as the LS-403's have micron output from the EXE, and the INI is set at 1000.
Since this Y axis encoder was flakey in the past when its supply voltage was below 5V, and last week I'd wired the active USB Hub to be powered by that same little 5V PSU, that is where troubleshooting will start.
Mark
Last edit: 7 years 11 months ago by RotarySMP.
The following user(s) said Thank You: tommylight
Please Log in or Create an account to join the conversation.
- RotarySMP
- Offline
- Platinum Member
-
Less
More
- Posts: 1635
- Thank you received: 595
7 years 11 months ago - 7 years 11 months ago #121307
by RotarySMP
Replied by RotarySMP on topic Retrofitting a 1986 Maho MH400E
Since I think the last job was a little ambitious, today I took it easy. Just milled wrenching flats on all thread to make the mounting/adjusting studs for the isolator mounts which the MAHO is going to stand on. I set up the indexer* with a mag base as a stop.
I want to configure the two encoders mounted to the front panel.I need to change encoders= from 3 to 5 in the Loadrt section of the HAL, but can I configure the MESA to have the encoders 1-3 and 5,6 loading? I wired up the two additional encoders to those positions, as it fit the cable routing better.
When physical buttons are added which duplicate touch screen buttons in Gmoccapy, (e.g spindle on), do I need to use the or2 component to set up either the Gmoccapy button, or the physical button switching the output?
# --- Spindle on ---
loadrt or2
addf or2.0 servo-thread
#Input
net maho_panel.r0c4_sig-out maho_panel.key.r0c4 => or2.0.in0
net gmoccapy_[spindle.on buttont] => or2.0.in1
#output
net start-spindle or2.0.out motion.spindle-on
Is this the correct idea? Or is there an easier ways of doing this? How do I find gmoccapy's spindle on pin? Using HALSHOW there is none? I looked through the source code in github, but couldn't identify it.
Mark
* Cool tool, although whoever made it didn't have much of an eye for finishing. I was lucky to find it locally, as it takes the same 358E, W23 collets as my Boley 4LV lathe
Last edit: 7 years 11 months ago by RotarySMP.
Please Log in or Create an account to join the conversation.
- RotarySMP
- Offline
- Platinum Member
-
Less
More
- Posts: 1635
- Thank you received: 595
7 years 11 months ago #121336
by RotarySMP
Replied by RotarySMP on topic Retrofitting a 1986 Maho MH400E
Has anyone used OR2 ? Please take a look at the questions from yesterdays post, as I would appreciate a bit of help on this. At the moment i have the spindle physical buttons commented out. Also the additional encoders.
Today I needed to add further hole to turn a motor mount plate through 45°for the sand muller I am making. First time I've tried G83.
I need to find time to design the pendant housing, to learn to use CAM. Would be cool to machine a more complex part, but I am hoping that the X Bellows arrive before that, as it would be better to have flood coolant for that.
Mark
Please Log in or Create an account to join the conversation.
- andypugh
- Offline
- Moderator
-
Less
More
- Posts: 19899
- Thank you received: 4655
7 years 11 months ago #121356
by andypugh
Replied by andypugh on topic Retrofitting a 1986 Maho MH400E
I don't think you need the or2, the GUI turns the spindle on outside of HAL.
You can just connect the button direct to halui.spindle.start to add a manual spindle start button.
You can just connect the button direct to halui.spindle.start to add a manual spindle start button.
Please Log in or Create an account to join the conversation.
- RotarySMP
- Offline
- Platinum Member
-
Less
More
- Posts: 1635
- Thank you received: 595
7 years 11 months ago #121515
by RotarySMP
Replied by RotarySMP on topic Retrofitting a 1986 Maho MH400E
Thanks Andy, I didn't look at that yet, but probably will need OR2, as I have already netted the HALUI pins to the gearbox COMP, so it can turn the spindle on and off.
Yesterday, I made a new, much more conservative program to mill down the sandvik lathetool holder, using a brand new 10mm chinese HSS four flute. Use 2mm depth of cut, 50% engagement, 480rpm and 75mm/min feed. The first ~250mm went fine with nice chips, but then it died.
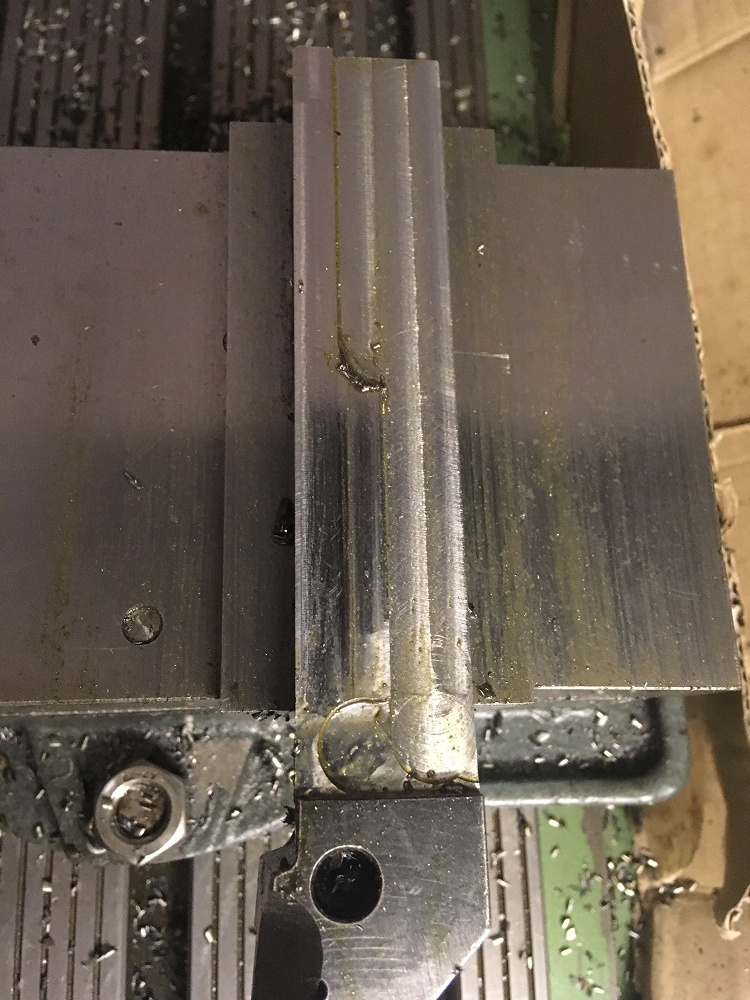
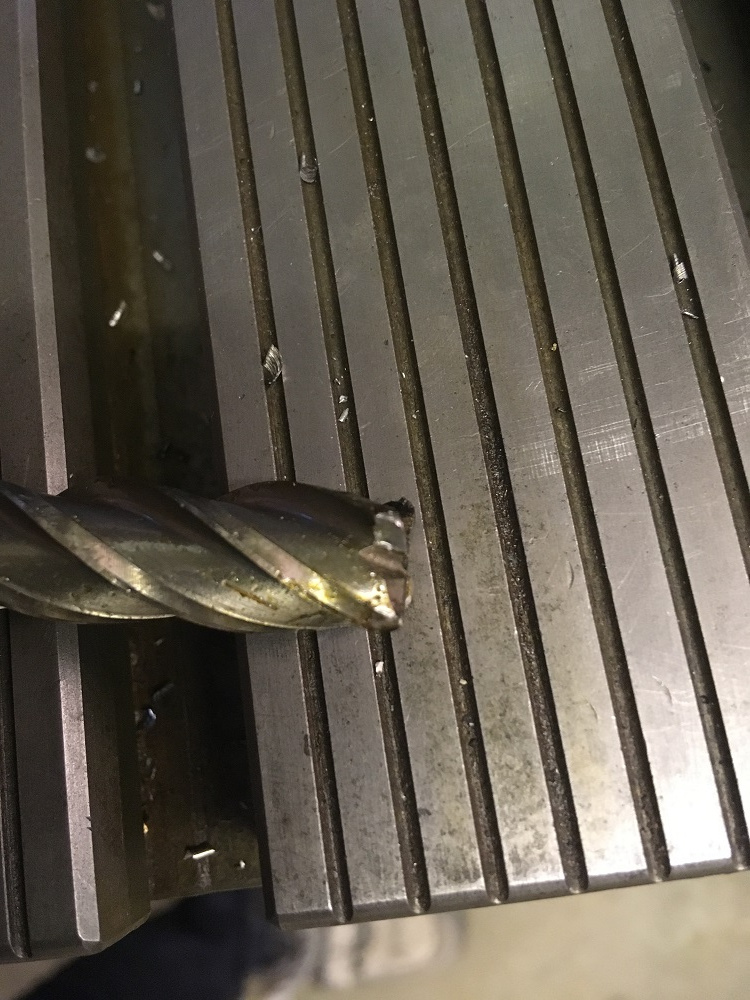
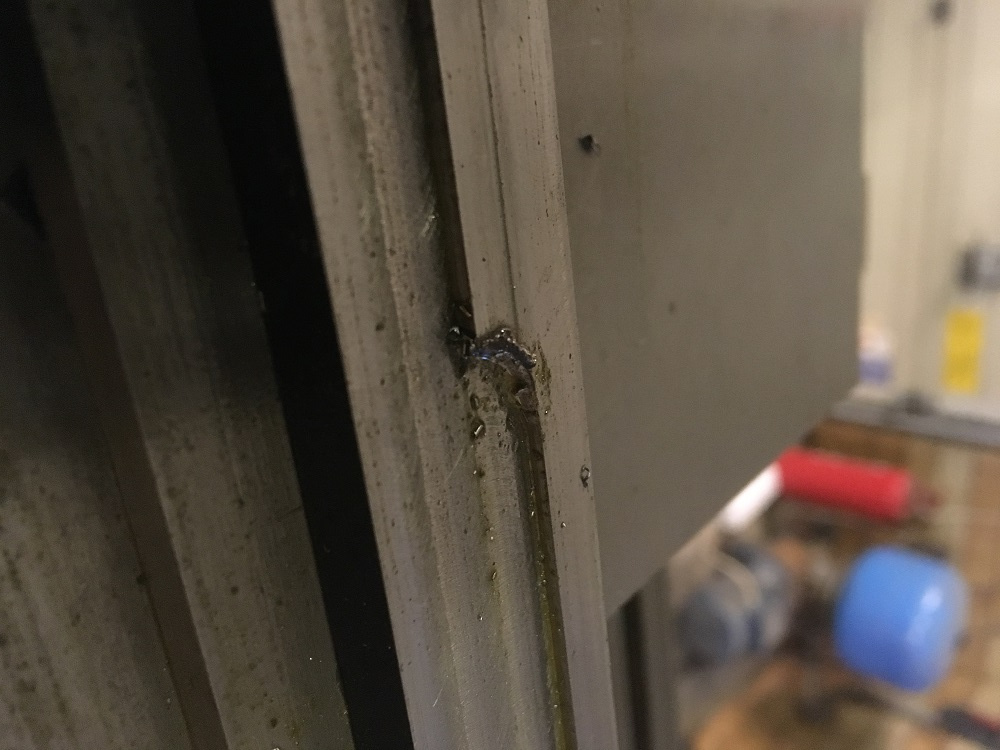
Although I did use cutting oil, itprobably need flood coolant to keep HSS cool enough to work in that steel. Oh well, another end mill for the hall of shame. Lucky I bought the Clarkson T&C grinder last year.
Mark
Yesterday, I made a new, much more conservative program to mill down the sandvik lathetool holder, using a brand new 10mm chinese HSS four flute. Use 2mm depth of cut, 50% engagement, 480rpm and 75mm/min feed. The first ~250mm went fine with nice chips, but then it died.
Although I did use cutting oil, itprobably need flood coolant to keep HSS cool enough to work in that steel. Oh well, another end mill for the hall of shame. Lucky I bought the Clarkson T&C grinder last year.
Mark
Please Log in or Create an account to join the conversation.
Moderators: piasdom
Time to create page: 0.188 seconds