
- Posts: 1635
- Thank you received: 595
Schaublin 125-CNC retrofit.
- RotarySMP
- Offline
- Platinum Member
-

Less
More
4 years 7 months ago #238544
by RotarySMP
Replied by RotarySMP on topic Schaublin 125-CNC retrofit.
Welcome William.
Hi Tommy,
Thanks for joining the conversation William, your inputs are excellent.
The back gear has to be selected with a stopped spindle out of a cut. Since there is no feedback, I would initialise the machine with a commanded high gear, and afterwards use the pneumaitc valve commanded position as "gear position", with some validation to fault out if the result is illogical.
According to the manual the original controller had CSS implemented, but then again you only got to choose from forty discrete speed steps. when programming Not sure if their CSS just stepped up through those discrete speeds, or whether they bang bang controlled the variator closed loop?
It seems to me that most cuts, at least turning, will not need large speed changes during cutting. So I could see setting the VFD to 50Hz, running the variator to the target RPM, and then letting the VFD maintain that rpm closed loop with the encoder feedback during the cut. Even for typical tapers that should suffice.
The once case where I could see the benefit of having both variator and VFD speed control during a cut would be facing a cast iron disc with HSS. The machine can swing 270mm, so you need that minimum speed of 36 at the start of the cut. Back gear, min Variator, 20Hz VFD.
Having the VFD close the loop, it will increase in frequency until topping out at 70Hz 125RPM. At that point, command the variator through to its max increase RPM stop (it takes nearly exactly 5secs for the Variator to traverse from min to max). During that variator speed change, the VFD is still closing spindle speed loop, so it is reducing frequency to maintain whatever spindle speed the LinuxCNC is commanding. Once the variator reaches the limit its travel, the vfd automatically returns to increaseing frequency until it tops out at 70hz (which is 660RPM) and the cut continues at that max to completion. For this, no addition encoders or switches on the variator should be needed. the trigger for variator command is the VFD analog speed command becoming pegged.
One limitation I see in this is that the Variator Lo / VFD Hi is 125RPM, but Var Hi / VFD Lo is 190RPM. That could be addressed by widening the VFD's speed range, or narrowing the variators.
Another limitation is that, quite early in a high torque cut, you would transition from max torque to min. Although a 3KW motor through a reduction which at that moment would be about 3:1 (6.5:1 backgear x 1:2 Var) may still be plenty?
Another strategy would use Williams suggestion and provide a look up table of 4 or 5 variator positions (eg approx 1 sec of variator activation between them) and dead reckon to approx variator positions based on time. Then just have the comp select variator positions based on required speed. There was a comment that the speed changes on variators is non-linear, with the bulk of the change coming in the last 1/5 of travel, so that I'd have to see how repeatable dead reckoning discrete steps would be.
Given that the VFD is already installed and already connected for analog control by LinuxCNC, I dont see much value in just using it for 50Hz. I could follow Tommy's suggestion and put an encoder on the variator arm for precise positioning, but given that the vfd can compensate for pretty large errors in Variator positoning, I doubt that the accuracy of closed loop variator positioning is really needed.
One thing is for sure. I need to map out the usage cases and make a flow chart of control, as my thoughts are still pretty jumbled. I did this control flow chart for the MAHO gearbox, for my mate who programmed that comp.
github.com/jin-eld/mh400e-linuxcnc/blob/...e%20flow%20chart.pdf
It is really good to have some guys to bounce idea off. Alone I would not have thought of half of the aspects affecting such a control.
Mark
The following user(s) said Thank You: tommylight
- jrosser
- Offline
- New Member
-

Less
More
- Posts: 1
- Thank you received: 0
4 years 7 months ago #238553
by jrosser
Replied by jrosser on topic Schaublin 125-CNC retrofit.
It's already mentioned above, but an approach could be to ebay/beg/borrow a linear potentiometer (like [url]
www.google.com/search?q=industrial+linear+potentiometer
[/url]) and mount it across the variator screw drive to get a simple and not too expensive way of getting the absolute position into your software through an analog input.
Some sense of absolute position would mean that there was no ambiguity if you reset the controller or at power on, and you could then drive the variator motor to position it roughly at a few defined points to make a virtual N-position gearbox. Having absolute position would also simplify the software and remove the need to 'home' the mechanism and do dead reckoning to know where you are. This is a bit of a half-way approach between dead-reckoning and continuous closed loop control of the variator position.
These linear sensors seem to ebay here for about £30, I'd expect you could find similar locally.
Thanks for replying to my youtube comment
 . Really enjoying your videos.
Some sense of absolute position would mean that there was no ambiguity if you reset the controller or at power on, and you could then drive the variator motor to position it roughly at a few defined points to make a virtual N-position gearbox. Having absolute position would also simplify the software and remove the need to 'home' the mechanism and do dead reckoning to know where you are. This is a bit of a half-way approach between dead-reckoning and continuous closed loop control of the variator position.
These linear sensors seem to ebay here for about £30, I'd expect you could find similar locally.
Thanks for replying to my youtube comment
- andypugh
- Offline
- Moderator
-

Less
More
- Posts: 19899
- Thank you received: 4655
4 years 7 months ago #238557
by andypugh
Replied by andypugh on topic Schaublin 125-CNC retrofit.
On the YouTube thread I suggested setting the VFD from a Lincurve (feedforward control) and running a PID to control the variator based on spindle speed.
The fixed rate of change of the variator might argue against that idea.
It is possible that two PID loops in parallel might work. The variator would use a PID with a large deadband and bang/bang control, with the VFD doing its own thing on top to adjust for the fixed speed of the variator.
What might work would be to have the VFD PID limits set to just a fraction more than the variator pid deadband (when inside the variator range. They could be expanded to the full frequency range at the top and bottom using lincurve)
As for only changing gear with the spindle stopped, this is only true if the gearbox has no neutral position. With speed feddback for the input and output shafts you can run electronic synchromesh. (I actually do that with my lathe, though I have magnetic clutches so there is less at risk)
The following user(s) said Thank You: RotarySMP
- RotarySMP
- Offline
- Platinum Member
-
Less
More
- Posts: 1635
- Thank you received: 595
4 years 7 months ago #238575
by RotarySMP
Replied by RotarySMP on topic Schaublin 125-CNC retrofit.
Keep the inputs coming. This really helps with focusing the options.
I just checked the manual.
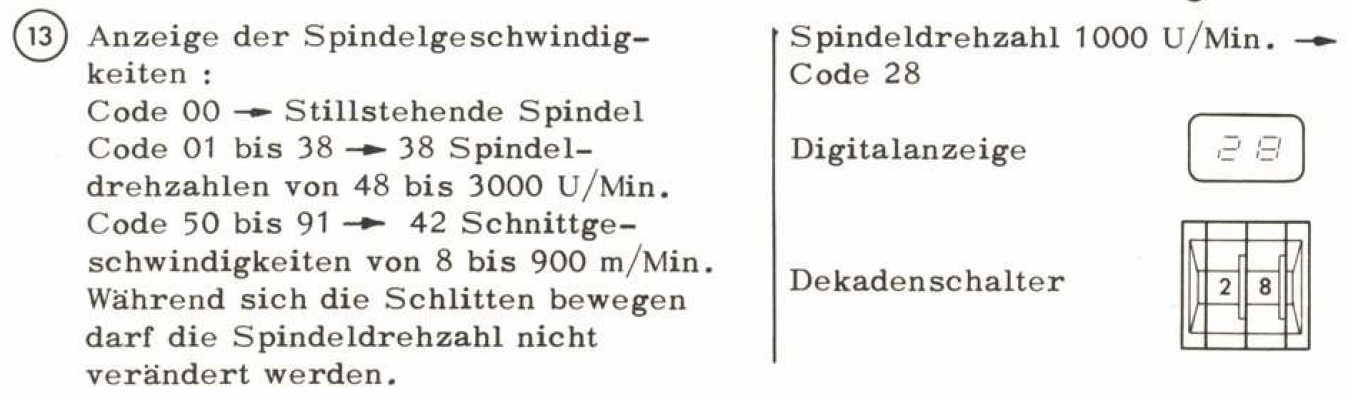
What it says is that there are 38 discrete speed settings, or 42 surface speed settings with the note that no speed changes can be made while the axis are moving. So what I thought was CSS is probably just a surface speed selection which is then interpreted as a constant RPM for that cut.
One thing I have no "feel" is how often you can drive that variator, before you chew up the contactors? Andy, when you talk of bang bang control of the variator, with a wide dead band, what would that mean in practice? It cant be a rpm range, as 20RPM down at lowest (36) is lots, but 20rpm at 3500 is nothing. Especialy with the none linearity of the variator. I guess it would need to be dead band as a percentage of current speed? Something like +/-20% adjust on VFD, beyond make a variator move first? Does this mean on a CSS cut, you buffer the start RPM, move the Variator that +20% in one go, then stop commanding it and at the same time let the VFD compensate to set -20% under speed to 20% over that buffered value? I cant picture how that can work, as the VFD is preventing the variator change from showing up on the encoder.
I am not really convinced that a feedback of Variator position is necessary yet. What do you guy feel about that? Also not sure whether dumping the contactors for a variator VFD be a good idea?
There seems to be two paths here:
- rough speed setting. Use the variator for 4 or 5 roughly fixed ratios, or,
- fine speed control. Control the variator infinitely.
Given the broad control range of the VFD It would seem to me that the first option offers the advantage of a software only solution, no risk of contactor early demise, with no practical disadvatage, assuming that dead reckoning of two or three intermediate variator positions can get roughly the repeatable ratios.
I just checked the manual.
What it says is that there are 38 discrete speed settings, or 42 surface speed settings with the note that no speed changes can be made while the axis are moving. So what I thought was CSS is probably just a surface speed selection which is then interpreted as a constant RPM for that cut.
One thing I have no "feel" is how often you can drive that variator, before you chew up the contactors? Andy, when you talk of bang bang control of the variator, with a wide dead band, what would that mean in practice? It cant be a rpm range, as 20RPM down at lowest (36) is lots, but 20rpm at 3500 is nothing. Especialy with the none linearity of the variator. I guess it would need to be dead band as a percentage of current speed? Something like +/-20% adjust on VFD, beyond make a variator move first? Does this mean on a CSS cut, you buffer the start RPM, move the Variator that +20% in one go, then stop commanding it and at the same time let the VFD compensate to set -20% under speed to 20% over that buffered value? I cant picture how that can work, as the VFD is preventing the variator change from showing up on the encoder.
I am not really convinced that a feedback of Variator position is necessary yet. What do you guy feel about that? Also not sure whether dumping the contactors for a variator VFD be a good idea?
There seems to be two paths here:
- rough speed setting. Use the variator for 4 or 5 roughly fixed ratios, or,
- fine speed control. Control the variator infinitely.
Given the broad control range of the VFD It would seem to me that the first option offers the advantage of a software only solution, no risk of contactor early demise, with no practical disadvatage, assuming that dead reckoning of two or three intermediate variator positions can get roughly the repeatable ratios.
- andypugh
- Offline
- Moderator
-
Less
More
- Posts: 19899
- Thank you received: 4655
4 years 7 months ago #238576
by andypugh
Possibly not a real issue with the use that the lathe will see in the future, I doubt you will have it working three shifts.
Replied by andypugh on topic Schaublin 125-CNC retrofit.
My concern with this approach would be uneven wear of the sheaves.- rough speed setting. Use the variator for 4 or 5 roughly fixed ratios, or,
Possibly not a real issue with the use that the lathe will see in the future, I doubt you will have it working three shifts.
The following user(s) said Thank You: RotarySMP
- RotarySMP
- Offline
- Platinum Member
-
Less
More
- Posts: 1635
- Thank you received: 595
4 years 7 months ago #238589
by RotarySMP
Replied by RotarySMP on topic Schaublin 125-CNC retrofit.
Hi Andy,
Three 20 minute shifts... per month. My dream job
If the positioning is just dead reckoning, I wonder how consistant that wear would be.Given the large overlap in vfd and variator speed range, I could also add some randomness to the timing of the dead reckoning, since the VFD wont care.
Could you please send me the link to your lathe spindle speed control comp again, so I can have a look? Thanks.
Mark
Moderators: piasdom
Time to create page: 0.955 seconds