Manual tool change problem

More
8 years 2 months ago #116542 by stidrvr
Replied by stidrvr on topic Manual tool change problem

curtisa wrote: There are ways of getting tool length compensation going in Axis following a manual tool change, but it is a little fiddly.

The way I've done it is to add a touchplate to my mill and remap the M6 command into a subroutine to make Axis measure the length of each tool every time a tool change is performed. Method is outlined here:

forum.linuxcnc.org/forum/10-advanced-con...h-off?start=30#48235

This works even if your collet/tools isn't designed to use preset-height cutters. It just measures the length of each tool and adds or subtracts that offset from the initial touch off.


This is exactly what I have been looking for. Im currently setting up my jobs in fusion using multiple setup, therefor running a separate program for each tool change. I'll look over the thread to see If I can implement using my touch plate. Thank You!

Please Log in or Create an account to join the conversation.

More
8 years 2 months ago #116575 by derekmac
Replied by derekmac on topic Manual tool change problem
Hello - thanks for all the replies.

I assume that the Z-axis DRO on the screen display is the actual tool tip position
If that is so, all intermediate positions of the display appear to be OK
impossible to measure or check as the tool keeps moving even with single step mode in operation
The first tool change always seems to occur at whatever level Z is set to at the start of the run
I can get around this by issuing a dummy tool change at the start of the program with the TLO set at around 2

Is it possible to set the AXIS GUI in some sort of pause mode during a run that will enable manual control (either by jogging or issuing MDI commands) and possibly using the touch-off command
I can only get it to do it by effectively killing the run - that leaves me with the problem of restarting it at the correct line - not good.

There is a definite bug in the M6 routines when different tool lengths are involved -
clicking on the tool change continue button instantly moves the display to the new tool position, but omits to move the actual mill Z-axis - the clue is in the "instantly".
It would be good to fix this, but where is the source code? I have found a load of code in github.com/LinuxCNC/linuxcnc/tree/master/docs/src/code but which is the relevant bit?
If I fix my own version, do I need to compile it? If so, how? Or do I just remap the M6?

The manual says about remapping the M6 code - "Note than when remapping an existing code, we completely disable this codes’ built in functionality of the interpreter".
Obviously if I am going to remap the M6 it would be good to see what the original version is doing so I can replicate it - another good reason to find the source code

Once that is fixed, I think there is a need for a new M6 that copes with different tool lengths.
If the headstock is moved to the new tool length (which is the case if the above bug were fixed) there is a risk of crashing the previous tool into the material (or other parts of the mill) if the new tool is shorter.

Tool change should be a 2 step operation where different tool lengths are involved -
first - move to the TLO position for current tool - remove tool
second - move to the TLO position for the new tool - fit new tool, save tool data for next tool change first stage

Parameters for the above operations appear to be -
#5400 - tool number
#5403 - Z tool offset
#5422 (also called #<_z>) - current Z position


My drills vary in length from 1.5" to 4.25", the drill chuck adapter adds a further 1.8" to that
I am doing a lot of drilling operations in the mill, hence the problem with the tool lengths

Jog & MDI appear to be inactive during M6 - this is explicitly stated for M0 & M1, but not mentioned for M6
So how do you jog (or do an MDI) in the middle of a program execution?


Please Log in or Create an account to join the conversation.

More
8 years 2 months ago #116579 by MaHa
Replied by MaHa on topic Manual tool change problem
Do you have the ini file entry in the [EMCIO] section
eg.
TOOL_CHANGE_POSITION = 200 200 0 (x y z)
TOOL_CHANGE_QUILL_UP = 1
?

Talking about a milling machine or router
Years ago I was not really happy with M6 because of fixed toolchange position. I have collet manual toolchange, it could be done anywhere within working area. A touchplate or toolsensor is required for my solution, first setup reference tool, then setup z offset. Use g43 in gcode.
If you or someone is interrested, tell me. I need some time to modify the files for general use, need to remove some my_machine specific parts.

Please Log in or Create an account to join the conversation.

More
8 years 2 months ago #116598 by derekmac
Replied by derekmac on topic Manual tool change problem
No - neither are set. I can't imagine why anyone would try to change a tool with the tip at Z0. Even a collet needs a bit of wiggle room (at least mine do) and a drill chuck needs even more, particularly if the drill size is near the maximum for the chuck.

Please Log in or Create an account to join the conversation.

More
8 years 2 months ago - 8 years 2 months ago #116602 by MaHa
Replied by MaHa on topic Manual tool change problem
I think most Linuxcncmachines have G53/machine coordinate system Z0 at the most faraway position from the table,workpiece. Very good idea to avoid crashing the machine. If you are working with toollength compensation, G43, it needs to be activated with the first z-move after toolchange. After the last move in z, toollength compensation must be deactivated with G49, for toolchange. Most machines refuse toolchange, if you don`t. That time z retracted to G53 Z0 (z+ direction), has nothing to do with the tooltip at all, it is the position of the Z-slide. then there should be enough space for your tool.
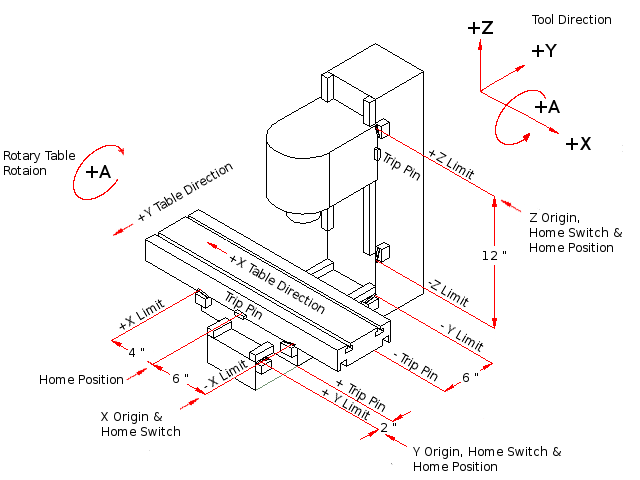
The attched picture is from the manual, Important User Concepts, 6. Machine Configurations.
Last edit: 8 years 2 months ago by MaHa.

Please Log in or Create an account to join the conversation.

More
8 years 2 months ago #116607 by derekmac
Replied by derekmac on topic Manual tool change problem
My Taig mill is very small by most standards - very much Model Engineering rather than commercial
Max travel is X11, Y5, Z5 which immediately imposes contraints on what I can do
Add to that the fact that none of my tooling is fixed and can move up and down in the chucks
I have always used it with Z0 set to the top of the material, moving Z to 0.5 for tool change with a half inch block between tool tip and material
That way I adjust the tool within the chuck to suit. Changing the tool at higher altitude would be impractical as I would have no way of adjusting it relative to the material.

Please Log in or Create an account to join the conversation.

Time to create page: 0.291 seconds
Powered by Kunena Forum