- Posts: 134
- Thank you received: 8


I try doneTry this:
Machine powered and enabled
Spindle off
watch the spindle encoder count in hal show
make a line on the spindle to have a 0 reference point where the encoder shows 0
turn spindle by hand 10 times
see the encoder count, it is 10 times bigger?
-
Check the spindle encoder scaling, if you have a 1024 PPR encoder, probably scale should be 4096.
In this case after 10 turns you should see 40960
If not, there are two possibilities, scaling is wrong or encoder is faulty/miss wired/not counting properly/does not have quadrature outputs/voltage to low/ outputs not able to swing high enough to register/

Please Log in or Create an account to join the conversation.
Please Log in or Create an account to join the conversation.
Please Log in or Create an account to join the conversation.
@abdulasis12
I noticed a similar problem with my setup. High speed spindle with encoder (36K rpm). Position would be accurate until I reach a certain rpm - 18000rpm in my case.
In your situation, you might be able to fix it (EMI?). In my case I wrote a simple COMP to reset the spindle Index = 1 or high after I issue an M3 command.
The COMP is waiting for an M3 (the spindle to reach an RPM range where the encoder signal is stable but above your tapping speed.
Hope this makes sense and it might be food for thought.
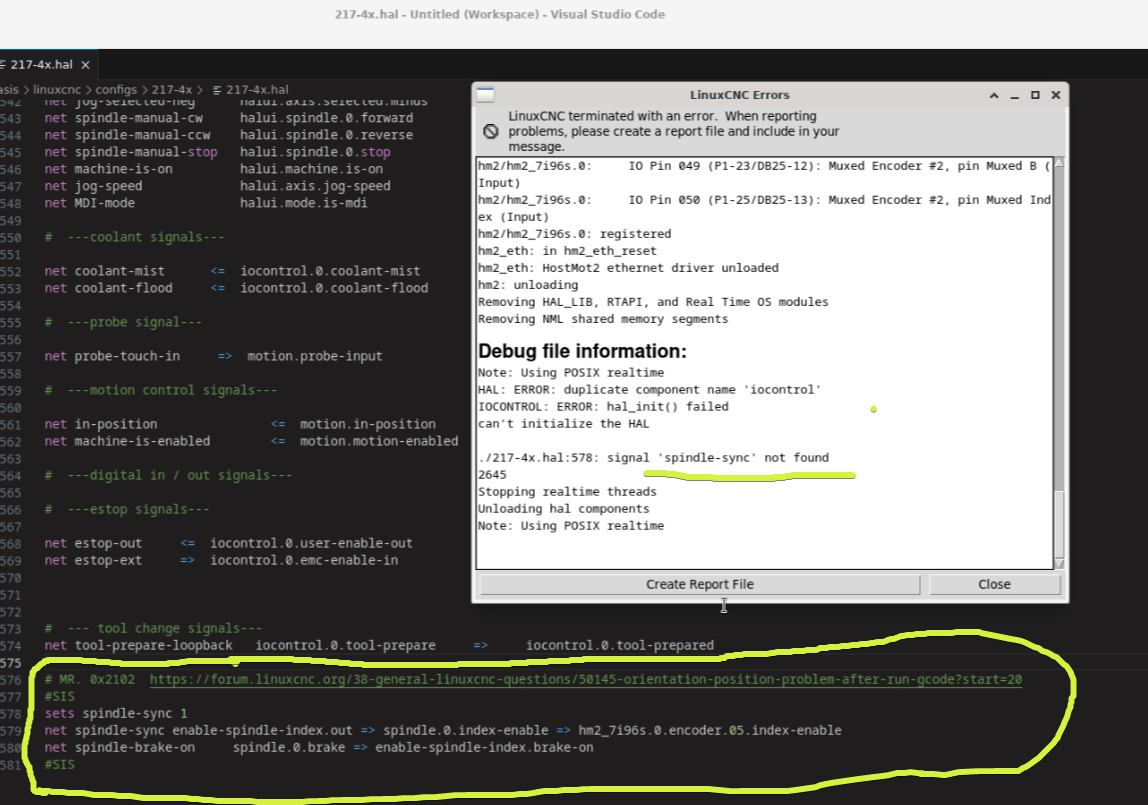
sets spindle-sync 1
net spindle-sync enable-spindle-index.out => spindle.0.index-enable => hm2_7i95.0.encoder.04.index-enable
net spindle-brake-on spindle.0.brake => enable-spindle-index.brake-on
Please Log in or Create an account to join the conversation.
Please Log in or Create an account to join the conversation.
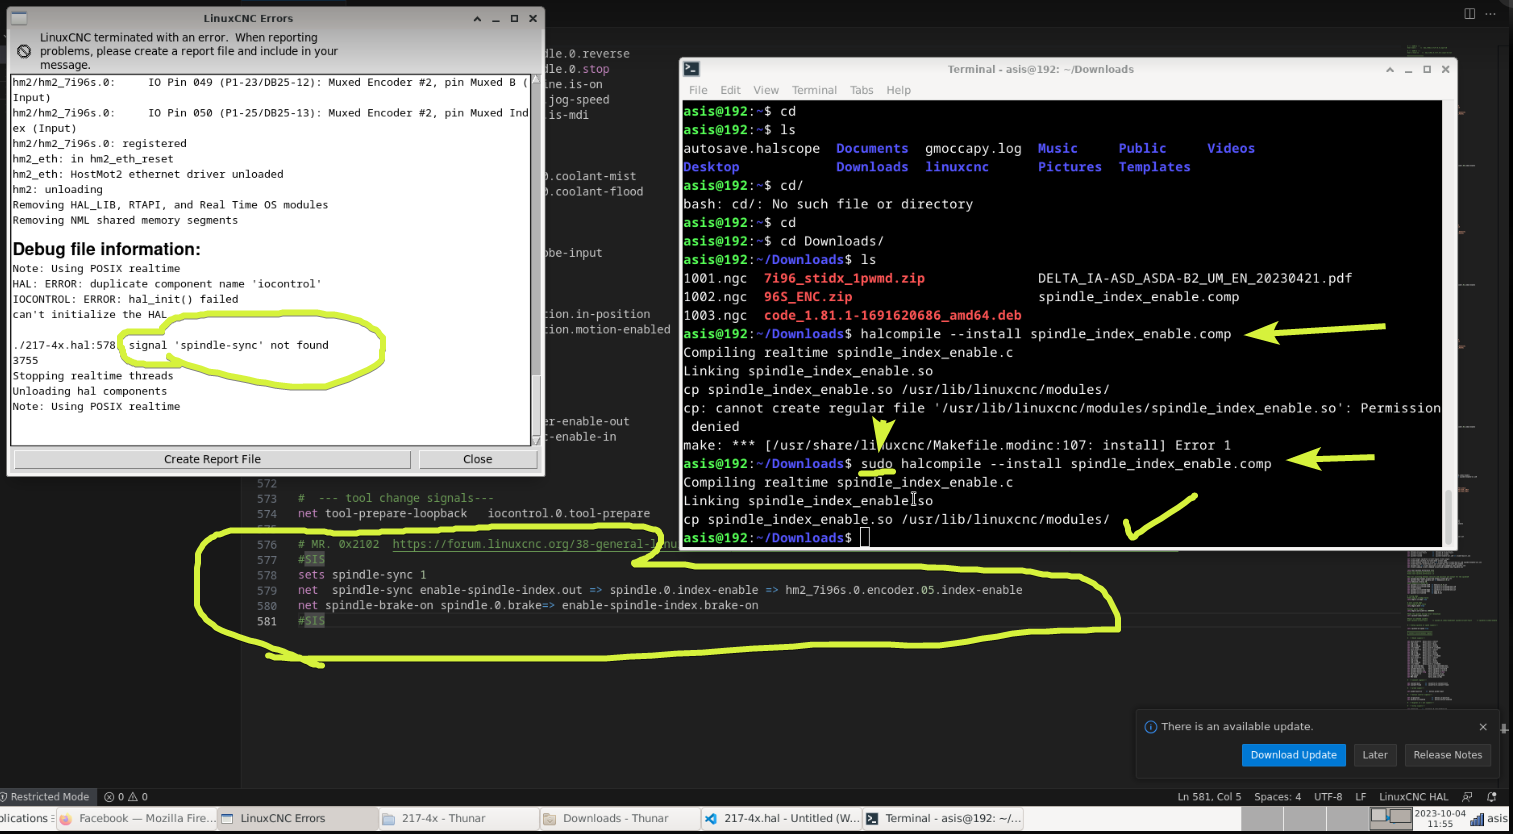
Thank you MR.Aciera1. Have you installed the component?
$ sudo halcompile --install spindle_index_enable.comp
(don't use 'sudo' if you are on a rip installation ie if you have compiled linuxcnc on your computer)
2. There also is another error 'duplicate component name iocontrol' not sure where that comes from.
Please Log in or Create an account to join the conversation.

