Lathe Macros

More
12 years 1 month ago #50926 by andypugh
Replied by andypugh on topic Lathe Macros

mariusl wrote: The lathe is setup in mm - G21 present
There seem to be an index enable pulse that occurs every revelution of the chuck.


How much does the value of motion.spindle-revs increase for a single rotation of the chuck?
I should count complete revolutions, and increase by 1 for each revolution.

Please Log in or Create an account to join the conversation.

More
12 years 1 month ago #50927 by mariusl
Replied by mariusl on topic Lathe Macros
Very difficult to say as it changes all the time. I have a very aggressive lowpass filter on the feedback.

What I just noticed is that the feedrate remains the same no matter what spindle speed I select. Surely that does not seem right?

Regards
Marius


www.bluearccnc.com

Please Log in or Create an account to join the conversation.

More
12 years 1 month ago #50928 by andypugh
Replied by andypugh on topic Lathe Macros

mariusl wrote: Very difficult to say as it changes all the time. I have a very aggressive lowpass filter on the feedback.

What I just noticed is that the feedrate remains the same no matter what spindle speed I select. Surely that does not seem right?


You shouldn't have any filtering between encoder position and motion.spindle-revs.

Also you need to make sure that motion.spindle-revs is spindle _position_ not spindle _speed_.

Please Log in or Create an account to join the conversation.

More
12 years 1 month ago #50939 by andypugh
Replied by andypugh on topic Lathe Macros

mariusl wrote: Will this feature be included in production (2.6.x) at any stage or will I have to make sure that I apply a fix after any update?


Unfortunately when I suggested adding this feature to the release version there was some disagreement with how I had implemented it.
There was a feeling that the code should be aware of the machine units, and should only convert once, etc etc.
That makes is a lot more difficult and complicated, so I gave up trying to sell the idea.

At the moment, for example, you can type "1in" and get "25.4" and then type "in" again in the same box and get "645.16"

From my point of view the extra characters are just short-cuts "in" for "convert from inches to mm" and "mm" for "convert from mm to inches" but others didn't see it that way :-/

I don't know if you have spotted it, but you can also type "3 25/64in" and get "86.122" though you do have to move the insertion point to the end before typing the "in" as the conversion after "/64" leaves it in the middle of the number in a way I haven't managed to fix yet.

Please Log in or Create an account to join the conversation.
More
12 years 1 month ago - 12 years 1 month ago #50941 by mariusl
Replied by mariusl on topic Lathe Macros

You shouldn't have any filtering between encoder position and motion.spindle-revs.
Also you need to make sure that motion.spindle-revs is spindle _position_ not spindle _speed_


No filtering between the two and it is connected to position.

From my point of view the extra characters are just short-cuts "in" for "convert from inches to mm" and "mm" for "convert from mm to inches" but others didn't see it that way :-/


Why not make a new widget rather than modify the old. Call it something else then the choice is that of the user whether he want to use it or not. That would be the democratic way I think.

Obviously this kind of widget is needed as can be proven already.

Regards
Marius


www.bluearccnc.com

Last edit: 12 years 1 month ago by mariusl.

Please Log in or Create an account to join the conversation.
More
12 years 1 month ago - 12 years 1 month ago #50942 by mariusl
Replied by mariusl on topic Lathe Macros
Some more pictures

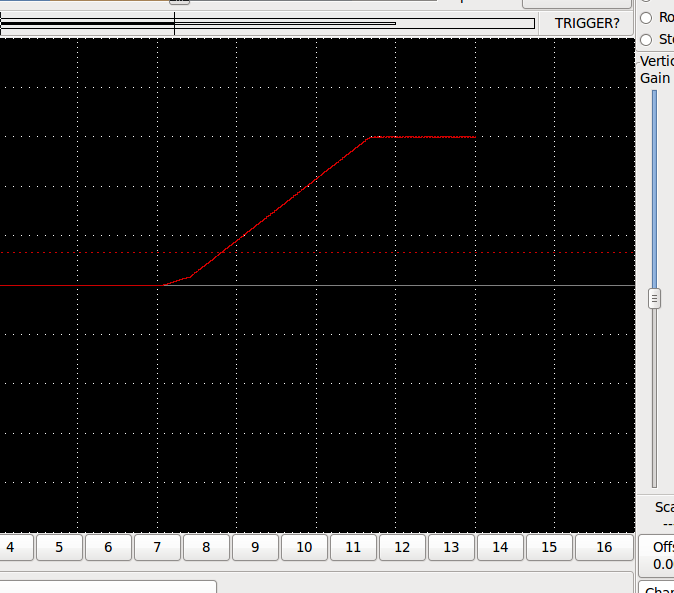
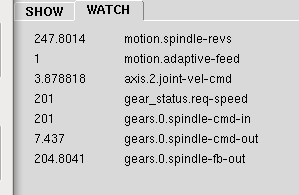
The first is the halscope capture of the velocity command and the second a halshow of some of the signals


Regards
Marius


www.bluearccnc.com

Last edit: 12 years 1 month ago by mariusl.

Please Log in or Create an account to join the conversation.

Time to create page: 0.175 seconds
Powered by Kunena Forum
