THC config that works.

More
9 years 3 months ago #95819 by ebartel
Replied by ebartel on topic THC config that works.
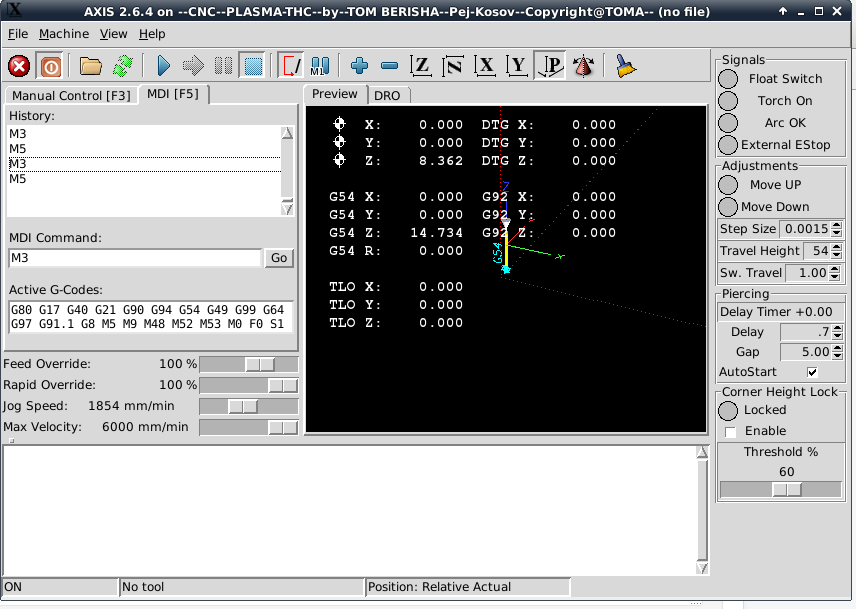
I've just finished my float switch setup and I'm trying to get the initial pierce sequence to work. My switch has 1mm of travel before activate (ie blue float switch indicator comes on). I'm cutting 3/8 mild steel so I've set the initial cut to 5mm and a delay of .7 sec. The z axis will go down, touch off, go to ~8.3 mm, and fire. This is of course to high so it just repeats.

Is there another setting I'm missing? Why does it go to 8.3mm instead of 5mm? Do I have to set something with the touch off button?

I'm a little confused as well on what the sequence is to initiall home the z axis. It seems if it is not high enough it will go down and hit the limit switch which cause a joint 2 error.

Thanks for advance for any help you can provide.

File Attachment:

File Name: thc_toma.ini
File Size:8.13 KB

File Attachment:

File Name: thc.hal
File Size:7.24 KB

Please Log in or Create an account to join the conversation.

More
9 years 3 months ago #96208 by tommylight
Replied by tommylight on topic THC config that works.
In the screenshot you have active offsets, so cancel them. Also make sure you have the correct scale for Z axis as that will mess up the height.

Please Log in or Create an account to join the conversation.

More
9 years 2 months ago #97695 by jeroenl
Replied by jeroenl on topic THC config that works.
Hi Tommy, my CNC - Plasma is really starting to work :) Thank you for all your work and help in this topic.

My plasma is a cheap one, and it needs to touch the material to ignite. Is there a option to automatically raise the torch after ignition? Or should the THC take care of this?

Please Log in or Create an account to join the conversation.

More
9 years 2 months ago #97931 by morocco119
Replied by morocco119 on topic THC config that works.
Hello, I have been trying to get this configuration up and running for the past few weeks, finally got my machine and THC to respond correctly.

However using inkscape as a Gcode generator has proven to be an issue, when I load up a file the entry point for the Pierce is not on (0,0) and when it jogs to the Pierce it wants to cut, ruining the part and cutting it in half.

Is there a way I can modify or delete some files so I can use fusion 360 as a post processor? If not can someone show me how to fix the earlier issue with inkscape?
Thank you.

Please Log in or Create an account to join the conversation.

More
9 years 2 months ago #98200 by andypugh
Replied by andypugh on topic THC config that works.
Have a look at SheetCAM. It isn't free, but it is designed for Plasma and runs natively on Linux:
www.sheetcam.com/downloads

Please Log in or Create an account to join the conversation.

More
9 years 2 weeks ago #100331 by kpj10
Replied by kpj10 on topic THC config that works.
Hi Tom,

I have posted a question regarding remembering the last position and to continue from where it left, then. Now I'm ready with a plasma table and below I mention where I'm finding it difficult to manage:

1. The complete configuration works on inches scale, I have edited LINEAR_UNITS = inch in "ini" file is this sufficient or I need to edit something more. The settings are done accordingly in other velocity, acceleration, and other section.

2. This is how I understood how to get an arc:
a. Let the Z-axis go downward until it detects the metal, as soon as it detects metal the torch is turned on.
b. Then torch moves to a certain height (I'm assuming this is the gap value, that can be adjusted in right hand side of the panel) above the surface of metal to trigger arc-ok signal.
c. Then the cut continues and the process iterates according to the program.

In my observation when I press F9 if Arc-ok signal light is green it starts taking the torch upwards, instead moving downward for metal detect. It is obvious the THC will not assign true signal for Arc-Ok until it triggers the Arc, what could be possibly going wrong. What i feel is my settings, do point out where I'm wrong:

My Z-axis is only capable of moving 0.75 Inches of total travel, so in travel height I'm setting it to 0.6 Inches. Travel height is the height I'm assuming at which plasma torch travels. I'm not getting what does switch travel value signifies, and what should I set it to.

Next is the Delay value, also I don't know what it is for but only once I have seen it to be triggered but I didn't get it why.

The gap value which need to be set is in the gap section, as 0.250 inch is sufficient should i directly set it to that value? Or is there any different math.

Threshold settings also I didn't get it.

I'm using a locally available THC, which function almost same like the Proma THC.

Thank You,
Kunal.

Please Log in or Create an account to join the conversation.

Time to create page: 0.327 seconds
Powered by Kunena Forum