

- Posts: 457
- Thank you received: 124
NativeCAM is Features renamed
9 years 3 months ago - 9 years 3 months ago #95719
by FernV
Hi Floris,
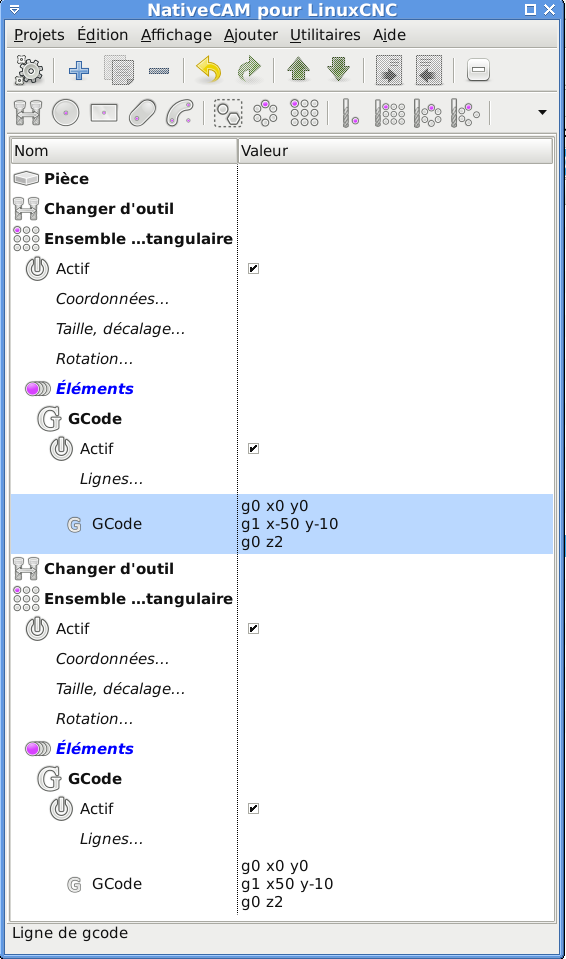
I spent much time testing and I really think tool changes should NOT be in arrays (they are in included files which are in Rectangular Arrays which make repetitive mounting and resetting tool length each time).
This way should not cause issues and tool length compensation will be applied to G54.
Fern
Replied by FernV on topic NativeCAM is Features renamed
eFalegname wrote: ...I think the problem only appears on the last "included gcode" file of the array with the tool change on its first lines.
Hi Floris,
I spent much time testing and I really think tool changes should NOT be in arrays (they are in included files which are in Rectangular Arrays which make repetitive mounting and resetting tool length each time).
This way should not cause issues and tool length compensation will be applied to G54.
Fern
Last edit: 9 years 3 months ago by FernV.
The following user(s) said Thank You: eFalegname
Please Log in or Create an account to join the conversation.
- eFalegname
- Offline
- Elite Member
-

Less
More
- Posts: 247
- Thank you received: 30
9 years 3 months ago - 9 years 3 months ago #95724
by eFalegname
Replied by eFalegname on topic NativeCAM is Features renamed
Hi Fern, the arrays work this way...
Later I'll try the second solution.
Thank you so much!
Floris
Floris,
To make sure that 'm6' is executed only once, modify the first line of your included files like this
Code:o100 if [#5400 NE 3] t3 m6 o100 endif
andCode:o100 if [#5400 NE 31] t31 m6 o100 endif
Fern
Later I'll try the second solution.
Thank you so much!
Floris
Last edit: 9 years 3 months ago by eFalegname.
Please Log in or Create an account to join the conversation.
9 years 3 months ago #95745
by FernV
Hi Floris
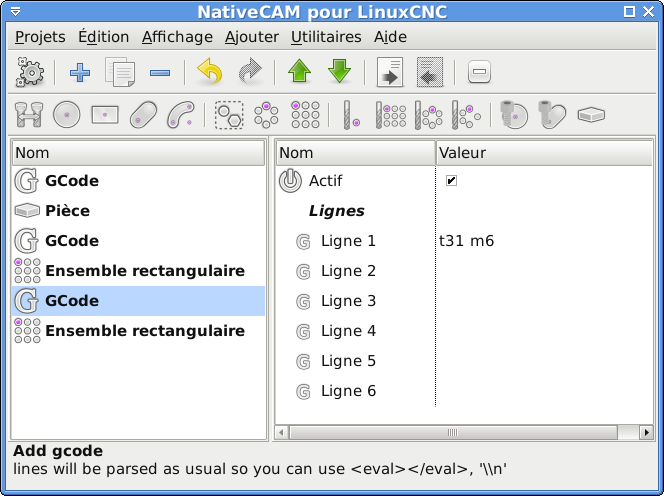
For very short custom gcode, I updated 'Custom GCode' and you can add any number of lines in it. Just hold Ctrl or Shift while pressing Enter to add a new line.
Fern
Replied by FernV on topic NativeCAM is Features renamed
eFalegname wrote: Hi Fern, the arrays work this way...
Floris,
To make sure that 'm6' is executed only once, modify the first line of your included files like this
Code:o100 if [#5400 NE 3] t3 m6 o100 endif
andCode:o100 if [#5400 NE 31] t31 m6 o100 endif
Fern
Hi Floris
For very short custom gcode, I updated 'Custom GCode' and you can add any number of lines in it. Just hold Ctrl or Shift while pressing Enter to add a new line.
Fern


Please Log in or Create an account to join the conversation.
- eFalegname
- Offline
- Elite Member
-
Less
More
- Posts: 247
- Thank you received: 30
9 years 3 months ago - 9 years 3 months ago #95752
by eFalegname
Replied by eFalegname on topic NativeCAM is Features renamed
Great job Fern!, Thank you very much! I was wondering how to introduce a starting and exit points for certain milling jobs (keyway and slot end mill), I think it would be a valid option. I would also like to impose a starting point or home position for the whole file, a place where the spindle is turned on, I do not like the spindle running over the entire work area of my cnc router before starting to mill or successive to the tool change. What do you think of my suggestion? Is it feasible?
Floris
Floris
Last edit: 9 years 3 months ago by eFalegname.
Please Log in or Create an account to join the conversation.
9 years 3 months ago #95753
by FernV
Fern
Replied by FernV on topic NativeCAM is Features renamed
Slots are in fact rectangles with rounded corners. Because of the corner options and limited time, I choose to have the starting point in the middle of an edge. I will review *-create.ngc to make it start in a corner. To start on a different edge, rotate and change the length and width as needed.eFalegname wrote: ... I was wondering how to introduce a starting and exit points for certain milling jobs (keyway and slot end mill)
Do you mean that changing the order of the shapes to cut is not enough ?eFalegname wrote: ... I would also like to impose a starting point or home position for the whole file
Adding an option in 'Tool Change' to start just before lead-in entry and stop after cut is easy. Would that be OK?eFalegname wrote: ... a place where the spindle is turned on, I do not like the spindle running over the entire work area of my cnc router before starting to mill or successive to the tool change
Fern
Please Log in or Create an account to join the conversation.

9 years 3 months ago #96202
by rene-dev
Replied by rene-dev on topic NativeCAM is Features renamed
Hi,
I got it to work, but a few issues:
after a few operations I always get this error: unable to open file <>
but the file is there. I can only recover by restarting linuxcnc.
also, in the lathe tool options, there is no option for spindle direction.
I need that, as I have some tools upside down, and nees the spindle to turn in the other direction.
Rene
I got it to work, but a few issues:
after a few operations I always get this error: unable to open file <>
but the file is there. I can only recover by restarting linuxcnc.
also, in the lathe tool options, there is no option for spindle direction.
I need that, as I have some tools upside down, and nees the spindle to turn in the other direction.
Rene
Please Log in or Create an account to join the conversation.
Time to create page: 0.137 seconds