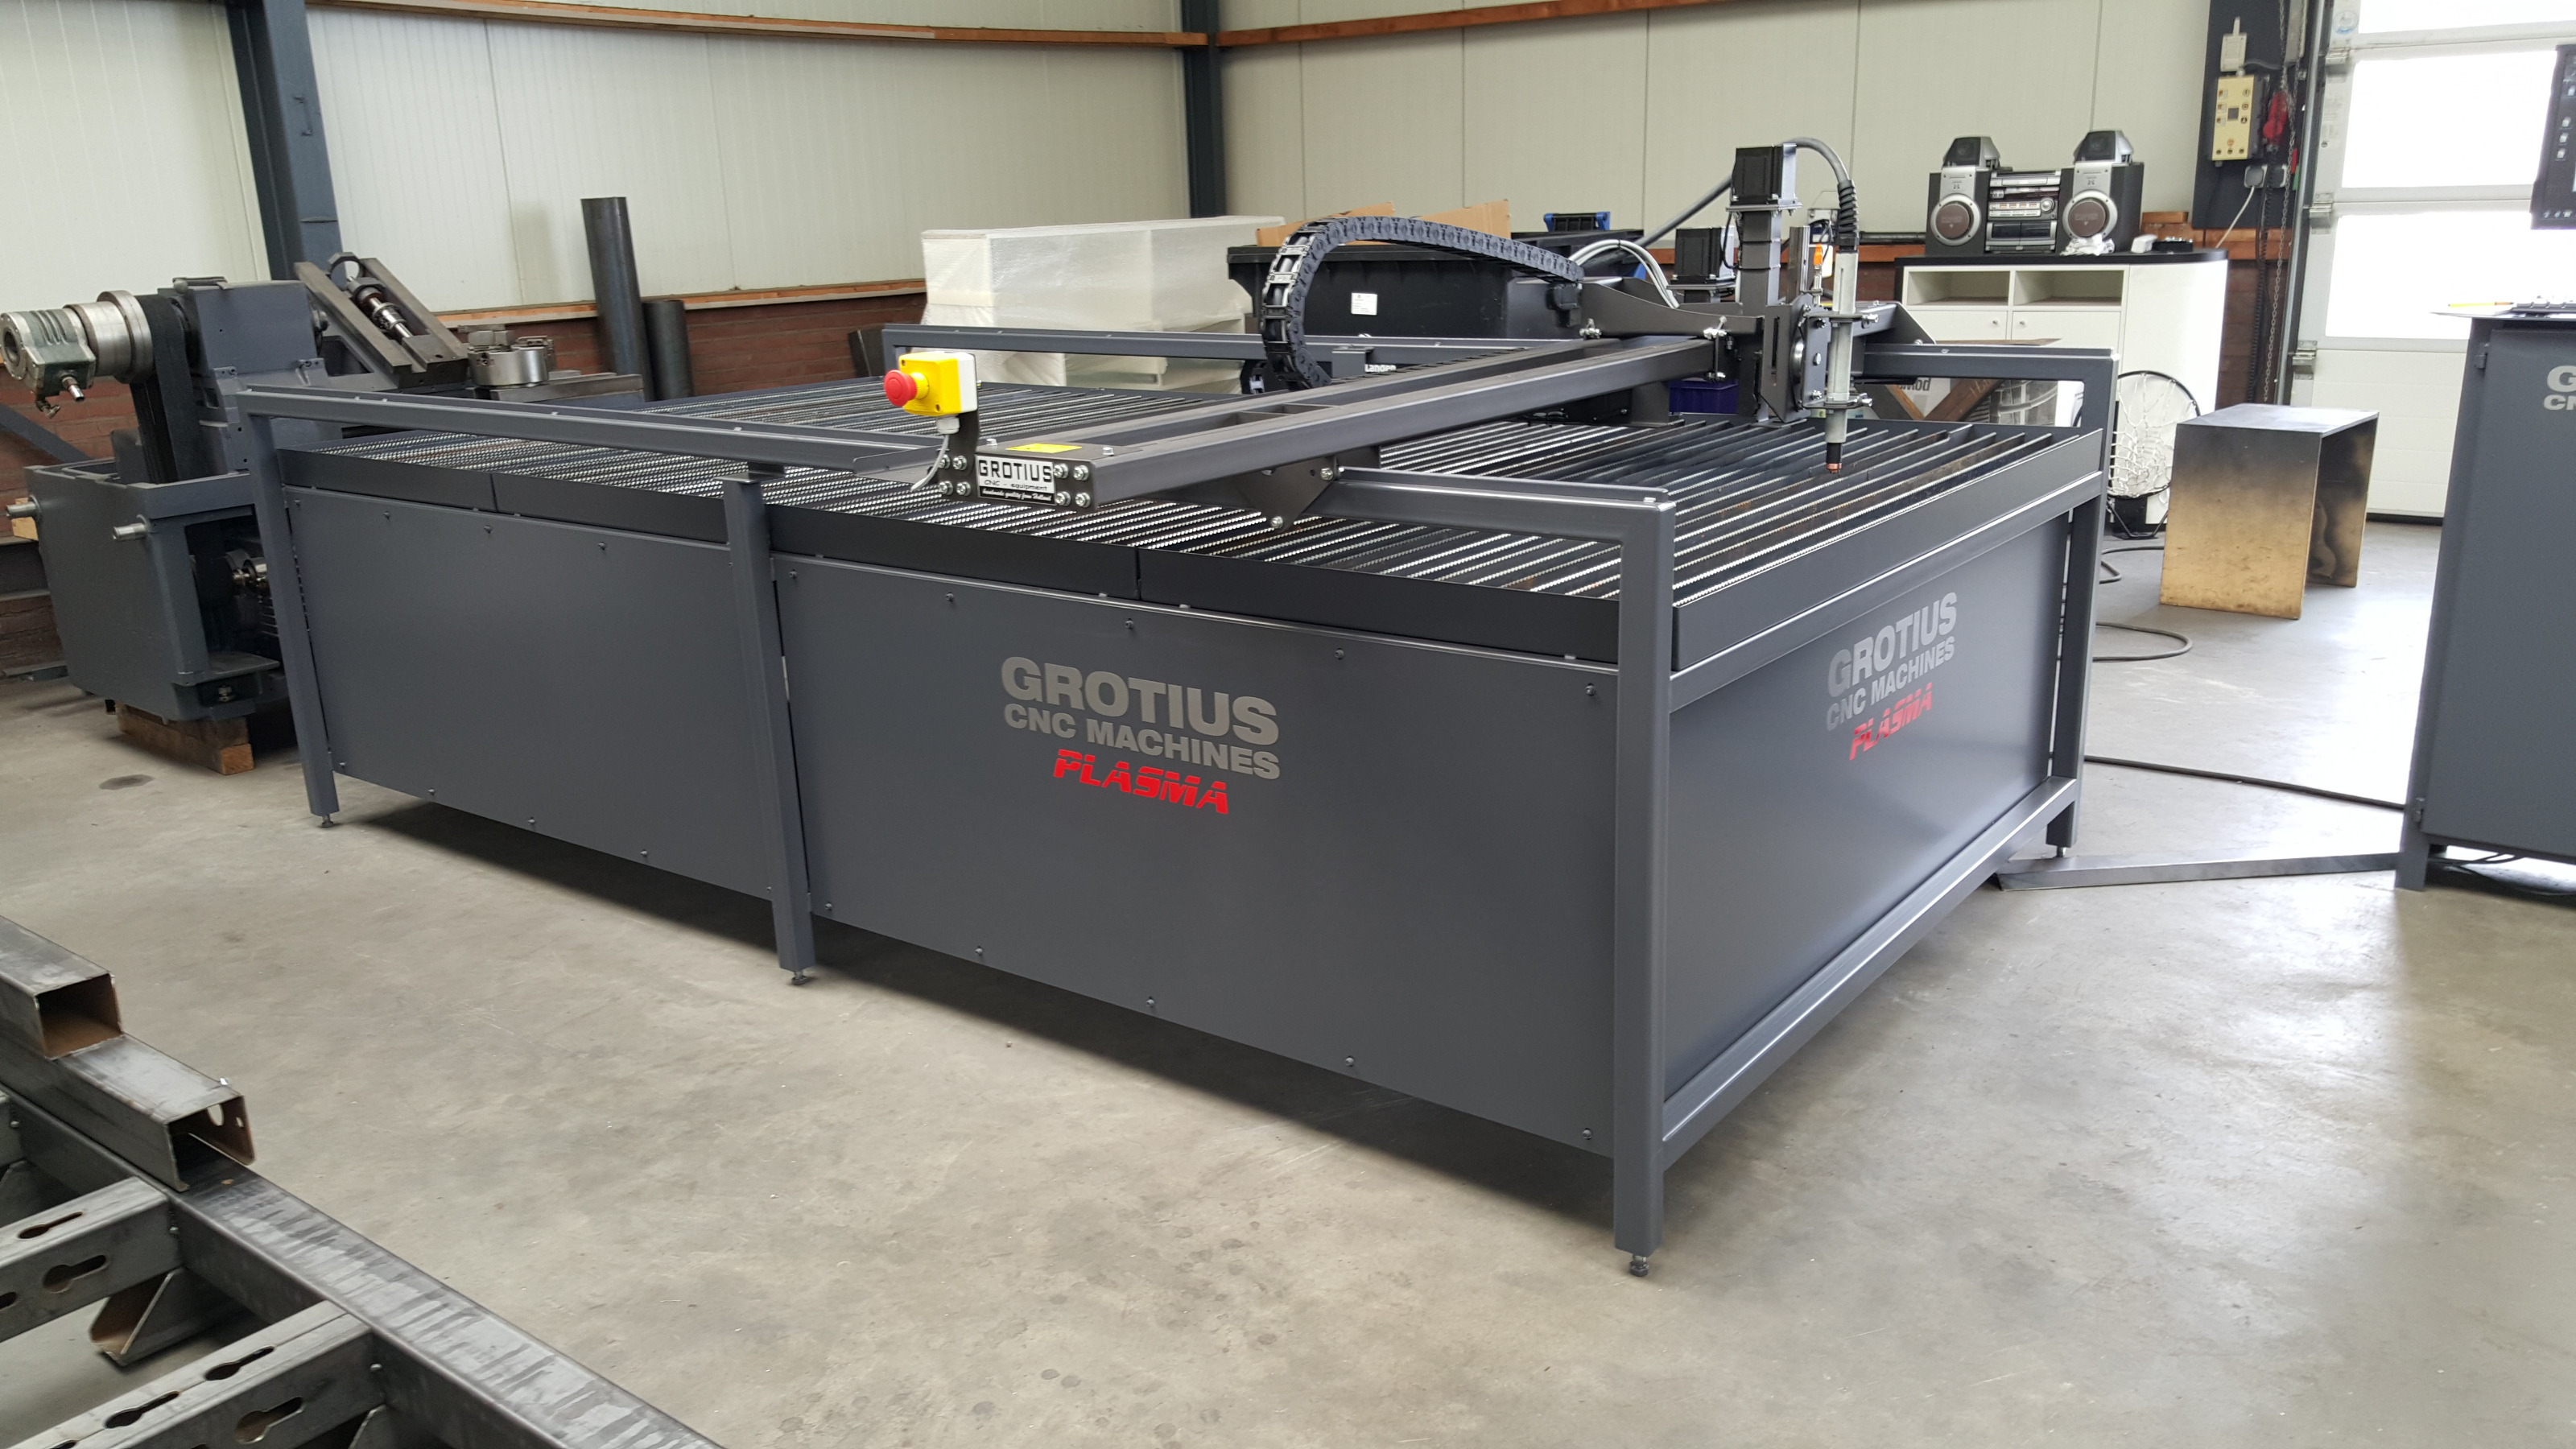
The thing with plasma CNC machines is, you have to know what you need from it. There is no "one size fits all" deal with plasma ( or any other cnc machine ).
The first and main question is: what do you want to cut with if ?
Now that is not addressed at the material you want to cut as plasma does not care much if it is cutting Alu, mild steel or extremely hard metals, that makes little difference.
Thickness makes a lot of difference as that is mainly dependant on speed, and speed is directly linked to profit i.e. less time to cut=more parts=more profit.
There are a lot of other things that will determine the speed of cut, but for us right now we are dealing with thickness.
Cutting from 1 to 3mm thick plates requires the machine to move fast, even with a 50A plasma source, so the machine needs to be light and agile and have very fast acceleration. At the other end of the spectrum, cutting 20mm thick plates goes slowly even with a 150A source, so the machine can move slowly, be heavy and have sluggish accelerations.
Then we to get to rapids. Rapids are not important for making one off's or doing large parts, say 2 to5 parts per plate. They are very important when you have to do 280 cuts in a single 2x1 meter plate and they are extremely important when doing 400 to 500 cuts on a 6x2 meter plate. This is very important for decorations and art.
Rapids greatly reduce the time it takes to do serial parts, and that in turn is good for profits.


 Topic Author