
- Posts: 12170
- Thank you received: 4153
Post Processor for LinuxCNC and PlasmaC
- rodw
- Offline
- Platinum Member
-

Less
More
7 years 4 months ago #136470
by rodw
Replied by rodw on topic Post Processor for LinuxCNC and PlasmaC
Exactly, either the gcode gets the feedrate from plasmac or the post processor (in this case sheetcam). But the feedrate is only one of the many settings contained in plasmac. The postprocessor is also designed to store these details (eg. cut height, pierce delay, pierce height feed rate etc). But the postprocessor is unable pass the parameters it holds to plasmac as there is no gcode interface.
Rule number one with data management is never to store the same piece of data in two places. So therefore, plasmac must be the single point of truth for all cut settings so the gcode generated by the post processor MUST use the plasmac feedrate. If its not done that way, there is a high risk of stuff ups if the data in the 2 systems gets out of step. Thats why the team made you come up with the current solution you now have And why it would be preferable if the user was unable to enter the feedrate stored in sheetcam while using the plasmac postprocessor.
Whilst its possible to insert code snippets altering the feedrate into sheetcam for hole cutting etc, I was hoping we could avoid altering the feedrate in these snippets and set the adaptive feed pin with M68 instead. That way, there is no need to use anything from sheetcam. Often, the THC is disabled when this is done, but I don't see that is necessary because of the cornerlock feature in sheetcam will do this for us.
Rule number one with data management is never to store the same piece of data in two places. So therefore, plasmac must be the single point of truth for all cut settings so the gcode generated by the post processor MUST use the plasmac feedrate. If its not done that way, there is a high risk of stuff ups if the data in the 2 systems gets out of step. Thats why the team made you come up with the current solution you now have
And why it would be preferable if the user was unable to enter the feedrate stored in sheetcam while using the plasmac postprocessor.Whilst its possible to insert code snippets altering the feedrate into sheetcam for hole cutting etc, I was hoping we could avoid altering the feedrate in these snippets and set the adaptive feed pin with M68 instead. That way, there is no need to use anything from sheetcam. Often, the THC is disabled when this is done, but I don't see that is necessary because of the cornerlock feature in sheetcam will do this for us.
Please Log in or Create an account to join the conversation.
- JTknives
- Offline
- Elite Member
-

Less
More
- Posts: 243
- Thank you received: 32
7 years 4 months ago - 7 years 4 months ago #136478
by JTknives
Replied by JTknives on topic Post Processor for LinuxCNC and PlasmaC
I guess my question is,
why is sheetcam posting 3 diffrent feed rates. I would think we would only need the one feedrate that gets updated from plasmac. The fixed feedrates that sheetcam puts in there where messing me up. Especially the F3.937 as it was moving so slow that the arc voltage would shoot way high and then then torch would dive into the table when it hit the F100.0
My thought is plasmac should set the feedrates and if the machine can’t do that feedrates it set then corner locking is on. It’s kinda frustrating having to have a feed rate in the gcode that matches the feed rate set in plasmac in order for corner locking to work. Being new to this I’m still veryhands on and adjusting voltage/speed on the fly to find what I really like.
Last night I was cutting these and had to enable M1 so I could switch THC off when it did the small holes. It would be nice if I could just have a tool for these holes that had the THC disabled.
Is there a readme on how I set up my tool file?
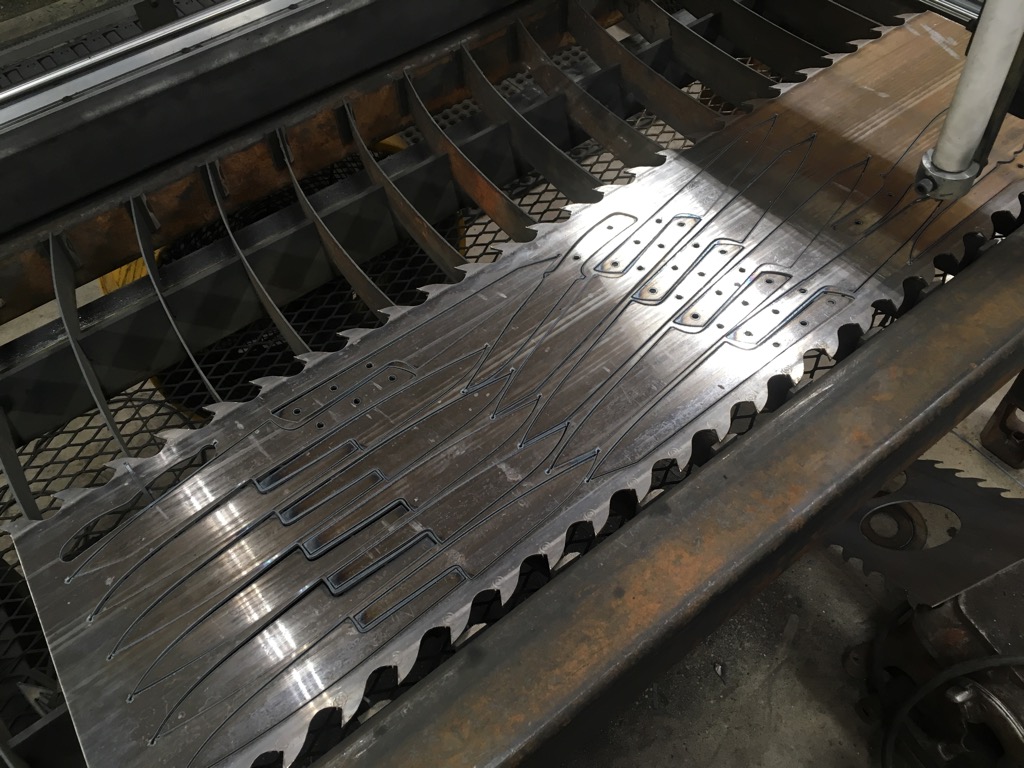
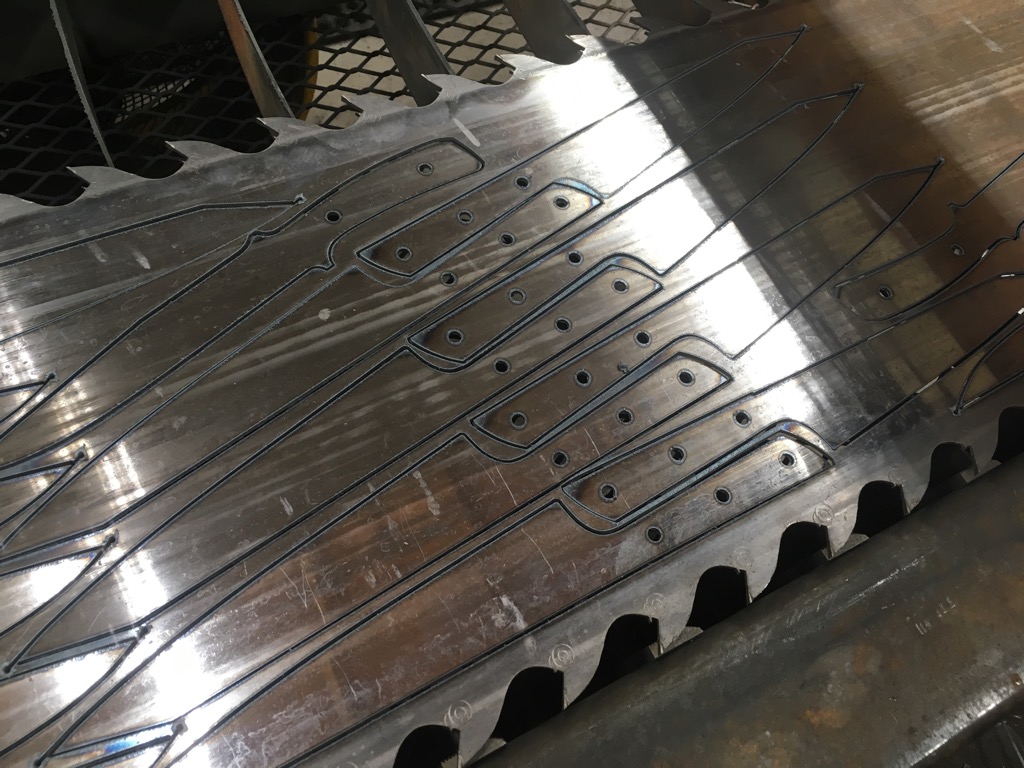
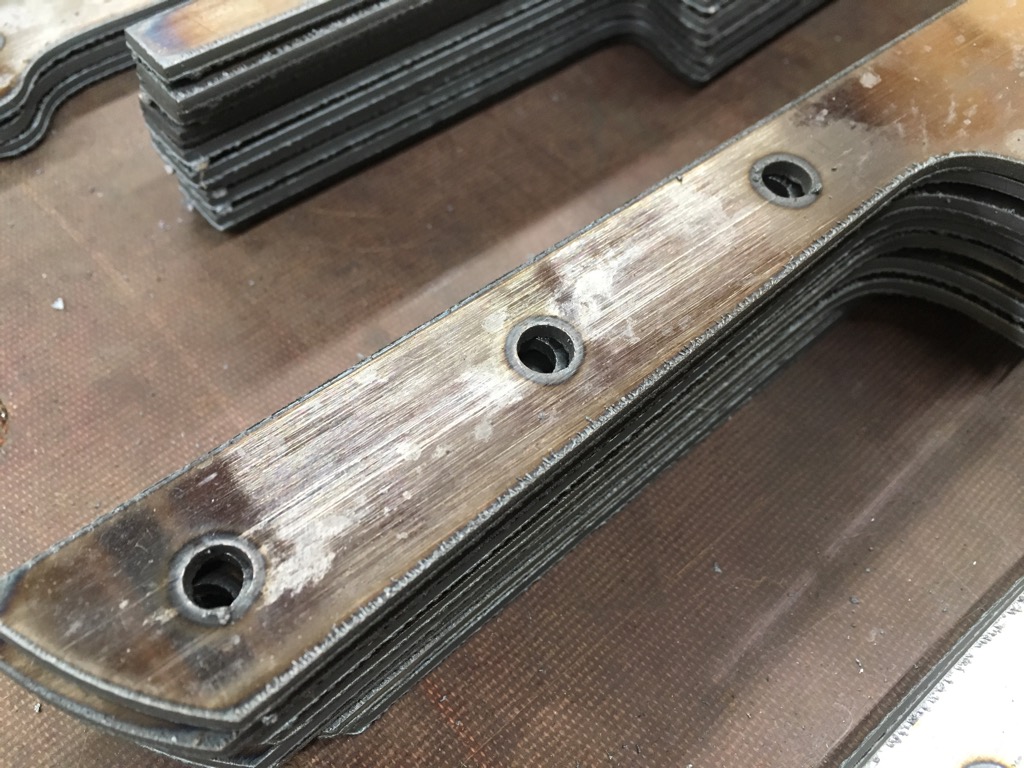
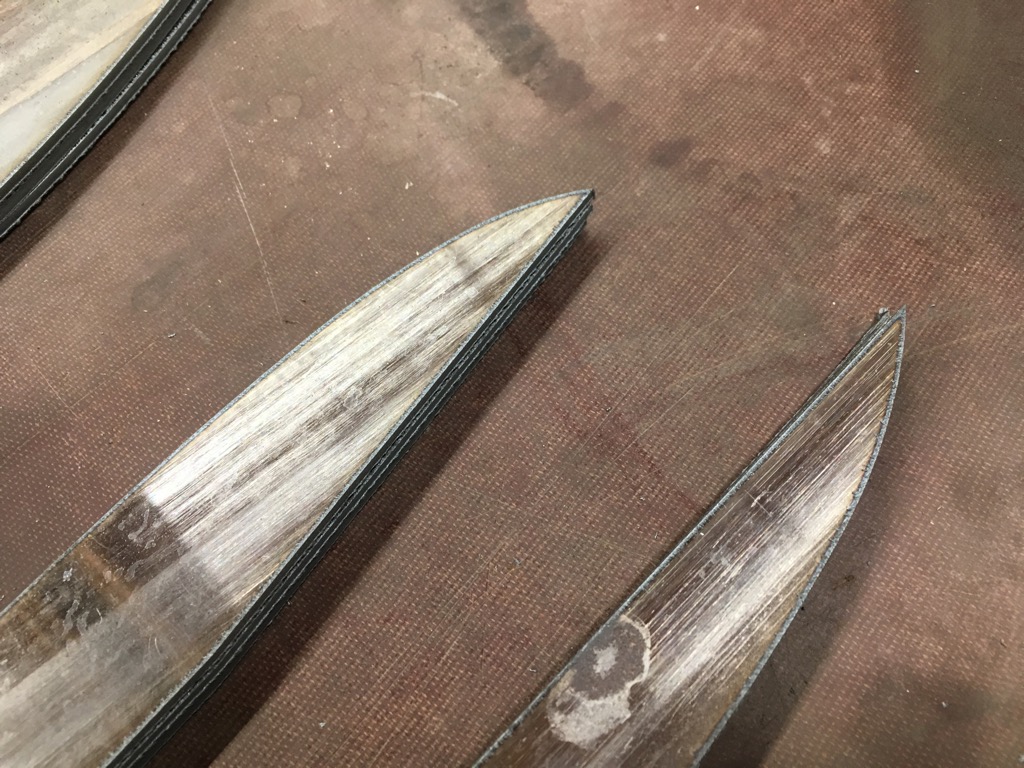
why is sheetcam posting 3 diffrent feed rates. I would think we would only need the one feedrate that gets updated from plasmac. The fixed feedrates that sheetcam puts in there where messing me up. Especially the F3.937 as it was moving so slow that the arc voltage would shoot way high and then then torch would dive into the table when it hit the F100.0
My thought is plasmac should set the feedrates and if the machine can’t do that feedrates it set then corner locking is on. It’s kinda frustrating having to have a feed rate in the gcode that matches the feed rate set in plasmac in order for corner locking to work. Being new to this I’m still veryhands on and adjusting voltage/speed on the fly to find what I really like.
Last night I was cutting these and had to enable M1 so I could switch THC off when it did the small holes. It would be nice if I could just have a tool for these holes that had the THC disabled.
Is there a readme on how I set up my tool file?
Last edit: 7 years 4 months ago by JTknives.
Please Log in or Create an account to join the conversation.
- islander261
- Offline
- Platinum Member
-
Less
More
- Posts: 757
- Thank you received: 216
7 years 4 months ago #136484
by islander261
Replied by islander261 on topic Post Processor for LinuxCNC and PlasmaC
JTknives
The reason you are getting extraneous F blocks is because your Sheetcam tool table and the Plasmac materials table are not the same. Rod's PP will work if they use the same values for feed rate. I suggest for the mean time you make sure your Plasmac materials tables are correct and match your Sheetcam tools, do not make one for every material under the sun yet only what you need for a particular job. I have used the fall back of inserting a M1 to pause the program so I can check parameters or manually change tools/settings many times.
Guys
A suggestion here. For new users CNC plasma is a steep hill to climb especially when you combine it with using a CAM program that does not have a minimal post processor for the Plasmac branch. The PP that Rod has posted as well as the one I use are adaptations of the CommandCNC post that is "overly complex" as stated by the Sheetcam author. What is needed is a simple PP with no extra features that new users have at least some hope of using with minimal effort. Most new users just want a working plasma cutter and don't care how Linuxcnc or Sheetcam work.
I may start on a really stripped down PP if I get some time.
John
The following user(s) said Thank You: Clive S
Please Log in or Create an account to join the conversation.
- JTknives
- Offline
- Elite Member
-
Less
More
- Posts: 243
- Thank you received: 32
7 years 4 months ago #136497
by JTknives
Replied by JTknives on topic Post Processor for LinuxCNC and PlasmaC
I currently dont have a material table for plasmac but i would like to.
Please Log in or Create an account to join the conversation.
- islander261
- Offline
- Platinum Member
-
Less
More
- Posts: 757
- Thank you received: 216
7 years 4 months ago #136499
by islander261
Replied by islander261 on topic Post Processor for LinuxCNC and PlasmaC
You need to add all need materials to your materials file using a text editor. The PP that Rod posted and the one I will post will not work unless you have your materials defined in Plasmac.
John
John
Please Log in or Create an account to join the conversation.
- tommylight
- Offline
- Moderator
-

Less
More
- Posts: 22011
- Thank you received: 7491
7 years 4 months ago #136529
by tommylight
Replied by tommylight on topic Post Processor for LinuxCNC and PlasmaC
That is a big blade, making small blades. Nice!
I am sure that F3.nnn should not be there, but I do not use sheetcam so I can not help much. I do think that sheetcam is the best CAM for the money, hands down. I know people who did pay way more money for CAM that was utterly useless.
I am sure that F3.nnn should not be there, but I do not use sheetcam so I can not help much. I do think that sheetcam is the best CAM for the money, hands down. I know people who did pay way more money for CAM that was utterly useless.
Please Log in or Create an account to join the conversation.
Moderators: snowgoer540
Time to create page: 0.580 seconds