
- Posts: 22011
- Thank you received: 7491
Post Processor for LinuxCNC and PlasmaC
- tommylight
- Offline
- Moderator
-

Less
More
7 years 4 months ago #136427
by tommylight
Replied by tommylight on topic Post Processor for LinuxCNC and PlasmaC
Moved from the wrong thread, my bad.
Finally nobody can say Linuxcnc does not do plasma cutting! Now there are two different types of fully automatic plasma control with integrated THC thanks to Mesa and PCW, both done in Linuxcnc but with two different approaches .
Now I need to check if plasmaC works with output from Inkscape directly, I know it did but after all the modifications somewhere I lost track. I always modify the gcode tools to output gcode without Z values and with the usual feed rate of 2000mm/minute, so I will have to check if I need any other modification to it. That is a must as all my clients use it.
If life does not get in the way as it usually does, I will change the torch and the cable on an Iskra plasma cutter I have @50A, make the earlier mentioned machine holder ( new machine torches from Trafimet in Italy, costing 190 euro a piece so I got 2 ), and finally wire the THCAD as it is still on a desk in my bedroom! Luckily plenty of Mesa cards to play with so a lot of testing is in order. Also the weather has improved last two days, it was miserable or "england weather". Sorry Andy an other UK residents, but I like summer, a lot.
FYI, was busy lately besides other things with sorting and testing roughly 150 Li-Ion batteries salvaged from laptops ( owned computer shops several years back ), and building battery packs with BMS ( battery management system ) and then testing said BMS's in preparation of finally modifying a Kawasaki GPZ600 to all electric. Need to find a decent motor or make one from an old car alternator and also build the required electronic for it.
Please Log in or Create an account to join the conversation.
- JTknives
- Offline
- Elite Member
-

Less
More
- Posts: 243
- Thank you received: 32
7 years 4 months ago #136449
by JTknives
Replied by JTknives on topic Post Processor for LinuxCNC and PlasmaC
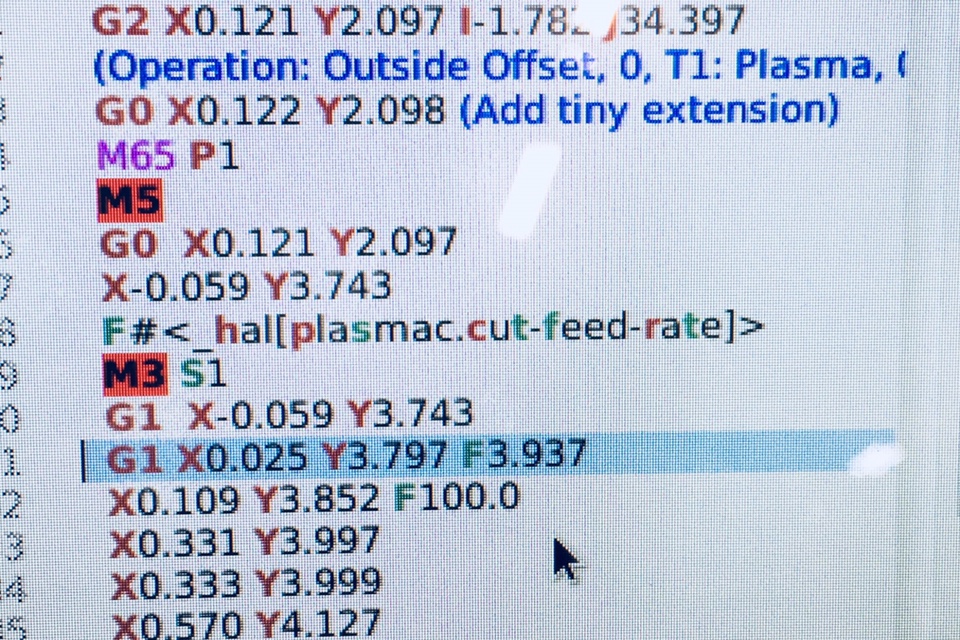
So any idea why the post processor would be spitting out these Fnnn commands? I have been manually deleting them.
Please Log in or Create an account to join the conversation.
- rodw
- Offline
- Platinum Member
-

Less
More
- Posts: 12170
- Thank you received: 4153
7 years 4 months ago #136451
by rodw
Replied by rodw on topic Post Processor for LinuxCNC and PlasmaC
Thats actually expected behaviour as its retrieving the feed rate defined in Plasmac.
Its a bit different for you because you don't have cut charts but if you had some already set up in sheetcam, Phill provided a materialverter script that will export the sheetcam tools to plasmac format.
All you have to do is make sure the plasmac and sheetcam tool numbers agree and keep the settings in plasmac.
Also, create a tool called "CENTERPUNCH". Then if you have holes you just want to mark hole centres for subsequent drilling, you can create a new layer in sheetcam and move your holes to that layer. Then do a drill operation with the centerpunch tool on that layer and it will spot them for you. It is pretty cool watching plasmac swap the tools and updating the GUI on auto pilot!
Please Log in or Create an account to join the conversation.
- phillc54
- Offline
- Platinum Member
-
Less
More
- Posts: 5711
- Thank you received: 2100
7 years 4 months ago - 7 years 4 months ago #136454
by phillc54
Replied by phillc54 on topic Post Processor for LinuxCNC and PlasmaC
If you define a F word like the F 3.937 then linuxcnc will use that as the feed rate. I don't think they should be there.
Cheers, Phill.
Cheers, Phill.
Last edit: 7 years 4 months ago by phillc54.
Please Log in or Create an account to join the conversation.
- rodw
- Offline
- Platinum Member
-
Less
More
- Posts: 12170
- Thank you received: 4153
7 years 4 months ago #136455
by rodw
The whole intent of this POST was to retain plasmac as the master of settings and the only sheetcam parameter used would be the tool number. Its not possible to delete the default variables in a Sheetcam tool setting but Les has suggested he might be able to hide them in the GUI based on a post processor setting so the only sheetcam setting visible when using the final POST is the tool number and name. So yes, they should be there.
In sheetcam speak, the M190 to select the tools is called in onToolChange() but setting the feed rate is deferred until onPenDown().so it is inserted just before the M3.
This makes sense as if a new tool is loaded M190 will select the tool and the plasmac feedrate is invoked every piearce before the M3. Its possible, it could be set onToolChange() but it seems safer this way which follows the logic in the post I started with.
JTK -- Did you notice that in 2019 Less is still talking about adding new features to Sheetcam?
Replied by rodw on topic Post Processor for LinuxCNC and PlasmaC
phillc54 wrote: If you define a F word like the F 3.937 then linuxcnc will use that as the feed rate. I don't think they should be there.
Cheers, Phill.
The whole intent of this POST was to retain plasmac as the master of settings and the only sheetcam parameter used would be the tool number. Its not possible to delete the default variables in a Sheetcam tool setting but Les has suggested he might be able to hide them in the GUI based on a post processor setting so the only sheetcam setting visible when using the final POST is the tool number and name. So yes, they should be there.
In sheetcam speak, the M190 to select the tools is called in onToolChange() but setting the feed rate is deferred until onPenDown().so it is inserted just before the M3.
This makes sense as if a new tool is loaded M190 will select the tool and the plasmac feedrate is invoked every piearce before the M3. Its possible, it could be set onToolChange() but it seems safer this way which follows the logic in the post I started with.
JTK -- Did you notice that in 2019 Less is still talking about adding new features to Sheetcam?
Please Log in or Create an account to join the conversation.
- phillc54
- Offline
- Platinum Member
-
Less
More
- Posts: 5711
- Thank you received: 2100
7 years 4 months ago #136465
by phillc54
Cheers, Phill.
Replied by phillc54 on topic Post Processor for LinuxCNC and PlasmaC
I don't fully understand what you mean by this. Plasmac doesn't set the feed rate, gcode gets the feed rate from plasmac and any subsequent F words in gcode will change the feed rate.The whole intent of this POST was to retain plasmac as the master of settings and the only sheetcam parameter used would be the tool number. Its not possible to delete the default variables in a Sheetcam tool setting but Les has suggested he might be able to hide them in the GUI based on a post processor setting so the only sheetcam setting visible when using the final POST is the tool number and name. So yes, they should be there.
Cheers, Phill.
Please Log in or Create an account to join the conversation.
Moderators: snowgoer540
Time to create page: 0.141 seconds