electronic tool setter, tool touch off process

More
5 years 9 months ago #196839 by swalts
Chris,

Success!!!!! add JOG to increments... so much more to learn. This was months in the making. 7i96 eth card works! tool setter...WORKS!!!, awesome probing routines...WORKS!!!, and now i can jog the machine without going back into AXIS gui...

Now I forgot the movie but... I feel like that kid standing in the middle of the room with stuff flying all around him, screaming IT'S WORKING!!! IT'S WORKING!!!

next thing to do is grab the micrometer and check my part for accuracy before i claim success...

MAN!!! what a struggle. I am going to make note of everything i did to get this machien up and running.

-Steve
The following user(s) said Thank You: tommylight

Please Log in or Create an account to join the conversation.

More
5 years 8 months ago - 5 years 8 months ago #197907 by Sebastianm1986
Hello, I started yesterday with Probe Basic Screen.

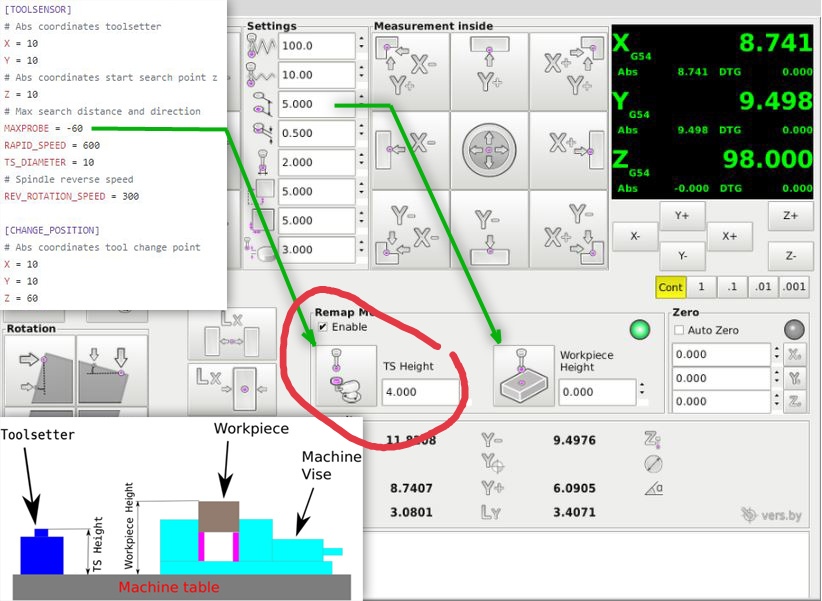
At first I have a spindle with no tool holders. Can anyone tell me what's the spindle zero is or how to measure the spindle zero? Is it like the TS height in the probe screen V2 by vers.by

I tried the following steps

1. Load touch probe tool 99
2. Tool touch off on the machine table (I'm using a fixed point. As I touch off the touch probe with the tool setter I can't say what's triggering first)
3. Z axis goes up to Z Homing position G53 Z0
4. In the offset page there's a positive value for TLO and a negative for current WC position (I used AXIS Gui before and the TLO is a negative number) example TLO is 130.5 and WC current position is - 130.5
4.a) Probing Z0 on my workpiece
5. Switching Tool setter position to my tool setter for example X68 Y7.5 Z0
6. Load tool 17
7. Touch off tool (Current WC position goes more in the negative direction)

Thx in advance

Last edit: 5 years 8 months ago by Sebastianm1986.

Please Log in or Create an account to join the conversation.
More
5 years 8 months ago #198101 by andypugh
The reference spindle zero can be anywhere. It often makes sense to use a reference tool (for example the touch probe) with a zero-length offset in the tool table, and then all the other tool lengths are relative to that.

On my mill I incorporated a tool tightening / measuring station in the table end-cover, and all tool lengths are measured from the top of the table. It's not a meaningful measure, but as long as all tools are referenced to the same point it doesn't matter.
The following user(s) said Thank You: Vector

Please Log in or Create an account to join the conversation.

More
5 years 8 months ago #198149 by Sebastianm1986
Hello,

I tried the following

1.Homing of machine, all Offsets are 0,spindle nose is also zero
2. load tool 100 spindle nose (touch probe in spindle)
3. tool touch off on my machine table
4. copied the probed value into spindle nose field
5. unload tool 100 and load tool 99 touch probe into the spindle (dragged it a little outside of the collet to see a difference)
6. Tool touch off probed tool offset is around 5 mm
7. Probing of Z0 on the surface of my workpiece
8. unloading tool 99 and loaded tool 17.
9. change tool touch off position to tool length switch
10. Probing
11. Going down to Z0 but the real Z0 is around 40 mm above my workpiece

Here's another way I've tried

1a. Homing and all offsets are cleared.
2. load tool 100 spindle nose and probing to my tool length sensor.
3. copied the probed value into spindle nose field.
4. unload tool 100 and load tool 99 touch probe.
5. Probing of Z0 on the surface of my workpiece
6. unloading tool 99 and loading tool 17
7. Probing of Z0 on the surface of my workpiece
8. change tool 17 and measure TLO
9. Going down to Z0 but the real Z0 is around the 2 mm above my workpiece

Please Log in or Create an account to join the conversation.

More
5 years 8 months ago #198218 by andypugh
Sorry, I think I have run out of help, as I don't really know what the probe screen does and I don't have a toolsetter.

Please Log in or Create an account to join the conversation.

More
5 years 8 months ago - 5 years 8 months ago #199210 by Lcvette

Sebastianm1986 wrote: Hello,

I tried the following

1.Homing of machine, all Offsets are 0,spindle nose is also zero
2. load tool 100 spindle nose (touch probe in spindle)
3. tool touch off on my machine table
4. copied the probed value into spindle nose field
5. unload tool 100 and load tool 99 touch probe into the spindle (dragged it a little outside of the collet to see a difference)
6. Tool touch off probed tool offset is around 5 mm
7. Probing of Z0 on the surface of my workpiece
8. unloading tool 99 and loaded tool 17.
9. change tool touch off position to tool length switch
10. Probing
11. Going down to Z0 but the real Z0 is around 40 mm above my workpiece

Here's another way I've tried

1a. Homing and all offsets are cleared.
2. load tool 100 spindle nose and probing to my tool length sensor.
3. copied the probed value into spindle nose field.
4. unload tool 100 and load tool 99 touch probe.
5. Probing of Z0 on the surface of my workpiece
6. unloading tool 99 and loading tool 17
7. Probing of Z0 on the surface of my workpiece
8. change tool 17 and measure TLO
9. Going down to Z0 but the real Z0 is around the 2 mm above my workpiece


The spindle zero height establishes the gauge line for all other tools, i did it this way because i have run into problems in the past when measuring agains something that can/may/will change such as a probe if damaged. this way the spindle nose will always remain a constant. once that is set , using the touch probe with G43 active will correctly locate the zero height relative to the spindle nose and all tools with actual individual tool offsets will work independently of a master tool (well in essence the spindle nose becomes the master tool).

for this to work properly you need to have a z ofset length for the touch probe as well and when you use the touch probe the G43 H99 will be active and take that probe tool length into consideration when setting the zero height. so your zero height will be to the actual spindle nose and then all other tools will be good!

Hope this helps!

Chris
Last edit: 5 years 8 months ago by Lcvette.
The following user(s) said Thank You: Vector

Please Log in or Create an account to join the conversation.

Moderators: KCJ, Lcvette
Time to create page: 0.403 seconds
Powered by Kunena Forum
