Search Results (Searched for: )

  • anfänger
11 Oct 2026 07:24 - 12 Oct 2026 08:34
Replied by anfänger on topic calling all probe basic lathe users!
I was gone for three years or so, cause I was moving house and shop.
I really fired um my lathe yesterday for the first time and updated to late latest version.
Great job guys and a big thank you to all who ware woking on the project, remembering how everything started this was smooth!
Just some things from my side to consider with the changes in the INI.
But it seems to run now and the conventional cycles are great now.
There are two thing I am missing.
One is, I would love to have a Hal pin for the jog increments to use fron the GUI. I have a user tab now for that, but I could use the space for some other stuff.

And a safety zone before the spindle. to not crash into the chuck, but to be able to also machine without one.
Kind of a tool table but for lathe chucks. then one also could set a limit to the RPM depending on the chuck.
At the moment I need to edit my ini for that.
But maybe there is already a solution for that. besides ignore limits.
I guess I'll give this lathe chuck extension a try, to get back in the LinuxCNC handling. I'll open a new topic for that.
  • tuxcnc
11 Oct 2026 06:48
This is a great project that may beat all others in the future because it supports all LinuxCNC g-codes, including those that will be added in the future. I'm not kidding, the simulator will show all the movements that will be sent to the virtual controller, no matter how they are generated.

Unfortunately, the project also has many drawbacks, which is not surprising at this stage of development, but makes its use in practice very difficult.
What I miss most at the moment is tool changing.
Of course, LinuxCNC will replace the tool, but the simulator will use only one, configured in its own ini file...
Honestly, I don't really have an idea how to solve this problem.
I thought about REMAP M6 in an ini file that could run any program, so also one that would inform the simulator about a tool change. But what will happen when the user wants to use his own REMAP M6 and see its operation in the simulator?
By the way, simulating tool measurement would also be useful...
  • FabLabRacing
10 Oct 2026 20:13
Replied by FabLabRacing on topic Is this a bug?
I was able to run the GCode above without issue, so I dont think its your GCode
  • HansU
10 Oct 2026 19:59 - 10 Oct 2026 20:05
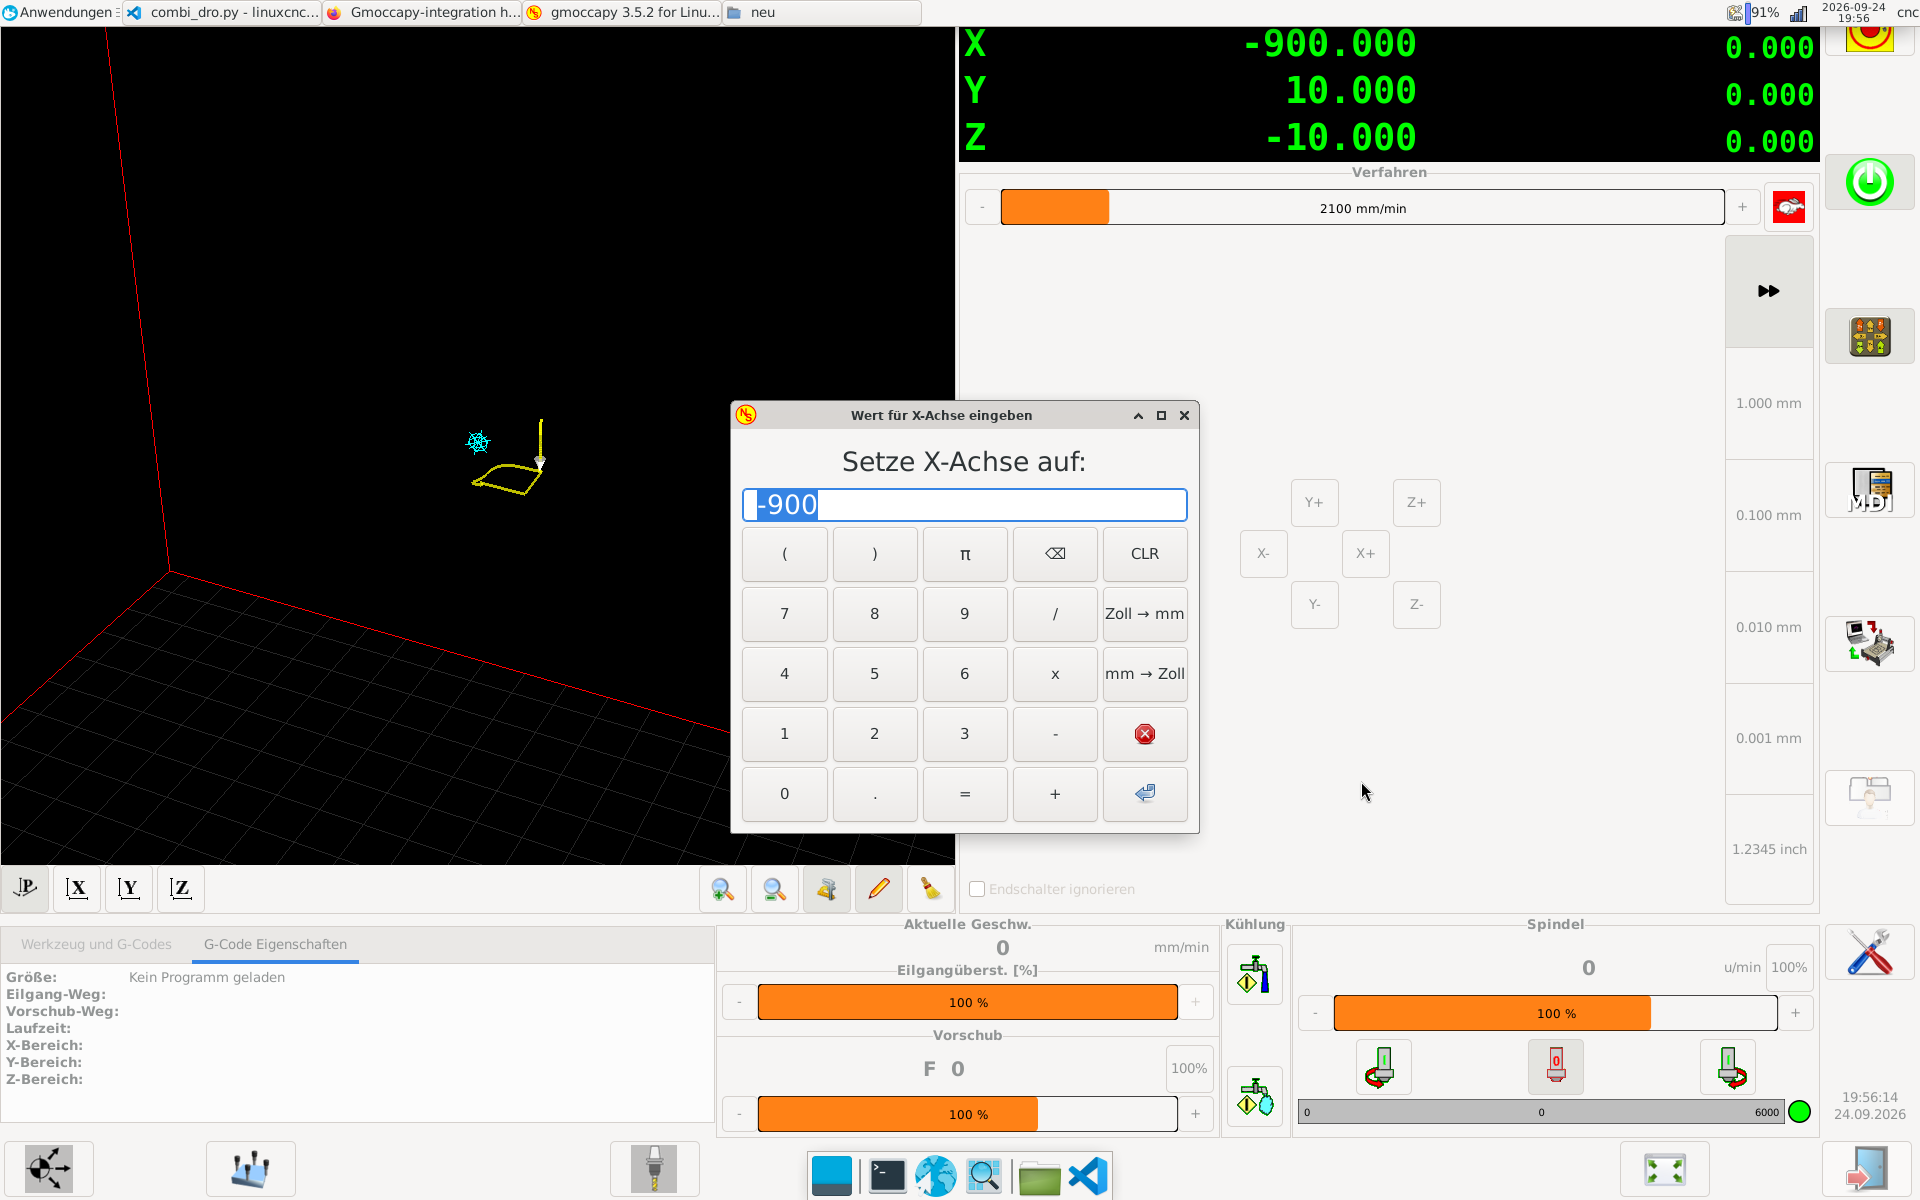
Replied by HansU on topic Re-designing the Gmoccapy DRO

I deleted all the G54s. Where will you put the G54 now (important information) and why will it be better?

On top like in my example image.
This also has the advantage that on touch off the task bar doesn't hide the X value like it currently does (in fullscreen mode).


I also talked with Norbert that we might don't display the coordinate system at all in the DRO, because it is already displayed in the G-Codes section.
  • Odessit
10 Oct 2026 19:18
Ah, got it, thanks. The supabase.co one is also mine. Supabase is a hosted Postgres database (open source, basically a self-hostable Firebase alternative), and it's the backend of the site: license keys and trial activations, the small forum on the site, and site settings like prices, download links and the support e-mail.

The footer pulls the support e-mail from it, that's why you see it on every page. It's just plain database reads, no tracking or ads.
  • tuxcnc
10 Oct 2026 15:41
Replied by tuxcnc on topic Re-designing the Gmoccapy DRO

Because the window is wide and low.
Removing G54 from all but one line will not give us any more space to display anything.
However, moving G54 to another line requires adding a new line, which means there will be less height for the position and more width, which we already have in excess of...
I'll say it again.
A CNC machine is not a toy, it may damage something or injure the operator, so the most important information and buttons must be large, legible and easy to find and use.
Whether it will be pretty or ugly is secondary.

I deleted all the G54s. Where will you put the G54 now (important information) and why will it be better?
 
  • HansU
10 Oct 2026 13:27
Replied by HansU on topic Re-designing the Gmoccapy DRO

Yeah that's also a possibility, but the duplicated "G54" consumes too much space IMHO.
 
There is no way to avoid this.
If we assume that G54 needs to be displayed somewhere, then we might as well display it several times and we need to have room for G59.3 (two more characters).
Why do we need it several times?
There cannot be different coordinate systems for different axes.
  • Hermle_Gerald
10 Oct 2026 11:38 - 10 Oct 2026 11:55
Hermle auswahl Mesa Karten was created by Hermle_Gerald
Hallo, ich lese nun schon länger hier mit.
Ich besitze eine Hermle uwf die ich komplett neu aufbaue. Angefangen habe ich vor ca 4 Jahre. Nun fehlt mir noch die Steuerung.
Die Videos vom Talla83 habe ich schon fast alle gesehen.
Meine Maschine hat:
3x Servomotoren
3x Heidehnhain Glasmastäb
1x Spindelmotor mit Fu
3x Achsklemmung
3x Soft Endschalter
3x Hardware Endschalter
Hydraulischer Werkzeugspanner
1x Zentralschmierung
Automatische Getriebeschaltung
Nun möchte ich die Mesa Karten Bestellen. 
Bitte sagt mir ob meine Recherche richtig ist. 
Bestellung: Mesa 7i76EU = hat sehr viele ein und Ausgänge für meine Schalter/Taster                   
                  Mesa 7I85 oder 7i85S ? bin mir nicht sicher welche ich nehmen sollte? für Heidenhain Glasmastäbe.

Danke, Gruß Gerald
  • DSS
10 Oct 2026 06:54 - 19 Oct 2026 23:05
I want to get my Taig mill up and running, listing some things for sale to help make it happen. 
  • Mesa 7i95T : New unused (only opened for photos)
  • Price SOLD

  • Geckodrive G540 : Used (was a bench test unit for me , never on a machine)
  • Price $160 + S&H

  • Geckodrive GR214V : [x3 units] New unused (only opened for photos)
  • Price $390 + S&H

  • EtherCAT AX58100 AX58100-EVB-1 Evaluation Board : Unused (only opened for photos)
  • Price $80 + S&H

  • Duet3D Duet 3 Mainboard 6XD V1.02 : Unused (only opened the box for photos)
  • Price $155 + S&H

    Any questions let me know, I tried to include manuals where applicable with the photos in case any additional product information is needed. I respond asap , Contact details and photos are here  desertshedstudio.com/listings/
  • sgd
10 Oct 2026 01:49
Replied by sgd on topic I think the forum needs some TLC
I don't mean to downplay your experience - I believe you. The forum has been slow for quite a while, but usually works eventually, It got a lot worse yesterday morning when the current attack began in earnest.
Things seem to be better now, but are not optimal or even acceptable.
We'll continue to work on keeping the forum running reliably.
Thanks!
  • snowgoer540
10 Oct 2026 01:05
Replied by snowgoer540 on topic I think the forum needs some TLC
For what it's worth, I've been trying to get a forum page to load from Wednesday morning until this evening.
  • concorde
10 Oct 2026 01:02
JMC Servo Drive Bricked! was created by concorde
Hi Guys, 
I'm new to the forum here. I have a milling machine with a JMC Servo motor (110JAS) driving the spindle. It has stopped working with an alarm AL-610 that started whilst I was loading/writing a new parameter to the servo drive via the JMC diagnostics software. As it was writing it triggered the alarm that caused the machine to e-stop. Powering back up even after leaving for 15minutes still produces the alarm. AL-610 is "encoder offline" fault. Despite that, I am confident the hardware is all fine and it is the parameters that have become corrupted. Does anyone know how to perform a factory reset? 
  • snowgoer540
10 Oct 2026 01:02
Replied by snowgoer540 on topic Usefull Open Source software, vibe coded in Rust
This is amazing, thank you for sharing!
  • FabLabRacing
09 Oct 2026 23:15
Replied by FabLabRacing on topic I think the forum needs some TLC
It is WAY better now, than it was this morning!!! A big thanks to all that worked on it!
  • tuxcnc
09 Oct 2026 19:53
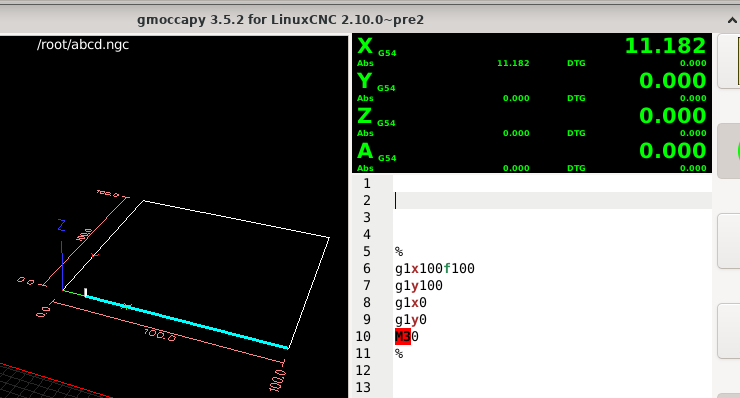
Since I understood absolutely nothing from the author's description of the thread, and the matter intrigued me, I decided to try to reproduce this error.

It looks like this:
 
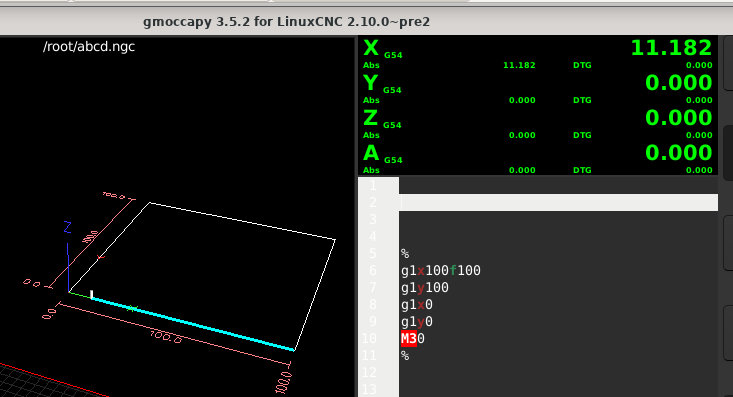
Here with the dark theme, which in my opinion is absolutely useless in practice, but shows better which line is highlighted:
 

To sum up.
The error only occurs when the percent sign is preceded by blank lines. (If any text precedes it, the program cannot be loaded.)
Then, if we select a path in the preview, the nth line of the file will be highlighted in the file window instead of the nth line of g-code.

Overall, the error is insignificant and occurs in very specific conditions, but this thread is proof that the user can become very confused... 
Displaying 346 - 360 out of 11915 results.
Time to create page: 0.283 seconds
Powered by Kunena Forum