
- Posts: 723
- Thank you received: 139
caxis.comp status
- smc.collins
- Offline
- Platinum Member
-

Less
More
2 years 9 months ago #290172
by smc.collins
Replied by smc.collins on topic caxis.comp - problems
subscribing, need to get this working on my lathe.
Please Log in or Create an account to join the conversation.
2 years 9 months ago #290174
by spumco
Replied by spumco on topic caxis.comp - problems
In case it helps here's the hardware i'm using:subscribing, need to get this working on my lathe.
- Drive
- Copley XSL
- Step & dir command
- Internally auto-tuned
- Motor
- 3kw BLDC converted to servo
- CUI encoder @4096ppr (16348 post-quad)
- ~1.389:1 poly-v belt drive to spindle
- Spindle encoder
- 600ppr (2400 post-quad)
- 1:1 on spindle via HTD-3M belt
The following user(s) said Thank You: smc.collins
Please Log in or Create an account to join the conversation.
2 years 9 months ago #290179
by spumco
Replied by spumco on topic caxis.comp - problems
I don't know if this will be useful, but I've got two halscope captures
First is running the spindle at 500rpm and stopping it. Capture is of the auto-repositioning move to C0 at M5.

Second is a back and forth G0 C0 to C90. No settings changed.
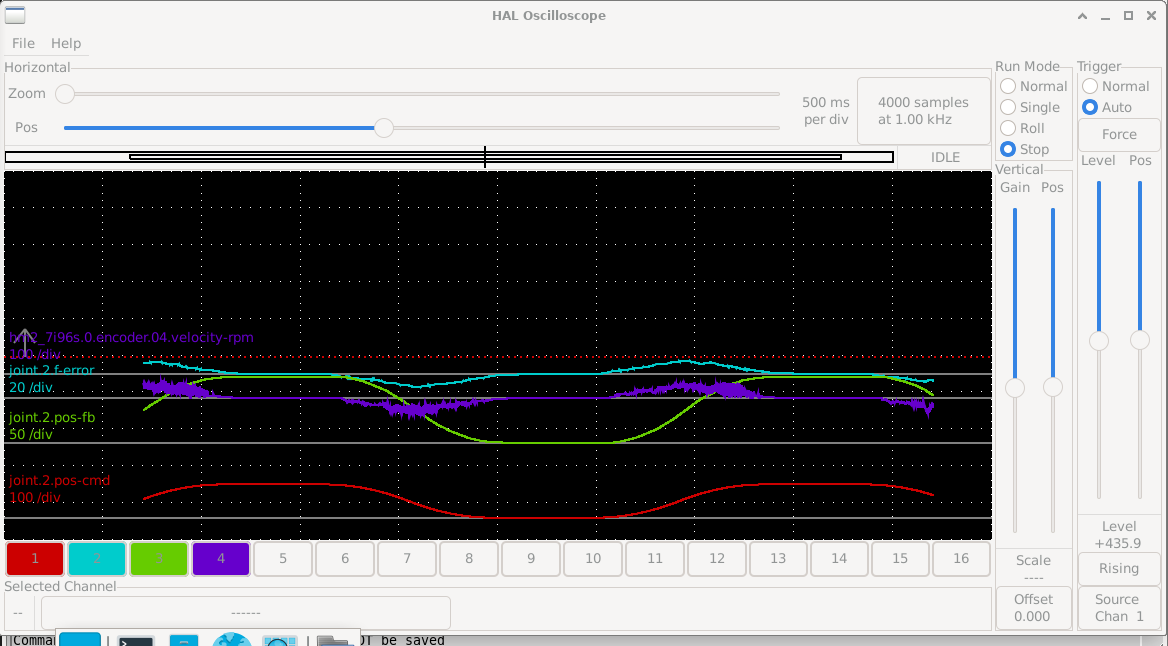
halscope is zoomed out on the second one, but that's the only difference.
No idea why the moves are so diferent.
First is running the spindle at 500rpm and stopping it. Capture is of the auto-repositioning move to C0 at M5.
Second is a back and forth G0 C0 to C90. No settings changed.
halscope is zoomed out on the second one, but that's the only difference.
No idea why the moves are so diferent.
Please Log in or Create an account to join the conversation.

2 years 9 months ago #290199
by Aciera
Replied by Aciera on topic caxis.comp - problems
Notice how pos-cmd in the first capture remains constant while it changes in the second.
I have no idea really but it looks like two different modes of the custom component, maybe?
I have no idea really but it looks like two different modes of the custom component, maybe?
The following user(s) said Thank You: spumco
Please Log in or Create an account to join the conversation.
2 years 9 months ago #290206
by spumco
Replied by spumco on topic caxis.comp - problems
I think that's a result of the conditions I needed to capture anything.
First case I started with spindle at C0, then did an M3 S500, then an M5. So the caxis component didn't change the position command - it was always C0. The duration of the move will always change as the M5 doesn't stop at a particular orientation.
Second case was a short C0-C9-C0 program, so the pos-cmd changed at each line.
What's bugging me is that the accel and velocity of the two moves are so different. And why I can't speed up (and smooth) the C-axis moves without getting really weird oscillation and crazy overshoot... yet the M5 move can be snappy and clean.
I'm wondering if the caxis.comp is using the spindle PID values for the automatic moves and regular c-axis moves are done using the c0.pid.
Or something along those lines.
First case I started with spindle at C0, then did an M3 S500, then an M5. So the caxis component didn't change the position command - it was always C0. The duration of the move will always change as the M5 doesn't stop at a particular orientation.
Second case was a short C0-C9-C0 program, so the pos-cmd changed at each line.
What's bugging me is that the accel and velocity of the two moves are so different. And why I can't speed up (and smooth) the C-axis moves without getting really weird oscillation and crazy overshoot... yet the M5 move can be snappy and clean.
I'm wondering if the caxis.comp is using the spindle PID values for the automatic moves and regular c-axis moves are done using the c0.pid.
Or something along those lines.
Please Log in or Create an account to join the conversation.
2 years 9 months ago #290257
by spumco
Replied by spumco on topic caxis.comp - problems
Bit of an update, and my dumb is showing itself again.
Turns out the motor encoder ppr was wrong. I thought I'd set it to 4096ppr (it's programmable), but I remembered when setting and tuning the servo drive it reported the motor as an 8-pole. Seems odd at the time, but I just ignored it and plowed on.
I got to thinking there was something wrong while fidding with this c-axis comp and decided to check everything from the basics.
Using the drive software to read the counts, it turns out the motor encoder is set to 2048 lines (8192ppr).
SO... after some re-tuning in the drive (now it's a 4-pole, joy) I've re-set my stepgen scale and things seem to be settling down a bit more. The c-axis moves are still pretty slow, but it's not doing the strange creep-way-past-target-and-reverse thing. G0 moves are smooth, as are the automatic return at M5. Both at the same speed (slow).
What's got me confused is that after the changes spindle mode RPM is about half what it should be.
Just in case somone wants to check my math...
So why is the spindle rotating at 270rpm when I command S500? And about 530rpm at 1000rpm commanded? Both speeds verified with photo tach just to be safe.
The step scale and encoder scale don't change between c-axis and spindle modes... so wth?
Turns out the motor encoder ppr was wrong. I thought I'd set it to 4096ppr (it's programmable), but I remembered when setting and tuning the servo drive it reported the motor as an 8-pole. Seems odd at the time, but I just ignored it and plowed on.
I got to thinking there was something wrong while fidding with this c-axis comp and decided to check everything from the basics.
Using the drive software to read the counts, it turns out the motor encoder is set to 2048 lines (8192ppr).
SO... after some re-tuning in the drive (now it's a 4-pole, joy) I've re-set my stepgen scale and things seem to be settling down a bit more. The c-axis moves are still pretty slow, but it's not doing the strange creep-way-past-target-and-reverse thing. G0 moves are smooth, as are the automatic return at M5. Both at the same speed (slow).
What's got me confused is that after the changes spindle mode RPM is about half what it should be.
Just in case somone wants to check my math...
- Motor encoder = 8192 counts/motor rev (verified via drive software)
- Spindle encoder = 2400 counts/spindle rev (verified using encoder count in LCNC)
- Motor encoder rotates 12110 counts per spindle rotation (turned by hand from 0-2400 spindle encoder counts in halshow)
- so belt drive is 1.478:1 (DIY poly-v, diameters were 'ish')
So why is the spindle rotating at 270rpm when I command S500? And about 530rpm at 1000rpm commanded? Both speeds verified with photo tach just to be safe.
The step scale and encoder scale don't change between c-axis and spindle modes... so wth?
Please Log in or Create an account to join the conversation.
Time to create page: 0.144 seconds