Retrofitting a 1986 Maho MH400E

More
7 years 5 months ago #134178 by RotarySMP
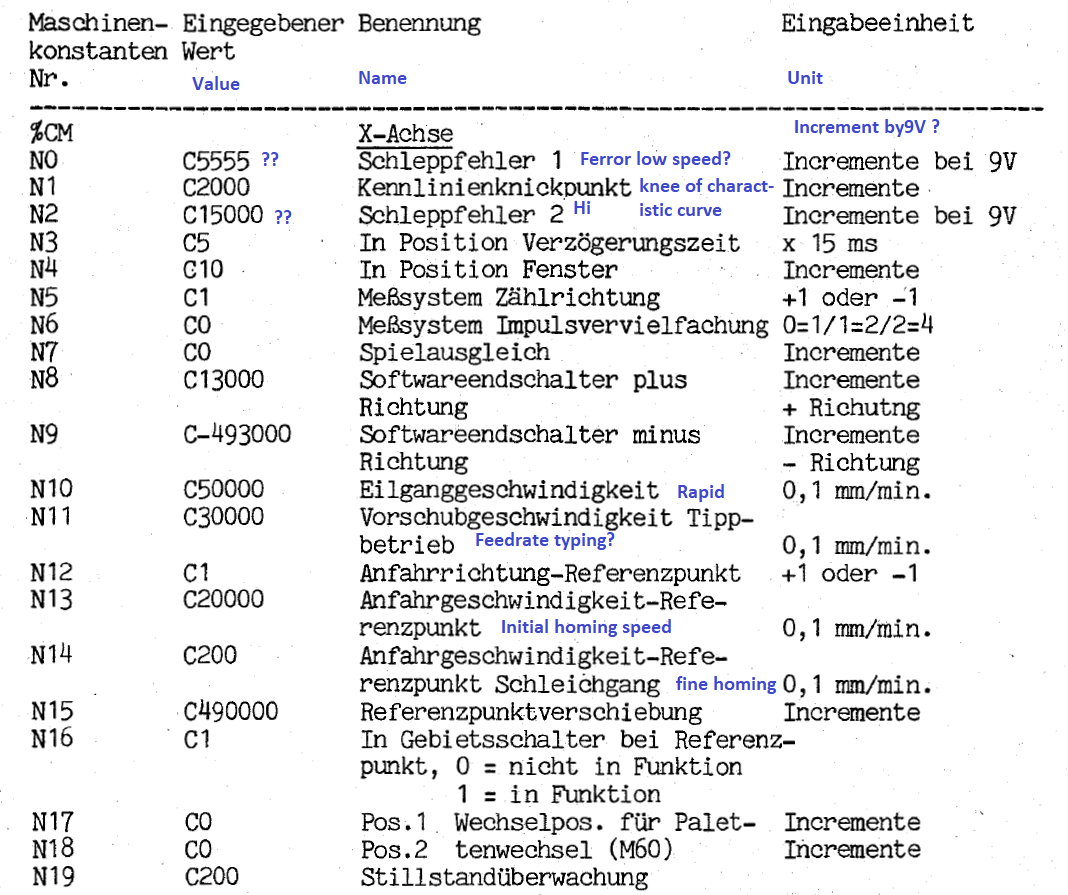
Your posting the machine constants reminded me that I have been saving everything MAHO related which I come across, and I found this 500C document...

It is the only document I have seen which actually provides some plan text description of the constants. Unfortunately we do not know what units these are, and therefore do not know the conversion to LinuxCNC Ini. In fact I don't even know if this is for a Phillips equipped machine.


Can we assume MAHO uses consistant Constant reference numbers across across models? Your 500E constants don't have an N0 as the 500C does.

Can we assume this?
No N1 = you have no low speed Ferror
N1 C3 = Linear characteristic curve (= same Ferror at all speeds)
N2 C72 = 72 [unit?] of Ferror

Please Log in or Create an account to join the conversation.

More
7 years 5 months ago #134179 by Glemigobles
Sadly, the same constant names set different parameters depending on the version of the controller. I checked that this morning with the manuals I downloaded. The Philips manuals not only tell you which do what, but also instruct system builders on how to set them up, find initial values and fine tune them. They did not correspond 1:1 to what is changed in LinuxCNC to achieve a tuned system, so you have to read the instructions first and see how they arrived at each value before you can come up with a "translation" to LCNC.

Please Log in or Create an account to join the conversation.

More
7 years 5 months ago #134180 by RotarySMP
Bummer. That would have been too easy. I was looking for such Phillips info when I find got the machine, before I gave up on repairing the 432. I have the constants for my machine, but only on punch hole tape.

Please Log in or Create an account to join the conversation.

More
7 years 5 months ago - 7 years 5 months ago #134181 by Glemigobles
All is not lost!

I'm a bit slow on the uptake, this manual I have seems to correspond with the constants you posted. They're from smoregrava as far as I can tell. Here it is on google drive:

drive.google.com/open?id=1IxHSQqD0w7Qd_oMKmUmk8gjWRuvD-lMd

Now we can compare the values with the instructions and arrive at the intended acceleration and following errors for that particular MH500C. Then we can see how that compares with our tuning efforts and maybe get closer to the designers' intentions.

Real stupid of me not to have downloaded the manual for my own version :laugh:

EDIT: also very ironic that the values we can check are for an MH500C, so neither the size nor the series matches our machines :)
Last edit: 7 years 5 months ago by Glemigobles.

Please Log in or Create an account to join the conversation.

More
7 years 5 months ago #134193 by Glemigobles
It seems to be the case that the first value is the following error that's allowed to happen so that a drive reaches it's maximum output voltage.

Instead of setting the gain, on the Philips you set the error and the gain was derived. Then there is a nod point, after which a second adjustment is made for lower voltage output.

All these values from the MH500C are orders of magnitude larger than what I have set.

Please Log in or Create an account to join the conversation.

More
7 years 5 months ago #134200 by Mike_Eitel
Hi RotarySMP
I own a tapmatic. You can exchange the shank. That way it will not get even longer than it is already.
Mike

Please Log in or Create an account to join the conversation.

Time to create page: 0.221 seconds
Powered by Kunena Forum