

Retrofitting a TOS FNG 32 NC

More
4 years 2 months ago #249051 by tommylight
Output scale can also be tuned in "calibration" menu, and settings saved without restarting LinuxCNC.

Please Log in or Create an account to join the conversation.

More
4 years 2 months ago #249078 by scotth
Replied by scotth on topic Retrofitting a TOS FNG 32 NC
I would put "EP1" relay in the spindle enable string to avoid this problem. Lack of field on spindle startup will draw max current and not start. Field loss at speed is even worse, it will get you a runaway condition. DC motors will throw windings at over speed.
The following user(s) said Thank You: Kevin_Pawlus

Please Log in or Create an account to join the conversation.
More
4 years 2 months ago #249105 by Kevin_Pawlus
I tried to cut some chips today. It works really good. 
Still some things to do of course like programing the buttons. Everything is plugged in and I can see that I get the signal when I push the button. 

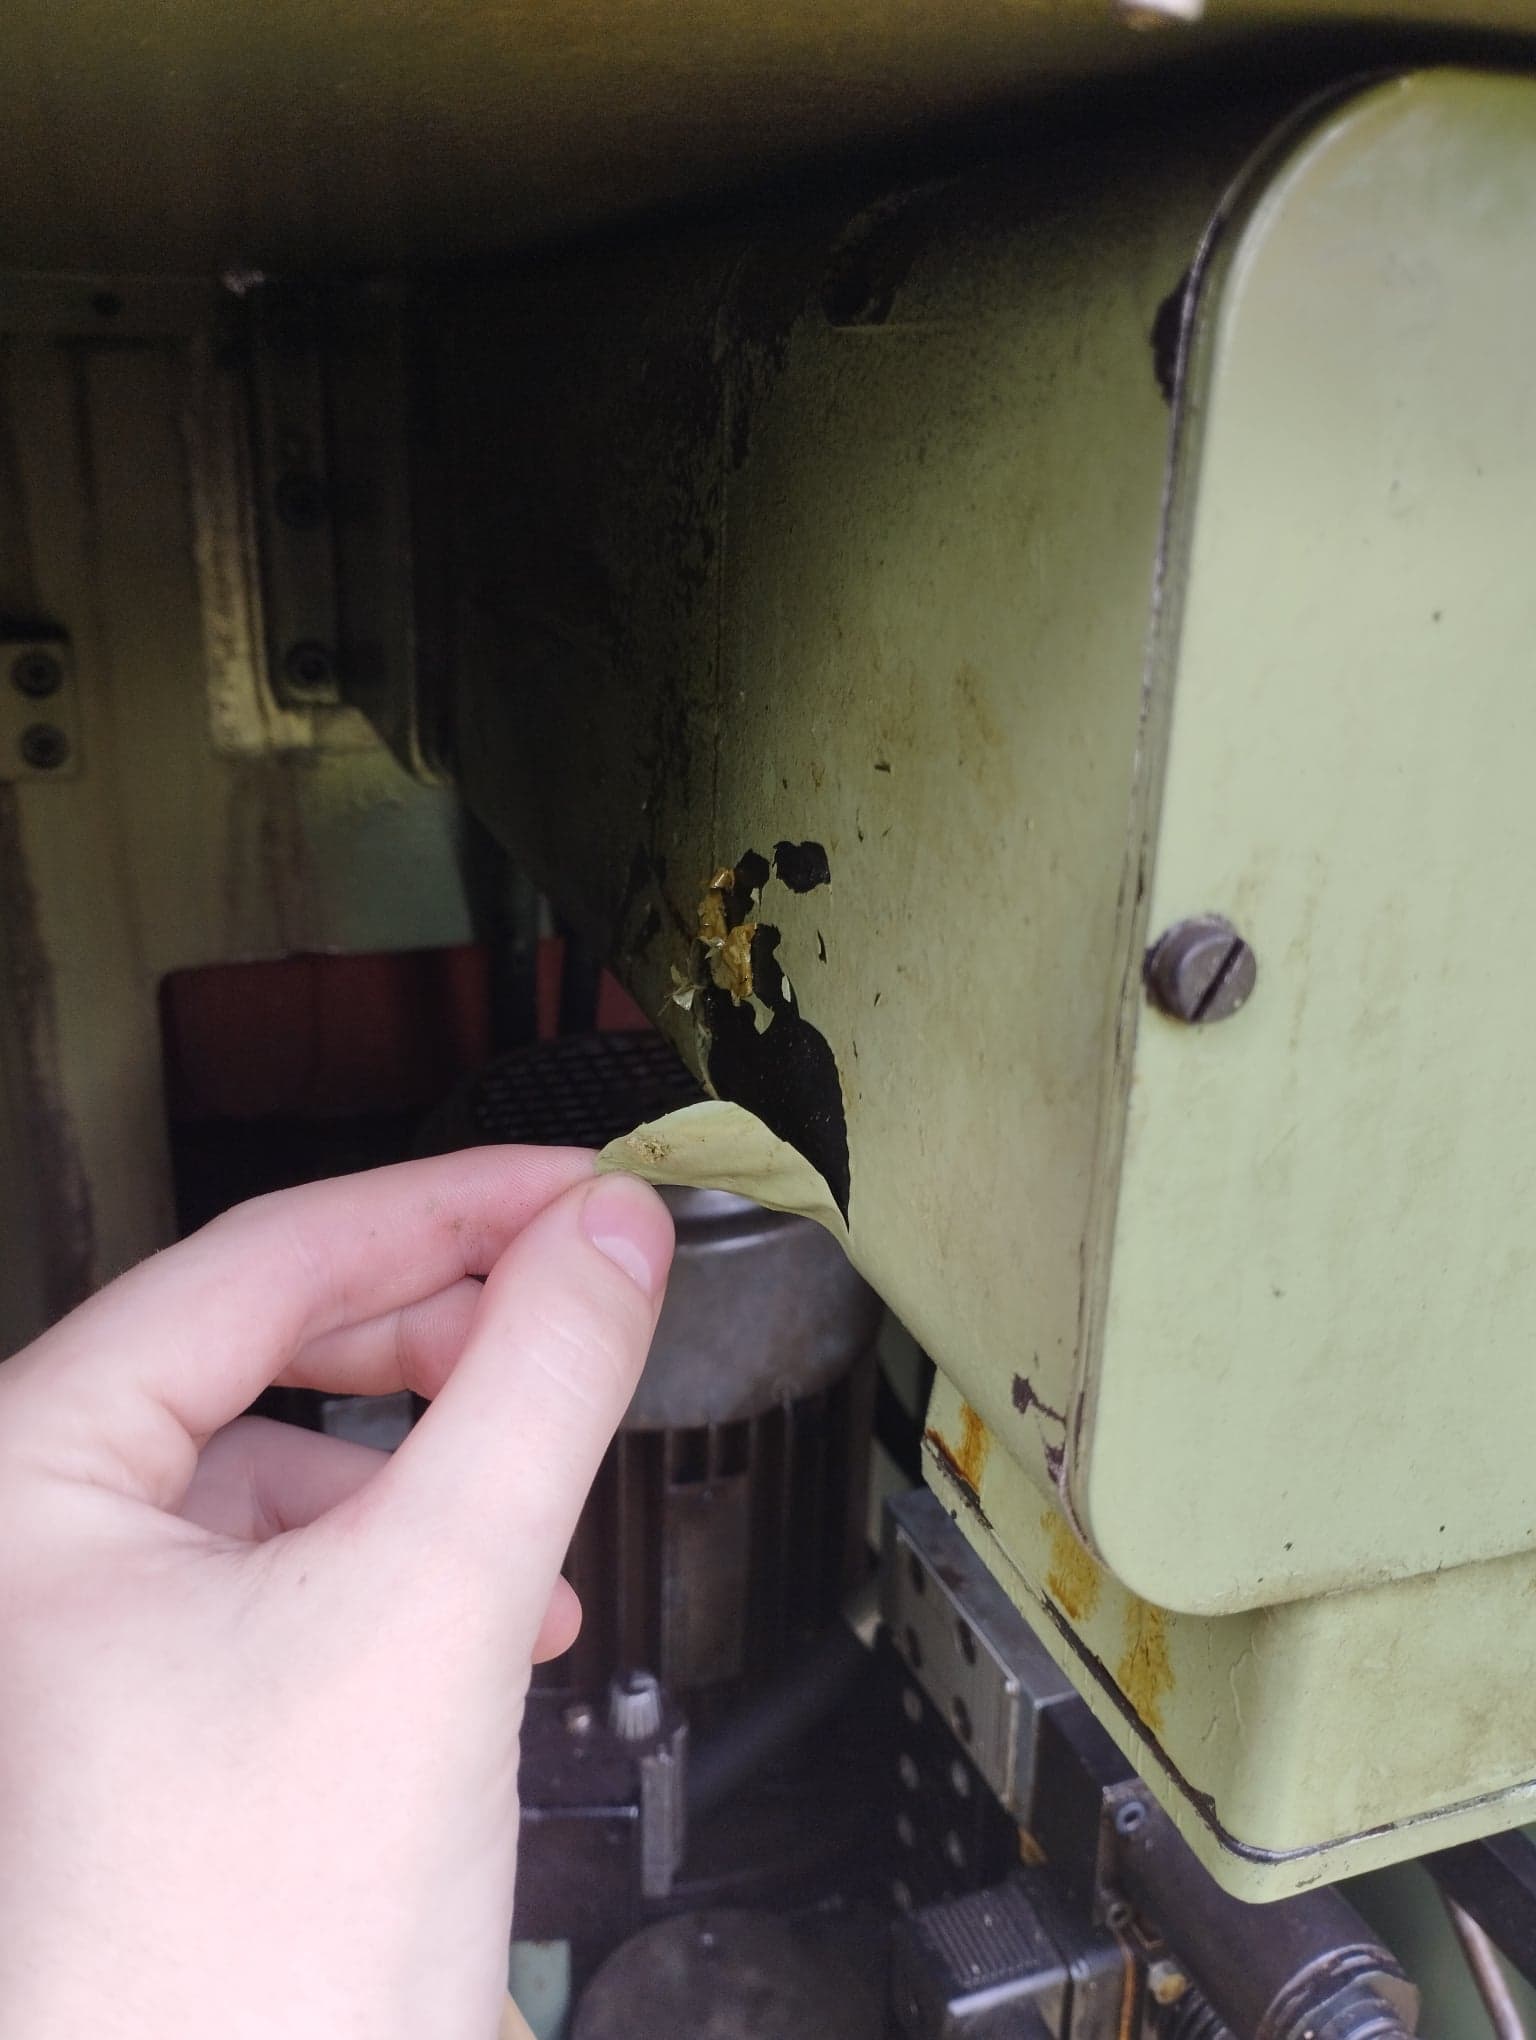
I did about 2 hours of milling and noticed that Y-motor is getting really hot. So hot that the paint is melting so that's something that needs to be fixed. There is some backlash in Y so you can hear the motor always going back and forth all the time, I don't know if this is the reason. X motor is also quite hot, I don't think its too hot though.  Z is only a bit warm. 


Please Log in or Create an account to join the conversation.

More
4 years 2 months ago #249164 by andypugh
If it was dithering inside the backlash it would be under no load, so probably wouldn't make much heat.

Can you move the axis with the motor unpowered? Try to feel if something is unusually stiff (thrust bearings are a likely culprit)
The following user(s) said Thank You: Kevin_Pawlus

Please Log in or Create an account to join the conversation.

More
4 years 2 months ago #249542 by Kevin_Pawlus
Hi,
I have been cutting some chips with this machine since last week, maybe 10-15 hours or so and now the servo drives won't start.
I have meassured that all enable signals is ok. Usually the first time I try to start it looks correct with the last digit on the DRO is flickering and I can hear a special humming sound from the drives that always have been there. But immediately when I try to jog the machine I will get Joint follow error. One time I could jog one axis 20cm, and when I tried the next one it was dead. 

After I have got the Joint follow error and I reset the machine I can't hear that humming sound that normally appears when the machine is enabled. 

The servo motors XY usually get quite hot so I only run the machine for 1 hour normally and let everything cool down. 

Spindle is fine.

/Kevin
 

Please Log in or Create an account to join the conversation.

More
4 years 2 months ago #249554 by tommylight

The servo motors XY usually get quite hot so I only run the machine f
 
Usually there are two reasons for the heat:
1.to much of P gain causing servos to constantly hunt back and forth
2.dust from the brushes inside the motor/commutator, if using brushed motors.

Please Log in or Create an account to join the conversation.

Time to create page: 0.439 seconds
Powered by Kunena Forum