
- Posts: 927
- Thank you received: 280
Remora - ethernet NVEM / EC300 / EC500 cnc board
- cakeslob
- Offline
- Platinum Member
-

Less
More
1 year 5 months ago #328335
by cakeslob
the gain thing was my mistake, they are both the same. remora outputs pwm, and if your hardware has a 0-10v, it will convert it to analog with the op-amp hardware circuit. digital signal might be referring to PWM
Replied by cakeslob on topic Remora - ethernet NVEM / EC300 / EC500 cnc board
Thanks Cakeslob, I forgot your using the stm32
the code in the hal file is the same for 0-10v and PWM ? Just the gain determines the difference?
In my VFD there is an option for 0-10v, 0-5v and external digital signal. Is it 0-5v or digital signal for PWM ?
@scotta , any ideas why it's doing this?
the gain thing was my mistake, they are both the same. remora outputs pwm, and if your hardware has a 0-10v, it will convert it to analog with the op-amp hardware circuit. digital signal might be referring to PWM
Please Log in or Create an account to join the conversation.
- Murphy
- Offline
- Elite Member
-

Less
More
- Posts: 163
- Thank you received: 5
1 year 5 months ago #328352
by Murphy
Replied by Murphy on topic Remora - ethernet NVEM / EC300 / EC500 cnc board
The more I think about this, It could very well be the PWM conversion onboard the EC500 is just to slow. It may not be able to keep up with the CSS speed adjustments. Any idea how to set the EC500 to output PWM instead and I'll hook up a PWM to Analog conversion board to test it. I know in the documentation you can switch it using Mach3 software.
Please Log in or Create an account to join the conversation.
- cakeslob
- Offline
- Platinum Member
-
Less
More
- Posts: 927
- Thank you received: 280
1 year 5 months ago #328407
by cakeslob
Replied by cakeslob on topic Remora - ethernet NVEM / EC300 / EC500 cnc board
It says theres a way to set it from analog to PWM in the manual, but the manual shows that its a software option, so Im not sure how thats supposed to even work...
Maybe it is an actual issue with the analog converter, I found a post from a few years ago about the older hardware
forum.linuxcnc.org/18-computer/44828-rem...ard?start=680#264265
Maybe @rbobey1989 has some insight, hes doing something with firmware and pwm nat the moment
Maybe it is an actual issue with the analog converter, I found a post from a few years ago about the older hardware
forum.linuxcnc.org/18-computer/44828-rem...ard?start=680#264265
Maybe @rbobey1989 has some insight, hes doing something with firmware and pwm nat the moment
Please Log in or Create an account to join the conversation.
- Murphy
- Offline
- Elite Member
-
Less
More
- Posts: 163
- Thank you received: 5
1 year 5 months ago #328418
by Murphy
Replied by Murphy on topic Remora - ethernet NVEM / EC300 / EC500 cnc board
That's interesting Cakeslob, this makes sense if it's to slow to react it would be like cutting the signal which it seems to be doing. There's something about changing it to PWM in Mach3 software and it uses a different pin.
If I can get the PWM signal direct and use an external PWM to Analog converter might work.
If I can get the PWM signal direct and use an external PWM to Analog converter might work.
Please Log in or Create an account to join the conversation.
- DarkPhoinix
- Offline
- Premium Member
-

Less
More
- Posts: 107
- Thank you received: 6
1 year 5 months ago - 1 year 5 months ago #328473
by DarkPhoinix
Replied by DarkPhoinix on topic Remora - ethernet NVEM / EC300 / EC500 cnc board
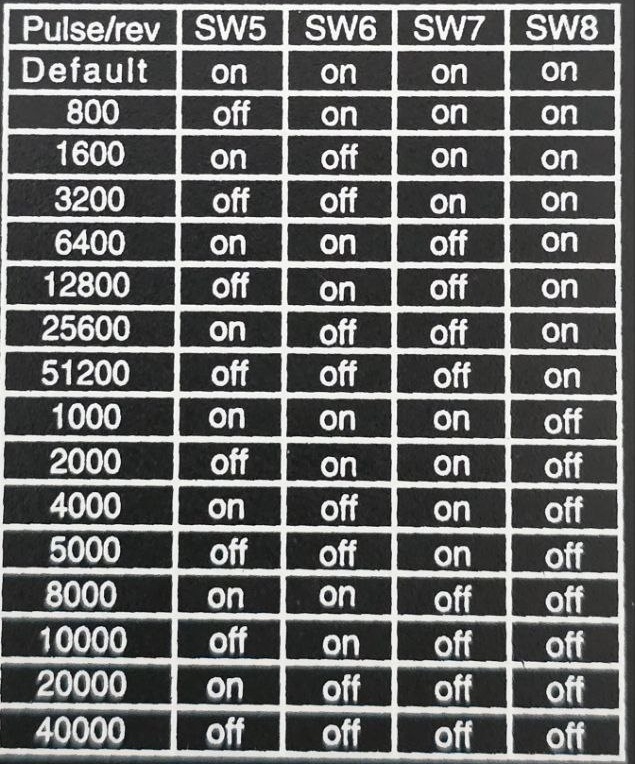
Which pulse/rev is best for NVEM RT1052?
Last edit: 1 year 5 months ago by DarkPhoinix.
Please Log in or Create an account to join the conversation.
- Spyderbreath
- Offline
- Senior Member
-

Less
More
- Posts: 47
- Thank you received: 9
1 year 5 months ago #328488
by Spyderbreath
Replied by Spyderbreath on topic Remora - ethernet NVEM / EC300 / EC500 cnc board
At the risk of the blind leading the blind, to me that is not quite the right question. That chart is for your micro-stepping. Like the 800 is 4 microsteps, if you're using a 1.8 deg. stepper. I have always looked at it this way - What are you doing with the motor? If your opening a door or driving a ram, picking 800 would be fine, but using that on a belt or lead screw may very well end up leaving artifacts in the work due to the rougher movement between points. The downside is the more micro-steps you have the more torque you lose. 3200 (16 micro-steps) seams to be a reasonable middle ground that most use as standard. The controller will put out as many steps as directed by LinuxCNC to make a revolution, just a matter of how fast it can do it.
Whatever you chose, that gets figured out when you tell LinuxCNC in your .ini file how many pulses it takes to move one unit. That is set with the SCALE on each axis. Like for me, I have 16 micro-steps (3200) and a 5mm pitch screw, which works out to SCALE = 640 or -640 depending which way you need the motor to move.
Whatever you chose, that gets figured out when you tell LinuxCNC in your .ini file how many pulses it takes to move one unit. That is set with the SCALE on each axis. Like for me, I have 16 micro-steps (3200) and a 5mm pitch screw, which works out to SCALE = 640 or -640 depending which way you need the motor to move.
The following user(s) said Thank You: DarkPhoinix
Please Log in or Create an account to join the conversation.
Time to create page: 1.070 seconds