
- Posts: 972
- Thank you received: 167

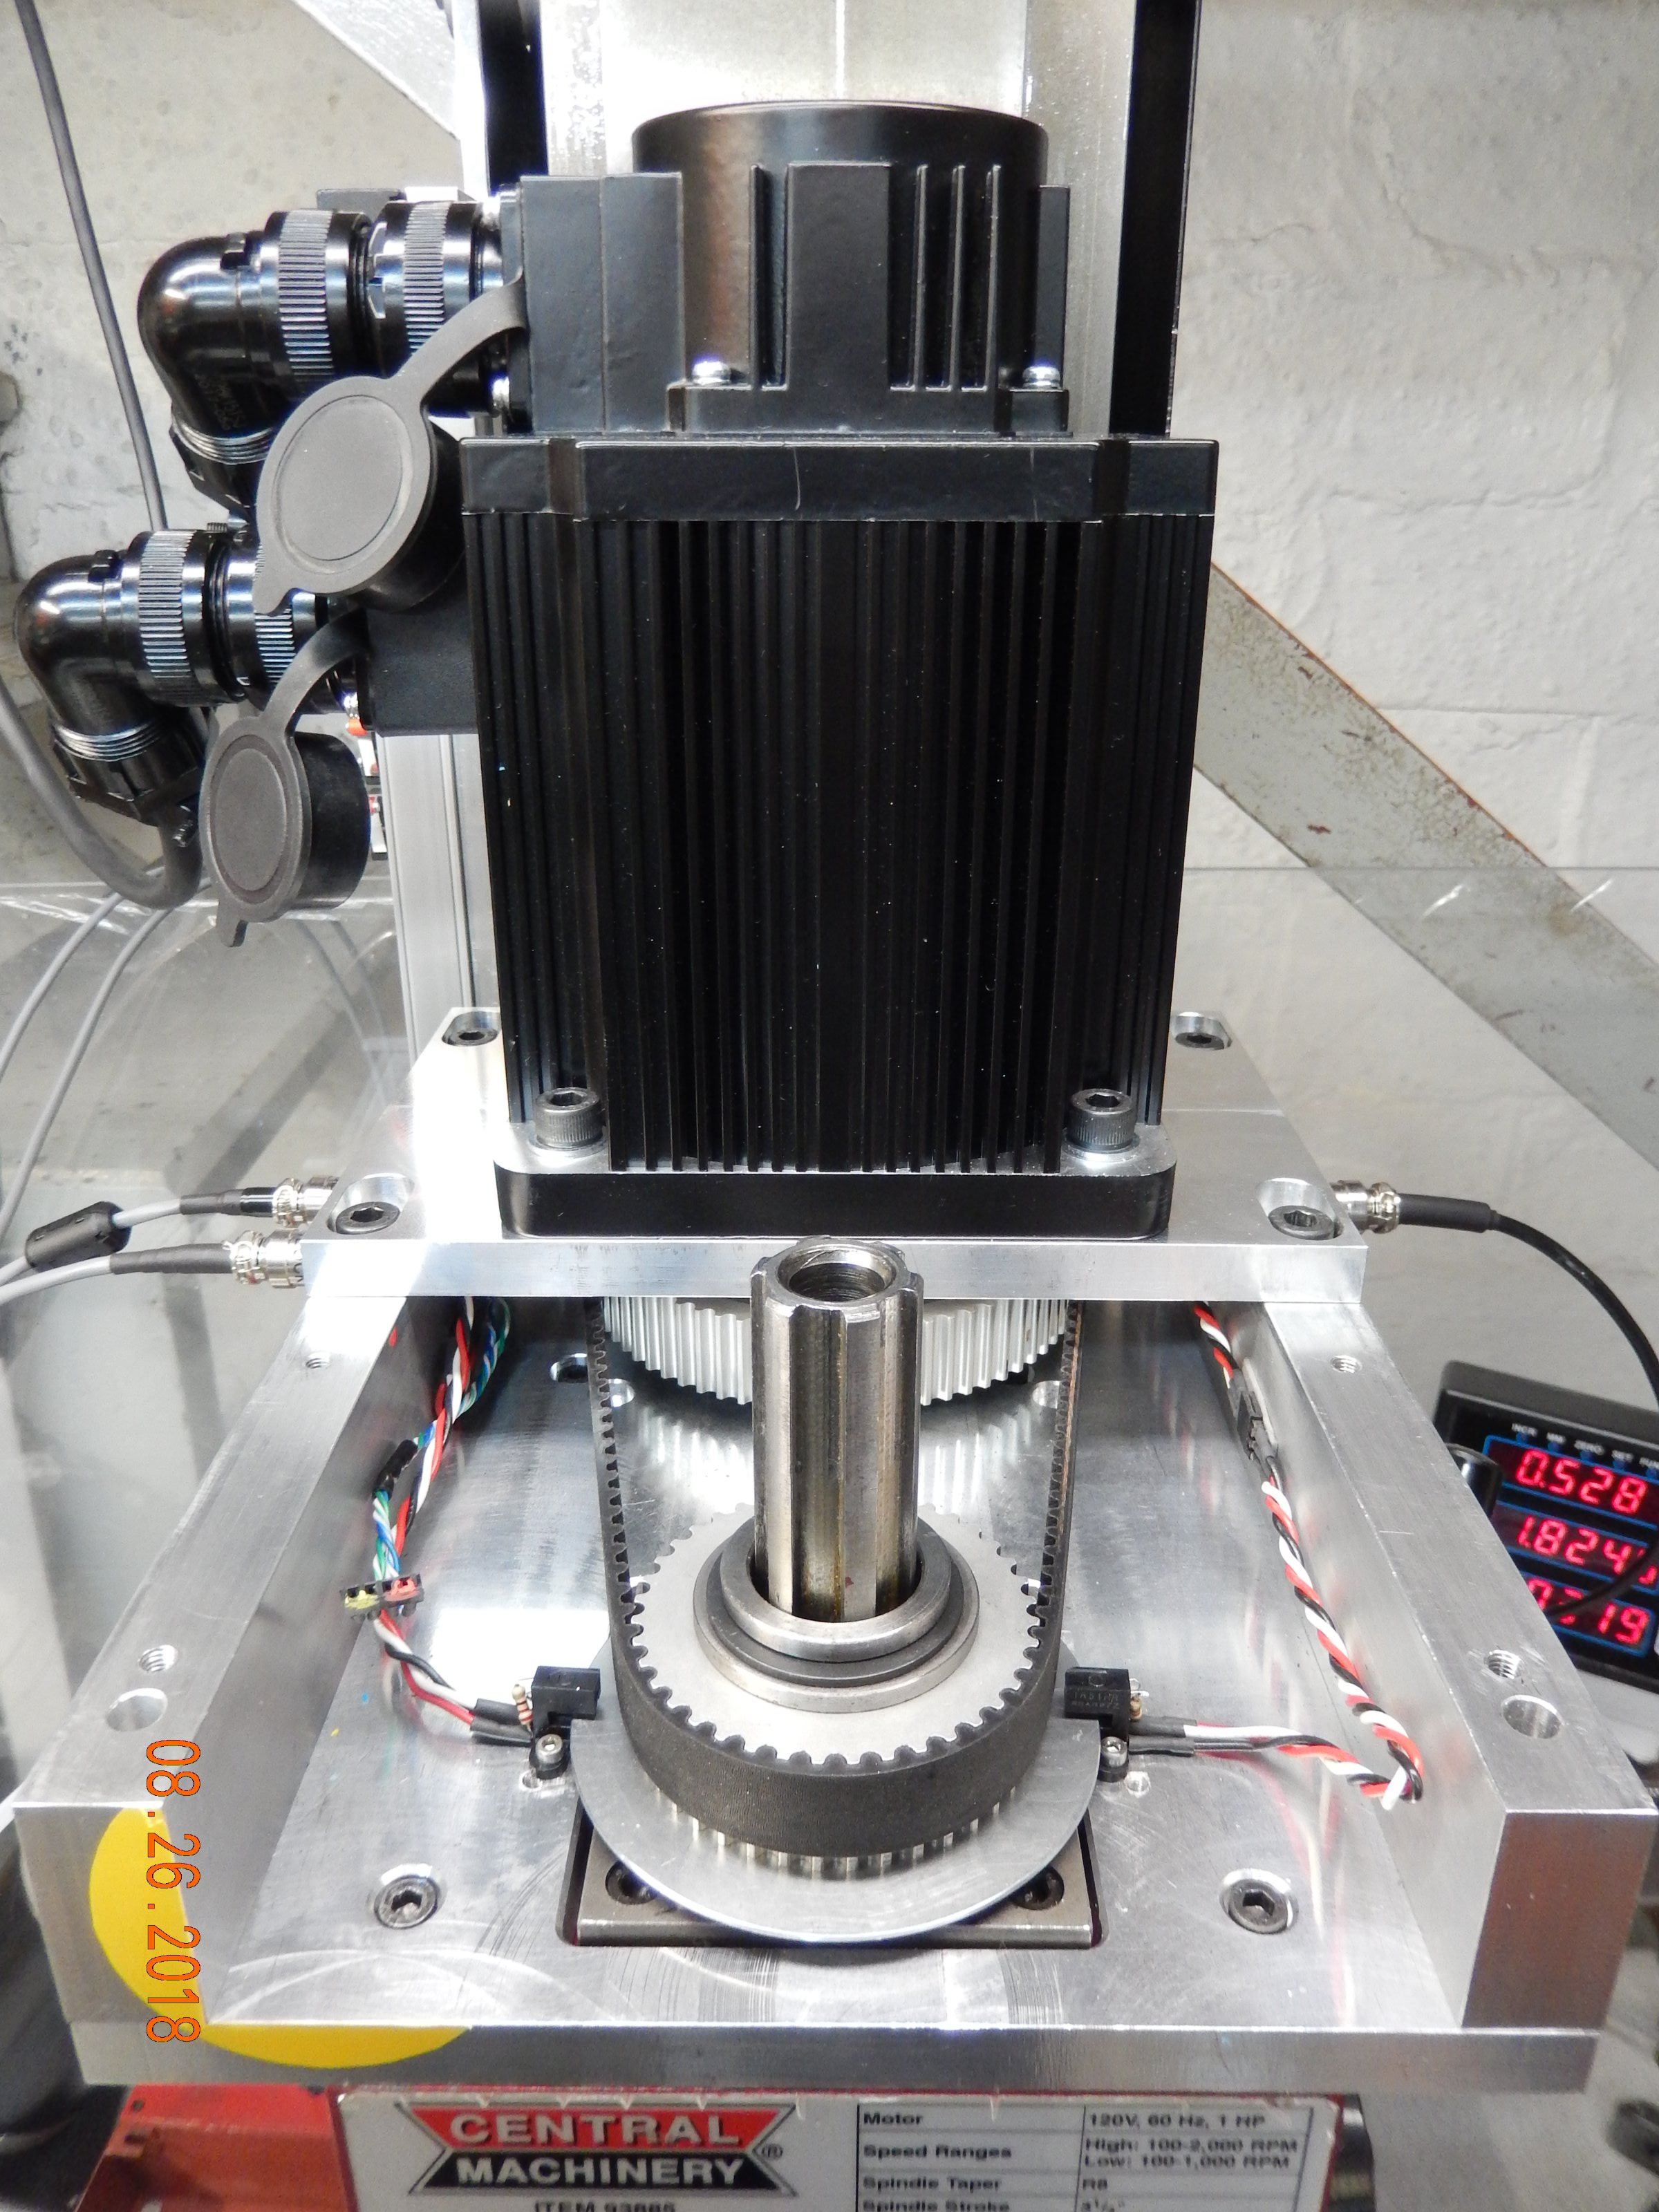
JohnnyCNC wrote: You could make that work. If it is geared 1:1 you can use the A/B/Z signals right from the encoder. On my mill I used the A/B signals that my spindle servo motor drive outputs and added a separate index signal to the spindle. This is because the spindle motor is geared 1:1.8. You will actually see two pickups for the index signal/ This is because the second one drives the a DRO that I also have on the mill.
Please Log in or Create an account to join the conversation.
Is that a 1kw motor? What kind of speed do you get out of that setup? I went with the 750w because it was the largest 5k rpm motor DMM had, figured I'd stick with the 2 step belt setup to get good torque upto 2500rpms and still be able to run upto 5k in high range. I really can't complain at all with this setup for this size mill, I haven't stalled the spindle yet.
Please Log in or Create an account to join the conversation.
Please Log in or Create an account to join the conversation.
Please Log in or Create an account to join the conversation.
PCW wrote: Typically spindle at speed is driven by a "near" component
so has a settable tolerance (say +-10%)
Displayed speed will always have some variation, this variation is made worse
by the fact that is the calculated speed from the last millisecond. The flicker in the displayed speed is normally fixed by filtering it with the low pass filter
which averages the noise to give a more stable display

Please Log in or Create an account to join the conversation.
Please Log in or Create an account to join the conversation.

