
- Posts: 33
- Thank you received: 4
[ Vfdmod ] An easy VFD control over MODBUS RTU
- SkyMoCo
- Offline
- Junior Member
-

Less
More
3 years 8 months ago #265289
by SkyMoCo
Replied by SkyMoCo on topic [ Vfdmod ] An easy VFD control over MODBUS RTU
Mine are all set to 5.00 so it has to be something else.
Register Setting
1 2
2 2
3 400
4 400
5 400
6 10
7 .5
8 110
9 15
10 5
11 20
12 1
13 0
14 10
15 10
16 5
17 5
18 5
19 5
20 5
21 5
Register Setting
1 2
2 2
3 400
4 400
5 400
6 10
7 .5
8 110
9 15
10 5
11 20
12 1
13 0
14 10
15 10
16 5
17 5
18 5
19 5
20 5
21 5
Please Log in or Create an account to join the conversation.
- RobC
- Offline
- Junior Member
-
Less
More
- Posts: 26
- Thank you received: 5
3 years 8 months ago #265336
by RobC
Replied by RobC on topic [ Vfdmod ] An easy VFD control over MODBUS RTU
It's setting 7 - change this from .5 to 50. I was just testing some different settings and this is the one that made the actual difference.
There are a few other settings we have different. 14 and 15 make a noticeable difference in accel and decel times / speed, others are not really noticed at all.
6 - 15
9 - 40
11 - 50
14 - 5
15 - 5
There are a few other settings we have different. 14 and 15 make a noticeable difference in accel and decel times / speed, others are not really noticed at all.
6 - 15
9 - 40
11 - 50
14 - 5
15 - 5
Please Log in or Create an account to join the conversation.
- SkyMoCo
- Offline
- Junior Member
-
Less
More
- Posts: 33
- Thank you received: 4
3 years 8 months ago #265337
by SkyMoCo
Replied by SkyMoCo on topic [ Vfdmod ] An easy VFD control over MODBUS RTU
I changed them all to match yours and still have the issue. Maybe I am not describing it well. When I bring up the Axis gui, and press on the spindle forward icon, it goes to 3996 and will not go any faster. Is this a linuxcnc setting or still something on my VFD?
I do appreciate your help, when I get this working I'll document all my settings and upload it.
I do appreciate your help, when I get this working I'll document all my settings and upload it.

Please Log in or Create an account to join the conversation.
- RobC
- Offline
- Junior Member
-
Less
More
- Posts: 26
- Thank you received: 5
3 years 8 months ago #265347
by RobC
Replied by RobC on topic [ Vfdmod ] An easy VFD control over MODBUS RTU
The screenshot shows some of the different vfdmod settings / syntax that we have, along with the different rpm in / out / spindle-at-speed values. To get your 3996 rpm out and 401 rpm in, did you click the spindle + button in axis, or do an MDI command? Try to doing M3 S6000 and see what those values say then.
Then the attached file shows all of your spindle related settings, with my spindle related settings below (with the // in front). These are spread over different files but I have pasted all into one so it's easier to see. Your main ini and vfdmod ini files seem to be fine, so I am thinking the problem lies in these vfdmod net settings.
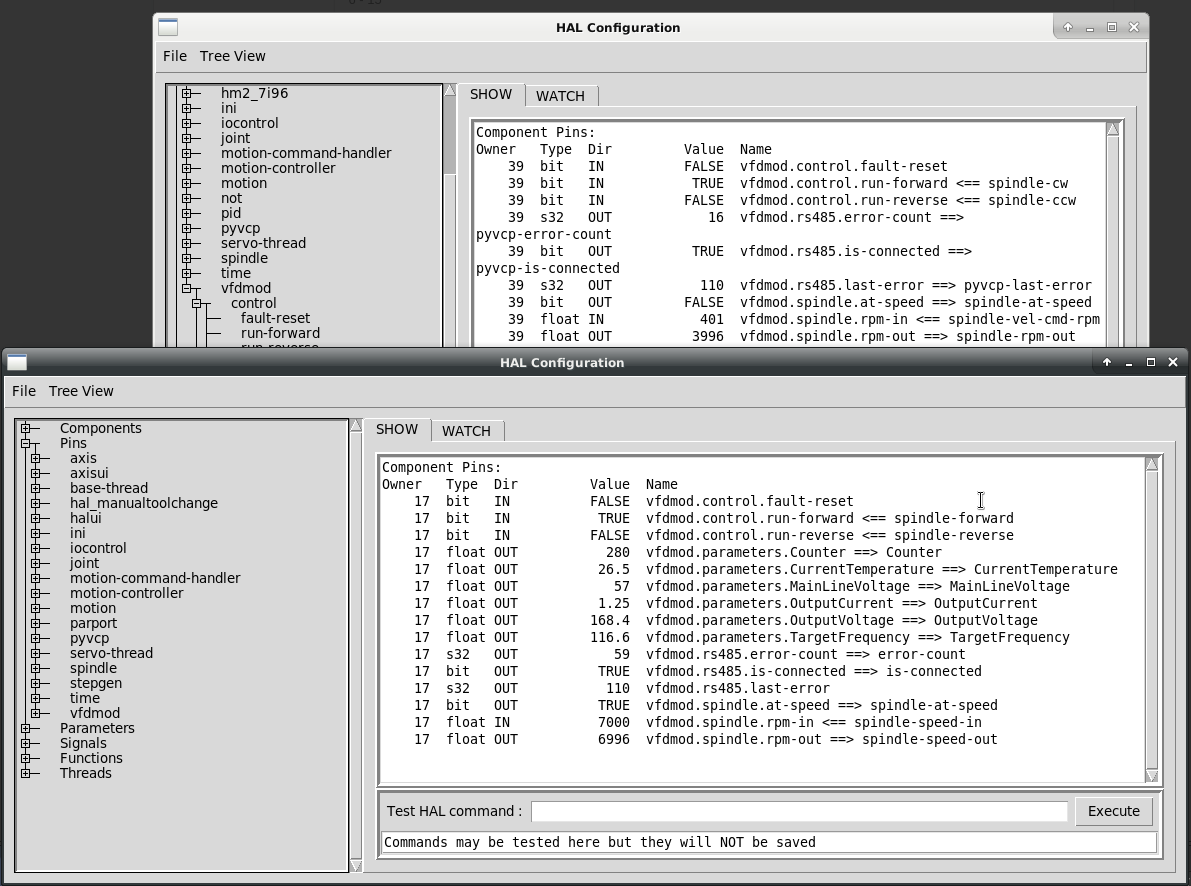
Then the attached file shows all of your spindle related settings, with my spindle related settings below (with the // in front). These are spread over different files but I have pasted all into one so it's easier to see. Your main ini and vfdmod ini files seem to be fine, so I am thinking the problem lies in these vfdmod net settings.
Please Log in or Create an account to join the conversation.
- SkyMoCo
- Offline
- Junior Member
-
Less
More
- Posts: 33
- Thank you received: 4
3 years 8 months ago #265352
by SkyMoCo
Replied by SkyMoCo on topic [ Vfdmod ] An easy VFD control over MODBUS RTU
I was doing a S6000 and F9. When I do a M3 S6000 (or whatever speed) it works!!! I guess I just assumed that F9 did the same as a M3.
Are our net settings different due to different linuxcnc versions? I'm at 2.8 but I could upgrade to 2.9.
I do get an 100 error now and then, should I adjust the baud rate or protocol delay?
vfdmod: setting control word value to 0 (0x0000)...
[0ERROR Connection timed out: select
1][06][02][00][00][00][88][72]
Waiting for a confirmation...
<01><06><02><00><00><00><88><72>
Please Log in or Create an account to join the conversation.
- RobC
- Offline
- Junior Member
-
Less
More
- Posts: 26
- Thank you received: 5
3 years 8 months ago #265359
by RobC
Replied by RobC on topic [ Vfdmod ] An easy VFD control over MODBUS RTU
My linuxcnc version is 2.8.4 and is sort of stalled out since I run a parport / rtai combo. The mesa configurations are quite a bit different than what I have, so I would suspect its just that.
As far as errors go, I get a number of errors just as a matter of course. As long as the vfd responds and the spindle does what it's supposed to, I don't worry about it.
As far as errors go, I get a number of errors just as a matter of course. As long as the vfd responds and the spindle does what it's supposed to, I don't worry about it.
Please Log in or Create an account to join the conversation.
Time to create page: 0.139 seconds