Considering a Full Rewire on a Working Schaublin 125 CNC

More
6 months 1 week ago - 6 months 1 week ago #345833 by Dudelbert
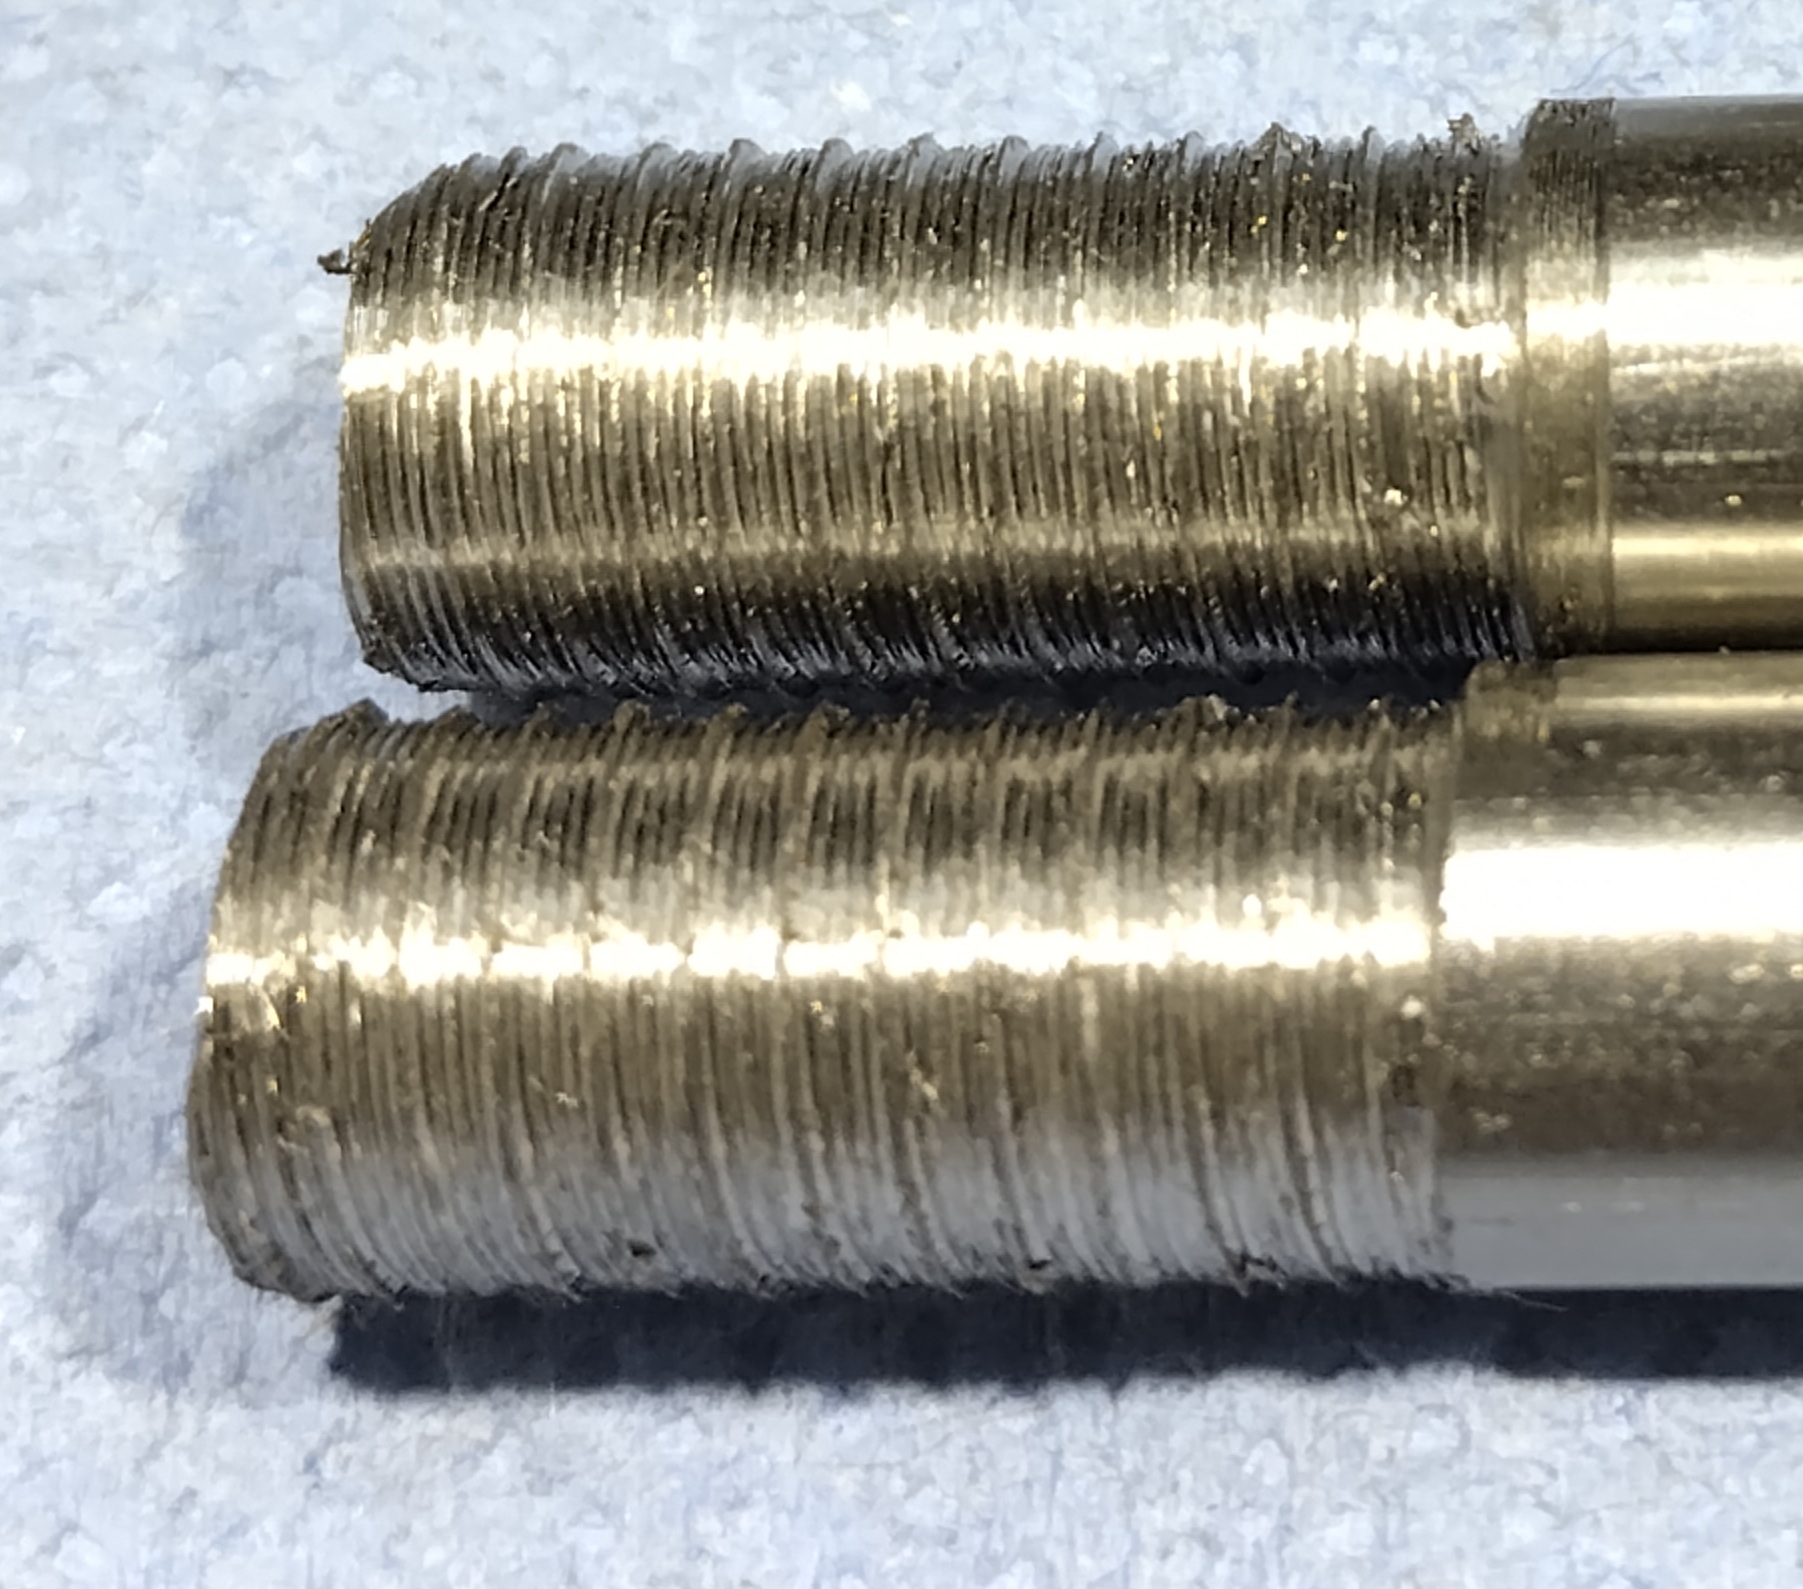
I am still struggling with threading.I have tested it at very low speed (100 RPM) in the hope to see something that helps me find what is wrong. But I cannot really say what I am looking at. The result is repeatable, and at least to me it looks like a constant offset that makes it wrong. I have set the cross-slide angle to 0, so that is not the reason. It is supposed to be an M8.

I would have expected a more random result if the spindle index was jittery, so that is probably not it. And spindle.0.revs, I tested it by turning the spindle by hand 25 turns, and spindle.0.revs was almost exactly 25. The remaining very small error can easily be attributed to me doing it by hand.
Additionally, I set the spindle to 1200 RPM and let it run. After it settled, I made a video filming the HAL Show screen and watching spindle.0.revs so I could later check it, and I got 1206 RPM that way.
I tried to make sure that the spindle really had 1200 RPM with a laser tachometer and by watching the encoder velocity RPM. Both agree within a margin of under 10 RPM. I don’t have any RPM measurement tools that are more reliable or accurate.

All these tests point me in the direction of the spindle encoder being OK. Are these tests the wrong way of testing this? What else can it be?
Last edit: 6 months 1 week ago by Dudelbert.

Please Log in or Create an account to join the conversation.
More
6 months 1 week ago #345835 by rodw
These are cheap as (can find them for half this price) and are well worth having
www.amazon.com.au/Mengshen-Tachometer-2-...ctive/dp/B0BFHXMKR3/
The following user(s) said Thank You: Dudelbert

Please Log in or Create an account to join the conversation.
More
6 months 1 week ago #345836 by Dudelbert
That is the exact type of “laser tachometer” I used. I agree that they are useful.

Please Log in or Create an account to join the conversation.
More
6 months 1 week ago #345841 by RotarySMP
I double checked our ini's, and we both have the encoder scaling set to 8000 pulses/rev. Not sure what would cause that drift you are seeing.
The following user(s) said Thank You: Dudelbert

Please Log in or Create an account to join the conversation.
More
6 months 1 week ago - 6 months 1 week ago #345855 by spumco

I am still struggling with threading.I have tested it at very low speed (100 RPM) in the hope to see something that helps me find what is wrong. But I cannot really say what I am looking at. The result is repeatable, and at least to me it looks like a constant offset that makes it wrong. I have set the cross-slide angle to 0, so that is not the reason. It is supposed to be an M8.


All these tests point me in the direction of the spindle encoder being OK. Are these tests the wrong way of testing this? What else can it be?

 
Take the below with a grain of salt, of course.

Spindle speed:  there is a bug in LCNC which causes a different start point during spindle synchronized motion if successive passes aren't at the same speed.  Constant surface speed is not OK in multi-pass threading.  Same reason folks have reported trying to do thread repair and lining up on a thread by hand, only to wipe out the threads when the spindle is run because the start point is different.

I don't think this was your problem, as I did a screen-cap of your video looking for the start point on each pass.  Pretty constant start point near as I can tell.

It looks like your thread is cutting mostly on the left (leading) side, which would correlate with the Q value you have set.  But it doesn't appear to be going much deeper each pass.

Like you cut one pass deep, then scrape the left side each successive pass without really going much deeper.  The chips look terrible... instead of a 'wire' each pass, you have scrapings.


Maybe run another attempt, but change the Q, E, and L values to 0 (straight in),  make sure I/J/K are diameter values, an R-value of 2.0, and ensure you have the spindle in G97.

This might help troubleshooting by taking out a few variables which may be obscuring machine issues.

EDIT - I jut re-watched the video and it's cutting the RIGHT side, not the left.  Like the "Q" value is backwards or something. The tool is moving at the same pitch each pass, but it's offset to the right slightly each successive pass.  Weird.
Last edit: 6 months 1 week ago by spumco. Reason: Dur-hur
The following user(s) said Thank You: tommylight, Dudelbert

Please Log in or Create an account to join the conversation.

More
6 months 1 week ago #345864 by spumco
Had another peek at the vid on a bigger screen, and each pass is certainly starting to the right of the previous pass.

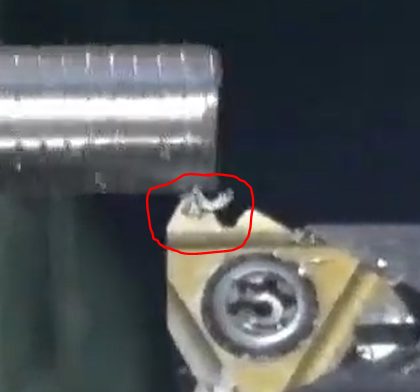
Start of pass 2, chip is forming on the right of the insert:
 

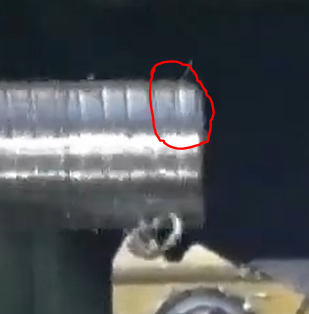
Two rotations later, and you can see a second groove forming to the right of the first pass... but it isn't much deeper.
 

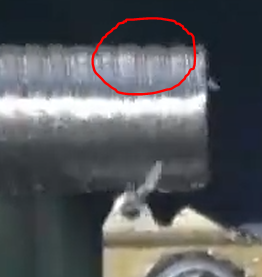
Third pass, and now there's a 3rd groove  - also to the right.  And also isn't much deeper.  Maybe deflection, but I didn't see the stock wobbling a ton or climbing the insert.  Almost like it isn't going any deeper each pass, just shifting to the right.
 

In addition to running a no-Q value test, it might be helpful to set up a halscope with the Z-axis position and the spindle index signal.  Try to see exactly where the Z-axis is when the index signal is triggered, and does the Z-axis then start moving immediately?

My earlier suspicion about the start point being the same may not be accurate - hard to spot 0.1mm-0.2mm shift of the insert on video.

Finally, you could put an ink pen in the tool holder and run a series of 3 to 4 G33 moves, using the pen to draw a thread.  Since "The G76 canned cycle is based on the G33 Spindle Synchronized Motion", multiple G33 passes should help you determine if the synchronization start point is exactly the same place without any other motion distractions.

Try it at different spindle speeds - but use the same speed for each set of repetitions.  If you want to test my claims about the bug, run a 4-pass test, but increase the spindle speed by 100-200rpm each pass.

If the start point is the same every time during G33 (same spindle speed) - but not during G76 - you've got a threading-specific problem.
If it's not the same, you've got a more fundamental synchronization problem... mechanical or LCNC configuration.  Or you may be encountering the bug I mentioned earlier from a different direction.
The following user(s) said Thank You: RotarySMP, Dudelbert

Please Log in or Create an account to join the conversation.

Time to create page: 0.186 seconds
Powered by Kunena Forum
