Light Machine Corp. Benchman XTr (retrofit)

More
9 years 10 months ago #84411 by TGTROPIC
24,
Looks like the exact same board.
I have one component missing from C14 that is present on your board.
Would you be willing to part with this board? :)
TG

Please Log in or Create an account to join the conversation.
More
9 years 10 months ago - 9 years 10 months ago #84441 by steve_a
Mac,
I went with the Kflop/Kannaolg because of the Mesa supply problem. I gave up waiting for them to be able to send me a card. At the time I think they were in the middle of supplying someone with a commercial application so my order was constantly being bumped.
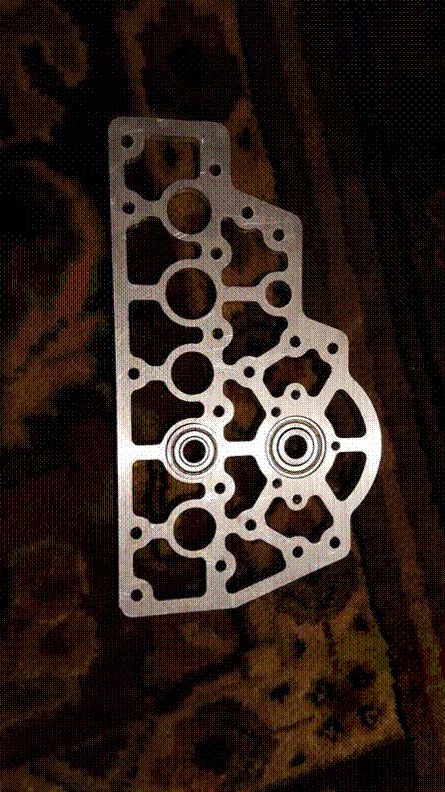
I have everything but the tool changer working. I made this part using a .25", 2 flute end mill, running at about 2500 RPM and 4 IPM. It takes about 2 hours for all the operations but I'm really happy with the accuracy. The bearings are press fit and that was what I was after. However, the numbers say I should be able to run about 4000 RPM at 12 IPM... The piece complains a lot and running it over 11 IPM I experience a spindle shut down that I believe is something in the Ultra 100. I used the application you shared and finally was able to talk to the unit! Now I just have to learn what it all means.
Last edit: 9 years 10 months ago by steve_a.

Please Log in or Create an account to join the conversation.

More
9 years 10 months ago #84444 by steve_a
OOOPS! Forgot to mention... the cut depth per pass, .0625".... Should be able to do twice that according to the numbers.... must be for Bridgeport sized machines.

Please Log in or Create an account to join the conversation.

More
9 years 10 months ago #84483 by Azik1
Does any one know good method to tram head along X/Y axis ? Seems like it has just 4 bolts holding spindle no adjustments visible.
Thanks!

Please Log in or Create an account to join the conversation.

More
9 years 10 months ago #84612 by TGTROPIC
Steve,
Contacted Intelitek re:recent findings. Below is that correspondence.
TG

MSG>>>I have gotten some help with trouble shooting have we have made the following observations;
The Copley controls are not getting power and there is no power getting to the J9 plug.

Is there a chance that the K4 relay has gone bad that switches the high voltage AC to the transformer?
If so, how difficult is that relay to swap out of the board?

REPLY>>>The copley controls are enabled by the software. It's unlikely that K4 is the culprit. Are yoi still getting the ENC S error?

REPLY TO REPLY>>>Yes on the error…so the Copley controls are not energized until directed by the software?
So the software is prohibiting the Copley’s from getting power until the error is cleared?

Final Reply>>>Correct, please see the schematic I send you and make sure the encoder circuit is working on your machine.

Please Log in or Create an account to join the conversation.

More
9 years 10 months ago #84622 by tommylight
You should also check the entire e-stop loop, as a single defect will not allow the power to the drives. Had that problem, but i do check that as the first thing on a machine, so i do not waste time chasing the tail. Some machines have a key switch for overiding the e-stop loop.

Please Log in or Create an account to join the conversation.

Time to create page: 0.277 seconds
Powered by Kunena Forum
