

1982 Matsuura MC-500v Retrofit

More
9 years 8 months ago #88590 by tommylight
Those look like car cam shaft pulleys, they do not look like they have the same number of teeth, if you plan on rigid tapping, they must be 1 to 1 ratio.
Try to find a dual cam shaft engine, they have 2 of the same.
Regards,
Tom

Please Log in or Create an account to join the conversation.
More
9 years 8 months ago - 9 years 8 months ago #88591 by chopper79
Yes they are cam shaft pulleys and I am only using one of them. Not sure which one if either would work fine.

Edit: If one of these does not do what I want then I will machine my own pulley and add as many teeth and mounting options as a I can. I wish I could make it from aluminum as then I have a 72 tooth pulley blank that I could use. Since the tooth sensors are magnetic...well, you get the idea.
Last edit: 9 years 8 months ago by chopper79.

Please Log in or Create an account to join the conversation.

More
9 years 8 months ago #88592 by andypugh

chopper79 wrote: I suppose the 42 tooth one would work fine as well. I mean its better then what is one there which is a single hall for indexing.


Lathe-threading works OK with a single pulse per rev.

Rigid-tapping on a mill needs more teeth to know at what point the spindle has reversed.
So, with a 42 tooth wheel you have 168 pulses per rev.
Tapping a 1/4" x 20 thread you have a pitch error of 1 / (20 * 168) inches. That's .0003". That would probably be lost in the spindle bearing end-float.

Please Log in or Create an account to join the conversation.

More
9 years 8 months ago - 9 years 8 months ago #88594 by chopper79
Hmm.... I use all metric threads. Might be an issue then if a 1/4-20 has that much error correct?

Thread sizes from M3 up to M6

May need to look into a higher count pulley to increase my ppr. Unless the 42 tooth would be fine when doing metric threads?
Last edit: 9 years 8 months ago by chopper79.

Please Log in or Create an account to join the conversation.

More
9 years 8 months ago - 9 years 8 months ago #88595 by chopper79
Doing some thinking on this.....

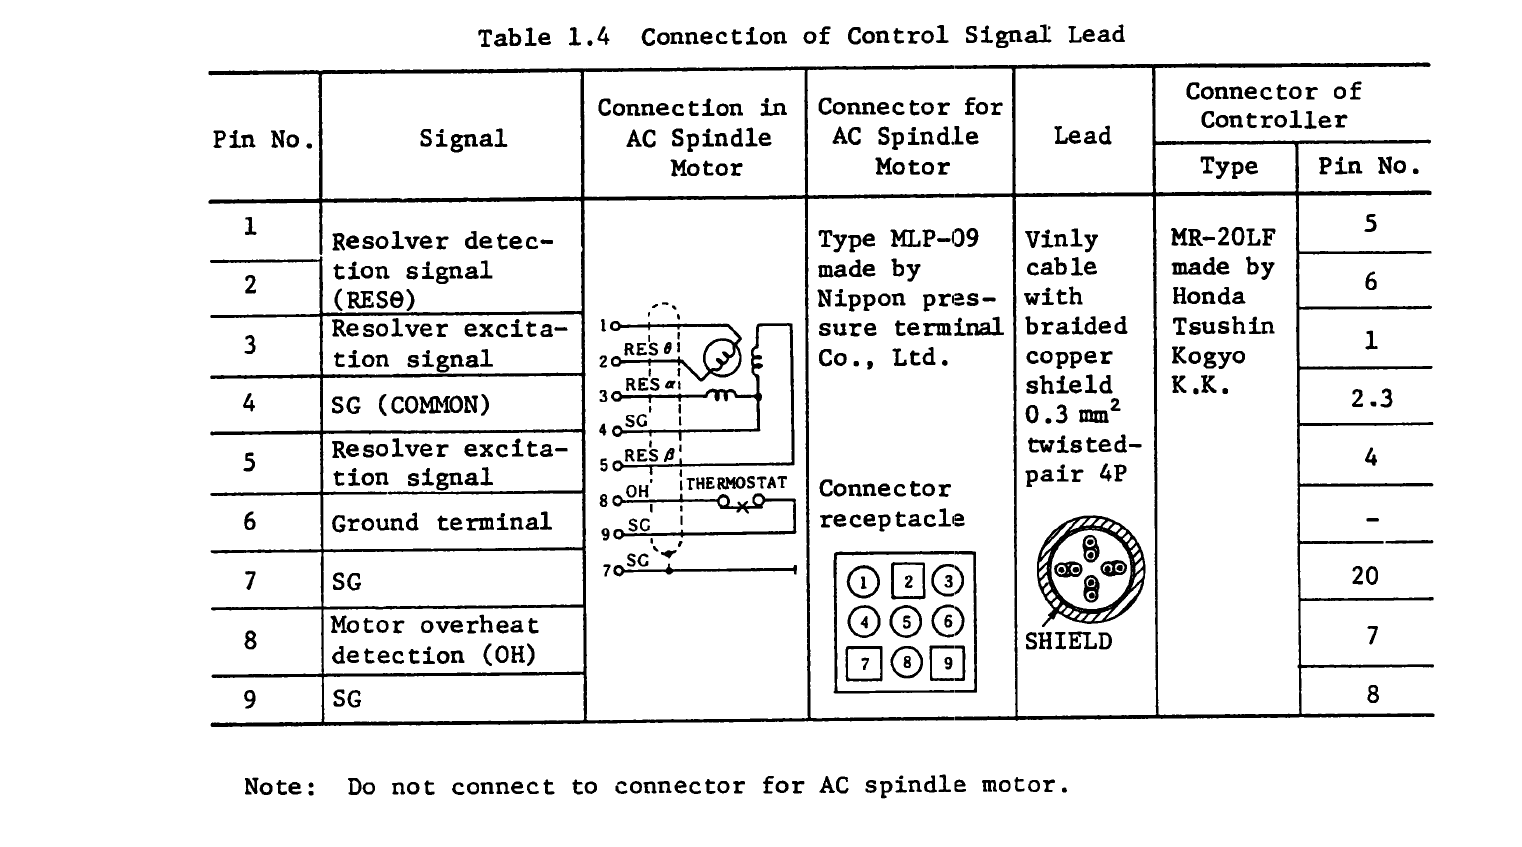
The machine tapped using a g84 from the factory. This means there had to be some sort of feedback from the spindle to the controller. Started looking at the manual for the spindle motor and there is something in there but not sure if this would be able to be used?

Might have to hook a meter up to these and see..

Last edit: 9 years 8 months ago by chopper79.

Please Log in or Create an account to join the conversation.

More
9 years 8 months ago #88597 by andypugh
Oh, you have a resolver!

What feedback do the axis motors use? It seems odd to have a spindle resolver and axis encoders?

My machines use Resolvers on both axes and spindles (I like them) but I chose my Mesa cards based around the 7i49, which I don't think is a comfortable fit to your system.

You should be able to use the resolver to quadrature converter from Pico, though.
The following user(s) said Thank You: chopper79

Please Log in or Create an account to join the conversation.

Time to create page: 0.107 seconds
Powered by Kunena Forum