Hurco BMC 30 AP
- Aciera
-
- Offline
- Administrator
-

Less
More
- Posts: 4818
- Thank you received: 2176
11 Jul 2026 12:13 #347680
by Aciera
Replied by Aciera on topic Hurco BMC 30 AP
Try this:
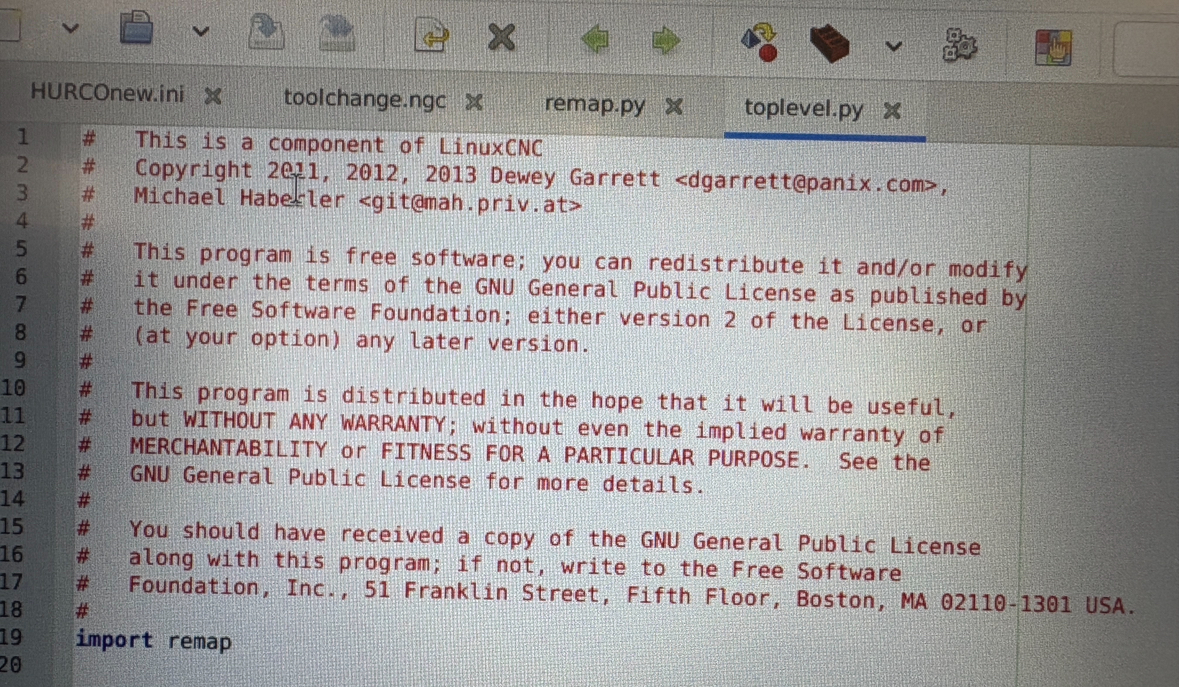
1. in your config folder create a new folder named 'python' and put the two attached files 'remap.py' and 'toplevel.py' into this new folder
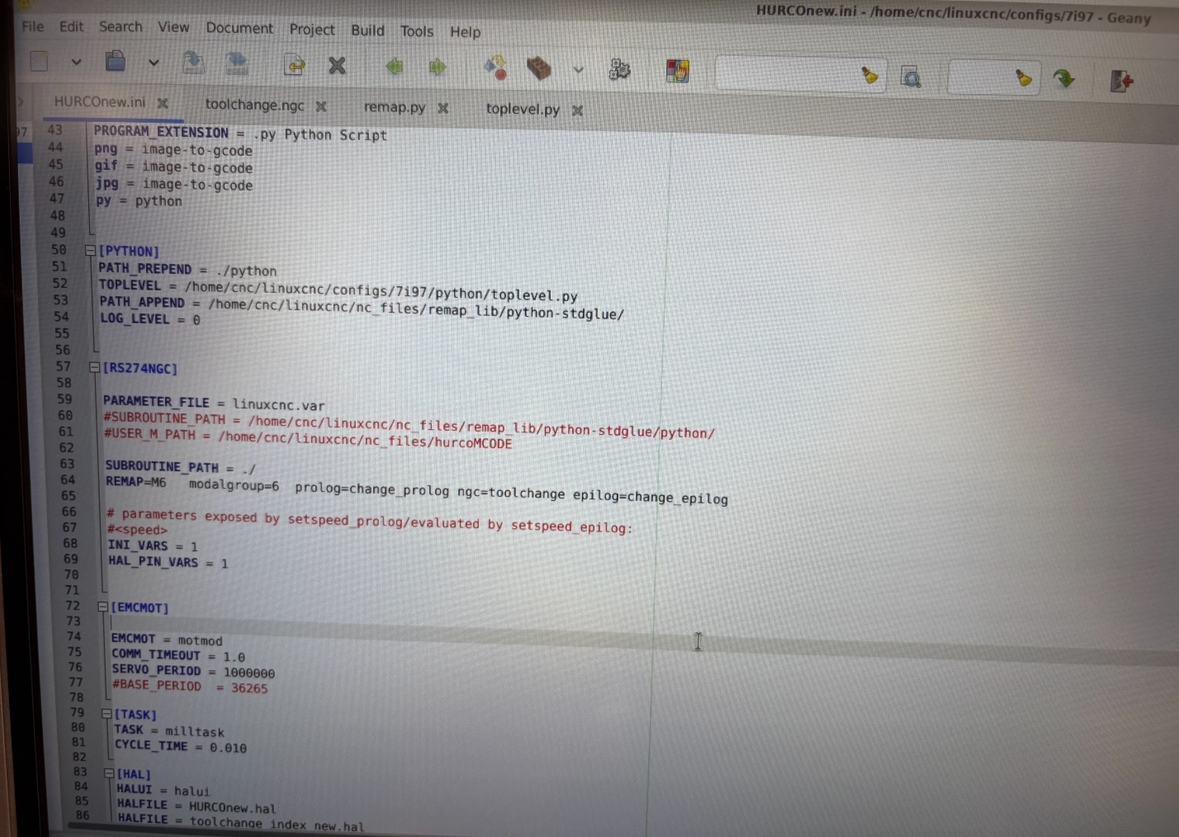
2. replace the entries in your [PYTHON] section of your ini file with this:
1. in your config folder create a new folder named 'python' and put the two attached files 'remap.py' and 'toplevel.py' into this new folder
2. replace the entries in your [PYTHON] section of your ini file with this:
PATH_PREPEND= ./python
PATH_APPEND= /home/cnc/linuxcnc/nc_files/remap_lib/python-stdglue
TOPLEVEL= ./python/toplevel.py
LOG_LEVEL = 0 Please Log in or Create an account to join the conversation.
- 5_Zylinder
- Offline
- Senior Member
-

Less
More
- Posts: 63
- Thank you received: 3
20 Jul 2026 21:42 #347893
by 5_Zylinder
Replied by 5_Zylinder on topic Hurco BMC 30 AP
We tried your suggestion, and the error message "G-Code error in axis.ngc" is now gone.
I did, however, forget to add the "TOP_LEVEL = 0" command. I'll add that now.
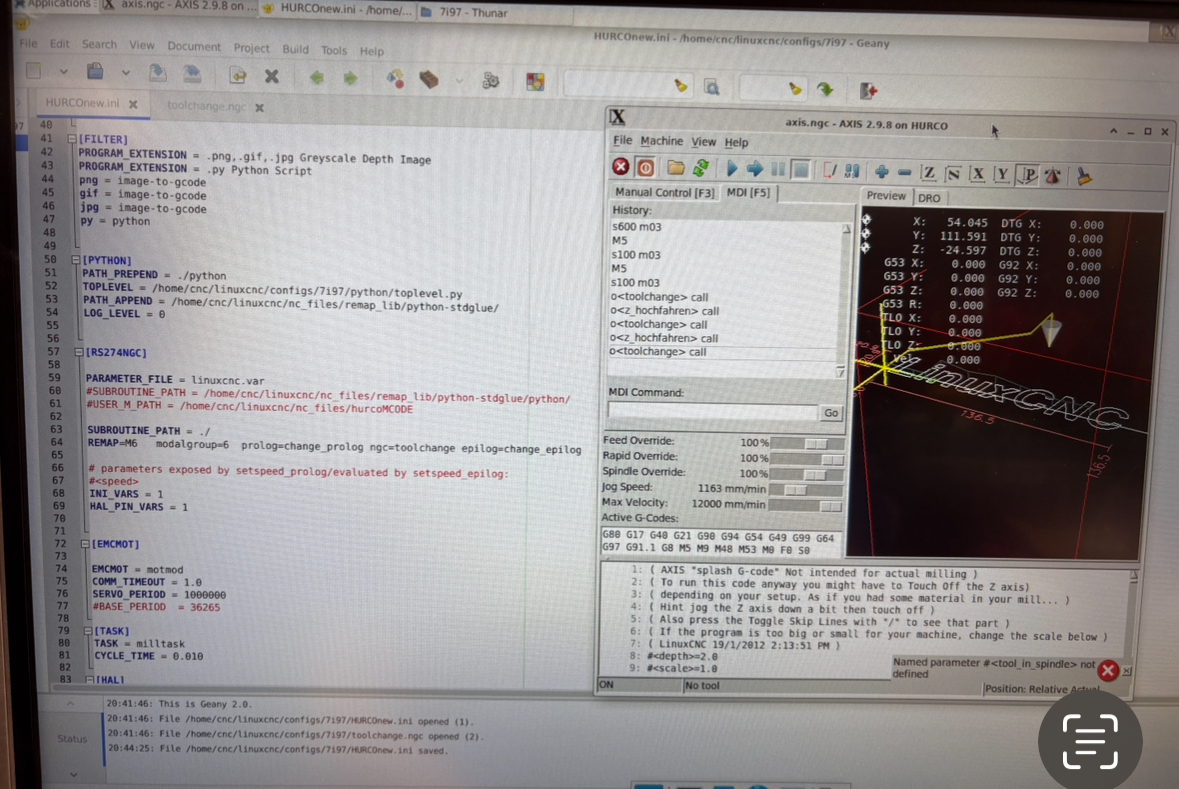
I wanted to execute the command "o<toolchange> call" in MDI mode. However, I received an error message referencing the tool change program sequence: "Named parameter #<tool_in_spindle> not defined." It seems to me that this parameter hasn't been declared yet, so the system can't locate it.
Perhaps you have a solution for this problem.
Please Log in or Create an account to join the conversation.
- tommylight
-
- Offline
- Moderator
-

Less
More
- Posts: 21957
- Thank you received: 7478
20 Jul 2026 23:39 #347895
by tommylight
Replied by tommylight on topic Hurco BMC 30 AP
That was not mentioned anywhere, so why?
I did, however, forget to add the "TOP_LEVEL = 0" command. I'll add that now.
PATH_PREPEND= ./python
PATH_APPEND= /home/cnc/linuxcnc/nc_files/remap_lib/python-stdglue
TOPLEVEL= ./python/toplevel.py
LOG_LEVEL = 0
Please Log in or Create an account to join the conversation.
- 5_Zylinder
- Offline
- Senior Member
-
Less
More
- Posts: 63
- Thank you received: 3
21 Jul 2026 03:42 #347901
by 5_Zylinder
Replied by 5_Zylinder on topic Hurco BMC 30 AP
Ah, sorry, it was late. Of course, I mean "LOG_LEVEL = 0".
The following user(s) said Thank You: tommylight
Please Log in or Create an account to join the conversation.
- tommylight
-
- Offline
- Moderator
-
Less
More
- Posts: 21957
- Thank you received: 7478
21 Jul 2026 04:07 #347903
by tommylight
Replied by tommylight on topic Hurco BMC 30 AP
No worries, just trying to prevent you wasting time and wondering "why it does not work" if you make the same typo where it actually matters.
Please Log in or Create an account to join the conversation.
- 5_Zylinder
- Offline
- Senior Member
-
Less
More
- Posts: 63
- Thank you received: 3
21 Jul 2026 19:35 #347930
by 5_Zylinder
Replied by 5_Zylinder on topic Hurco BMC 30 AP
Thanks for the help.I’ve now implemented everything just as Aciera described. The error persists. I think a directory is still missing here?
Please Log in or Create an account to join the conversation.
- Aciera
-
- Offline
- Administrator
-
Less
More
- Posts: 4818
- Thank you received: 2176
22 Jul 2026 07:19 - 22 Jul 2026 07:22 #347951
by Aciera
Replied by Aciera on topic Hurco BMC 30 AP
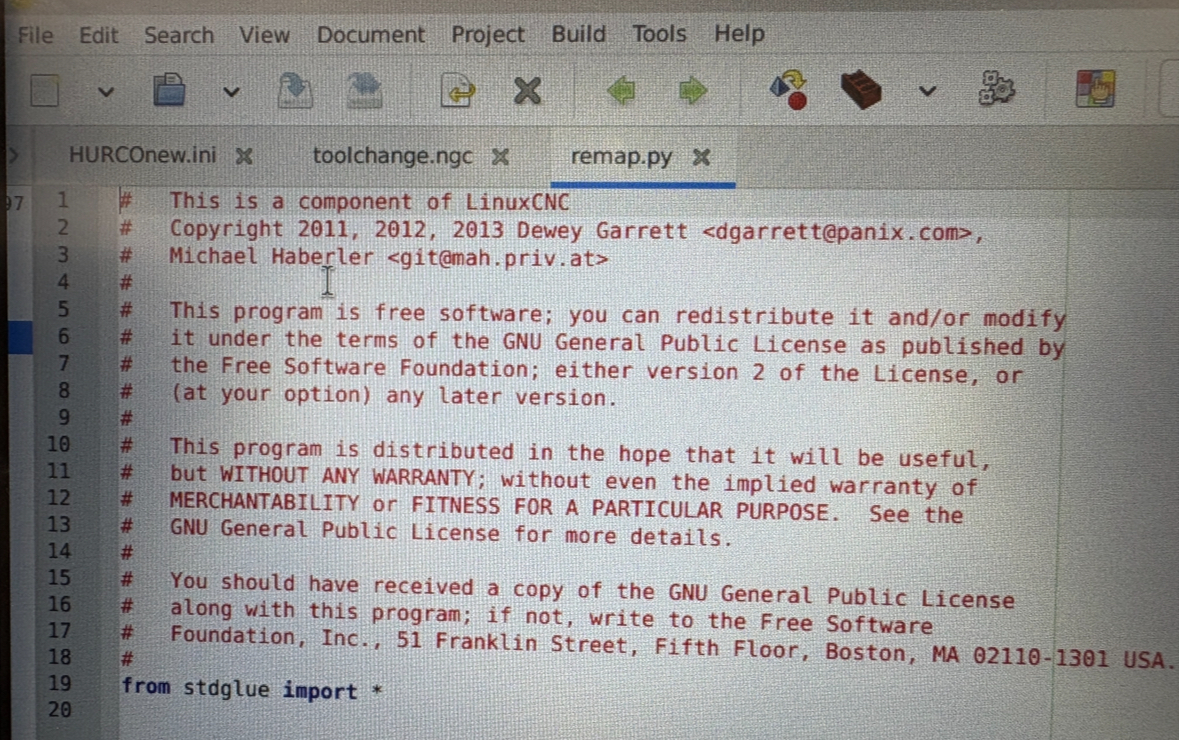
I just noticed that the file I attached had a date appended 'remap_2026-07-11.py', this date needs to be removed.
So make sure you go to your 'python' folder inside your config and rename that file to 'remap.py'.
So make sure you go to your 'python' folder inside your config and rename that file to 'remap.py'.
Last edit: 22 Jul 2026 07:22 by Aciera.
Please Log in or Create an account to join the conversation.
- 5_Zylinder
- Offline
- Senior Member
-
Less
More
- Posts: 63
- Thank you received: 3
22 Jul 2026 20:42 #347966
by 5_Zylinder
Replied by 5_Zylinder on topic Hurco BMC 30 AP
I checked the folder name again today; it was correct—without a date. I also have the latest Python3 version, 3.13.5-1. The error persists.
Please Log in or Create an account to join the conversation.
- 5_Zylinder
- Offline
- Senior Member
-
Less
More
- Posts: 63
- Thank you received: 3
31 Aug 2026 21:29 - 31 Aug 2026 21:31 #349165
by 5_Zylinder
Replied by 5_Zylinder on topic Hurco BMC 30 AP
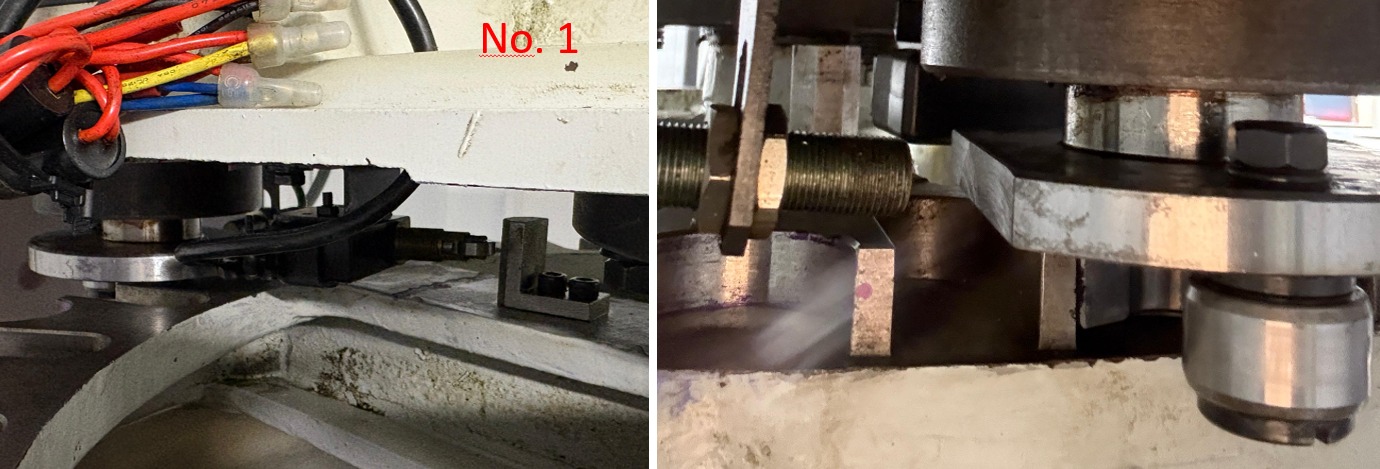
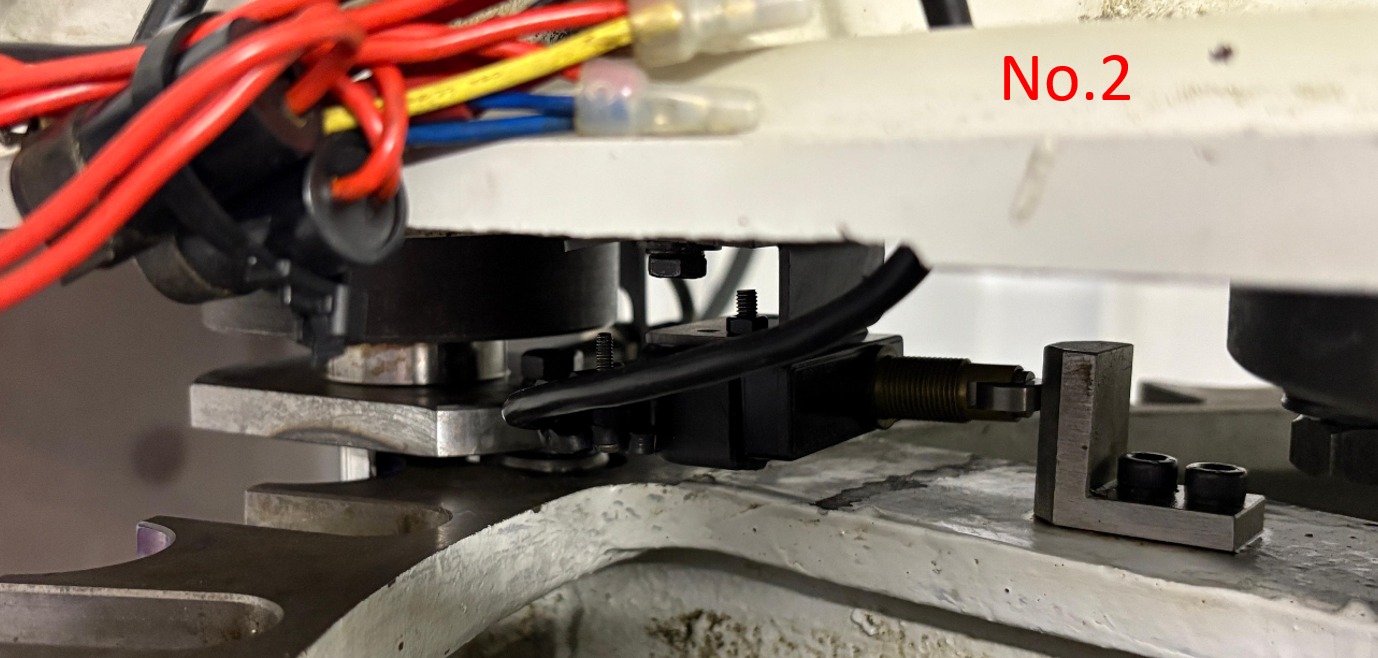
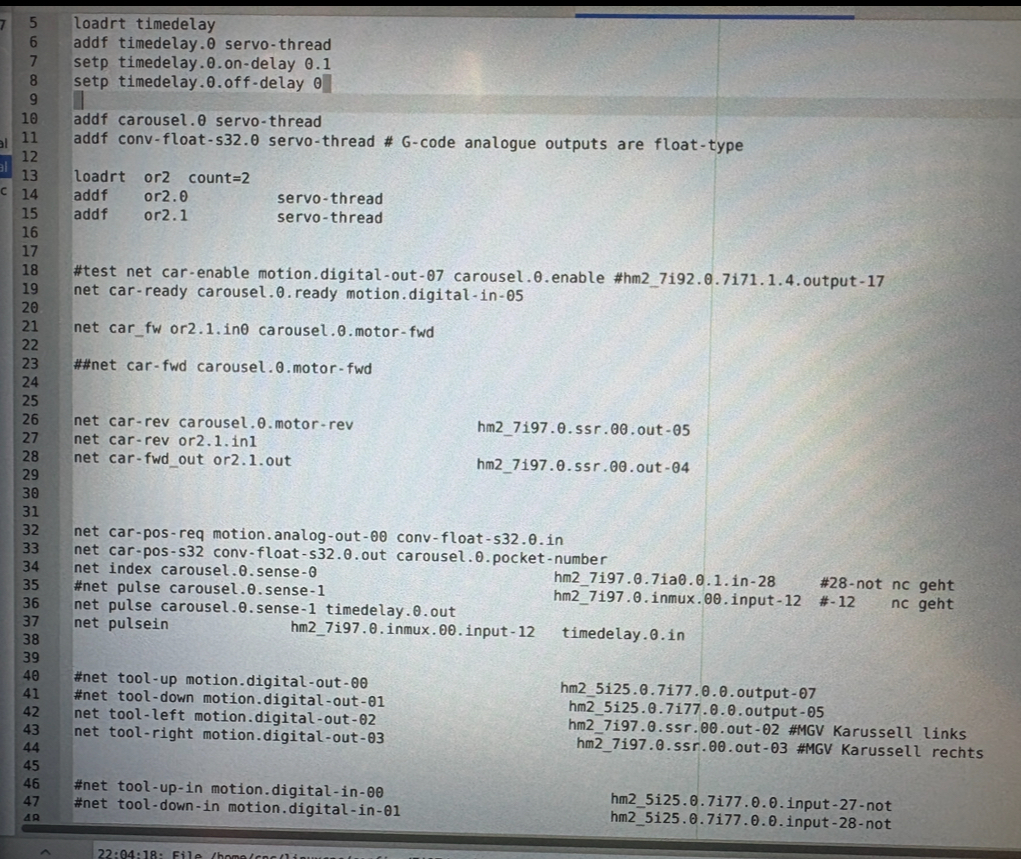
Hi everyone,I’m persisting in my efforts to get my machine finished using various methods.We’ve been trying to work with `carousel.comp`, but we’re running into issues with positioning the carousel. The cam limit switch is connected to Pin 28; it indicates the home position and is wired as Normally Open (NO). Pin 12 is connected to the proximity switch used for positioning the drive motor. It’s an NPN sensor: the contact is inactive when the cutout (missing material) passes by, and the sensor activates when material is present. Image 2 shows the program sequence as displayed in the screenshot. The problem arises when the cam limit switch (Pin 28) is triggered: the motor shuts off, but the carousel ends up positioned between two pockets. The motor needs to rotate another 180° so that the cutout aligns with the sensor. Image 1 shows the correct position—with the cutout aligned to the sensor (Pin 12)—even though the limit switch (Pin 28) has already been cleared.Can anyone suggest a solution for getting the positioning right?We’ve tried using "NOT" commands within `carousel.comp`, tried to wired as NC but haven't been able to resolve this specific issue.
Last edit: 31 Aug 2026 21:31 by 5_Zylinder.
Please Log in or Create an account to join the conversation.
- andypugh
-
- Offline
- Moderator
-
Less
More
- Posts: 19898
- Thank you received: 4654
09 Sep 2026 12:49 #349492
by andypugh
Settting decel-time and align-dc should activate this behaviour.
linuxcnc.org/docs/stable/html/man/man9/carousel.9.html
If the sense of the index marker is wrong, then you can typically connect to the inverted HAL input signal that most drivers support.
For example Mesa cards have pins like hm2_5i24.00.7i64.0.0.input-00-not which is an inverted version of hm2_5i24.00.7i64.0.0.input-00
Replied by andypugh on topic Hurco BMC 30 AP
Which version of "carousel"? The newer version supports a slow-speed search for the index marker.The problem arises when the cam limit switch (Pin 28) is triggered: the motor shuts off, but the carousel ends up positioned between two pockets. The motor needs to rotate another 180° so that the cutout aligns with the sensor.
Settting decel-time and align-dc should activate this behaviour.
linuxcnc.org/docs/stable/html/man/man9/carousel.9.html
If the sense of the index marker is wrong, then you can typically connect to the inverted HAL input signal that most drivers support.
For example Mesa cards have pins like hm2_5i24.00.7i64.0.0.input-00-not which is an inverted version of hm2_5i24.00.7i64.0.0.input-00
Please Log in or Create an account to join the conversation.
Time to create page: 0.325 seconds