Orientation position problem after run Gcode

More
3 years 1 month ago - 3 years 1 month ago #281390 by abdulasis12

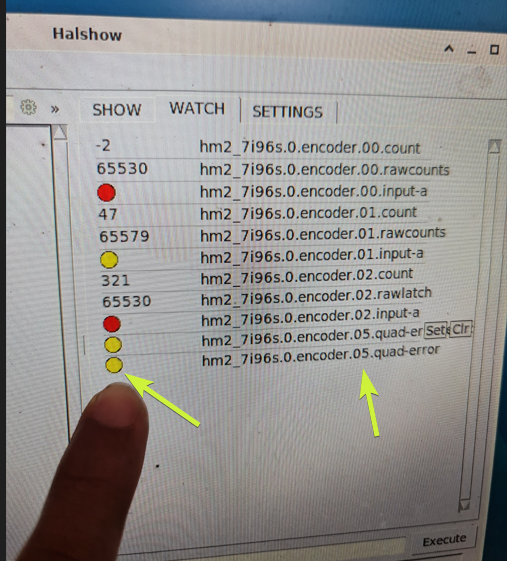
I would set the hm2_7i96s.0 encoder.05.quad-error-enable bit,
do your gcode test and see if hm2_7i96s.encoder.05.quad-error gets set true

Is the spindle encoder differential?
If so, is the 7I77 set for differential inputs?

 
My spindle type encoder differential signal , I can use function  "hm2_7i96s.0 encoder.05.quad-error-enable true"  right ?
Today I try.......
Change jumper on 7i77 Encoder 05 to quadrature position jump,

In hall I put use setp......... quad-error-enable true,
I test run step-up speed
M3 s200,
s500 ,
s1000
s2000
s3000
before s3000 all run good no show error .

When M3 s3000 it's show  "hm2_7i96s.0: Encoder 5 : quadrature count error"
any for me check next step ?


Last edit: 3 years 1 month ago by abdulasis12.

Please Log in or Create an account to join the conversation.

More
3 years 1 month ago - 3 years 1 month ago #281392 by PCW
OK I would first verify the you have valid differential signals at the 7I77
You can do this by measuring the differential voltage with a voltmeter

You measure _between_ A and /A  and _between_ B and /B
and verify that you have > 2V absolute in each state.
(you need to wiggle the spindle around to get each state)
One state should be >+2V and the other < -2V
(absolute value always greater than 2V)
Last edit: 3 years 1 month ago by PCW.

Please Log in or Create an account to join the conversation.
More
3 years 1 month ago #281630 by abdulasis12

OK I would first verify the you have valid differential signals at the 7I77
You can do this by measuring the differential voltage with a voltmeter

You measure _between_ A and /A  and _between_ B and /B
and verify that you have > 2V absolute in each state.
(you need to wiggle the spindle around to get each state)
One state should be >+2V and the other < -2V
(absolute value always greater than 2V)
Hi Mr. PCW
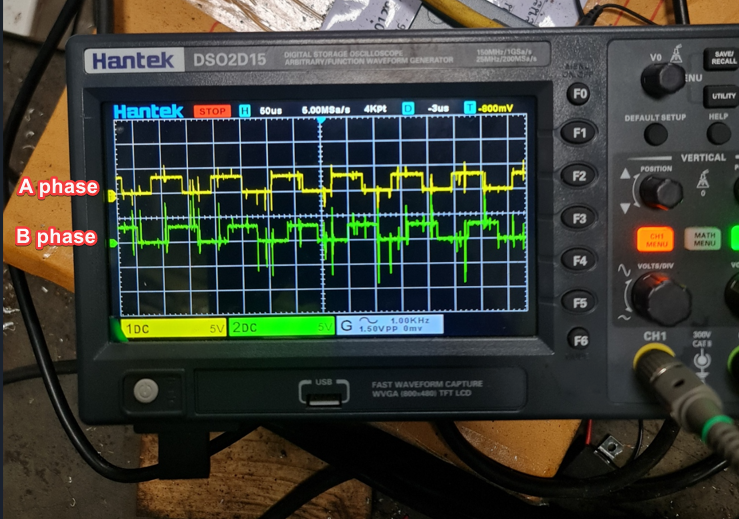
I check done , result show below in picture
Asis,


Please Log in or Create an account to join the conversation.

More
3 years 1 month ago #281999 by abdulasis12
Hi,
new update,
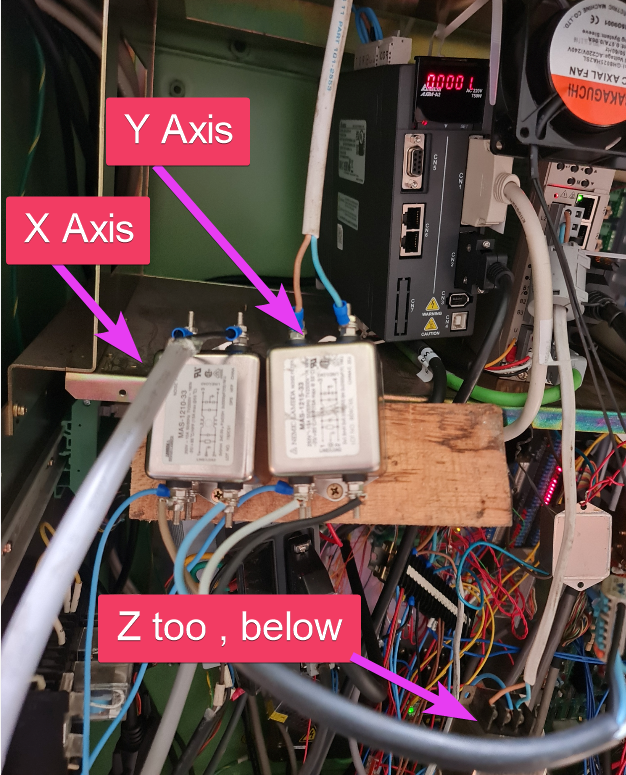
Yesterday I try install  EMI Filter on Servo Drive X,Y,Z 
result is same , after run gcode about 2 mins "M19 r0"  will wrong position.


Please Log in or Create an account to join the conversation.

More
3 years 1 month ago #282003 by Aciera
I'd recommend using shielded cables and proper grounding.
The following user(s) said Thank You: abdulasis12

Please Log in or Create an account to join the conversation.

More
3 years 1 month ago #282008 by abdulasis12

I'd recommend using shielded cables and proper grounding.
Have any idea for orientation with 7i77 ?
I Ever use spindle motor mitsubishi Meldas it's have orientation mode internal .
When sent signal output to trick spindle amplifier orientation, it's will spin up (in second) and decrease speed down with lock position for orientation before toolchange .

I think if can reset index or position encoder before orient will work with 7i77 too , for clear all error signal before orient (I try a lot time if spindle run lower 3000 rpm will orient correct all time, but in real when working I use spindle 6500 rpm+ and will wrong position encoder maybe from noise)

Can for reset index or encoder position before M19 ?

Please Log in or Create an account to join the conversation.

Time to create page: 0.074 seconds
Powered by Kunena Forum