Configuration 7i92m_7i76x1D

More
8 years 8 months ago - 8 years 8 months ago #105561 by aleksamc
Hi, dear forumers.

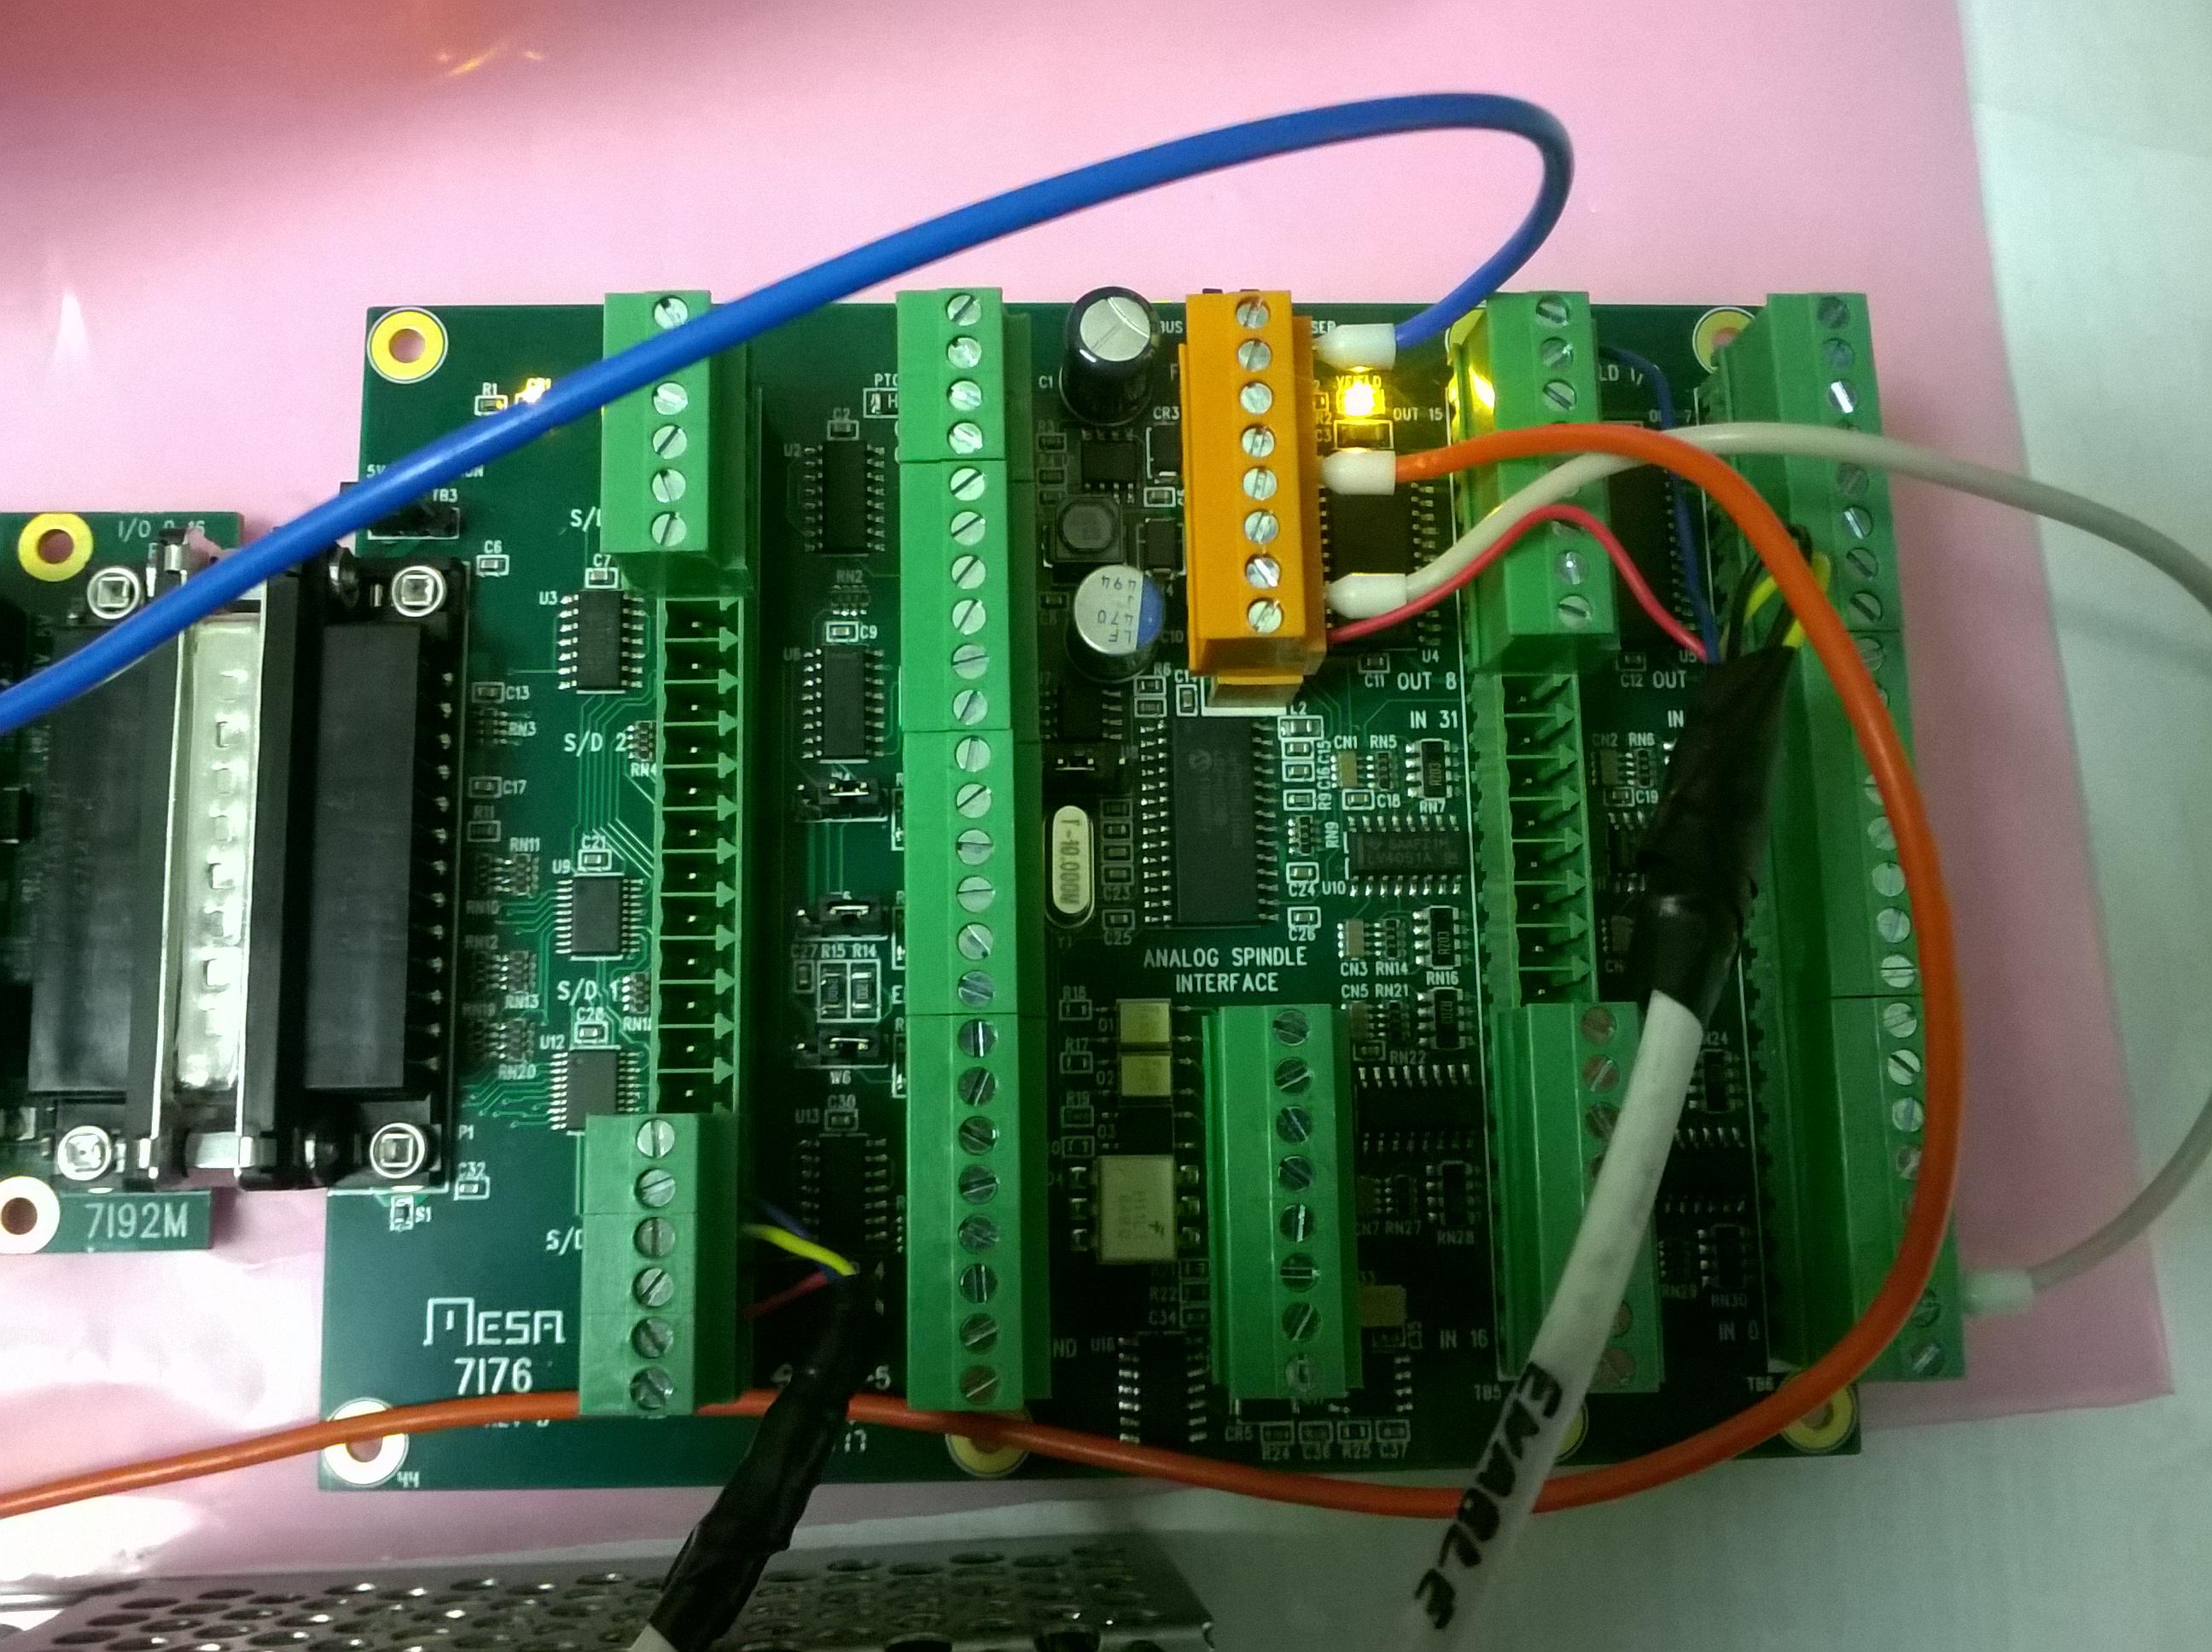
I've finaly got MESA 7i92M and 7i76 boards. It's my first experiance of configuring MESA.
I used to configure 5i25 configuration. And leave all at default settings to see what I really need in the future.

1. I loaded Mesaflash data to EEPROM of board.
2. Cnanged hm2_pci to hm2_eth
3. Changed 5i25 to 7i92.

Try to run linuxcnc but it terminates with error. What is wrong and why it's heppening? Simple stepconf configuration easyly runs but not that.

I attach config file and errors. Please help me to run my cnc.

File Attachment:

File Name: linuxcnc_t...ated.txt
File Size:60.96 KB

File Attachment:

File Name: MachineCNC.hal.txt
File Size:16.14 KB

File Attachment:

File Name: MachineCNC.ini.txt
File Size:4.63 KB
Last edit: 8 years 8 months ago by aleksamc.

Please Log in or Create an account to join the conversation.
More
8 years 8 months ago #105570 by andypugh
To use the Ethernet Mesa cards you can not use the RTAI kernel.

./MachineCNC.hal:8: Can't find module 'hm2_eth' in /usr/realtime-3.4-9-rtai-686-pae/modules/linuxcnc

Seems to indicate that you are usint RTAI (I would assume a default ISO install).

Make a copy of your config files somewhere safe (off the PC) and then install the PREEMPT-RT version of LinuxCNC mentioned here: forum.linuxcnc.org/38-general-linuxcnc-q...69-7i76e-quick-setup
(This is instructions for the 7i76E, but there is some commonality)
The following user(s) said Thank You: aleksamc

Please Log in or Create an account to join the conversation.

More
8 years 8 months ago - 8 years 8 months ago #105704 by aleksamc

andypugh wrote: To use the Ethernet Mesa cards you can not use the RTAI kernel.

./MachineCNC.hal:8: Can't find module 'hm2_eth' in /usr/realtime-3.4-9-rtai-686-pae/modules/linuxcnc

Seems to indicate that you are usint RTAI (I would assume a default ISO install).

Make a copy of your config files somewhere safe (off the PC) and then install the PREEMPT-RT version of LinuxCNC mentioned here: forum.linuxcnc.org/38-general-linuxcnc-q...69-7i76e-quick-setup
(This is instructions for the 7i76E, but there is some commonality)


Thanks for that AndyPugh. I run linuxcnc now.
Now I get new configuration errors. As I said, I use default configurations and changed them a little unconsciously.

I have two errors:
1) joint # following error. May be my configuration need to have encoder inputs as feedback. But I don't have encoder inputs. I need to cotrol servos with sted/dir signals only and PID regulation live to servodrive.

2) hm2/hm2_7i92.0: stepgen.00.maxvel is too big for current step & position-scale, clipping to max possible - it's for X axis. How to define this maxvel parameter for ethernet? As I worked with stepconf withard it was very simple - there was only latencytest.

File Attachment:

File Name: MachineCNC.hal
File Size:19.61 KB

File Attachment:

File Name: MachineCNC.ini
File Size:5.09 KB


My servodrive has 10000 impulses per/rev but I can change it to 1000 for example.
Last edit: 8 years 8 months ago by aleksamc.

Please Log in or Create an account to join the conversation.

More
8 years 8 months ago - 8 years 8 months ago #105706 by PCW
Replied by PCW on topic Configuration 7i92m_7i76x1D
There are a couple of issues here

1. The following errors are due to some pncconf bugs with metric configurations.
To fix, delete these lines in the hal file:
setp pid.x.maxerror .0005
setp pid.y.maxerror .0005
setp pid.z.maxerror .0005

Then in the INI file, X axis section, change:
P = 50.0
to
P = 1000

The reason you get the maxvel error is that you have specified a X velocity of 3000 mm/second (!)
but you cannot reach that velocity with your 10000 ns steplength 10000 ns stepspace timings.
In fact, with your 10000/10000 timings, and a scale of 10000 steps per mm you can only reach 5 mm/second.
Last edit: 8 years 8 months ago by PCW.

Please Log in or Create an account to join the conversation.

More
8 years 8 months ago #105712 by aleksamc
Thanks for very!!! fast answer, PCW. I've perform your advice and that problems are out.

But I have another problems now))) Axes are not moving. I wonder, how to know if output board generates pulses at connected outputs if I don't have osciloscope? It could be problem with servodrive, but it's hard possible - they are was in work and everything was fine.

My servo drive (Maxsine EP1C) has monitoring parameter tat defines number of input pulses ( it's instead of osciloscope) but there is 0 and nothing change. Feed voltage is 5V.

It can't be low step/dir timing because step time is 1400ns in datasheet.
May be my outputs are not connected to needed inputs in hal.
As for "Enable input" - the driver see it fine.
My jumpers are in such positions:
7i92: w1 - up, w3: down , w4: up
7i76: w1 -left, w2 - left, w3 - left, w4-w6 - right.
Does somebody know what it should be?

File Attachment:

File Name: MachineCNC...10-3.ini
File Size:5.08 KB

File Attachment:

File Name: MachineCNC...10-3.ini
File Size:5.08 KB

File Attachment:

File Name: MachineCNC...10-3.ini
File Size:5.08 KB

File Attachment:

File Name: MachineCNC...10-3.hal
File Size:19.66 KB

Please Log in or Create an account to join the conversation.

More
8 years 8 months ago #105714 by PCW
Replied by PCW on topic Configuration 7i92m_7i76x1D
You can check the step outputs with a LED. You may set the steptime to a fairly high number
to see the LED light up (the dir pin is easy to check with a LED though)

Note that a LED across the step pins will light up brightly in one direction (use the other direction)

Please Log in or Create an account to join the conversation.

Moderators: cmorley
Time to create page: 0.395 seconds
Powered by Kunena Forum
