Lathe Macros

More
3 years 11 months ago #256597 by andypugh
Replied by andypugh on topic Lathe Macros
You shouldn't need to be registered.
I have collected all the versions as .zip files here:

github.com/andypugh/LatheMacros/releases

You should expaned the "Assets" of v3.0 and download the .zip file.
The following user(s) said Thank You: Masiwood123

Please Log in or Create an account to join the conversation.

More
3 years 11 months ago #256599 by Masiwood123
Replied by Masiwood123 on topic Lathe Macros
that's great, thanks a lot, I'll let you know what happens as soon as I try it

Please Log in or Create an account to join the conversation.
More
3 years 11 months ago #256605 by Masiwood123
Replied by Masiwood123 on topic Lathe Macros
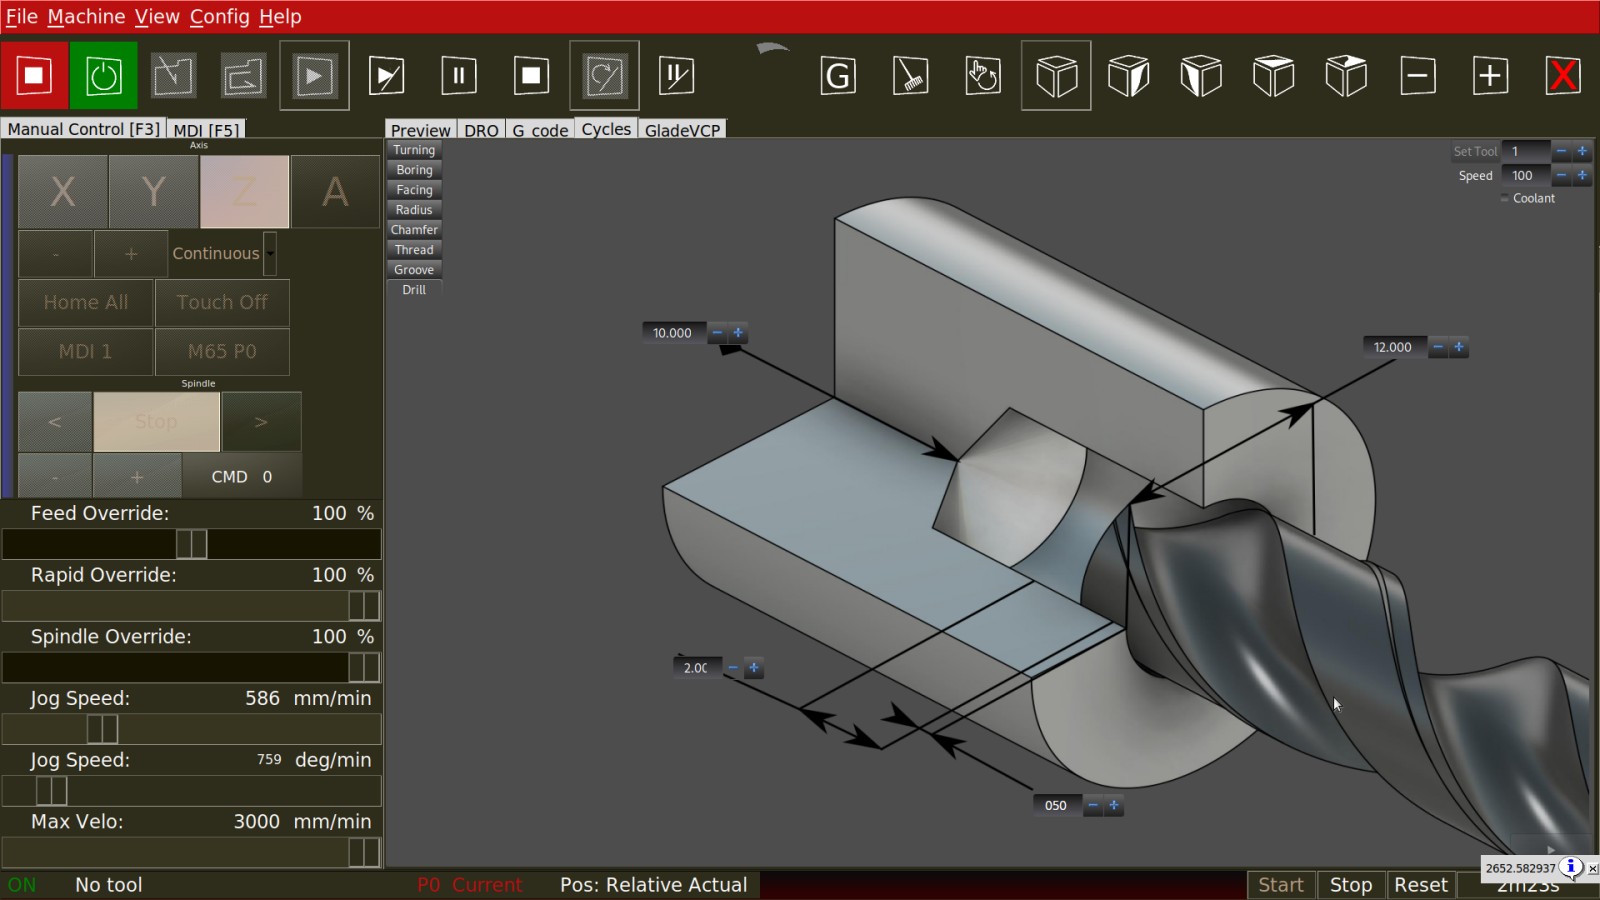
now it works:)) and I really like the interface, unfortunately it won't start the program, it shows in the background that the program is running (and this red line also signals that the gcode is being executed, but the axes don't move) however, I usually edit the start line of the gcode to would the program work or ``run from here'' for some simple program, here I am not able to see the lines of the program.. is there a possibility for linuxcnc to export the gcode through this macro so that I can edit it? 

Please Log in or Create an account to join the conversation.

More
3 years 11 months ago - 3 years 11 months ago #256610 by Masiwood123
Replied by Masiwood123 on topic Lathe Macros
;drilling

; Use T = 0 for tailstock drilling, then this just sets speed

O<drilling> SUB

G18 ; XZ Plane
G21 ; Metric Units
G90 ; Absolute Distance
G91.1 ; but not for arcs

#10 = [#2 * 1000 / [ #1 * 3.141592]]
(debug, #10)
O90 IF [#7 GT 0.5]
M8
O90 ENDIF

O100 IF [#6 LT 0.5]
G97 M3 S#10
O<drilling> RETURN
O100 ENDIF

M6 T#6 G43
G0 X0

O83 IF [#5 GT 0] ; Pecking
G17
G95 F#3 ; Feed-Per-Rev Mode
G97 M3 S#10
G98
G83 R#<_z> Q#5 Z#4
M5 M9 G18
O<drilling> RETURN
O83 ENDIF

O82 IF [1]; not pecking
G17
G95 F#3 ; Feed-Per-Rev Mode
G97 M3 S#10
G98
G82 R#<_z> P0.5 Z#4
M5 M9 G18
O82 ENDIF

O<drilling> ENDSUB

O<drilling> call [10] [100] [0.03] [0] [2] [0] [1]

M2

or maybe I should try to edit this routine to skip some of the first lines of execution, add or similar..maybe is CSS problem?
Last edit: 3 years 11 months ago by Masiwood123.

Please Log in or Create an account to join the conversation.

More
3 years 11 months ago #256626 by andypugh
Replied by andypugh on topic Lathe Macros
It's all in CSS and feed-per-rev so you need spindle speed feedback or there will be no motion.

Do you have a spindle encoder?
The following user(s) said Thank You: Masiwood123

Please Log in or Create an account to join the conversation.

More
3 years 11 months ago #256627 by andypugh
Replied by andypugh on topic Lathe Macros
Oh, and 100m/min (the default) is much too fast for a HSS drill, best change that now before it's too late.

Please Log in or Create an account to join the conversation.

Time to create page: 0.328 seconds
Powered by Kunena Forum
