Lathe Macros

More
3 years 5 months ago #271614 by andypugh
Replied by andypugh on topic Lathe Macros
My lathe uses Touchy. As I do almost everything with the macros I don't really miss the preview.

Please Log in or Create an account to join the conversation.

More
3 years 5 months ago #271615 by Baldorcete
Replied by Baldorcete on topic Lathe Macros
I really like the preview. Old school, preview and simulate when you can and it's reasonable. Heck, define a big Z tool offset and simulate phisically!! I have seen to many hard crashes by a missplaced character when coding some very simple program directly on the CNC. Simulatinons are cheap, repairs and redoing entire parts are expensive.

(And sorry for my poor english. You should have noticed by now it is not my native language)

Please Log in or Create an account to join the conversation.
More
3 years 3 months ago - 3 years 3 months ago #275356 by RotarySMP
Replied by RotarySMP on topic Lathe Macros
Hi Andy,
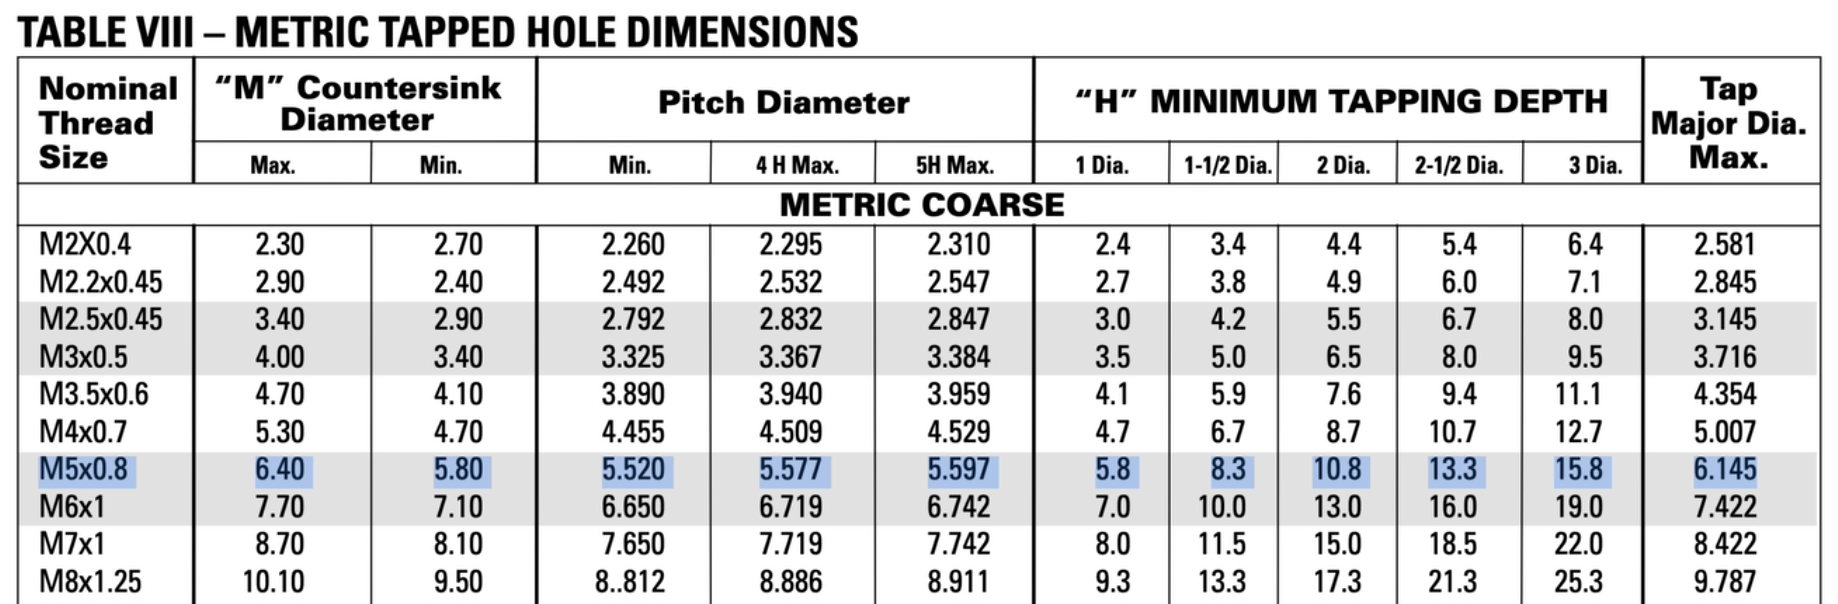
I see that the threading page only has inputs for pitch and OD. Does this mean that it does all the calculations for metric and unified threads automatically? I just cut a test M5x0.8STI (the Helicoil tap for M5), which has these dimensions:
 

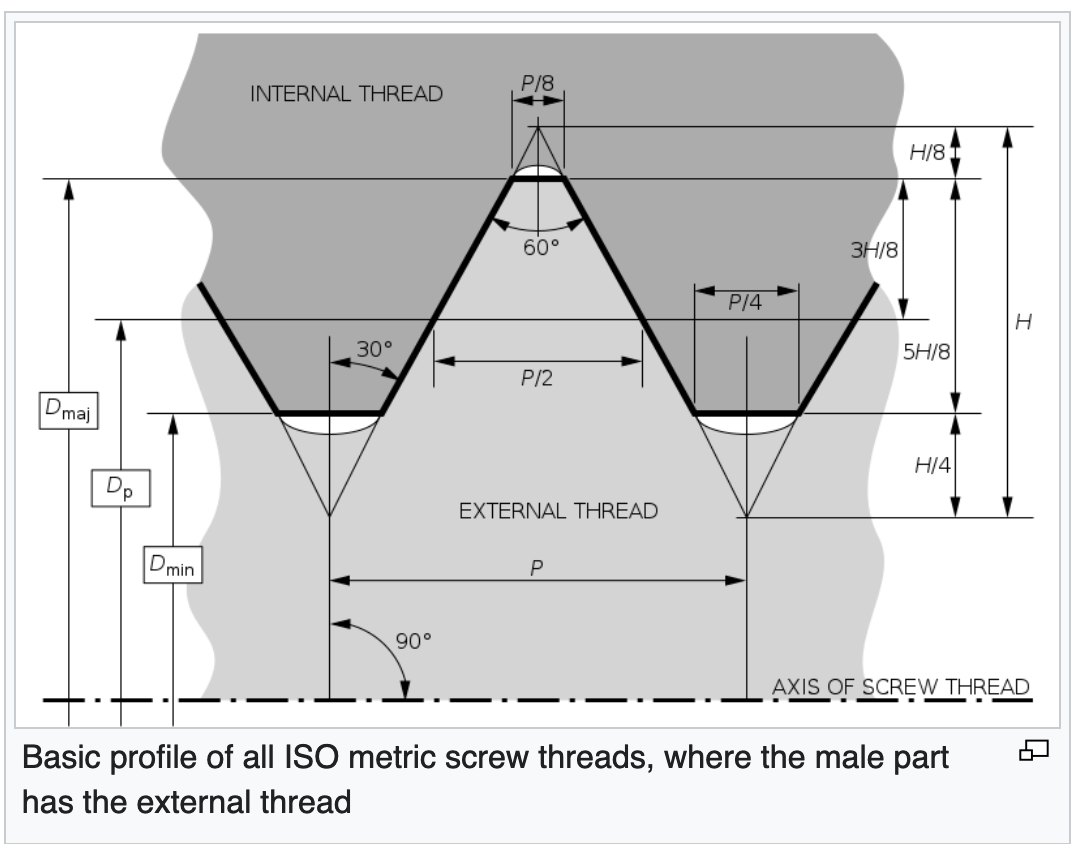
Setting 6.145mm OD in your macro, it first did a turning pass at about 6.05mm, before turning the thread. Does that mean you are expecting the nominal diameter to be given, and are turning off the H/8 thread tip on that pass?
 

Since the Heilcoil manual gives a dimension for the taps major diameter, rather than a nominal diameter, do you think I should be inputting 6.145 + (6.145-6.05) = 6.24mm into the lathe macro as my nominal diameter, so that macro can remove the H/8 again?

Cheers, Mark
Last edit: 3 years 3 months ago by RotarySMP.

Please Log in or Create an account to join the conversation.
More
3 years 3 months ago - 3 years 3 months ago #275360 by andypugh
Replied by andypugh on topic Lathe Macros

I see that the threading page only has inputs for pitch and OD. Does this mean that it does all the calculations for metric and unified threads automatically?

Yes. It's a bit out for Whitworth or BA because of that.
Note that the number entry box will let you type (for example) 11 then tpi-pitch then in-mm to program an 11tpi thread.

Setting 6.145mm OD in your macro, it first did a turning pass at about 6.05mm, before turning the thread. Does that mean you are expecting the nominal diameter to be given, and are turning off the H/8 thread tip on that pass?


Yes, exactly that.
Last edit: 3 years 3 months ago by andypugh.
The following user(s) said Thank You: RotarySMP

Please Log in or Create an account to join the conversation.

More
3 years 3 months ago #275363 by RotarySMP
Replied by RotarySMP on topic Lathe Macros
Thanks for the quick confirmation Andy. Nice work there. Another good reason to avoid Whitworth, BA etc :)

Okay, for 0.8mm pitch, I'll need to add 2x H/8 to the Dmaj, to get the nominal which your macro starts with. So my DMaj of 6.145mm will be Nominal of 6.284mm given a tool with no radius.

Please Log in or Create an account to join the conversation.

More
3 years 3 months ago #275589 by endian
Replied by endian on topic Lathe Macros
hello,

thanks a lot for your job. It will make our life better and easier with this macro page. It is really nice stuff!

I want to aske, if there missing drilling and grooving page in V2 macros which I downloaded from AndysGit , is possible to implement to V2 running on v2.8 or move to v2.9?

Regards Slav

Please Log in or Create an account to join the conversation.

Time to create page: 0.557 seconds
Powered by Kunena Forum
