
- Posts: 757
- Thank you received: 216
Another plasma component...
- islander261
- Offline
- Platinum Member
-

Less
More
7 years 6 months ago #131099
by islander261
Replied by islander261 on topic Another plasma component...
Phill
I had always thought of automatic fallback to the float switch when it is activated first but the setting the retries solution should be workable as you usually know when you want to use the float switch VS ohmic.
I still had a large number of false shorted probing failures. Every time I checked with the test button the torch was clear. I must admit that with my Gmoccapy configuration I always probed very slowly down and 1/16 the probe speed up. I have my debounce set to 5 times so that may be why I didn't get many false alarms.
I run my table like a milling machine and not like some Mach 3 configuration from PS. I home the machine on startup to establish the machine coordinates. The machine Z zero is at the top (away from bed) of the Z motion. Then I place the material on the table and set the work piece zero by jogging the torch to the correct location (I have a couple of laser line generators to make a crude set of cross hairs). I then set the G54 X zero and Y zero offsets to that location. So at this point my machine knows where it is and the offsets to the work piece. When I probe the material I set the work piece Z zero to the top surface of the material using a G92 Z0 (one could also use a known offset). Then I start cutting. At the end of the Gcode file I always do a G92.1 to clear the G92 offsets. So when cutting my DRO always shows the height above the material the torch is. Oh, I do have a "permanent" G54 Z offset so that the work piece Z is the actual approximate height above the slats.
Here are a couple of videos that show the probing I described previously.
I also grabbed a halscope of part of the outside cut on one of the crabs. The big voltage spikes are the slowdowns for the sharp corners. Look at how nice and steady the voltage is in between. One thing I found when working out the corner lock on my system is that one needs to keep the height hold active until the speed gets back to 99% of the target speed. !00% always caused problems over being reliable. What happens is the arc voltage lags the torch speed a bit so if you restart THC at the same point you held the height the voltage is still way high and the torch dives.
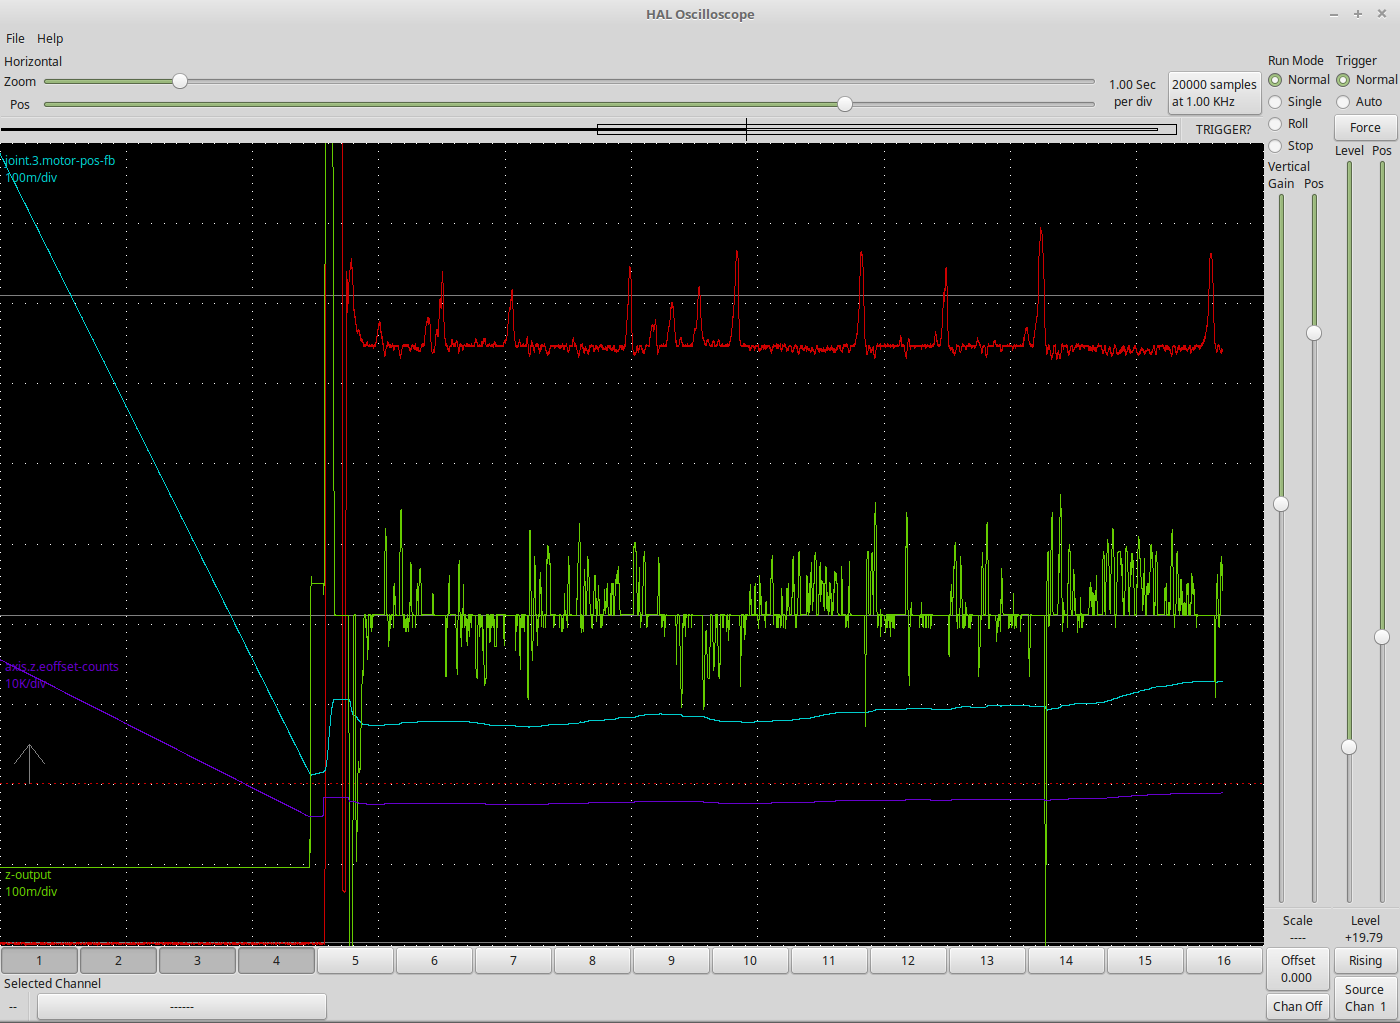
For those that haven't done much of this it is a good plot of a real (non straight line) cut.
John
I had always thought of automatic fallback to the float switch when it is activated first but the setting the retries solution should be workable as you usually know when you want to use the float switch VS ohmic.
I still had a large number of false shorted probing failures. Every time I checked with the test button the torch was clear. I must admit that with my Gmoccapy configuration I always probed very slowly down and 1/16 the probe speed up. I have my debounce set to 5 times so that may be why I didn't get many false alarms.
I run my table like a milling machine and not like some Mach 3 configuration from PS. I home the machine on startup to establish the machine coordinates. The machine Z zero is at the top (away from bed) of the Z motion. Then I place the material on the table and set the work piece zero by jogging the torch to the correct location (I have a couple of laser line generators to make a crude set of cross hairs). I then set the G54 X zero and Y zero offsets to that location. So at this point my machine knows where it is and the offsets to the work piece. When I probe the material I set the work piece Z zero to the top surface of the material using a G92 Z0 (one could also use a known offset). Then I start cutting. At the end of the Gcode file I always do a G92.1 to clear the G92 offsets. So when cutting my DRO always shows the height above the material the torch is. Oh, I do have a "permanent" G54 Z offset so that the work piece Z is the actual approximate height above the slats.
Here are a couple of videos that show the probing I described previously.
I also grabbed a halscope of part of the outside cut on one of the crabs. The big voltage spikes are the slowdowns for the sharp corners. Look at how nice and steady the voltage is in between. One thing I found when working out the corner lock on my system is that one needs to keep the height hold active until the speed gets back to 99% of the target speed. !00% always caused problems over being reliable. What happens is the arc voltage lags the torch speed a bit so if you restart THC at the same point you held the height the voltage is still way high and the torch dives.
For those that haven't done much of this it is a good plot of a real (non straight line) cut.
John
The following user(s) said Thank You: phillc54
Please Log in or Create an account to join the conversation.
- phillc54
- Offline
- Platinum Member
-
Less
More
- Posts: 5711
- Thank you received: 2100
7 years 6 months ago #131100
by phillc54
Replied by phillc54 on topic Another plasma component...
Thanks John,
That probing is just plain wrong, I will try to emulate that on my test rig.
Cheers, Phill.
That probing is just plain wrong, I will try to emulate that on my test rig.
Cheers, Phill.
Please Log in or Create an account to join the conversation.
- phillc54
- Offline
- Platinum Member
-
Less
More
- Posts: 5711
- Thank you received: 2100
7 years 6 months ago #131110
by phillc54
Replied by phillc54 on topic Another plasma component...
I have pushed another update:
- fix a timing issue causing probe trip errors.
Probing works like:
If ohmic-max-attempts = 0, a probe will trigger by the first of ohmic or floatswitch.
If ohmic-max-attempts = n, probing will attempt an ohmic probe, if unsuccessful move to probe height and try again, if unsuccessful n times, move to probe height then trigger by the first of ohmic or floatswitch.
Any successful probe will then move on to pierce height.
Cheers, Phill.
Please Log in or Create an account to join the conversation.
- islander261
- Offline
- Platinum Member
-
Less
More
- Posts: 757
- Thank you received: 216
7 years 6 months ago - 7 years 6 months ago #131186
by islander261
Replied by islander261 on topic Another plasma component...
Phill
I installed the latest today and only got as far as static testing.
In the configuration tab the safe height (Safe Z) now only allows entries in the .04" to .25" range now. The previous build I was using had a default value of .75" and I set mine to 1.0". This appears to be some kind of configuration problem as the sim works as it should.
Ohmic Probing is now ending up about .01" high right now. I set .09" and get .1". I check the physical height frequently so this isn't a show stopper for me, at least the error is in acceptable direction.
John
Last edit: 7 years 6 months ago by islander261.
Please Log in or Create an account to join the conversation.
- phillc54
- Offline
- Platinum Member
-
Less
More
- Posts: 5711
- Thank you received: 2100
7 years 6 months ago - 7 years 6 months ago #131201
by phillc54
Minimum = 0.1
Maximum = ini.z.max_limit
Default = 0.75 (only if there is no entry in the cfg file)
These are in plasmac_config.py, probably quite a few of the defaults in here need revisiting...
EDIT: It won't be that, I have tried imperial and metric configs with debounce at 1 and at 20, at 1 it is within 2 thou (always higher) and at 20 is higher by less than 3.4 thou - these are conversions as I only have metric feeler gauges. Also the measurements are very consistent.
I think I may have misinterpreted (again) your probing sequence.
Rather than having the spinbutton for ohmic attempts should it just be a checkbox to allow floatswitch fallback labelled "Float Switch".
If "Float Switch" enabled, successful probe on first to activate, ohmic or float.
If "Float Switch" not enabled then error after ??? attempts.
Trying to get it right for those who do have ohmic and those who don't...
Cheers, Phill.
Replied by phillc54 on topic Another plasma component...
Currently the settings are:In the configuration tab the safe height (Safe Z) now only allows entries in the .04" to .25" range now. The previous build I was using had a default value of .75" and I set mine to 1.0". This appears to be some kind of configuration problem as the sim works as it should.
Minimum = 0.1
Maximum = ini.z.max_limit
Default = 0.75 (only if there is no entry in the cfg file)
These are in plasmac_config.py, probably quite a few of the defaults in here need revisiting...
That is a lot more error than I get here, what is your debounce set to?Ohmic Probing is now ending up about .01" high right now. I set .09" and get .1". I check the physical height frequently so this isn't a show stopper for me, at least the error is in acceptable direction.
EDIT: It won't be that, I have tried imperial and metric configs with debounce at 1 and at 20, at 1 it is within 2 thou (always higher) and at 20 is higher by less than 3.4 thou - these are conversions as I only have metric feeler gauges. Also the measurements are very consistent.
I think I may have misinterpreted (again) your probing sequence.
Rather than having the spinbutton for ohmic attempts should it just be a checkbox to allow floatswitch fallback labelled "Float Switch".
If "Float Switch" enabled, successful probe on first to activate, ohmic or float.
If "Float Switch" not enabled then error after ??? attempts.
Trying to get it right for those who do have ohmic and those who don't...
Cheers, Phill.
Last edit: 7 years 6 months ago by phillc54.
Please Log in or Create an account to join the conversation.
- rodw
- Offline
- Platinum Member
-
Less
More
- Posts: 12170
- Thank you received: 4153
7 years 6 months ago #131202
by rodw
Replied by rodw on topic Another plasma component...
Well, its taken a while but you may have noticed I've started to adopt plasmac now I have Ohmic sensing on my table (I hope). I'll try and keep it clean of chatter so its an installation manual. But I will report on things I find here.
One thing I noticed in the INI file you have
It should follow the axes in the machine as follows:
This is enough for one session. I gotta stand at the machine so there is only so much of that I can handle.
One thing I noticed in the INI file you have
Code:
[TRAJ]
COORDINATES = XYYZ
It should follow the axes in the machine as follows:
Code:
[TRAJ]
COORDINATES = XYZ
This is enough for one session. I gotta stand at the machine so there is only so much of that I can handle.
Please Log in or Create an account to join the conversation.
Moderators: snowgoer540
Time to create page: 2.478 seconds