Center Spot Sheetcam Post

More
7 years 1 month ago #145102 by phillc54
Replied by phillc54 on topic Center Spot Sheetcam Post
That was referring to Stevens 45XP set to Gouge mode, 10A and marking consumables.
The following user(s) said Thank You: thefabricator03

Please Log in or Create an account to join the conversation.

More
7 years 1 month ago #145137 by islander261
Rod

I am sure that without using external hardware (as Keith does) or fast arc voltage monitoring the path to success will be different for HT and TD power supplies. My TD A-60 requires a torch fire signal at least .7s long to get the torch to fire even briefly when using the torch fire button on Plasmac (maybe some knowledgeable TD engineer can weigh in on this) . The OK to Move signal is also very slow, I typically use zero pierce delay up to 10ga steel. I believe that stopping the arc is fairly quick once the torch fire signal is removed. This is sounding like it is time for a little halscope investigation.

John

Please Log in or Create an account to join the conversation.
More
7 years 1 month ago #145171 by docwelch
Replied by docwelch on topic Center Spot Sheetcam Post
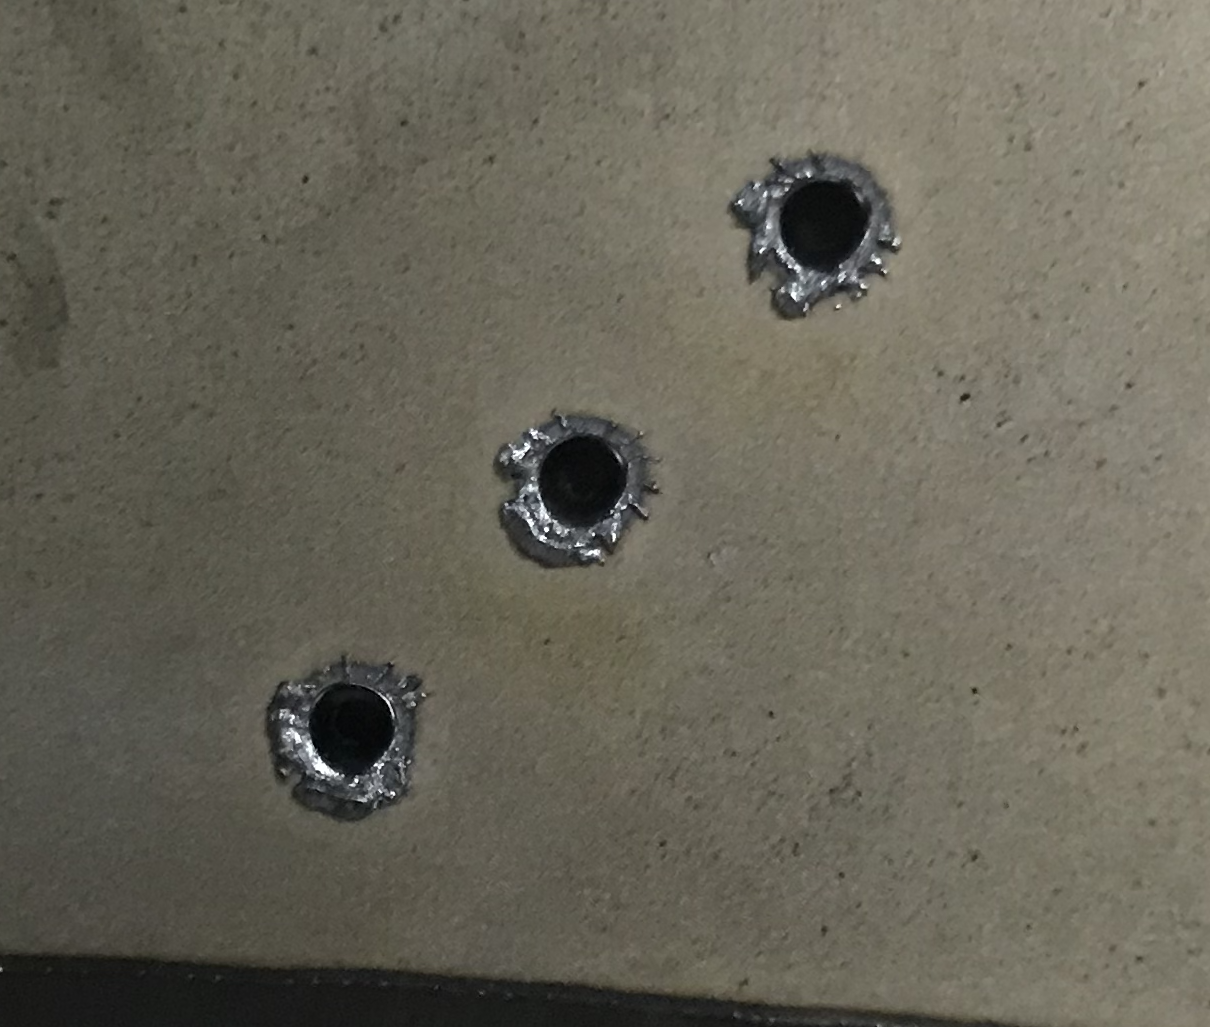
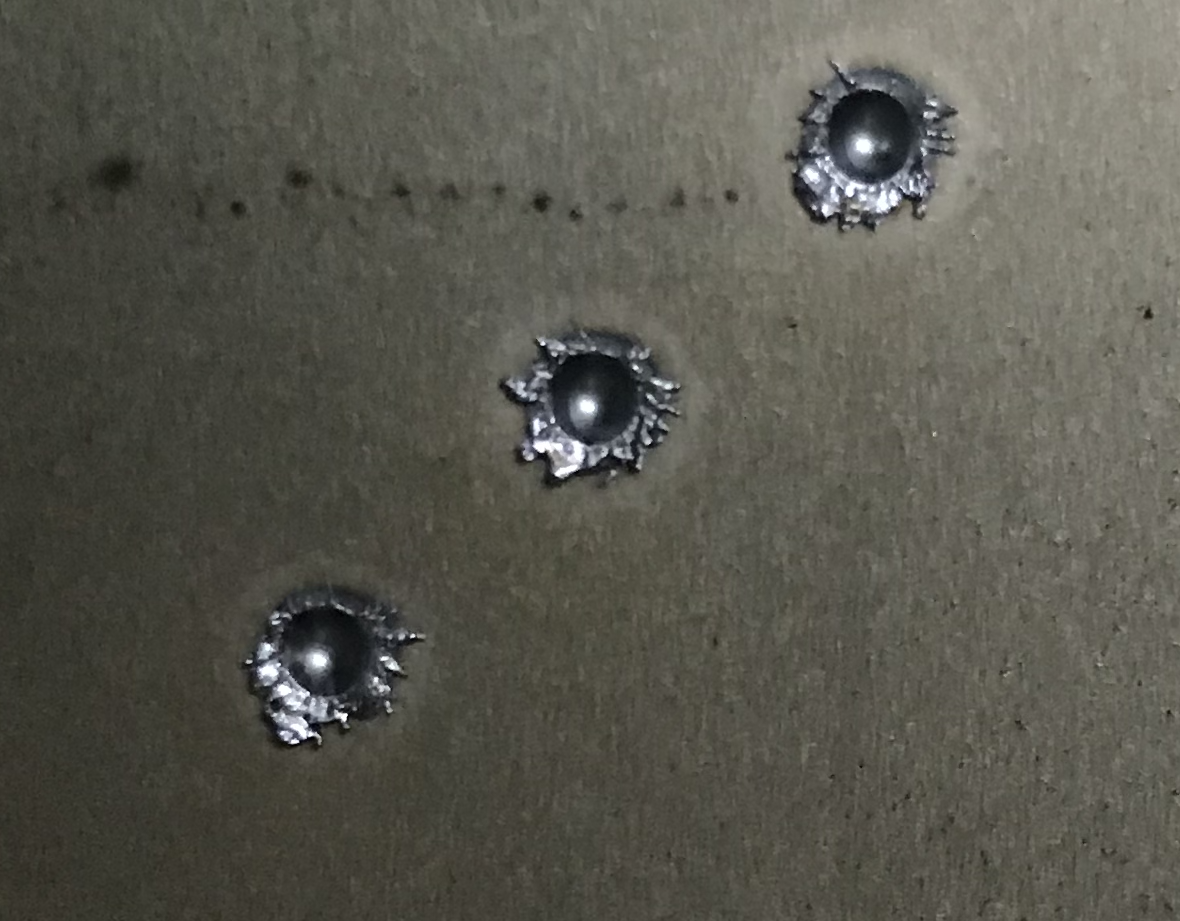
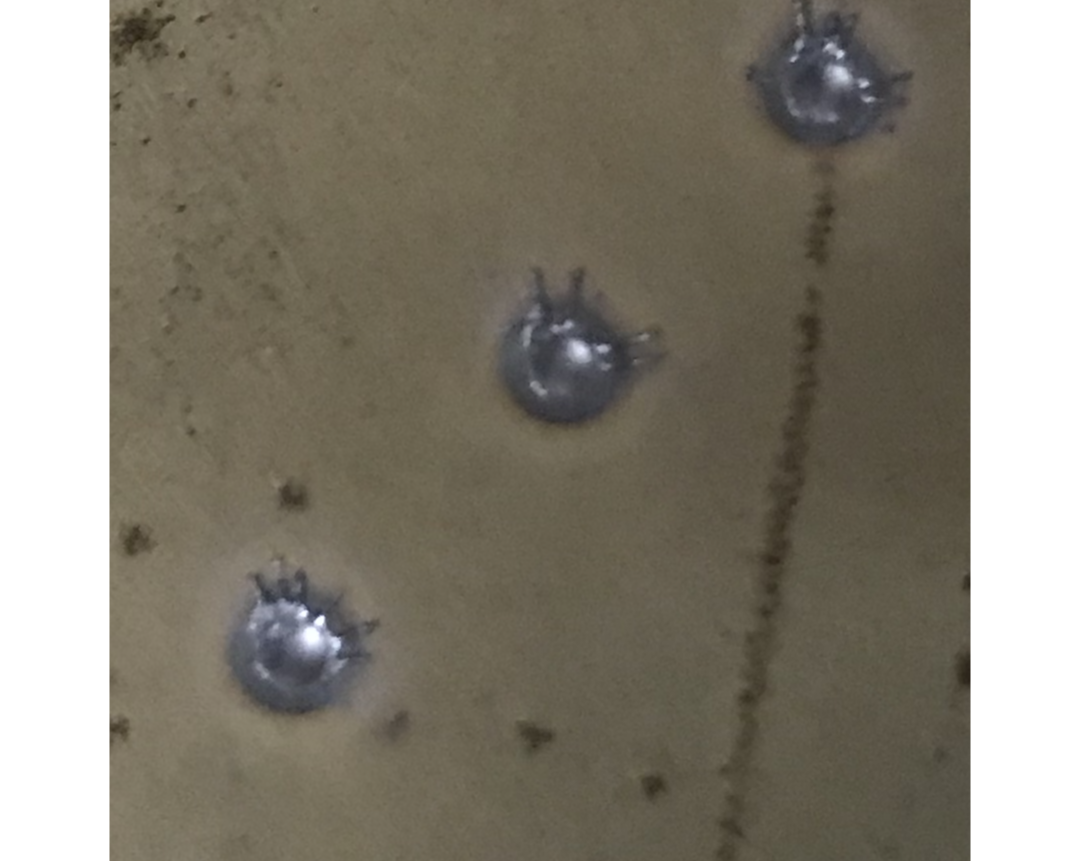
Success! Using Phill's experimental plasmac.comp (and remembering to rebuild LinuxCNC), my machine made 3 nice dimples in a row. I set the torch on time to 299. I think Phill said this would cause the torch to fire and then turn it off when it got an Arc OK signal. The really good news is I could make dimples with my usual fine cut consumables in cut mode. I did try using the marking/gouge mode but there was no difference (at least with my fine cut consumables).

The following pictures are of 18g CR steel, fine cut consumables, cutting mode. The dimples are at (0.25", 0.25"), (0.5",0.5"), and (0.75",0.75") to give you some idea of the size:

45a at a pierce height of 0.15" - it did not completely pierce the material but you can feel the dimple on the back side.


10a at pierce height of 0.15" - makes a nice dimple


10a at a pierce height of 0.25" - makes a nice dimple but more shallow. I did this as the Hypertherm cut charts for dimpling use this height.


So, a great big thanks to Phill and good news for those with Hypertherm equipment - it can work without changing consumables and modes and current.

Steven
The following user(s) said Thank You: phillc54, thefabricator03

Please Log in or Create an account to join the conversation.
More
7 years 1 month ago - 7 years 1 month ago #145173 by islander261
Guys

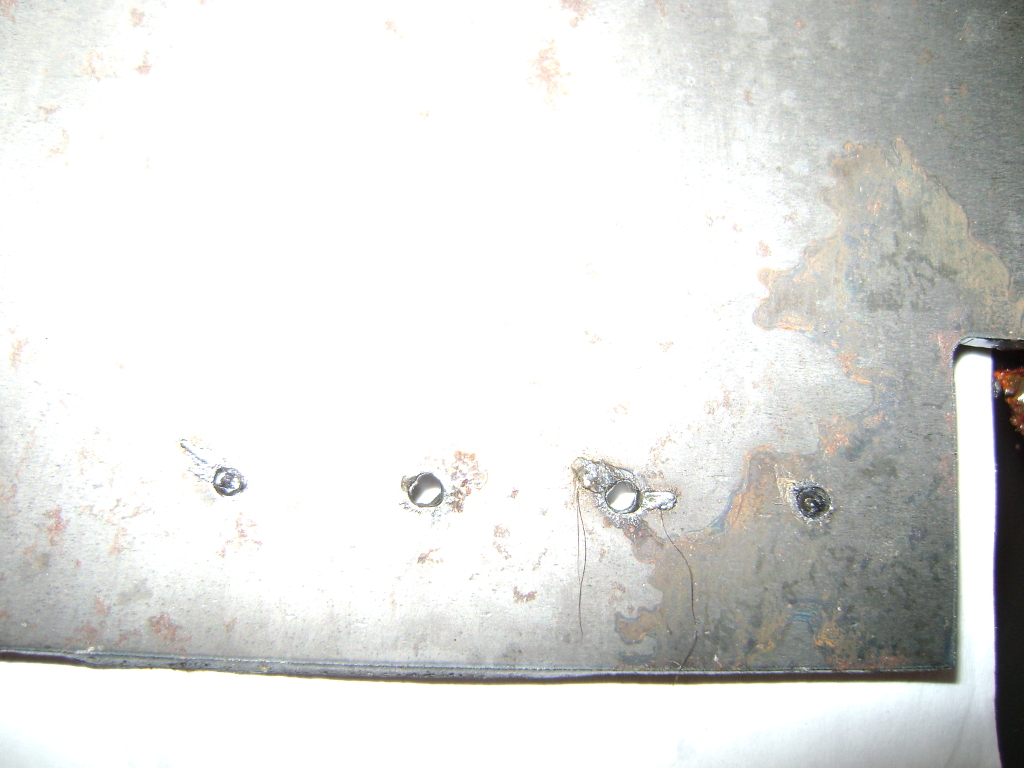
I did a few tests with my TD A-60 and did manage to make a couple of marks. The power supply was set to 45A and the torch height was .090", the correct height for piercing with the Finecut consumables used. I tested using the torch pulse function at pulse widths from .1s to .9s. The test material was 14ga (2mm) hot rolled steel. Sorry I haven't looked into using the center punch post or PlasmaC functions.

Some top level observations:
1. The power supply didn't produce any arc voltage until the plasmac.torch-on pulse width was .6s or greater.
2. The arc voltage starts to decay rapidly 7ms to 10ms after plasmac.torch-on goes low.
3. The power supply OK to Move signal (plasmac.arc-ok-in) is delayed from the apparent arc transfer by about 15ms.
4. At approximately 2.5ms of arc time past OK to Move (plasmac.arc-ok-in) going true the center punch mark produced an approximately .039" (1mm) deep mark. I had no way to finely control this time during the test so the next longest increment punched all the way through the material.


The pulse times from right to left are .7s, .8s, .9s and .7s. While in the photo it appears that both .7s dimples went all the way through the material I wasn't able to push a 30ga wire through either hole. When I examined the back side of the material it confirmed that the .7s pulses (about 2.5ms arc time after Ok to Move went true) did not penetrate the material completely.

I have attached Halscope screen shots for pulse times of .6s to .9s.
6_10... 1412-16-19.png is .6s pulse width
7_10...1412-22-48.png is .7s pulse width, far right dimple in photo
8_10...1412-26-50.png is .8s pulse width, second from right in photo
9_10...1412-30-10.png is .9s pulse width, second from left in photo
7_10-2...1412-38-32.png is .7s pulse width, far left in photo

The results for using a TD torch or using a HT power supply will be different.
John
Last edit: 7 years 1 month ago by islander261. Reason: clearifying attached screen shot origins
The following user(s) said Thank You: phillc54, thefabricator03

Please Log in or Create an account to join the conversation.
More
7 years 1 month ago #145182 by rodw
Replied by rodw on topic Center Spot Sheetcam Post

islander261 wrote: Rod

I am sure that without using external hardware (as Keith does) or fast arc voltage monitoring the path to success will be different for HT and TD power supplies. My TD A-60 requires a torch fire signal at least .7s long to get the torch to fire even briefly when using the torch fire button on Plasmac (maybe some knowledgeable TD engineer can weigh in on this) . The OK to Move signal is also very slow, I typically use zero pierce delay up to 10ga steel. I believe that stopping the arc is fairly quick once the torch fire signal is removed. This is sounding like it is time for a little halscope investigation.

John


Thanks John, the intent is to turn on the torch relay, wait until an arc starts, then turn off the arc after the delay expires. That way the lag in turning on is eliminated.
I too thought the TD arcOK was fairly slow.
The following user(s) said Thank You: phillc54

Please Log in or Create an account to join the conversation.
More
7 years 1 month ago - 7 years 1 month ago #145194 by phillc54
Replied by phillc54 on topic Center Spot Sheetcam Post
John,
What is the first arc voltage pulse, is that HF start?

Rod,
The experimental component I posted will do that, for values over 300 the delay is (300 minus value)mS after Arc OK detected.

Edit: Or did you mean after any arc voltage is sensed?
Last edit: 7 years 1 month ago by phillc54.

Please Log in or Create an account to join the conversation.

Moderators: snowgoer540
Time to create page: 0.471 seconds
Powered by Kunena Forum
