Plasmac Post Processors

More
2 years 1 month ago #310286 by phillc54
Replied by phillc54 on topic Plasmac Post Processors
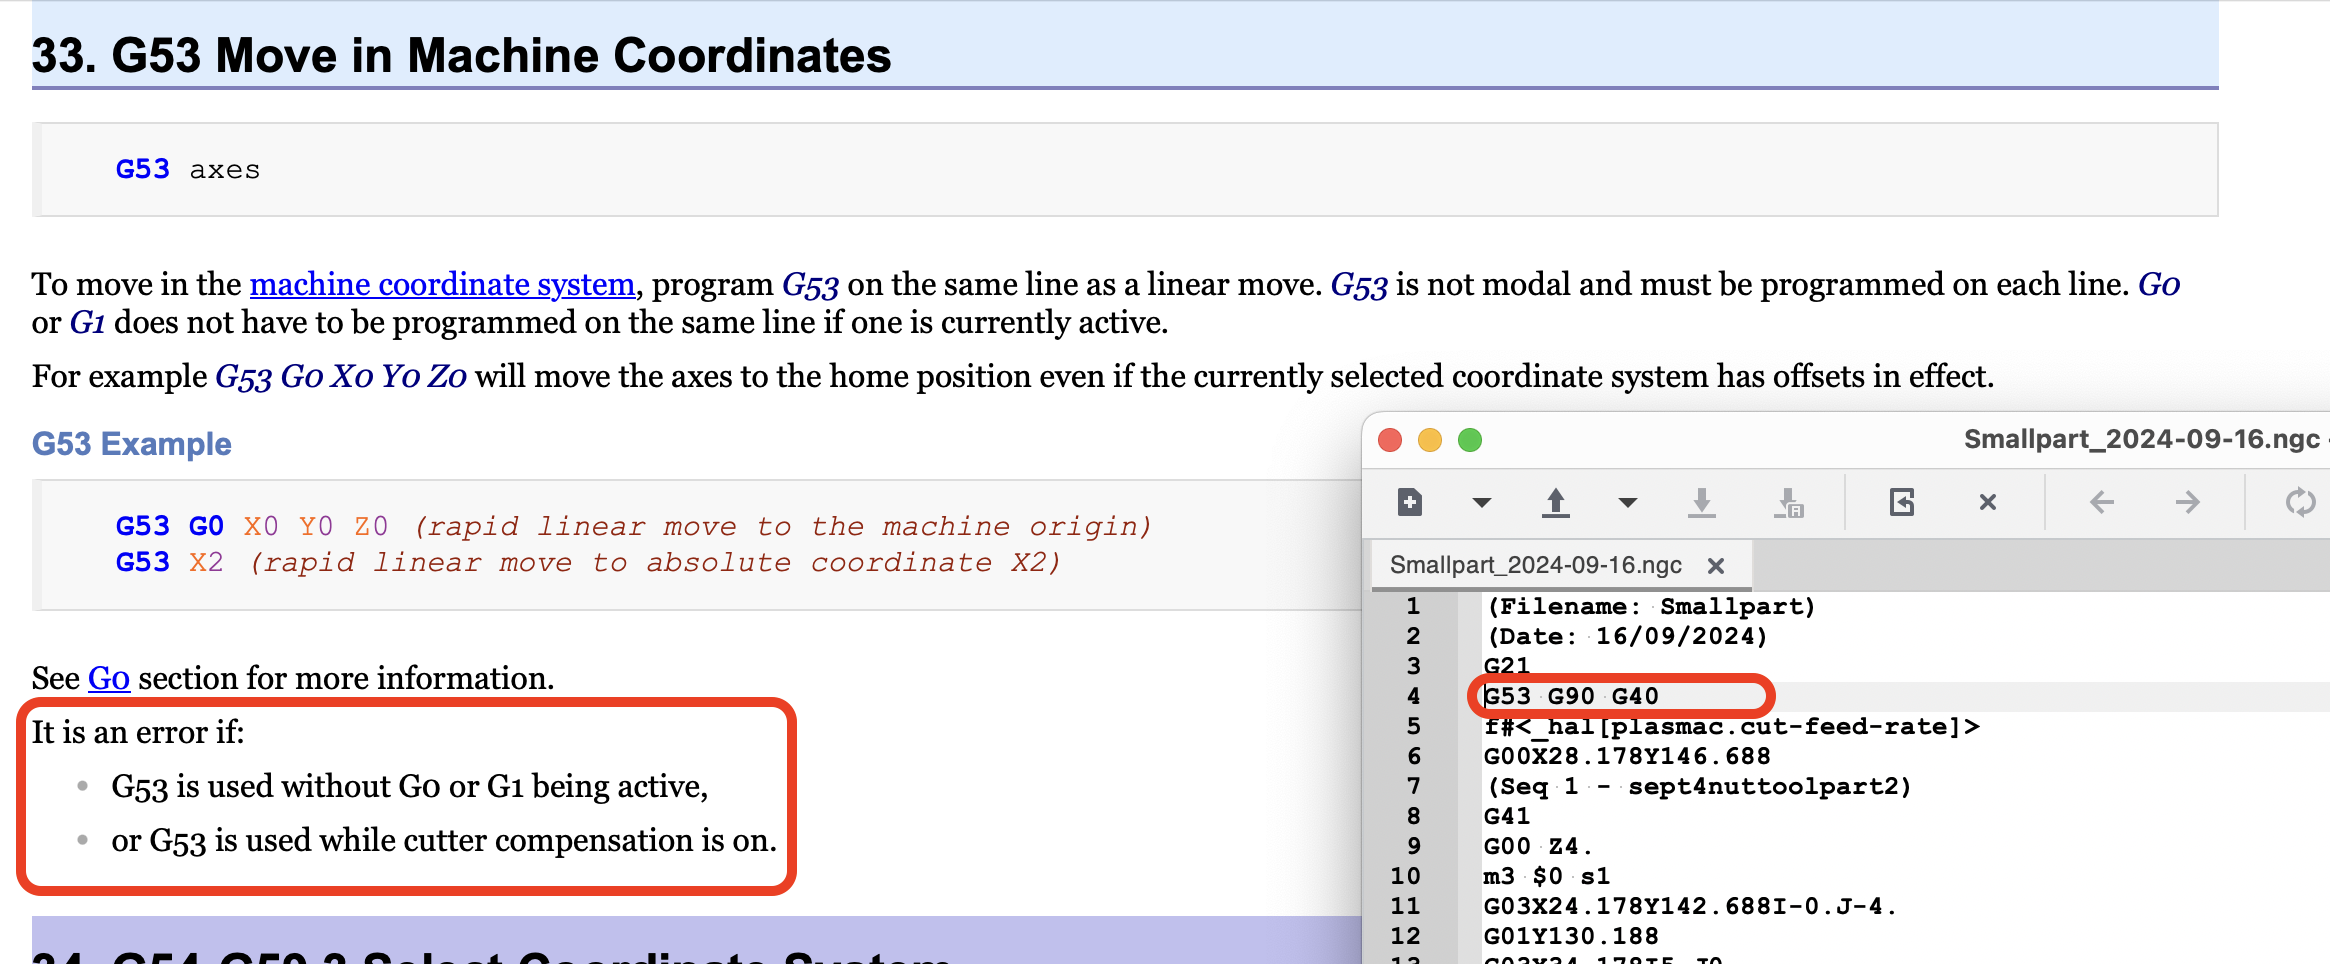
The error is from line #4 in the original gcode:
Warning: Spoiler!

linuxcnc.org/docs/devel/html/gcode/g-code.html#gcode:g53
The following user(s) said Thank You: rodw

Please Log in or Create an account to join the conversation.

More
2 years 1 month ago #310353 by SteveatSteelCut
Thanks, got rid of that error but now there is another one.
Operator error:
G-code error
Radius to end of arc differs from radius to start:
rel_err=97.5794%
I have attached the error.
I have found a lot about this on linuxcnc forums and the solution given is to change the tolerance in linuxcnc:2.4. [RS274NGC] Section
Code:
CENTER_ARC_RADIUS_TOLERANCE_MM =
 n 
It says to add it in the ini file. I can't find where this is meant to go. I tried adding it but it didn't work. I couldn't find this center arc radius tolerance in any of my config files. I tried increasing the accuracy on the cam side but it didn't change anything.


Please Log in or Create an account to join the conversation.

More
2 years 1 month ago #310354 by phillc54
Replied by phillc54 on topic Plasmac Post Processors
A 97% error seems quite large.
Does the PP output the I & J values as absolute or incremental distances? The LinuxCNC default is incremental.
linuxcnc.org/docs/devel/html/gcode/g-cod...ml#gcode:g90.1-g91.1
 

Please Log in or Create an account to join the conversation.

More
2 years 1 month ago #310523 by SteveatSteelCut
I tried lots of different things and in the end I have changed to sheet cam.
I use the nestmaster to create a nest and then use sheet cam to create the gcode for qt plasmac... seems to be a good solution.
The following user(s) said Thank You: rodw

Please Log in or Create an account to join the conversation.

More
1 year 7 months ago #323188 by Bjornstabo
Replied by Bjornstabo on topic Plasmac Post Processors
I am having the same problem with "Radius to end of arc differs from radius to start" with a +90% error rate, using the fusion 360 post. I am able to post out some parts that will run and some that dont. All of theese have previosly been run with no issues on a Mach3 plasma with the same cut settings. Files 1001 and 1005 runs fine. But not 1002 and 1006? Any idea on how to fix this?
 

Please Log in or Create an account to join the conversation.

More
1 year 7 months ago #323693 by Bjornstabo
Replied by Bjornstabo on topic Plasmac Post Processors
SOLVED: Doug solved my problem, now it works great!
 
The following user(s) said Thank You: tommylight

Please Log in or Create an account to join the conversation.

Moderators: snowgoer540
Time to create page: 0.416 seconds
Powered by Kunena Forum