Plasmac Post Processors

More
1 year 4 months ago #330120 by Mcelroy434
Replied by Mcelroy434 on topic Plasmac Post Processors
Hi taloot, I am very new to CNC and am trying to setup my home made machine with QTPlasmaC. This post processor is a .doc file, Fusion is prompting me for a .cps post configuration file. Am I missing another step or something really obvious for how to load this post into my Fusion library? Appreciate any advice!

Please Log in or Create an account to join the conversation.

More
1 year 1 month ago #334833 by mal136
Replied by mal136 on topic Plasmac Post Processors
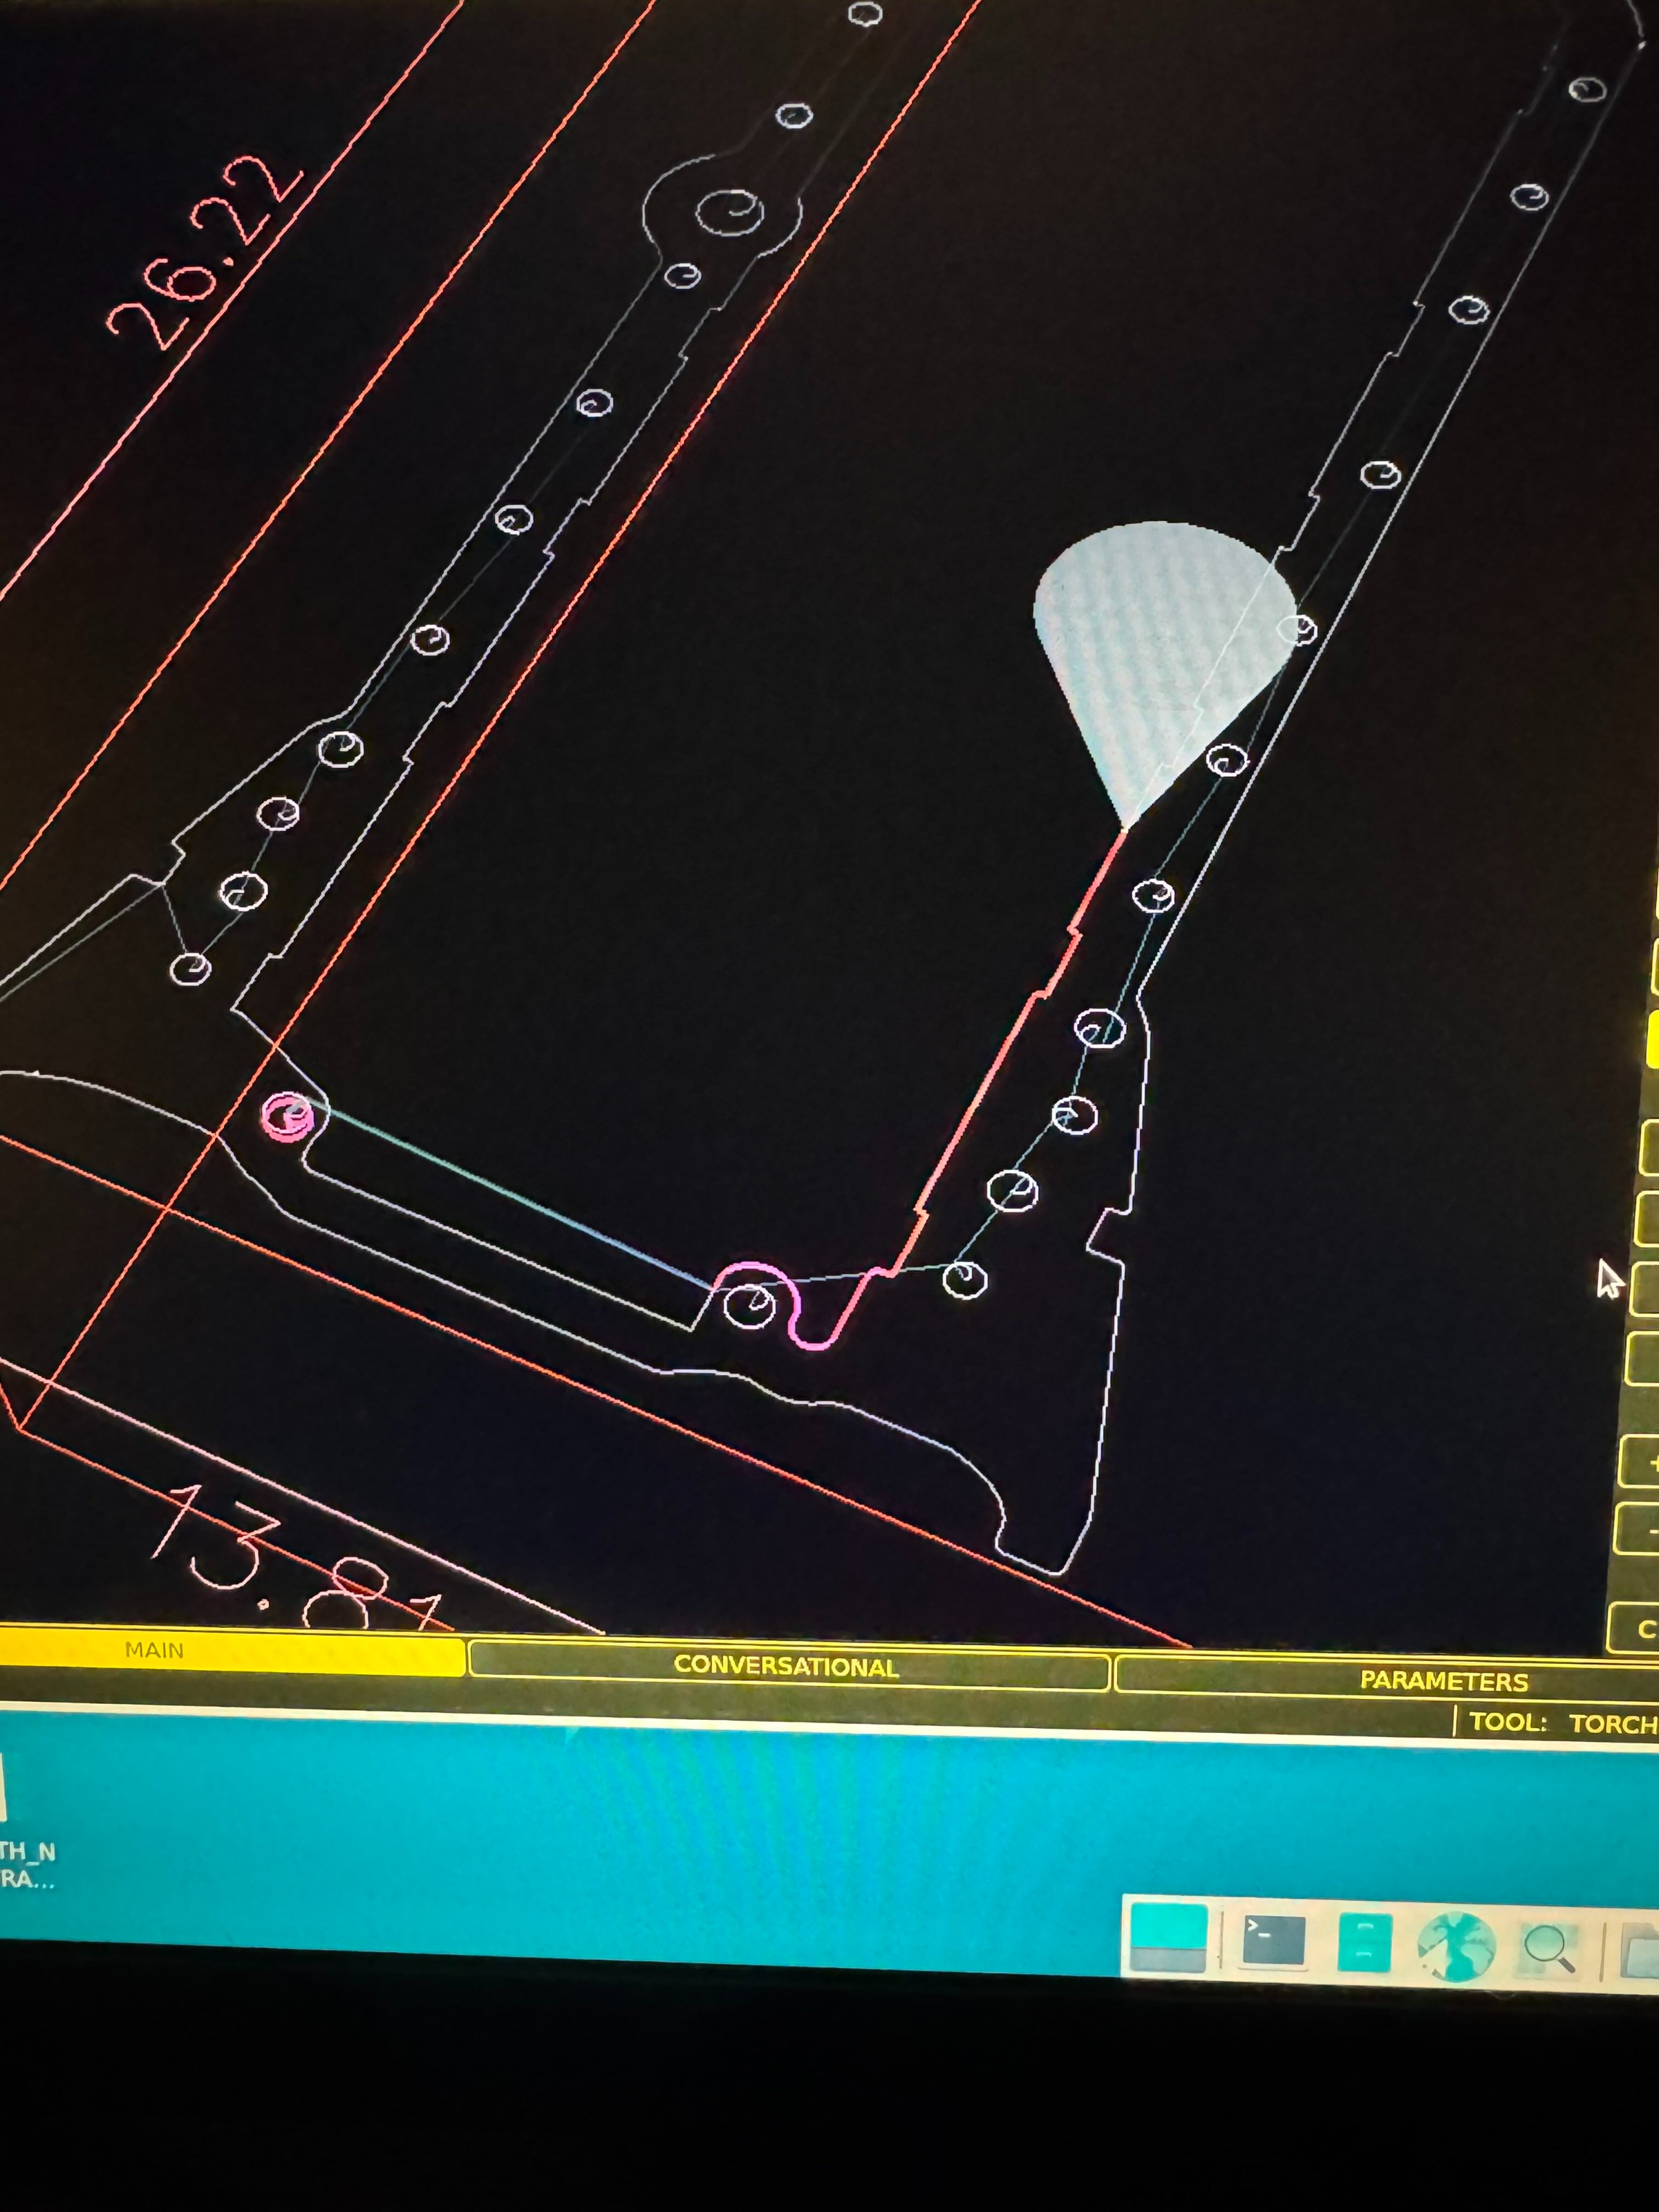
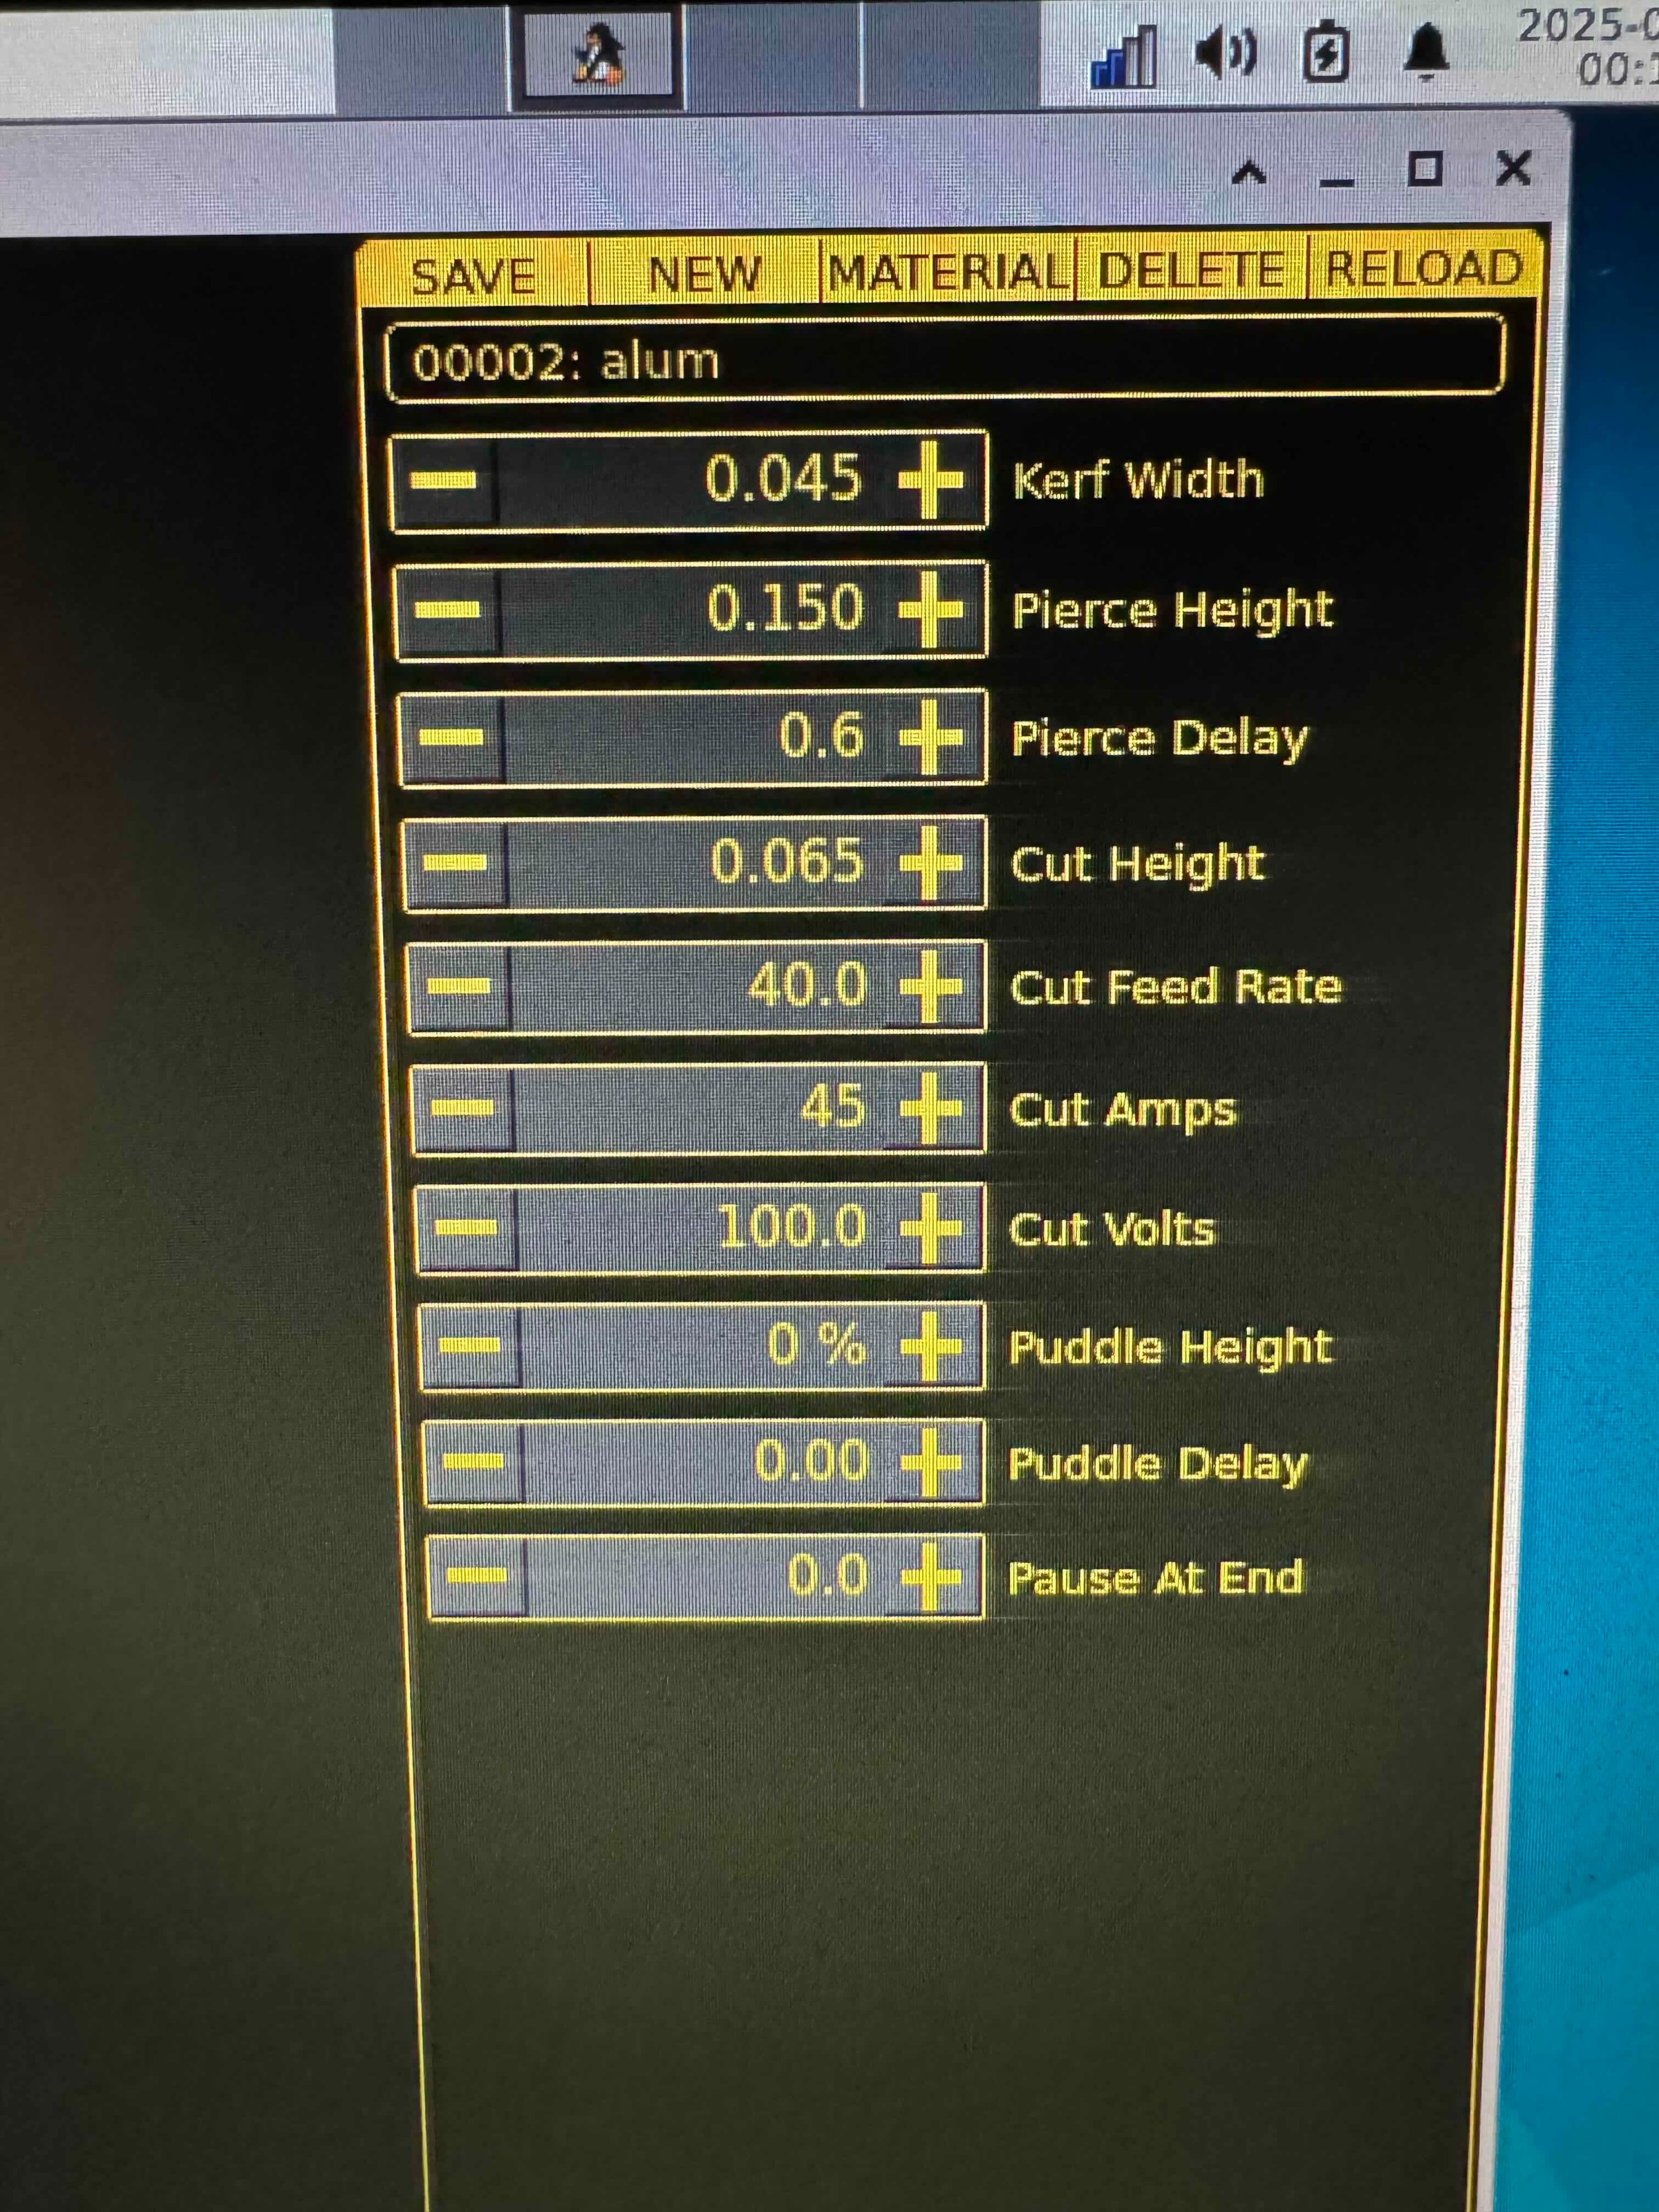
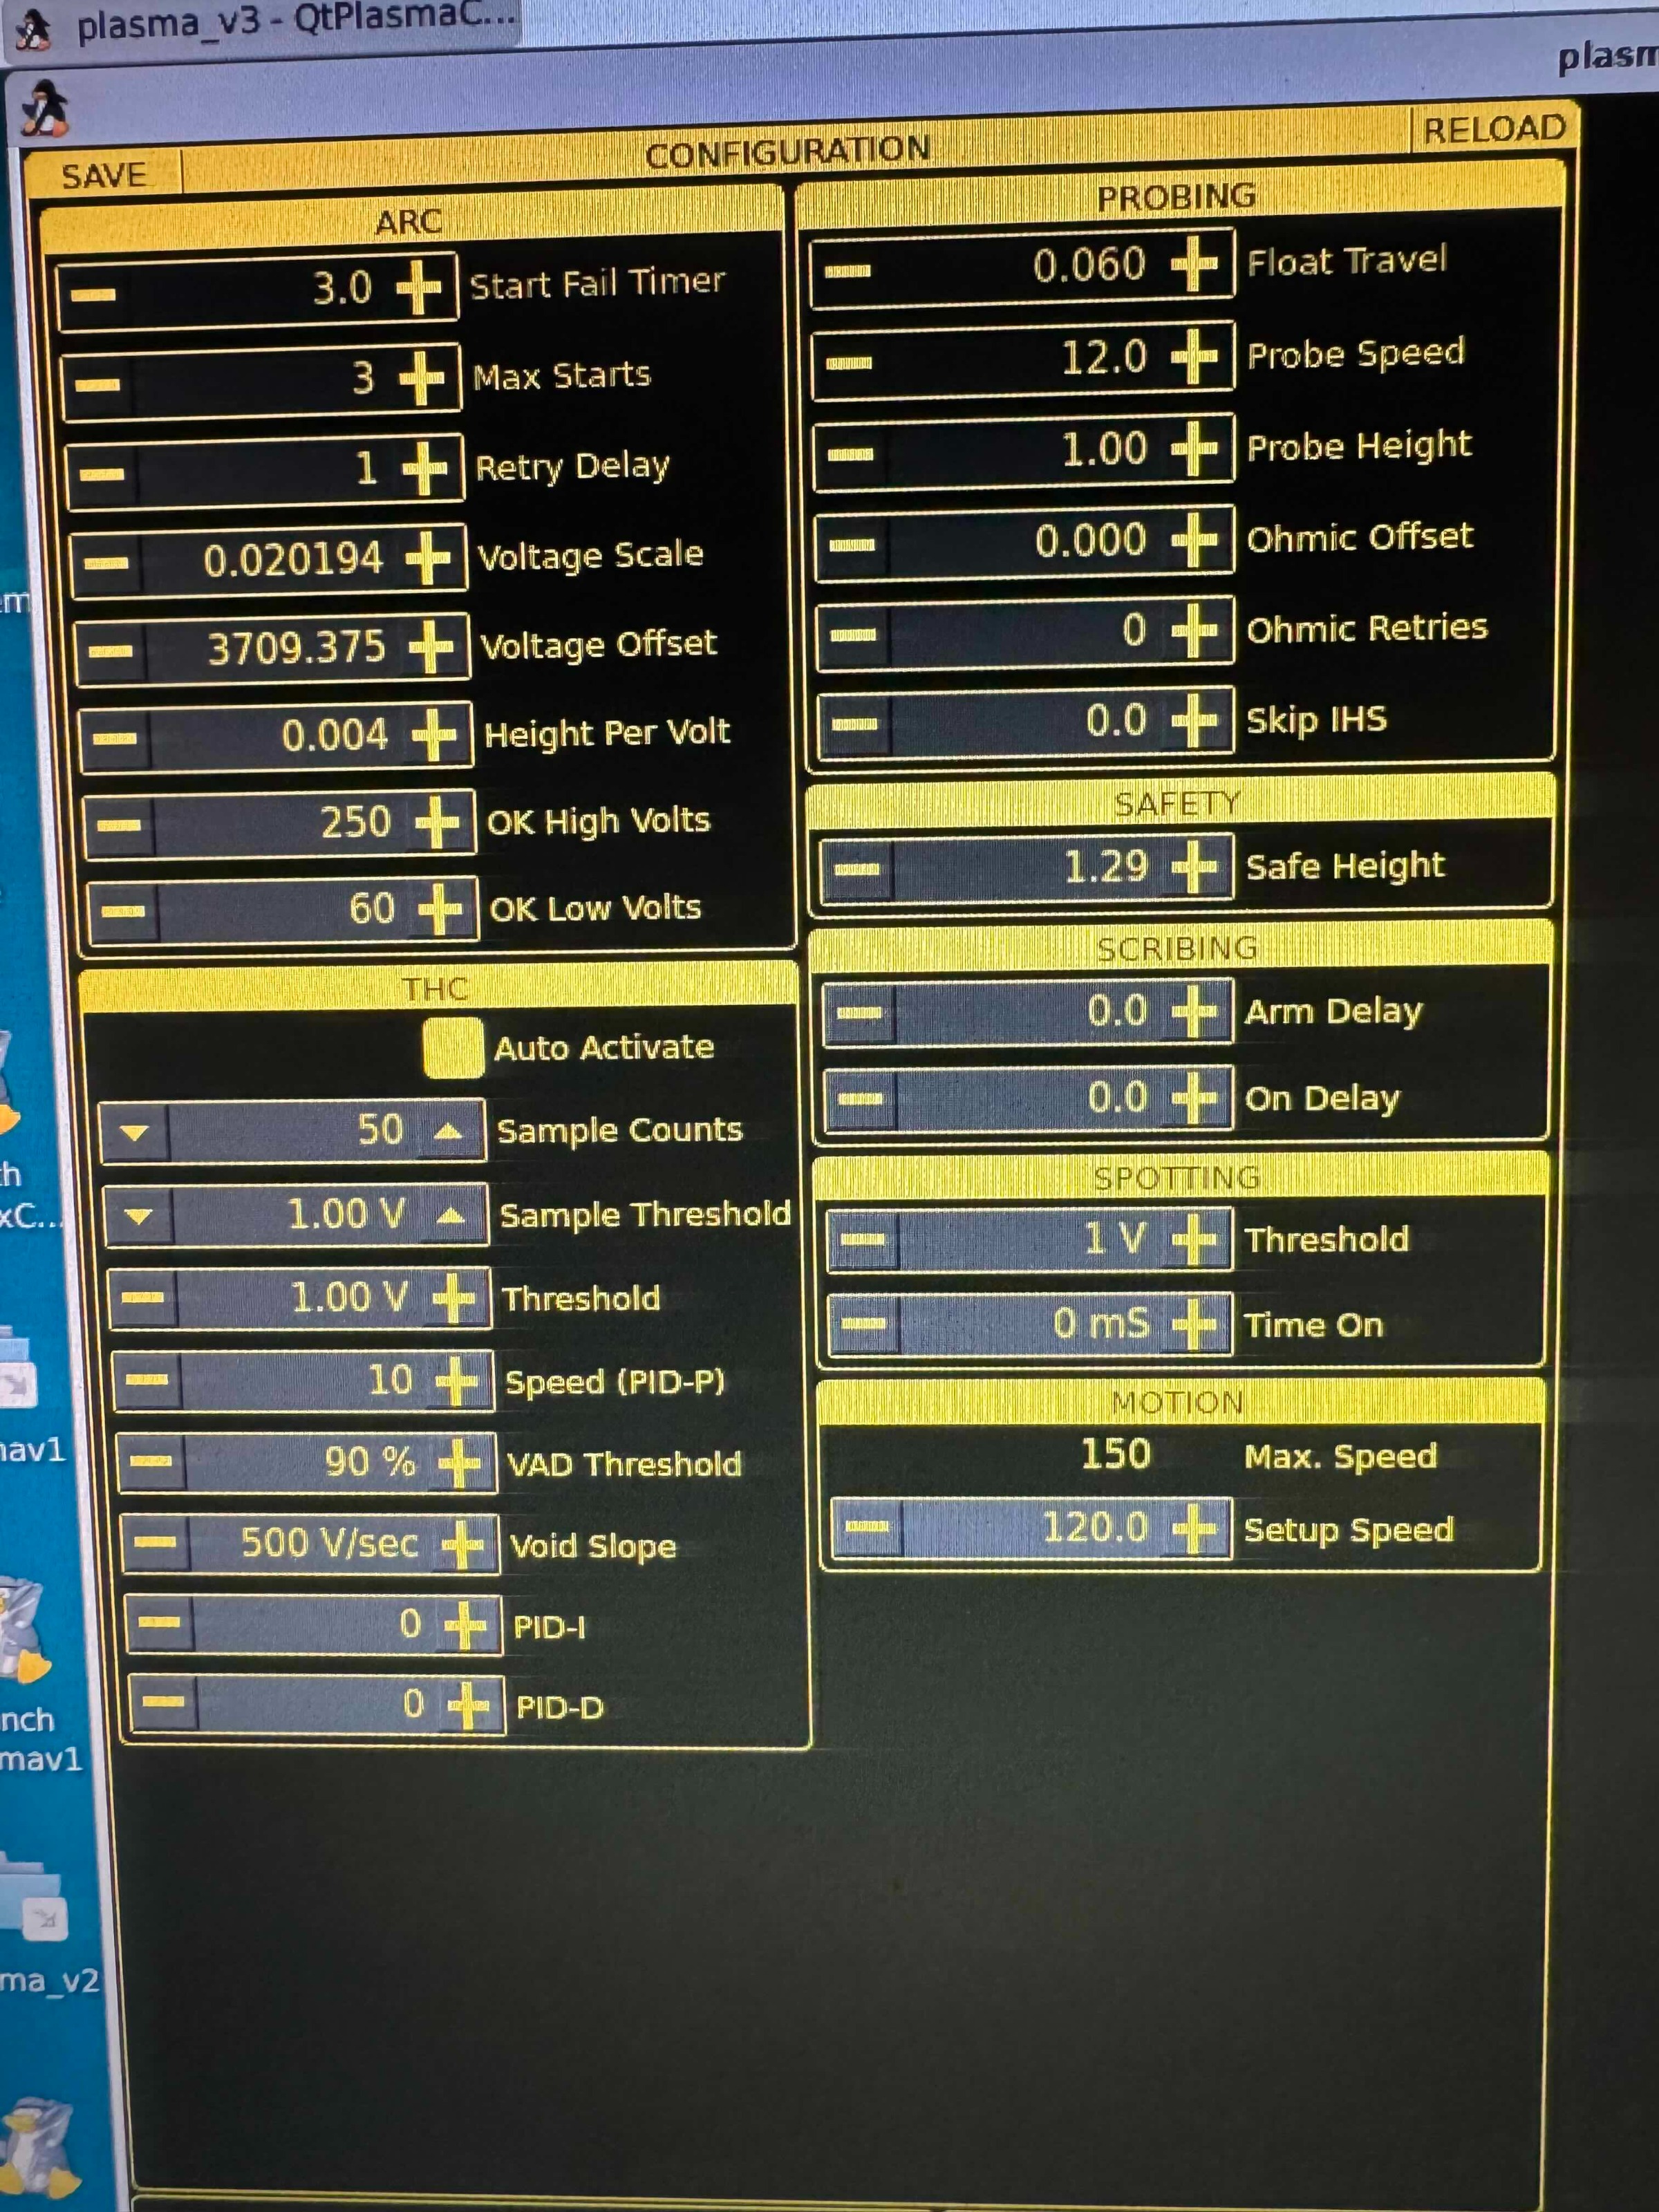
Hello All, I'm using this post processor (PlasmaCv2.1) in Fusion 360. My issue is that my first round hole in the gcode cuts no problem, machine come downs and probes, makes a perfect cut and then the Z axis rises 1-2inches and continues along the path in the gcode but doesn't come back down to start the plasma arc, it just runs the whole program without coming back down to initiate arc and cut the material. I don't get an "arc okay" error which is odd .I went back into Fusion360 and set my retract height and clearance height to 0 to see if that would help and maybe the THC via THCAD through a MESA 7i76 board would work but it just gave me an error. "Safe Traverse Height has been reduced to 0.23in"


Images attached of my cut parameters ,material properties , gcode from Fusion 360 and some misc info. 

The machine cuts simple parts using the conversational in QTplasmaC no problem, and my THC works so I've isolated it to the Fusion 360 Gcode and unsure how to fix my issue. Possible bug maybe?

I feel like I'm doing something really dumb and overlooking something really simple, in an effort to not waste another couple days going in circles, could anyone point me in the right direction, i greatly appreciate it!
 

Please Log in or Create an account to join the conversation.

More
1 year 1 month ago #334836 by tommylight
Replied by tommylight on topic Plasmac Post Processors
There are no
N75 M3 $0 S1
in the gcode after the first piece, and no M5 at the end of the cut except for the first cut.
Those must be added by the post processor.

Please Log in or Create an account to join the conversation.

More
1 year 1 month ago #334914 by mal136
Replied by mal136 on topic Plasmac Post Processors
IInteresting—I used the Fusion360 post processor from the first page of this thread ( forum.linuxcnc.org/plasmac/38438-plasmac...t-processors?start=0 ). After rereading the PDF, it doesn’t explicitly say so, but I think I need to create separate 2D profiles for each feature I’m cutting. Since the post processor doesn’t generate Z movements, would that mean making individual profiles for all 12+ holes plus the part outline? and i assume plasmaC will control Z when it goes to probe for each cut?  I also tried Inkscape (which I like), but it skips certain splines and rounded corners in my parts. Redesigning everything just to fit Inkscape’s gcode output would be counterproductive.

Thank you so much Tommylight for your reply, i greatly appreciate your help!
The following user(s) said Thank You: tommylight

Please Log in or Create an account to join the conversation.

More
1 year 1 month ago - 1 year 1 month ago #334933 by tommylight
Replied by tommylight on topic Plasmac Post Processors
Sorry i can not help with Fusion, i use strictly Inkscape for all plasma machines, just use "prepare for plasma" and then export with the tool chosen as plasma.
Last edit: 1 year 1 month ago by tommylight.

Please Log in or Create an account to join the conversation.

More
2 months 1 day ago #349151 by twatchorn
Replied by twatchorn on topic Plasmac Post Processors
Hi,
I am using Fuson 360 and QtPlasmaC. 
I am having the start radius - end radius errors that I see others have but don't know or understand the remedy. As far as I know I am using the second PP on the list below as when I go to import it, is says it already exists and do I want to cancel or replace. 
Clicking of the first link to QtPlacmac PP does not take we to a file for downloading. Is this PP somewhere and the link needs correcting?

Can someone help with a PP. or with instructions for a dummy on how to not get the errors
Kind regards  Trevor

This thread is for user donated post processors for CAM software that has no native post processer for QtPlasmaC/PlasmaC.
I will make this sticky and unlocked and just keep current versions here.
If there are posted comments or corrections I will delete them after they have been actioned.

Current PP's:
There are no third party PP's here for SheetCam, use the PlasmaC PP included with SheetCam for both QtPlasmaC and Plasmac.

PP creators need to be aware of the following:
  • LinuxCNC does not allows analog/digital input or output while cutter compensation (G41) is active.
  • QtPlasmaC disables G92 offsets.

All work product by the author is provided ​“AS IS”. The Author makes no other warranties, express or implied, and hereby disclaims all implied warranties, including any warranty of merchantability and warranty of fitness for a particular purpose.

Please Log in or Create an account to join the conversation.

Moderators: snowgoer540
Time to create page: 0.313 seconds
Powered by Kunena Forum