Search Results (Searched for: )

  • mh300
03 Mar 2026 08:06
Replied by mh300 on topic Maho MH-400 Retofit
Ja, war direkt mit den Glasmaßstäben, weil ich sowieso den Umbau auf 3-Achs-CNC vorhatte.
Hast du den Original-Vorschubmotor/Scheibenläufer schon gegen einen Servo getauscht? Der Scheibenläufer hat nur einen Tacho und keinen Encoder.
Falls du schon einen Servo hast, sollte das auch via Servo-Encoder machbar sein. Das Nachregeln könnte man allerdings durch entsprechende Reglereinsteellungen auch verhindern (Deadband). Gibt zwar bestimmt einiges an Umkehrspiel durch die ganzen Getriebe, weiß aber nicht, ob das bei den Trapezspindeln noch groß ins Gewicht fällt.
  • Giovanni
03 Mar 2026 07:50
Replied by Giovanni on topic Probleme mit NativeCam
Here it seems to work as expected.
Could you describe the error, or attach a screenshot?

Regards
Giovanni
  • Muecke
03 Mar 2026 06:46
Replied by Muecke on topic Forum Fehler, ... :-(
Ich habe es gerade auf der Arbeit probiert, auf einem anderen PC, und auch dort kann ich in die Themen nichts mehr antworten, ohne die Fehlermeldung zu erhalten.
Warum kann ich das in diesen Themen?
=>  400V Servo (51 Nm) mit EtherCAT / CiA402 in LinuxCNC – bezahlbarer Drive gesucht - LinuxCNC
und 
=>  Umstieg von LinuxCNC + Mesa auf EtherCAT (Leadshine EL8 / Beckhoff) – Erfahrunge - Page 2 - LinuxCNC

 
  • Muecke
03 Mar 2026 06:06
Replied by Muecke on topic Forum Fehler, ... :-(
Ich habe so etwas nicht. :-( Und bei mir funktionieren zwei Browser nicht. Handy und Tablet gehen auch nicht. :-( 
  • T_D
03 Mar 2026 06:01
Replied by T_D on topic Probleme mit NativeCam
 

File Attachment:

File Name: mh500cnc2.zip
File Size:37.45 KB
  • T_D
03 Mar 2026 05:35
Replied by T_D on topic Probleme mit NativeCam
I am using a milling maschine, i am New to linuxcnc and the editing of files , ist that possibly the problem that i User the default files ?
  • hitchhiker
03 Mar 2026 04:27 - 03 Mar 2026 05:39
I got it work with a own component to make 1 move from position to position forwaes with lock backward and reduce pwm.

But the turret can only travel to next position in forward.

If i am on tool 5 and i want tool 1.. i need 2 times the move.
Is it possible to do this in the component with a abs function?

what i mean... i must handle the rollover=

presenttoolslots 6
currenttool is 6
calledtool is 1
Turretmoves = calledtool - currenttool = -5
Commandedmoves= presenttoolslots - (abs) turretmoves

next step is the to count every move.
moved = i++
if moved == commandedmoves
toolchange done

Sounds ok?!

I do the coordination of the forward and backward stuff with 2 time delays. On the end i set the pwm value lower to lock agoinst the pawl with lower current to not blow the dc motor.


Thanks
  • sivaraj
03 Mar 2026 02:48
Based on the data provided, if the motor is a permanent magnet type, it is likely in the range of approximately 7.5 kW (or max 11 kW)

From the peak data shared, I estimate that the motor’s rated current at stall torque would be around 50A. Accordingly, you may need to consider a universal drive rated at approximately 50A.. This will be around 22kw

Can you verify whether the motor nameplate specifies a rated voltage 400V, or is this value being assumed based on the drive input power?
  • tcbmetalworks
03 Mar 2026 02:42
Replied by tcbmetalworks on topic QTPLASMAC integrated cad/cam
Got my first cuts made with it today, took a while to get the gcode to work correctly with qt plasma c
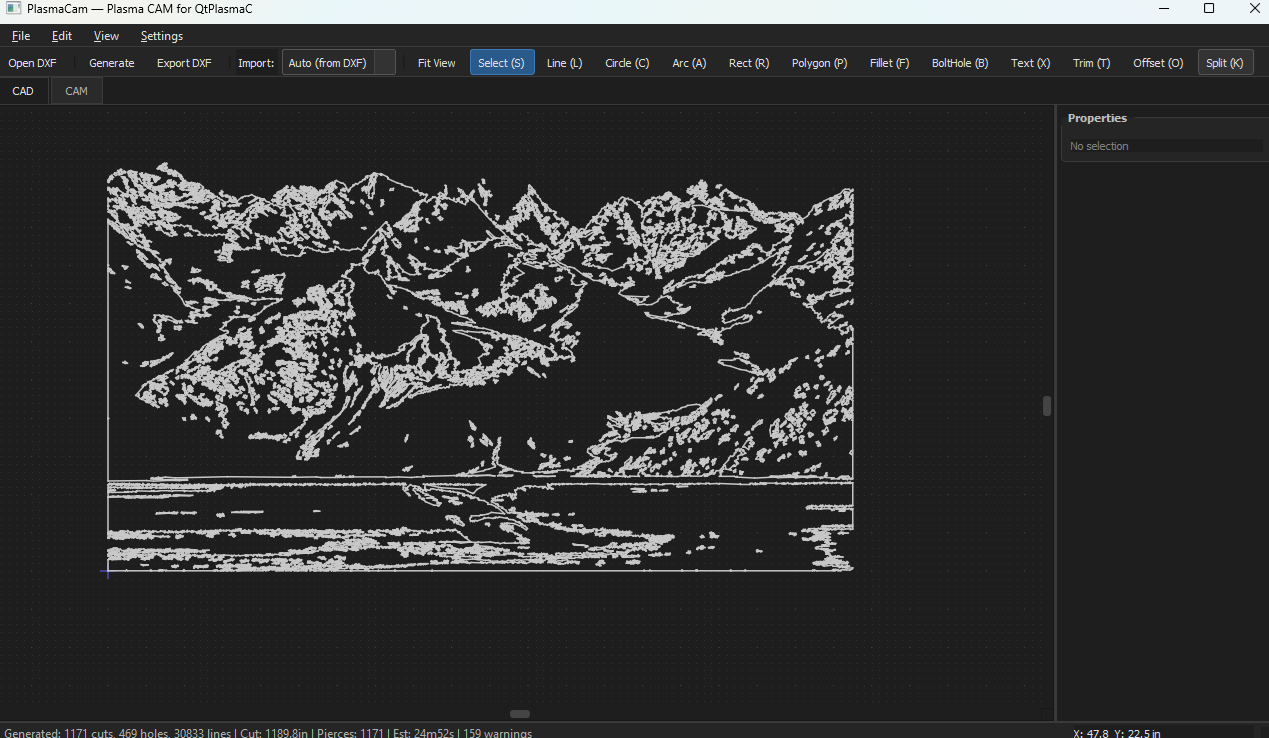
We also added a image to dxf function, still needs some work but its a start. 
I added a kerf width calculation wizard... cut out a test piece input the actual cut size vs the wanted cut size and it calculates what your kerf width is spoused to be. I did a install on a friends computer and some of the install seems broken, need to make it more shareable if anyone else wants to easily use it. Not to shabby tho for only being 2 weeks into the project part time.  
  • tommylight
03 Mar 2026 00:50


i have here a l298n modul and a mesa 7i92 with bitfile adjusted to have pwm and 2 gpios for setting direction.
You could start by having a look at the "etch a sketch" config included with LinuxCNC, it is for parallel port so needs changing pin names to Mesa, and it is for L298.
Probably doing some timing stuff in hal using timedelay and/or oneshot and maybe flip-flop ....
  • rodw
03 Mar 2026 00:21
Replied by rodw on topic XHC WHB04B development?
Reading something today. Maybe try using smp affinity to lock the USB interrupt to  Core1 (away from core 0 housekeeping) and assuming > 2 cores. You can find the interrupt by
cat /proc/interrupts | grep -i usb

Then follow one of the many posts about cpu affinity for networking. Just remember you need to reset this on every boot.
  • tommylight
02 Mar 2026 23:09
Replied by tommylight on topic Forum Fehler, ... :-(
I use "dark reader" and since 3 days ago it does not allow me to reply to anything here without disabling it.
  • tommylight
02 Mar 2026 23:08
Replied by tommylight on topic New Laser Build - raster engraving
Yes and no, sorry my bad, i thought i uploaded the new config there, so thank you for reminding me.
I did upload the new config there and added some more info at the top, so have a look at your own leisure.
These are also new machines i have built and use the same configs for PWM and here i did upload the new configs.
forum.linuxcnc.org/show-your-stuff/46752...ver-etcher-scratcher
  • tommylight
02 Mar 2026 22:53 - 02 Mar 2026 22:58
Latest config with provisions for disabling PWM on program pause or stop and enabling on resume.
Edit:
Attached the latest config to the first post, also.
  • rdtsc
02 Mar 2026 21:07
Replied by rdtsc on topic New Laser Build - raster engraving
Tommy are you talking about the engravertest.zip?
Displaying 6226 - 6240 out of 11376 results.
Time to create page: 0.277 seconds
Powered by Kunena Forum