Homemade CNC Plasma - hypertherm, Mesa, gear drives, nema 34.

More
1 year 4 months ago #331061 by Daan96
Looks good!
I'm following ;)
The following user(s) said Thank You: RNJFAB

Please Log in or Create an account to join the conversation.

More
4 months 1 week ago - 4 months 1 week ago #347180 by RNJFAB
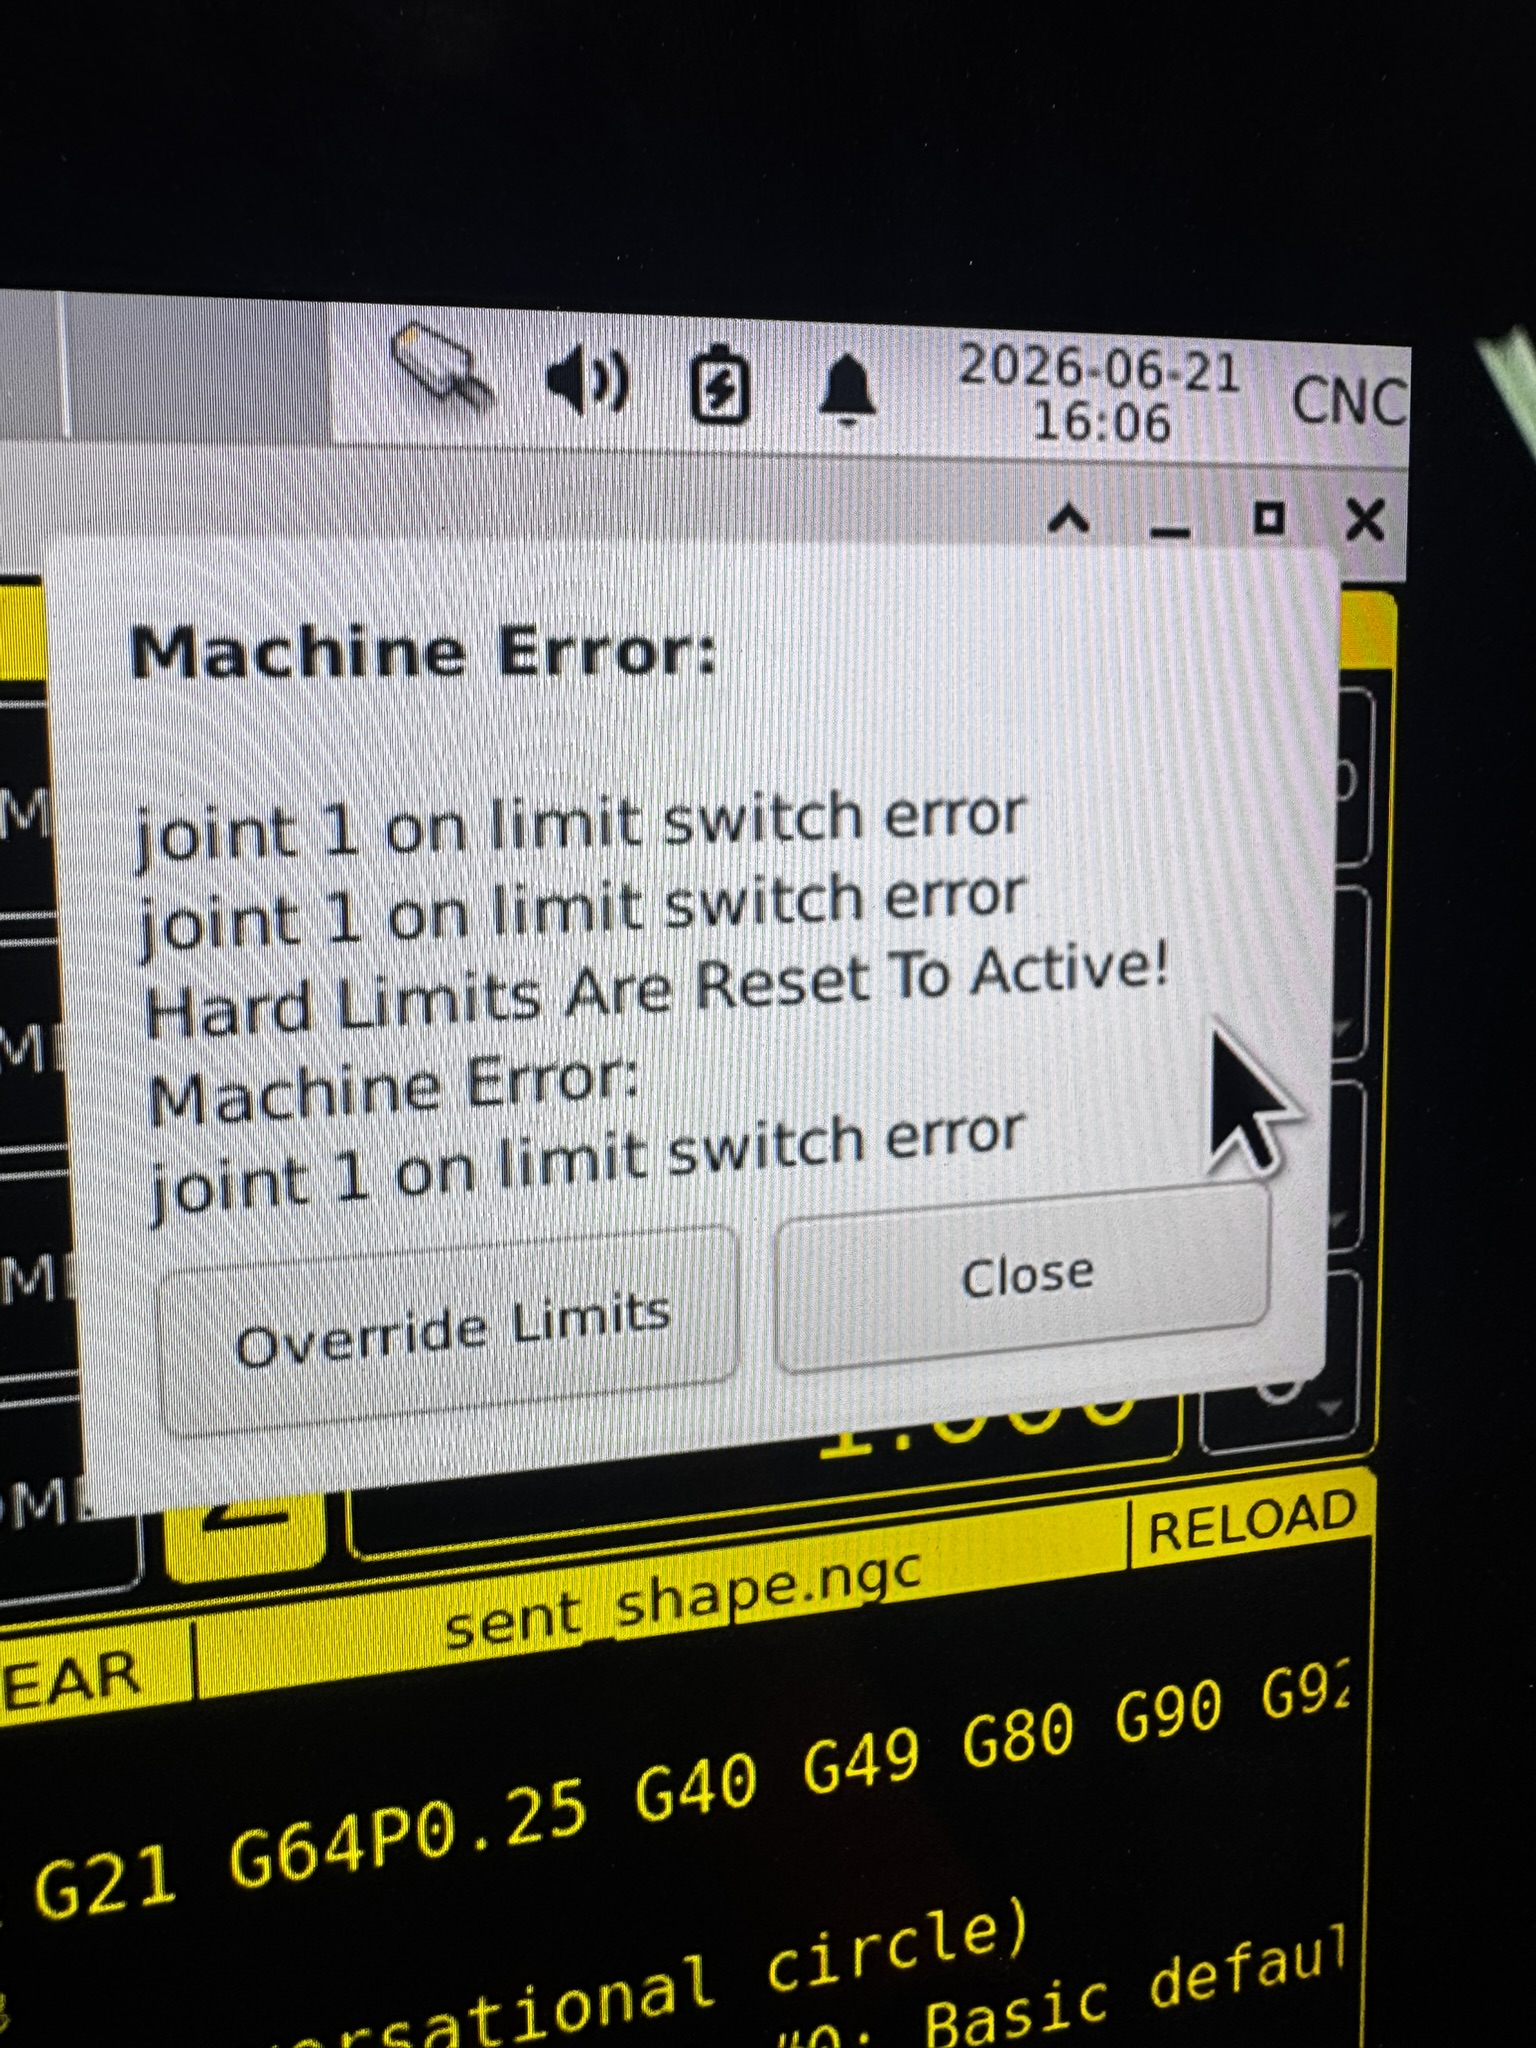
Over a year of flawless cutting, new issues today. 
It has been creeping in for a few weeks now. Occasionally, then every day, then ever cut, now every pierce. And now impossible to cut anything. 
Doing my head in why it appeared. 

Because I'm useless at linux and the cnc has no internet connection, getting anything on the computer is a mission. So, I have not updated linux in years. 

Any ideas? things that may have changed? 

Am I just overthinking this and just need to bump the debounce from 5 to 7?
Last edit: 4 months 1 week ago by RNJFAB.

Please Log in or Create an account to join the conversation.

More
4 months 1 week ago #347183 by rodw
At a guess, something has changed slightly with a home switch and its left triggered. Try editing your HOME_OFFSET on joint 1 in your ini  file and make it a bit bigger, maybe by 0.5 to 1.0 mm. This should move the sensor away a bit  more after homing. Ohh and check for anything loose. 
The following user(s) said Thank You: RNJFAB

Please Log in or Create an account to join the conversation.
More
4 months 1 week ago #347193 by tommylight
The following user(s) said Thank You: RNJFAB

Please Log in or Create an account to join the conversation.

More
4 months 1 week ago #347199 by RNJFAB
Thanks guys,
Triggers most when the following criteria are met. move to location-touch off-pierce =ERROR.
Then I can often tell it to start again and it will pierce and continue on its way. However it will ERROR after it cuts a little.
Yes triggers on pierce. 
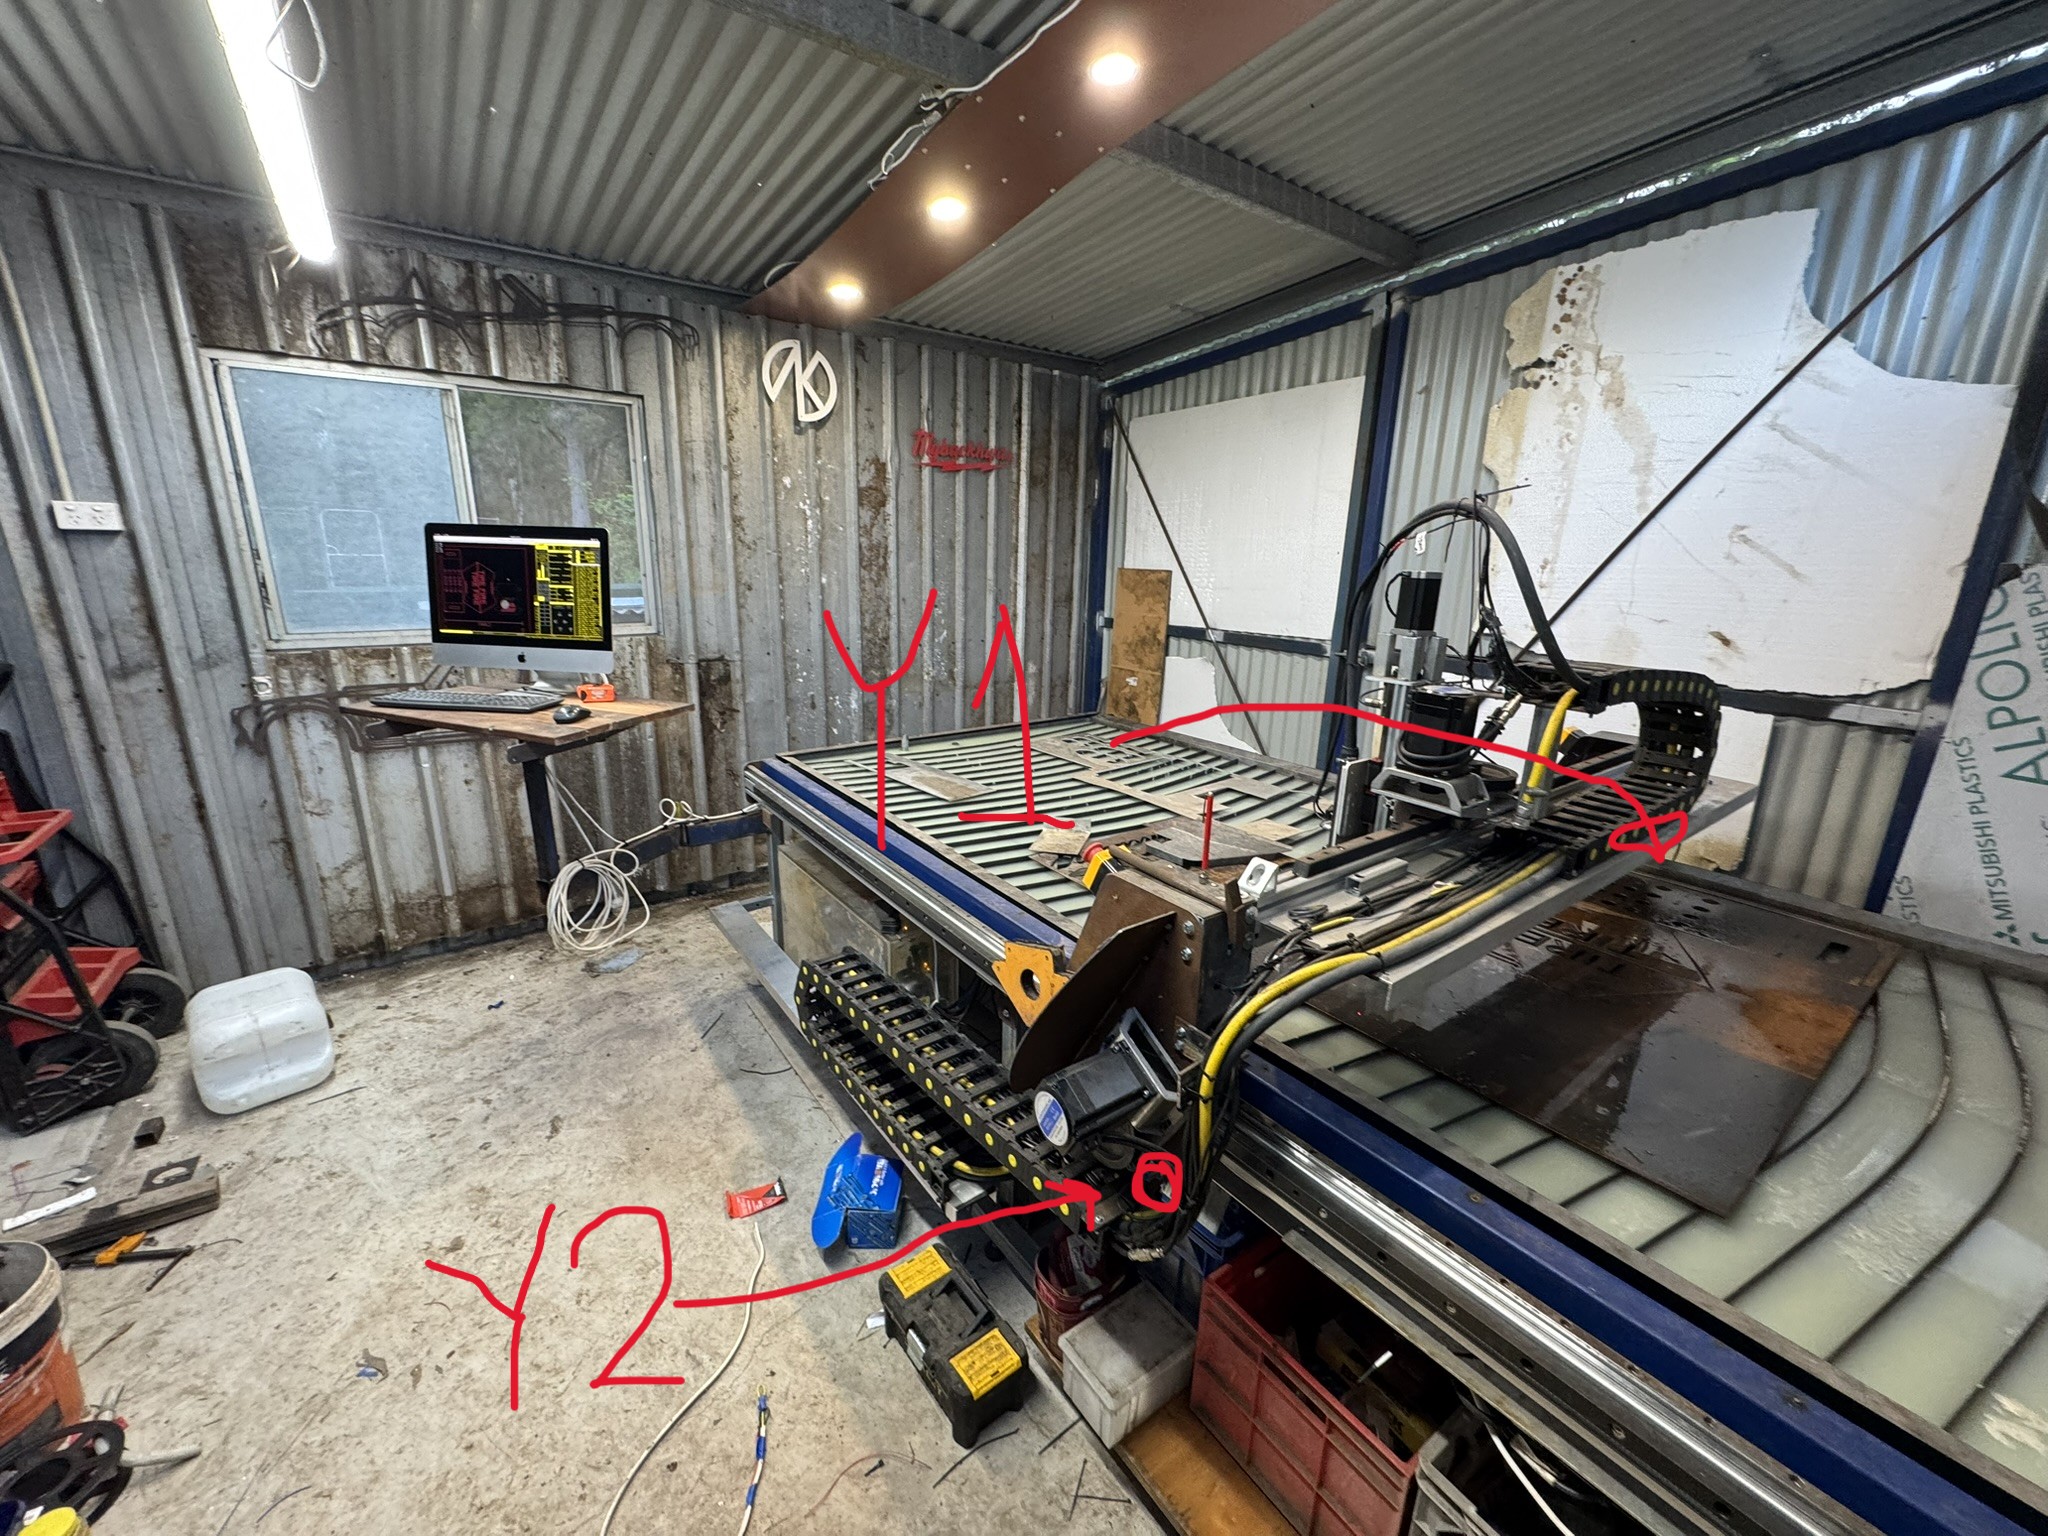
I'm cutting in the middle of the table. The joint 1 sensor is a proximity sensor that is below the left side of the table. 

Please Log in or Create an account to join the conversation.
More
4 months 1 week ago #347200 by tommylight

Yes triggers on pierce. 
95% interference/shielding/grounding issue
5% brownout due to inadequate wiring in the shop and the subsequent voltage drop when plasma goes from pilot to cut
Since it was OK and lately developed this, first thing to check is shop grounding, earth dries up and does not conduct properly or at all.
-
Had the same issue a few years back at a client, i kept telling him the above, but he did reject that as reasonable so i asked him to wire machine ground to the water line as i recalled he has metal water pipes in the ground, never ever complained again.
The grounding rods are way to close to the surface if this happens to be the issue.
For the 5%, use a DVM with memory and check where does the voltage fall to when plasma triggers.
Might also be the power supply caps are drying up.
For interference, a scope would be nice, but you can use a DVM set to manual AC voltage range and measure between GND points and metal case and/or metal machine parts. If you get any reading above 5-10V, that is not OK so grounding and shielding must be corrected. Although i have seen machines with 60V still working properly, but i would not risk it, ever.
The following user(s) said Thank You: RNJFAB

Please Log in or Create an account to join the conversation.

Time to create page: 0.101 seconds
Powered by Kunena Forum
