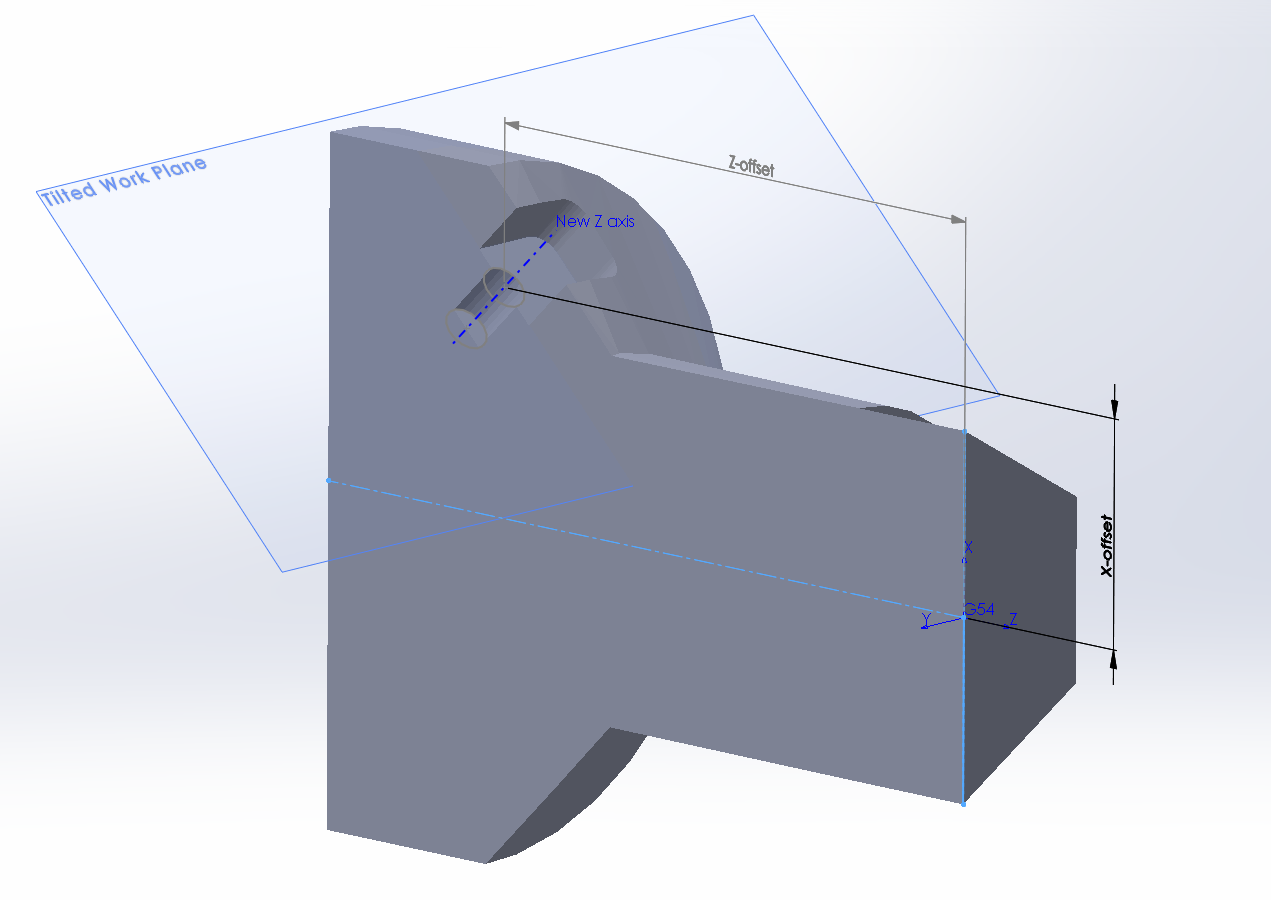
Here is the promised sim config:
To test:
1. unzip
2. 'halcompile --install' the enclosed 'mazak_integrex_200y_kins.comp'
3. start 'mazak-integrex-200y' config and run the preloaded gcode program
If you have any questions, which is likely, just ask.
Text from the enclosed README file:
Code:
Experimental simulation of a 5axis Mill/Turn machine (eg MAZAK Integrex 200Y)
Implemented Gcodes:
- 'G67 B': Moves the B-axis to the 'B'-word position and activates 'HALF TCP Lathe' mode.
- 'G68 B (X Y Z)': Moves the B-axis to the 'B'-word position then defines and activates a work plane perpendicular the this current tool orientation with the origin at the current WCS (optionally offset by any [X,Y,Z]-Words). This will change WCS to 'G59' where the transformed work offset values have been written to (ie the prior values stored in G59 will be lost!).
- 'G68.1 (X Y Z)': Defines and activates a work plane perpendicular the the current tool orientation with the origin at the current WCS (optionally offset by any [X,Y,Z]-Words). For change to WCS see 'G68'
- 'G69': Cancels the work plane set by 'G68' and (currently) switches back to 'G54'.
NOTES:
- This config defines the work-spindle as '$0' and the tool-spindle as '$1'. Example: 'M19 $1 R90' will orient the tool-spindle to 90°. (For real hardware it is recommended to use the spindle encoder-position instead of using 'spindle.1.orient-angle'.)
- 'HALF/FULL TCP MILL/LATHE' modes include tracking of tool-spindle rotation.
- 'HALF TCP MILL/LATHE' modes do not track the work spindle rotation, this is intended behavior.
- 'FULL TCP MILL' mode will track all rotations.
- Tool-offsets must only be changed in 'Identity' mode as it may cause sudden joint movements otherwise.
- Lathe tools must only be used in 'Identity' or 'HALF TCP Lathe' mode.
- Mill tools must only be used in 'HALF/FULL TCP Mill' or 'TWP' mode.
- Due to easier abort handling we currently restrict the use of twp to G54 as LinuxCNC seems to revert to G54 as the default system.
Abort behavior can be handled by using a subroutine defined in the ini file under [RS274NGC]ON_ABORT_COMMAND'.
- The TWP remap code in this config does not implement virtual rotations (ie no optional 'R' word).