Planning to Retrofit a Mazak Integrex200Y Mill-Turn Machine

More
1 year 5 months ago - 1 year 5 months ago #328544 by Aciera
That is because the PP uses G18 to rotate the coordinate system for milling.
Have you tried setting the rotational axis to Z as suggested here:
forum.linuxcnc.org/10-advanced-configura...hine?start=50#327942

The underlying problem is that linuxcnc applies the x-,y-z- tool-offsets internally, so the tool-length is automatically subtracted from the Z position shown in the DRO. That is why the kinematic model for milling has the tool spindle pointing in the negative machine Z direction and the model for turning has it pointing in the negative X direction.
While it might be possible to remove the tool-offset as linuxcnc applies them and add them to different axes in the kinematic I'm rather skeptical that it is worth the effort.
You need to remember that the planner currently has no information about the custom kinematic used, neither does the preview. The nice thing about TWP is that you can load any G17 XYZ milling toolpath and it will be displayed correctly in the screen.
Generally speaking limit violation checking and tool path preview will only be of limited use for more complex kinematics.

Note though that limit values can be changed when changing kinematic modes. For an example see:
github.com/LinuxCNC/linuxcnc/tree/master...xis/vismach/millturn

The actual values are changed using executable Mcodes:
github.com/LinuxCNC/linuxcnc/tree/master...mach/millturn/mcodes
Last edit: 1 year 5 months ago by Aciera.

Please Log in or Create an account to join the conversation.

More
1 year 5 months ago #328570 by jochen91
Thanks for the input. The softlimit not working with joint limits just with axis limits is sad :(I tried to include to millturn limit changer but LCNC reports: Unknown M code used. I assume somethings not right in the .ini ? Also is it possible to change the key binding dependent on TWP is active or not?

Also: How can a custom component can be executed from a custom M-Code? Background is, that a custom g code or m code is needed to rotate and lock the tool spindle. I feel comfortable creating my own component, but how to execute it from within m code i don't know.

Thank you and kind regards,
Jochen
 

Please Log in or Create an account to join the conversation.

More
1 year 5 months ago #328576 by Aciera
- You need to mark the files 'M128' and 'M129' as executable (rightclick-> Properties -> Permissions).

I don't know about changing the key binding at run time but I would strongly advise against using keybord bindings to jog the actual machine. Much better to use hardware panel buttons connected to realtime hardware inputs.

Not sure what you mean by 'executing' a custom component. A 'custom component' refers to something that runs in HAL and as such runs periodically.
linuxcnc.org/docs/html/hal/comp.html

Do you maybe mean a 'remap' to create/redefine a g- or m-code?
linuxcnc.org/docs/html/hal/comp.html

Please Log in or Create an account to join the conversation.

More
1 year 4 months ago - 1 year 3 months ago #330614 by jochen91
Hello,

im sorry for being a long time without news.

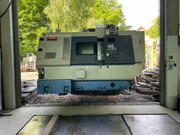
I bought the Machine and transported it to my location. At the moment I am trying to make everything work under the old Fusion640MT control.
Sadly i realized, that the milling spindle seen better times. Runout is quite high, and the bearings sound not good. I'm in the process of getting it fixed.

After i checked as many functions as i can with the old control, i will start the retrofit. The questions i have for now:

Shall i continue this thread or open a new one in the right subforum for the retrofit itself ?
Last edit: 1 year 3 months ago by jochen91.
The following user(s) said Thank You: besriworld

Please Log in or Create an account to join the conversation.

More
1 year 4 months ago #330615 by jochen91
The following user(s) said Thank You: besriworld

Please Log in or Create an account to join the conversation.

More
1 year 4 months ago - 1 year 4 months ago #330617 by jochen91
And finally a tiny video:

Last edit: 1 year 4 months ago by jochen91.
The following user(s) said Thank You: besriworld, Aciera

Please Log in or Create an account to join the conversation.

Time to create page: 2.714 seconds
Powered by Kunena Forum