Hello everyone,
over the past few weeks we have been able to fix several bugs—mostly in the software—so that the machine is now ready for milling, even without the tool changer.
We are currently working on the tool changer and have been able to learn a great deal from the LinuxCNC documentation and successfully implement what we’ve learned.
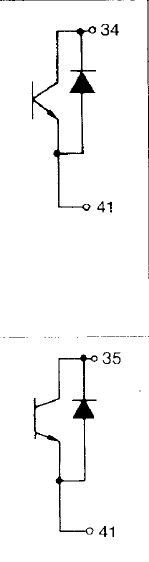
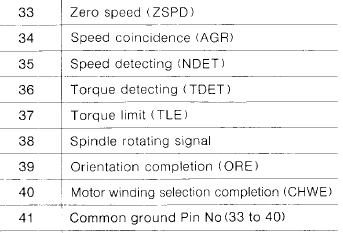
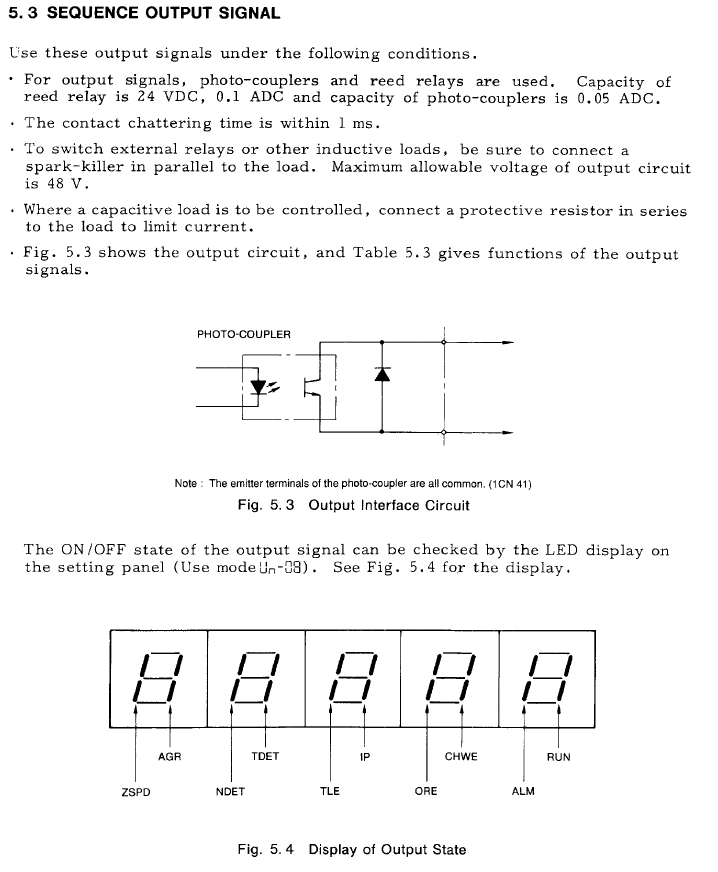
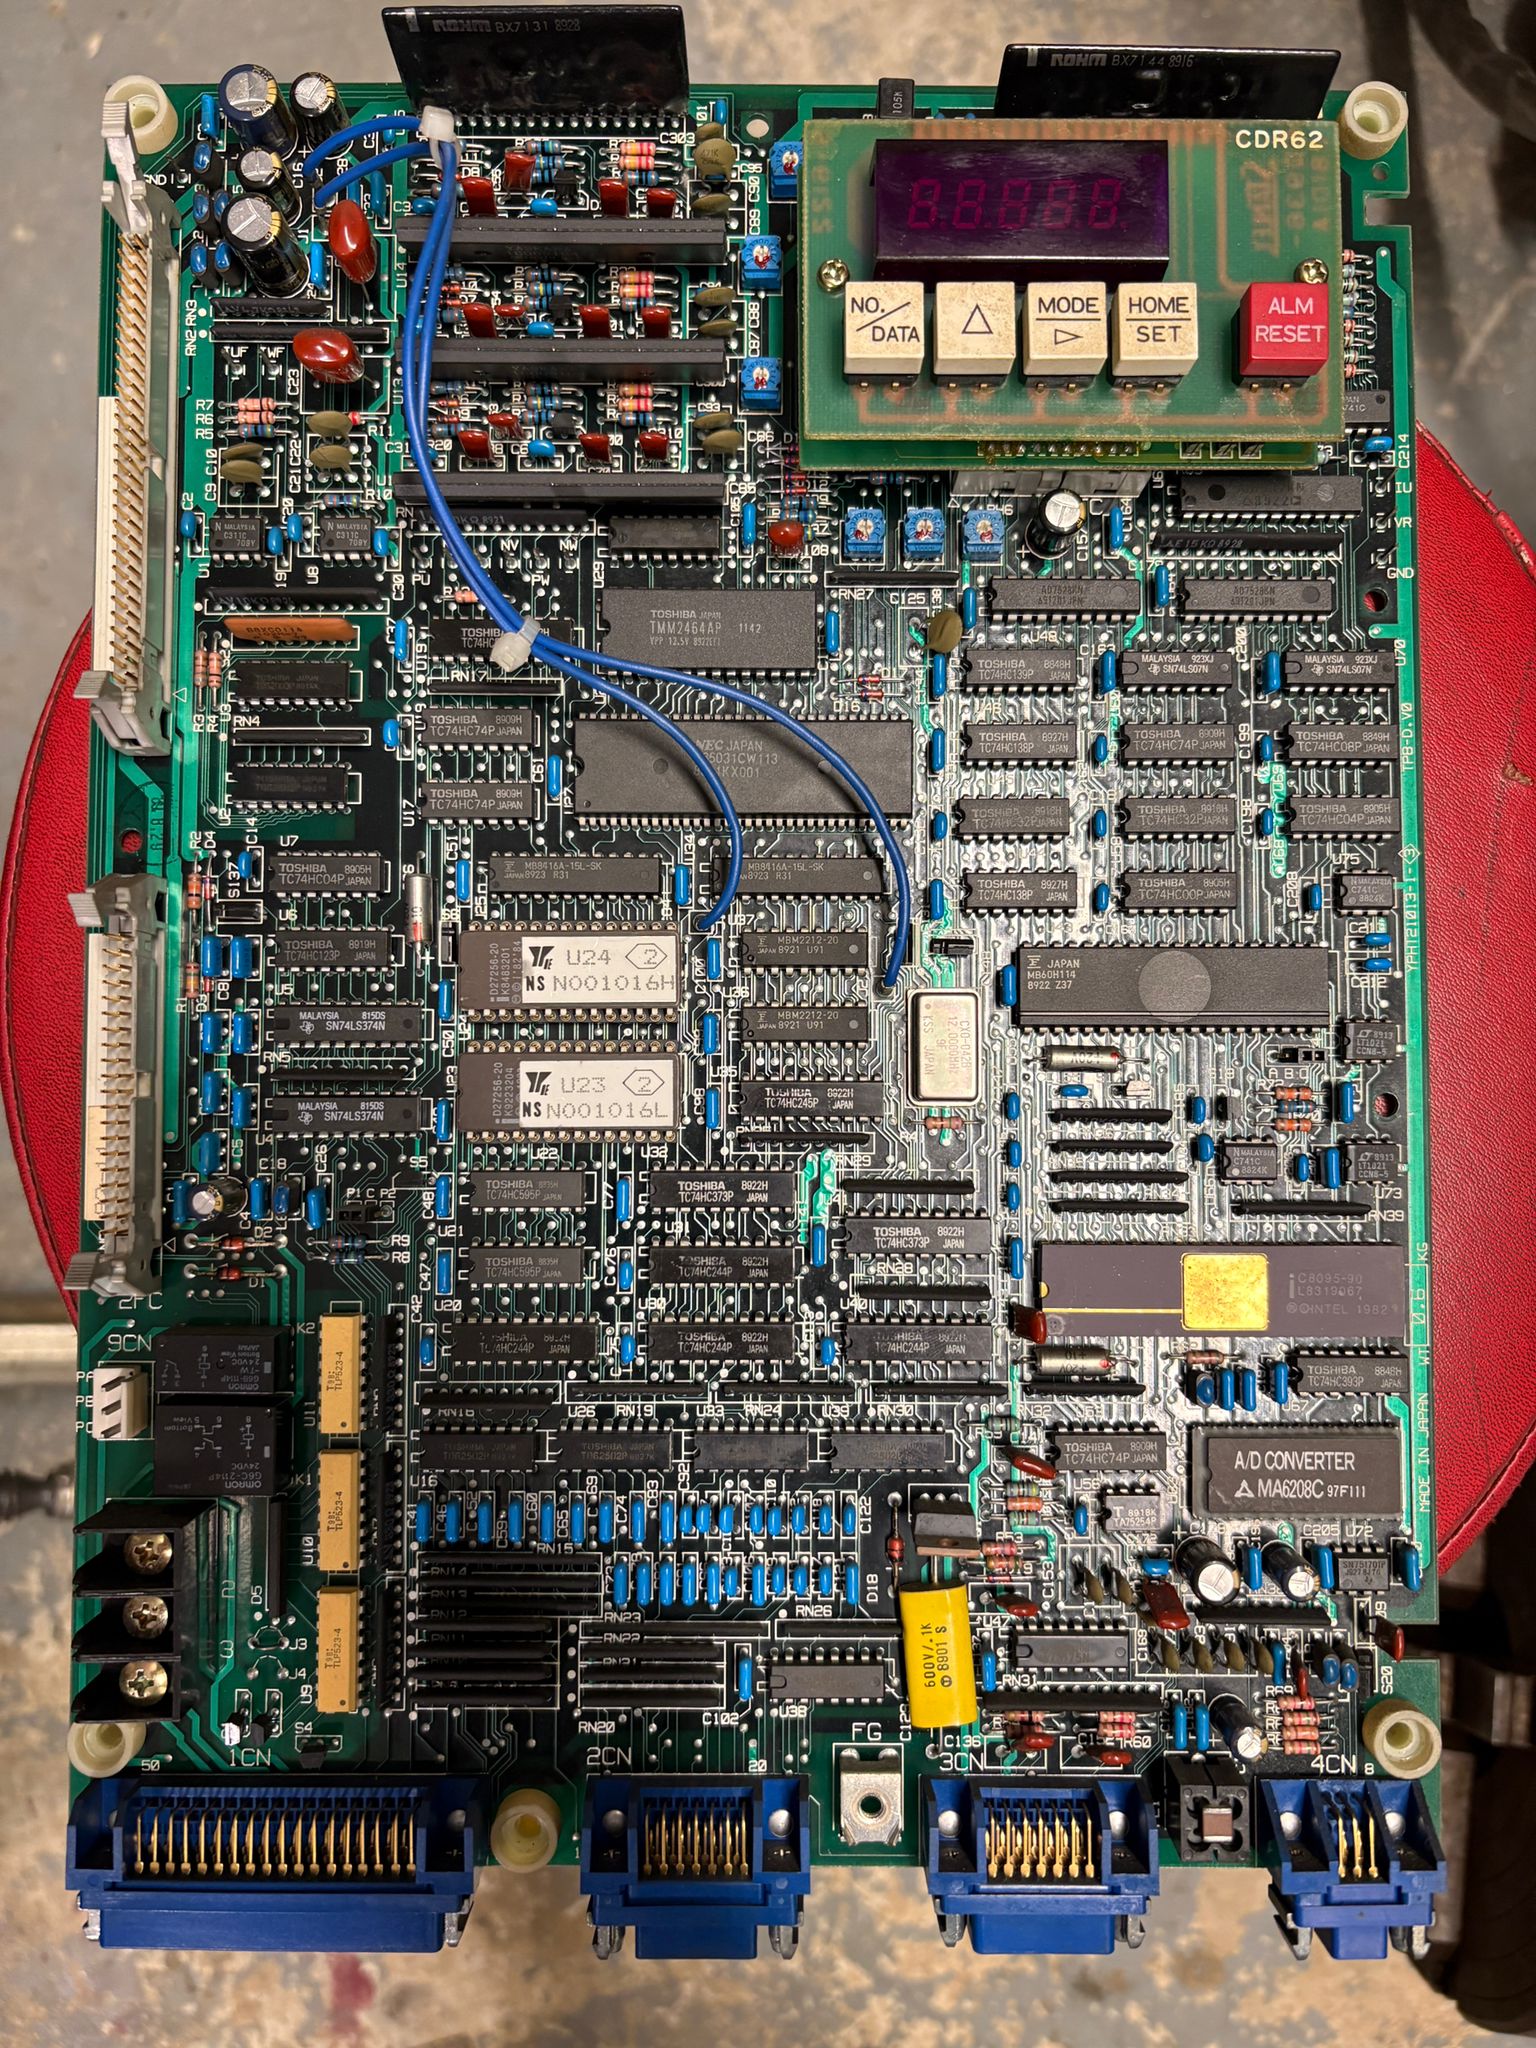
Right now, the Yaskawa spindle inverter is giving me a bit of a headache. Perhaps there is someone here who can tell me how to connect the output signals—as shown in the pictures—within the Mesa card.
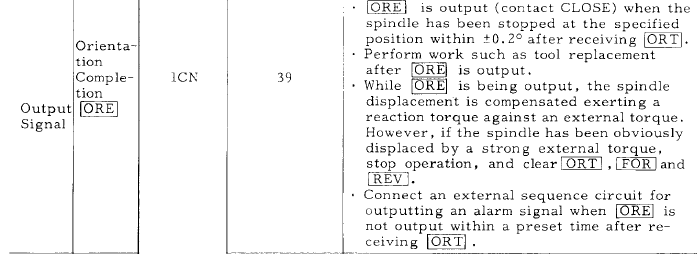
As an example: the spindle orientation function uses signal contact 39, while contact 41 serves as the common (COM). As soon as I initiate the spindle orientation and the process is complete, the VFD outputs the signal via contact 39. To verify this, I can see on the VFD's display that the signal is being generated internally; however, I am having trouble reading this signal with the Mesa card.
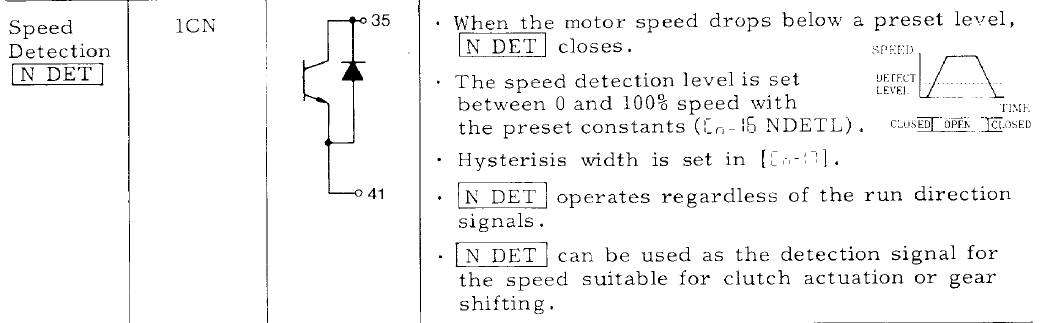
Another example would be speed detection. How is the signal processed?
What is the difference between Signal 34 and 35?