2 seperate MPG handwheels for each axis - CNC Lathe build

More
6 years 5 months ago - 6 years 5 months ago #168035 by denhen89
I am not at home right now, but I wrote just minutes ago quiet a lot on my phone but when I posted it I got a "kunena internal error". As soon as will be back at home i will reply to all your answers.
Last edit: 6 years 5 months ago by denhen89.

Please Log in or Create an account to join the conversation.

More
6 years 5 months ago #168039 by denhen89
Alright, i am back at the test PC.

@PCW: Thanks for that! Now i do understand that the input pins 16 and 17 dont need to be somewhere in the HAL, because those pins are already linked with "hm2_7i76e.0.7i76.0.0.enc0.count". Correct?

To count, the inputs must swing below 2V and above 3V relative to field ground

So, 4.10V is totally fine.

@rodw: I have read your build thread many times, really, but my problem is, i have no switches at all, so i dont know what i have to change in the HAL so that the MPG is always active just to test it.

The only thing I thought of is that if you don't have the axis select switch installed, you might have to setp the MPG scale pin to a value. If it is 0 , nothing will happen.

Thats a good point. Make sense for me, but again i dont know what i have to enter/change in the HAL to set one scale which is always active, so that no switches are needed.

It seems that i would need to study all those codes for linuxcnc and the complete MESA 7i76e manual or so, but i want to be honest: I want a working machine and not be a pro in Linuxcnc setup. Some time ago i wanted to set up a test pc and learn classic ladder etc., but i do not have a lot of time anymore, so i want spent my free time with other things than something which i will not really need a lot in future. Of course i would like to understand the configuration, because later when the mechanical part on the Lathe is done, i want a panel with a switch for the scale change (ordered the same as you have, but i already wrote that i think on page 1). Also i want to have some buttons to start/stop g code, but right now i just do not want to think about it. As soon as i get the switch for the scale and some buttons i will start thinking about that.

In my next post i will precisly explain my current setup, so that it will be easier to help me out.

Please Log in or Create an account to join the conversation.

More
6 years 5 months ago #168042 by rodw
Thats the thing. There is not a dedicated support desk so you need to work a few things out yourself.

Where I said
Code:
net x-jog-scale mux4.0.out => axis.x.jog-scale
Try
Code:
setp axis.x.jog-scale 1

Assuming a metric machine, that will give you a 1mm step. Change it to suit if you are in inches ot it will move 1 inch per click!
I might ad that I di move 1 meter per click once!

Please Log in or Create an account to join the conversation.
More
6 years 5 months ago #168043 by denhen89
So, i just upgraded to Linuxcnc 2.9 pre.
Debian vers. 9

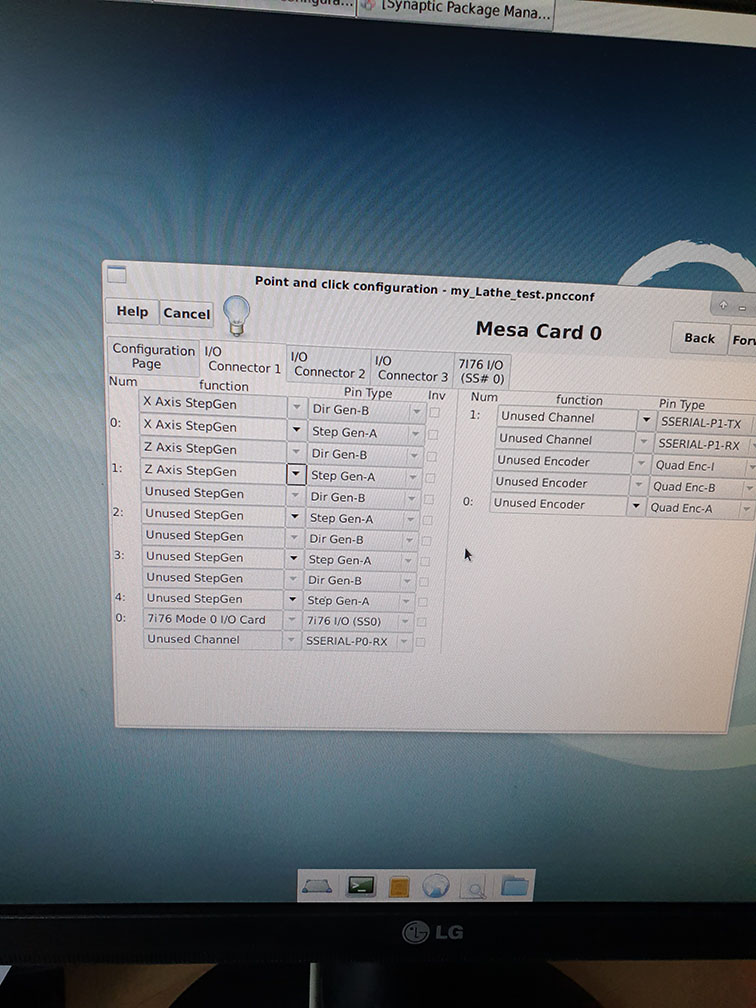
Wiring of MPG to Mesa 7i76e: See picture:

*GND from TB3 Pin 9 is connected to GND of TB3 Pin 23

I used PCCONF to create a RAW setup. See pictures:
Everything else has been not set up and left as default.
After the set up i changed in the HAL the sserial port: sserial_port_0=2xxxx
I attached the .HAL and .INI file

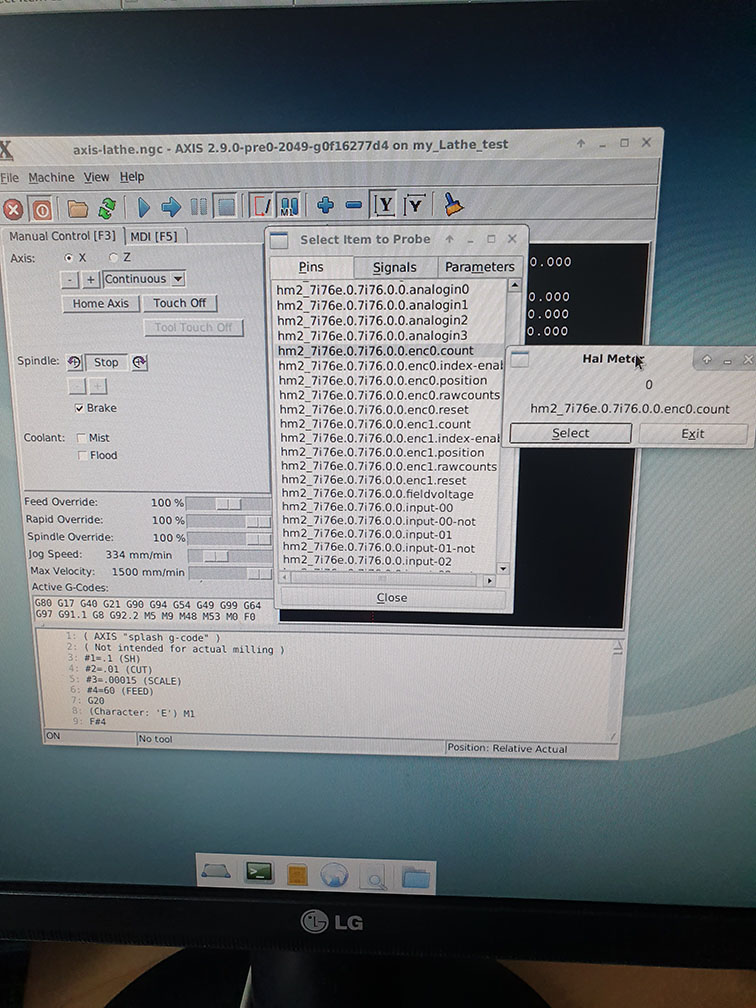
I started Linuxcnc, opened the Halmeter and unfortunately nothing happens when turning the MPG handwheel, no matter which Pins enc0 pins i choose. See picture:
Do i understand it correctly, that if the wiring of the MPG is correct, then something should happen in the Halmeter when selecting the correct Pin ?

To remember: I have no switches to select the scale also no buttons to enable to MPG, so as Rodw wrote, i would need to set a standard scale. Also i would need to have the MPG active without any buttons to press.
I hope that are all informations you need to help me out.
Of course, in meantime until i get some help i will try to get it done by my self and not just wait until someone helps :)

Thanks in advance guys.

Please Log in or Create an account to join the conversation.
More
6 years 5 months ago #168044 by denhen89
@Rodw: Of course i understand to find out a lot of things by my self, but i really tried but its difficult for me.
Thanks for "setp axis.x.jog-scale 1", but if in Halmeter nothing happens when turning the handwheel, then i think that the problem might be in the wiring, or am i wrong ?

Please Log in or Create an account to join the conversation.

More
6 years 5 months ago #168045 by rodw
Can you chexk what I used here
Code:
sserial_port_0=200xxxx

I have a feeling I might have been different.

If the mode is right and it is not counting, then look at wiring.

Please Log in or Create an account to join the conversation.

Time to create page: 0.204 seconds
Powered by Kunena Forum
