Help needed to get my 7i76E + 7i85S + 7i73 on my mill going.

More
8 years 1 month ago #117196 by tecno
Code:
motor_speed_out = speeds[13] * (spindle_speed_in / speeds[i+1]);

So now we have some action but S80 is in fact 110rpm at 32.32Hz. We are getting closer.

S445 runs at 598rpm

Please Log in or Create an account to join the conversation.

More
8 years 1 month ago #117197 by tecno

Hakan wrote: I know, but there is no code to set different max speeds when the pin is high or low.
I added that code.


# Motor High
net motor-high-signal <= GB-2speed.0.motor-high
net motor-high-signal => hm2_7i76e.0.7i76.0.0.output-10

Gear setting 10-11-12-13 should activate above as I understood this.

Please Log in or Create an account to join the conversation.

More
8 years 1 month ago - 8 years 1 month ago #117198 by tecno

tecno wrote: As a side note, homed all my axis and suddenly X is out of order.

Power on but not stiff as I can rotate shaft by hand = no error message on driver.
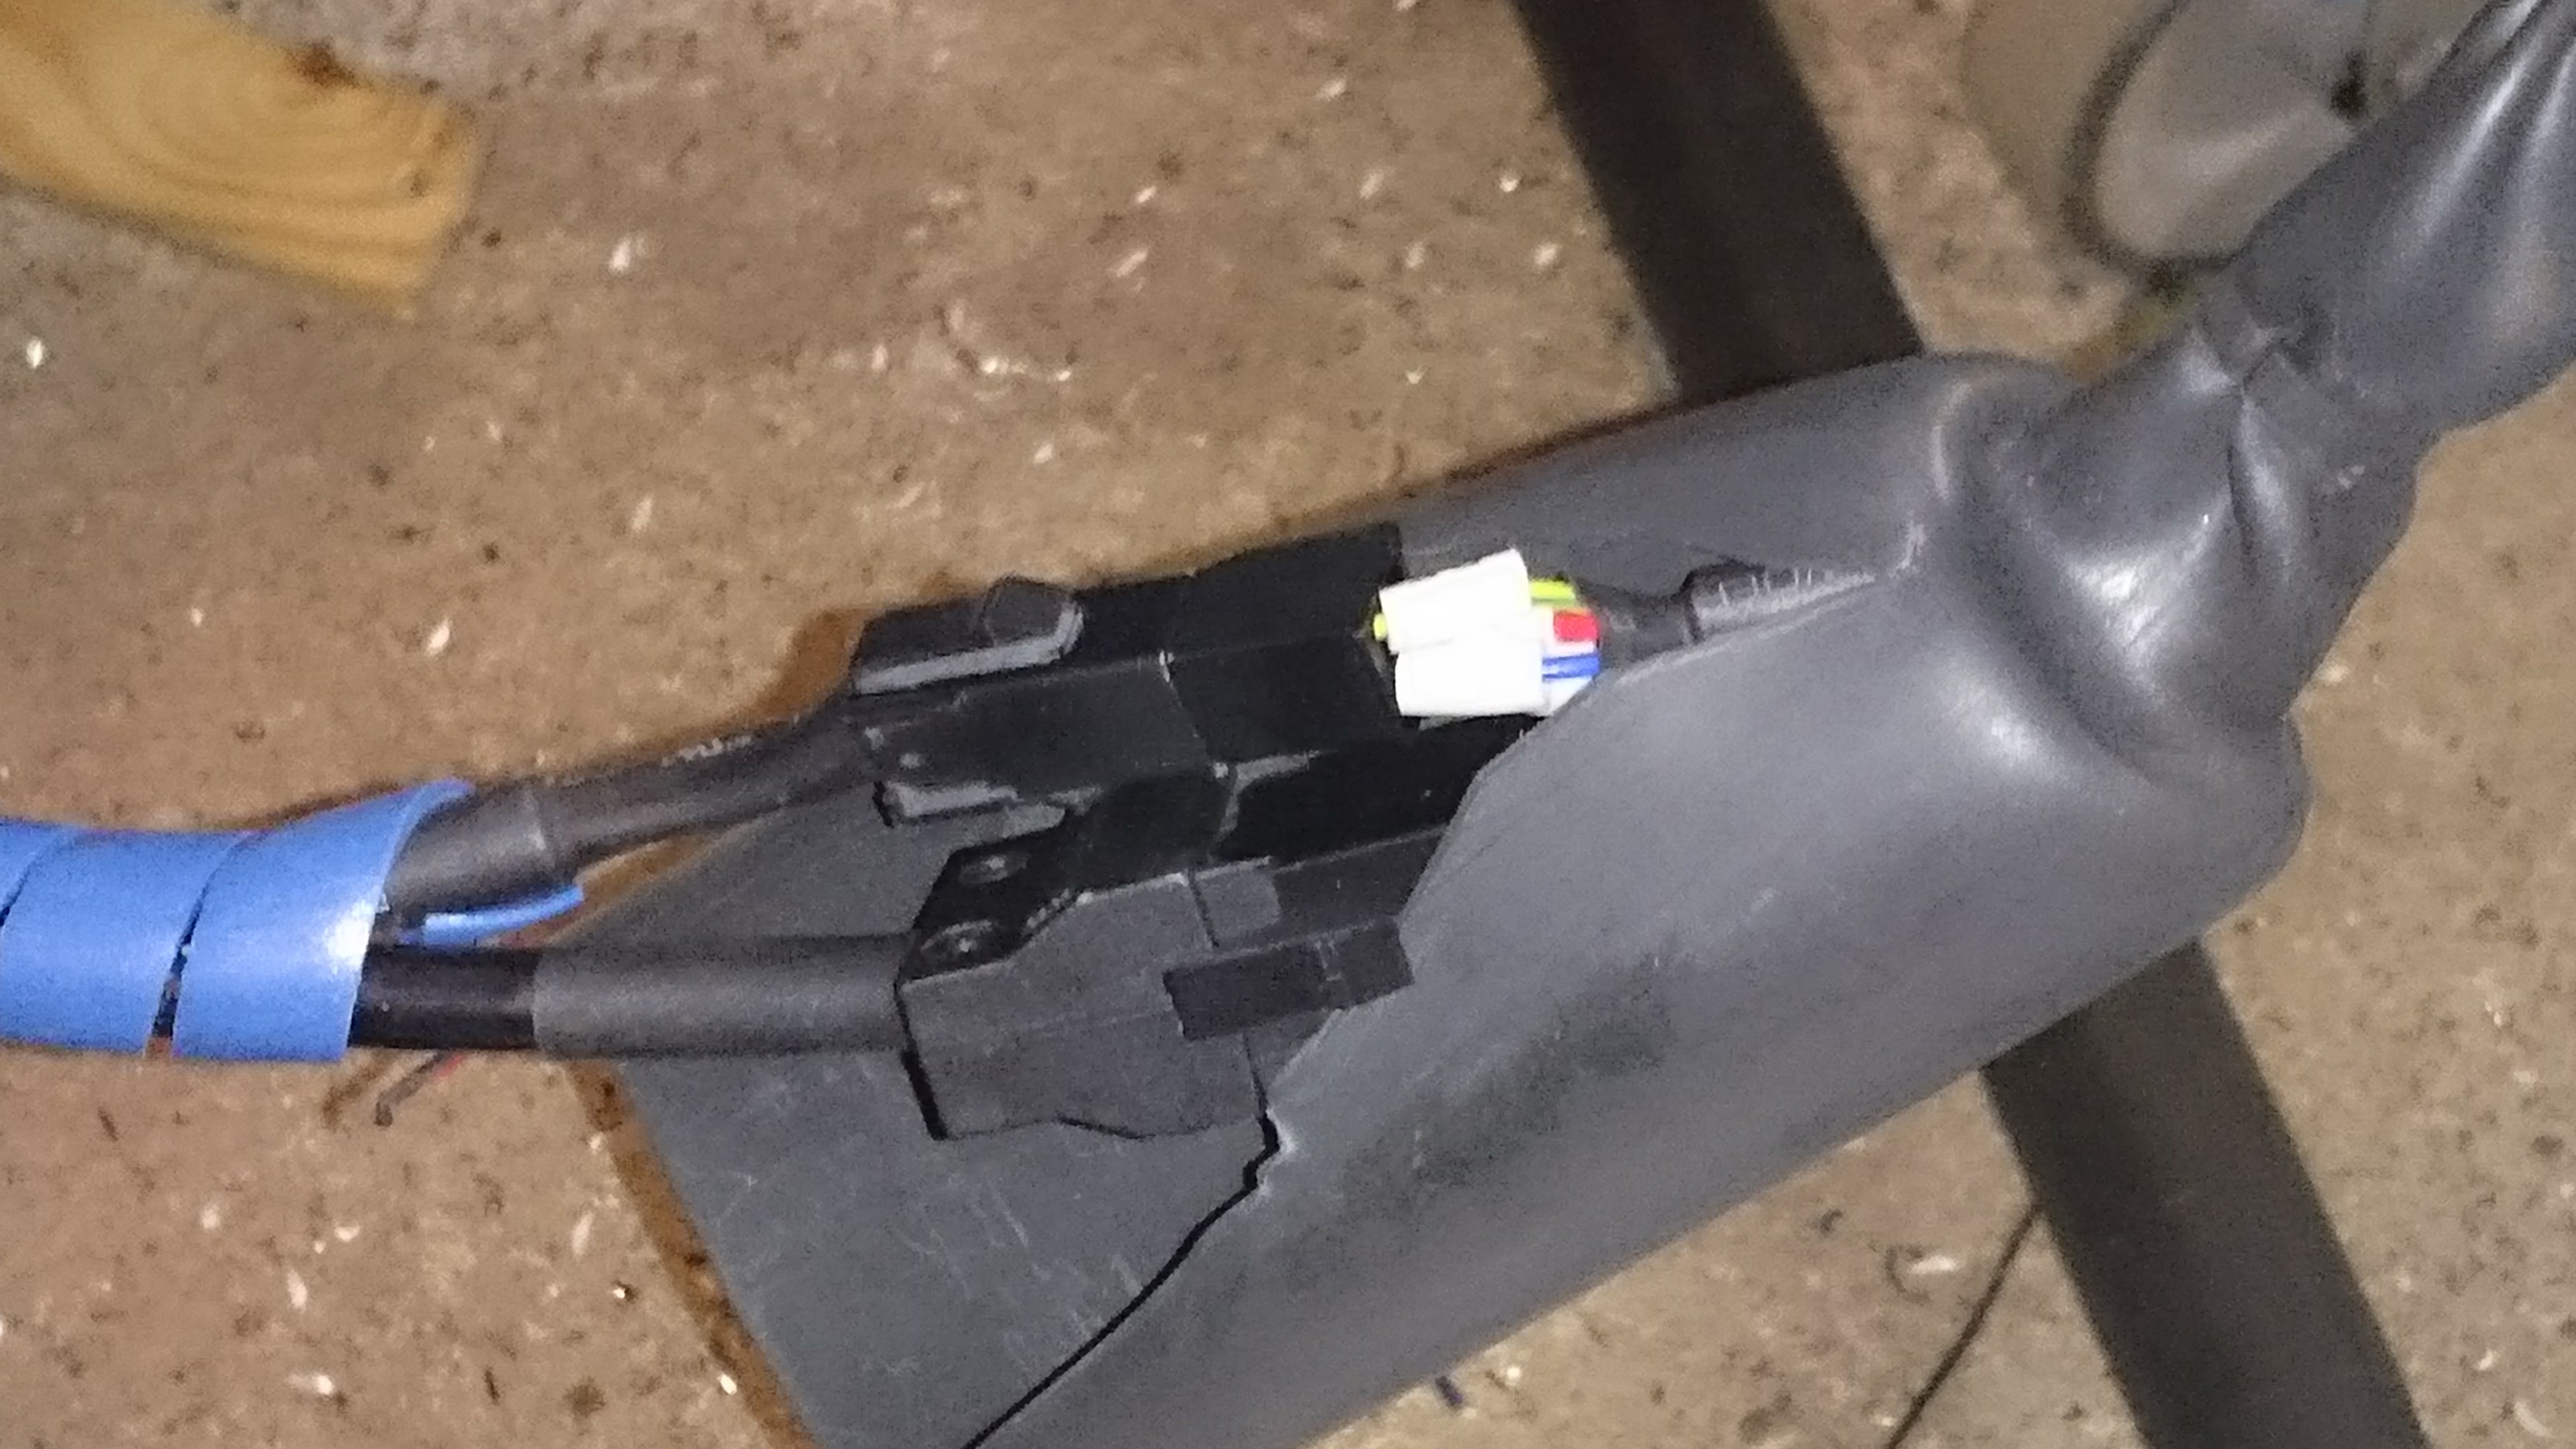

I found the error = SHIT CONNECTORS!!!!!!
From motor there is a fixed cable and ends in 4-pole connector = bad hooks !! So now I have to do something that fixes this this connection SOLID!

Last edit: 8 years 1 month ago by tecno. Reason: added jpg

Please Log in or Create an account to join the conversation.

More
8 years 1 month ago #117199 by Hakan

tecno wrote:

Hakan wrote: I know, but there is no code to set different max speeds when the pin is high or low.
I added that code.


# Motor High
net motor-high-signal <= GB-2speed.0.motor-high
net motor-high-signal => hm2_7i76e.0.7i76.0.0.output-10

Gear setting 10-11-12-13 should activate above as I understood this.


This is not what I call code. These are hal connections.

There is no code in the comp to use anything but 2500 rpm as the max speed.
Add the four lines. Or Andy maybe has an other idea how to do it.

Please Log in or Create an account to join the conversation.

More
8 years 1 month ago - 8 years 1 month ago #117201 by tecno
Will the 4 lines handle output 10 when needed?
Code:
FUNCTION(_){ int actual, message, double motor_max_speed; int i; // These need to be edited to suit the gearbox int speeds[15] = {0, 80, 125, 160, 215, 270, 360, 450, 595, 750, 1000, 1191, 1500, 2500, 0x1P30}; int reqd_gear[15] = {0x0, 0x01, 0x21, 0x02, 0x22, 0x04, 0x24, 0x08, 0x28, 0x10, 0x48, 0x68, 0x50, 0x70, 0x0}; if (spindle_speed_in == 0) return; actual = (gear_high * 0x40 + motor_high * 0x20 + gear_A * 0x10 + gear_B * 0x08 + gear_C * 0x04 + gear_D * 0x02 + gear_E * 0x01); for (i = 0; spindle_speed_in > speeds[i] && i < 14; i++); gear_required = reqd_gear[i]; if (gear_required == actual && gear_required != 0x0){ // We are in the right gear spindle_enable_out = spindle_enable_in; if (motor_high) motor_max_speed = 2500; else motor_max_speed = 1450; motor_speed_out = speeds[13] * (spindle_speed_in / speeds[i+1]);
Last edit: 8 years 1 month ago by tecno. Reason: added text

Please Log in or Create an account to join the conversation.

More
8 years 1 month ago #117212 by Hakan
Almost, the "speed[13]" on the last line needs to be replaced as well.

Check forum.linuxcnc.org/39-pncconf/33069-help...ing?start=640#117193

If you have a different max speed than 1450 you can just change to whatever is the max speed.

Please Log in or Create an account to join the conversation.

Moderators: cmorley
Time to create page: 0.257 seconds
Powered by Kunena Forum
